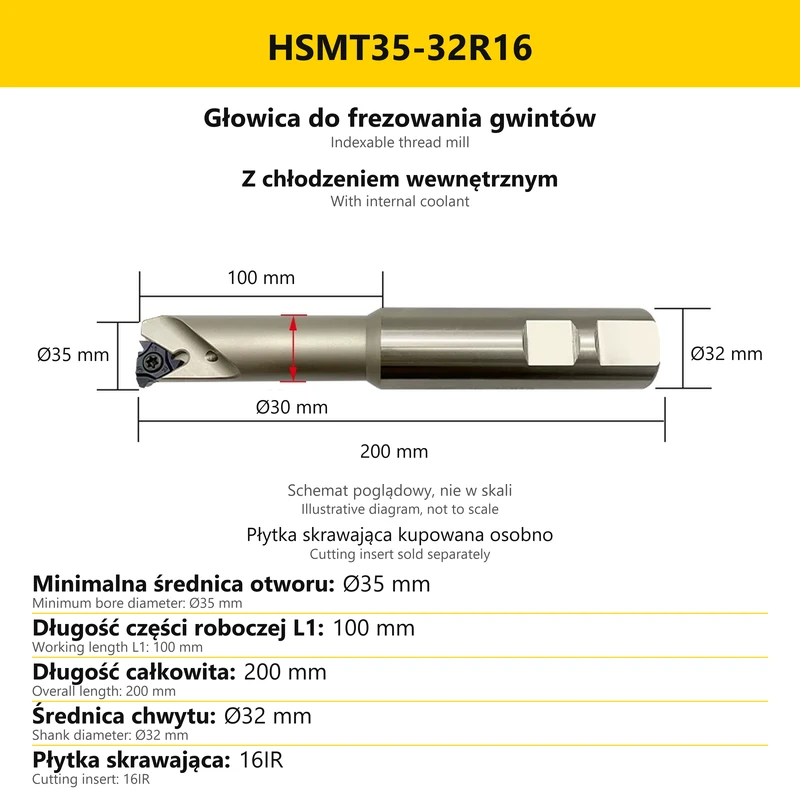
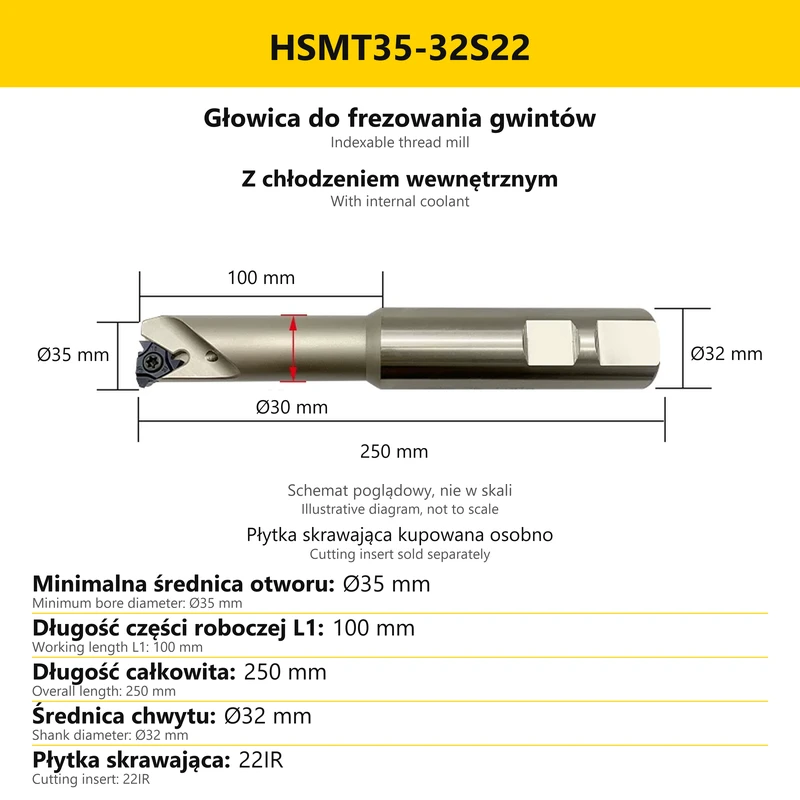


HSMT threading head – for IR inserts (08IR / 11IR / 16IR / 22IR)
Shipping costs are not included in the price.
Shipping costs are not included in the price.

Weekly deals
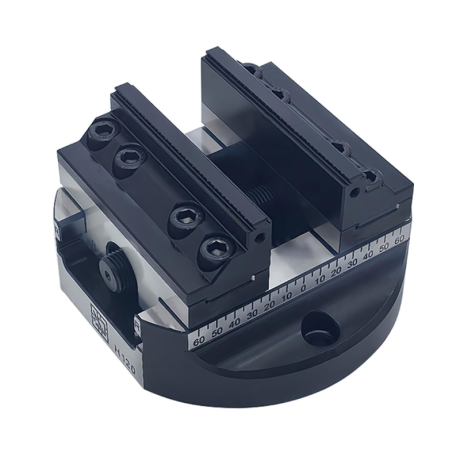
5-axis vise with hard jaws
Self-centering machine vise. Hard jaws included.
excl. VAT
Regular price:
Lowest price in the 30 days before the reduction:
Time left
Offer ends 06.11.2026 23:59. Offer applies to the vise + hard jaws bundle only.
Ask about the product

The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: F122-2493A
Product description
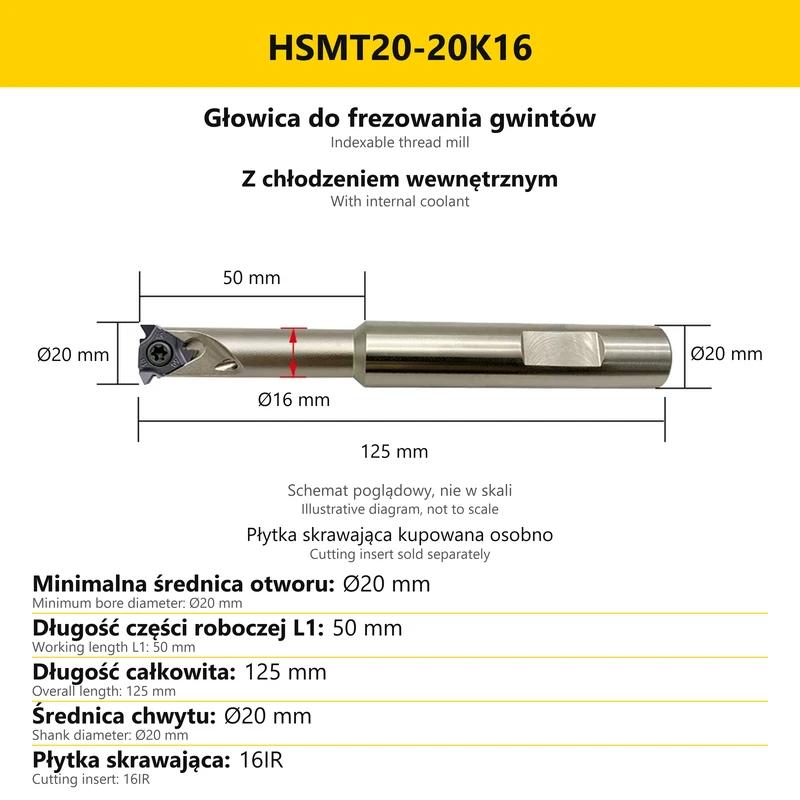
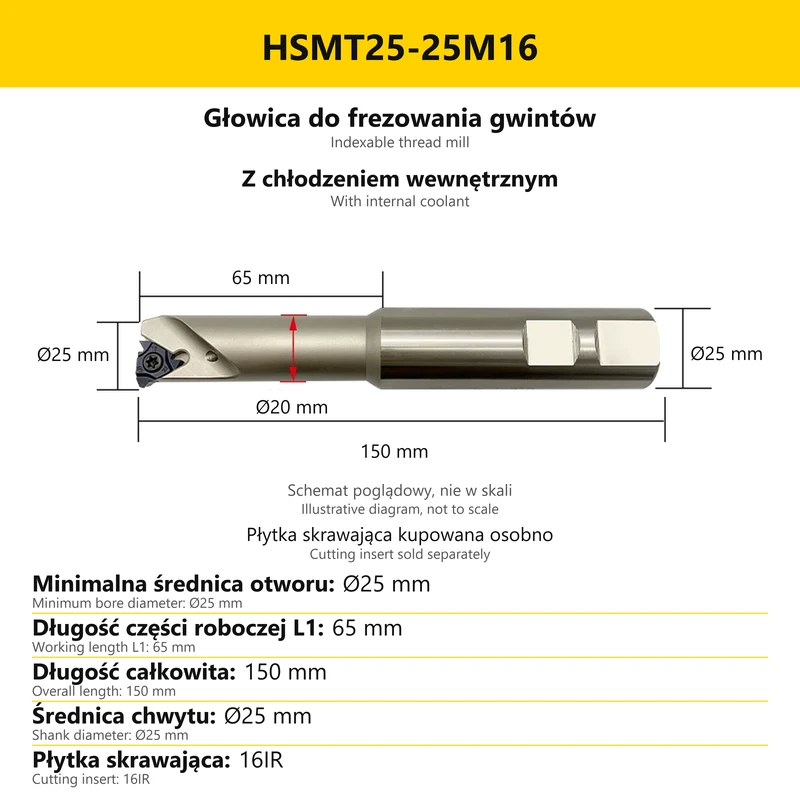
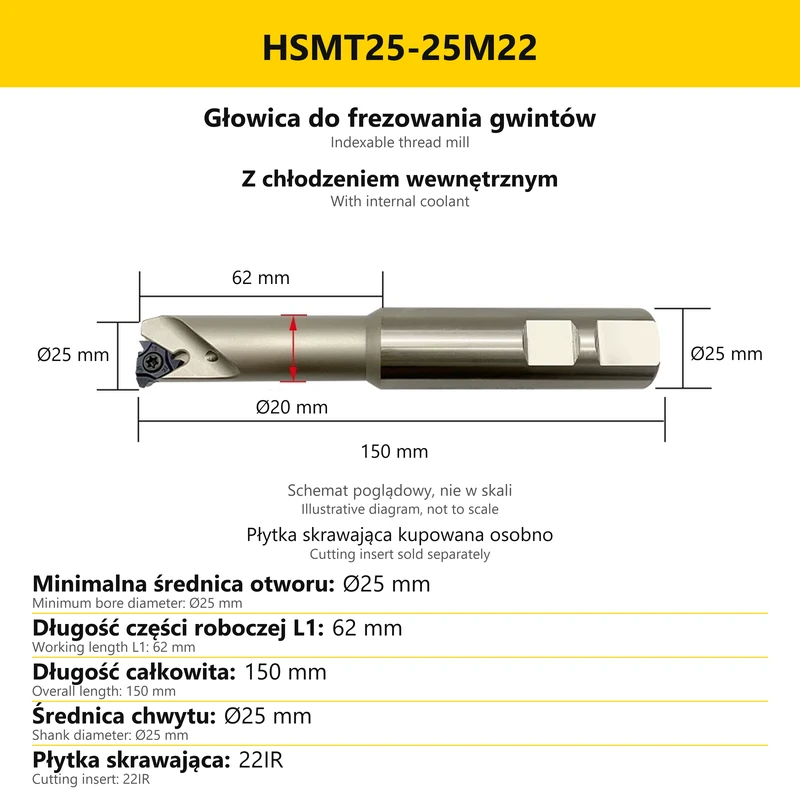
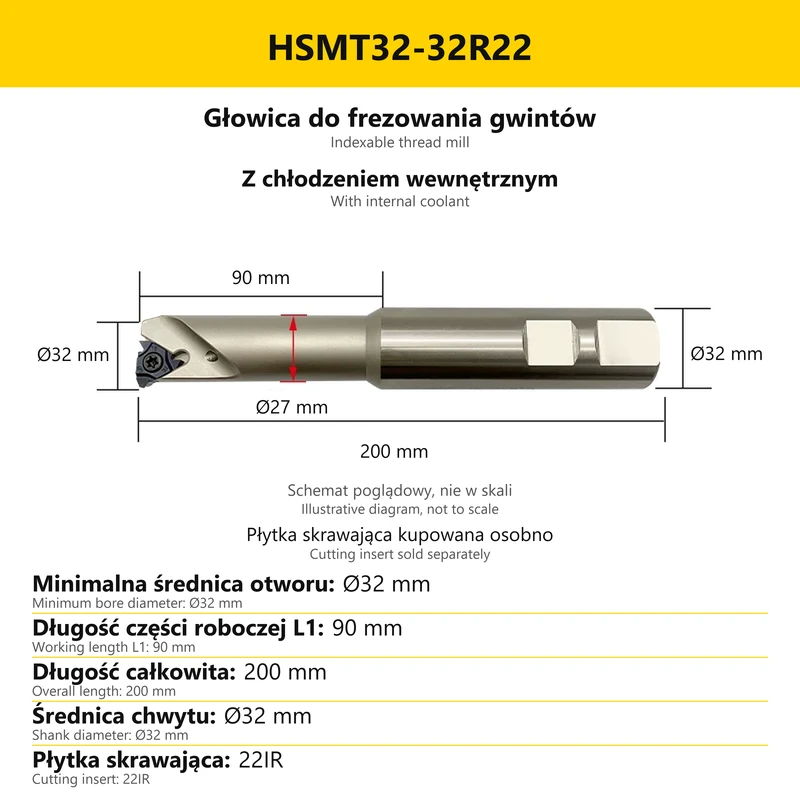
HSMT indexable thread mill
HSMT is a shank-type tool for CNC thread milling, using a replaceable threading insert secured by a central screw. The family supports internal and external threads when the insert and machining path are selected appropriately. The body is made of vacuum-hardened 42CrMo alloy steel.
The selected option defines minimum bore diameter, body dimensions, insert size and coolant version. Bodies with and without internal coolant are available.
The purchase is one body in the selected size, without a cutting insert. The installed insert in the photograph illustrates seating; purchase the insert separately. The card for the selected option states the required IR insert size.
Applications and workpiece materials
The tool is used for thread milling on CNC machining centres. Right-hand or left-hand threading requires an appropriate insert and a correctly programmed machining path. The body designation does not replace selection of thread profile, pitch or insert version for the workpiece material.
| Workpiece material | Selection requirement | Application scope |
|---|---|---|
| Structural, alloy and mould steels | Suitable IR insert grade and geometry | Thread milling using an insert intended for the particular steel |
| Stainless steel | An insert version for stainless steel | Account for the material when selecting the edge and operating conditions |
| Aluminium, aluminium alloys, copper and non-ferrous metals | An insert suitable for the particular material | Insert application must be considered separately from body material |
| Cast iron and titanium alloys | An appropriate insert version | A common seat size does not give every insert the same grade |
| Plastics | Geometry and operating conditions suited to the workpiece | Selection must also account for the particular plastic |
The body holds the insert and transfers milling loads, while the insert edge generates the thread. Therefore, 42CrMo steel and body hardness do not mean that any insert can machine every listed workpiece material. Select cutting conditions for the particular tool assembly.
Body construction and technical data
| Parameter | Construction | Meaning |
|---|---|---|
| Family | HSMT | Shank-type tool for thread milling |
| Body material | 42CrMo alloy steel | Structural body material, separate from insert material |
| Body hardness | 30–45 HRC | This is not permissible workpiece hardness |
| Body processing | Vacuum hardening and grinding | Vibration resistance and preparation of mounting surfaces |
| Insert fastening | Central screw | The insert is supported by its intended seat |
| Cutting arrangement | One working insert | The insert is the replaceable cutting component |
| Insert system | 08IR, 11IR, 16IR or 22IR | Match the size to the particular body option |
| Purchase item | One body without an insert | Cutting inserts sold separately |
The rigid body is adapted for continuous operation; ground surfaces provide stable mounting. The seat locates the insert and the central screw retains it against its support surfaces. Working-part geometry provides space for chip evacuation.
When replacing an insert, check seat cleanliness and correct contact with the support surfaces. The body and fastening component must be in a condition that allows the cutting edge to seat correctly. A replaceable insert can be changed without replacing the complete body.
Reading the dimensions on an option card
| Designation | What it describes | Use when selecting |
|---|---|---|
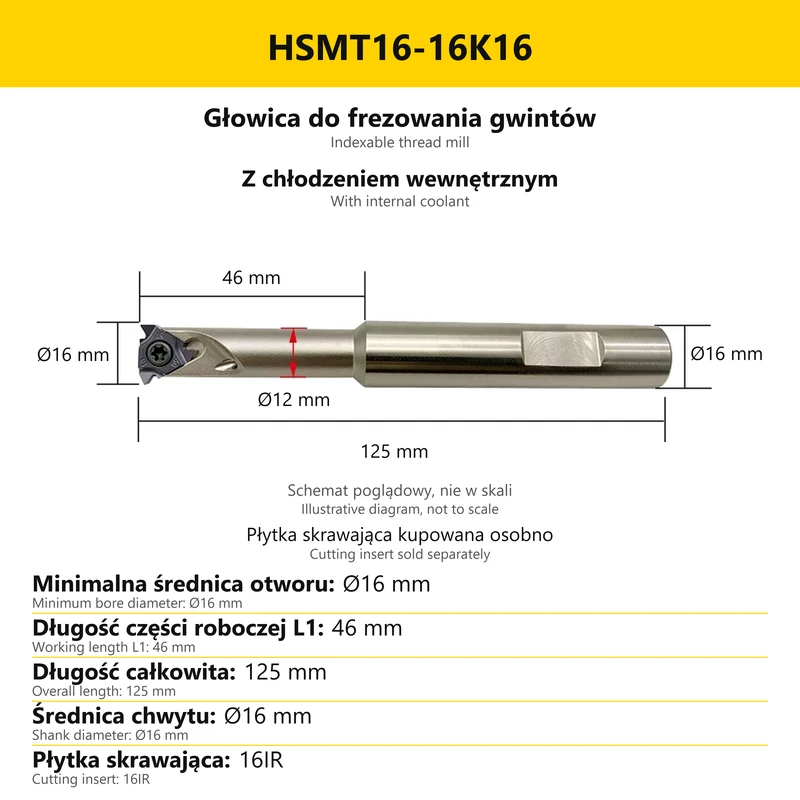
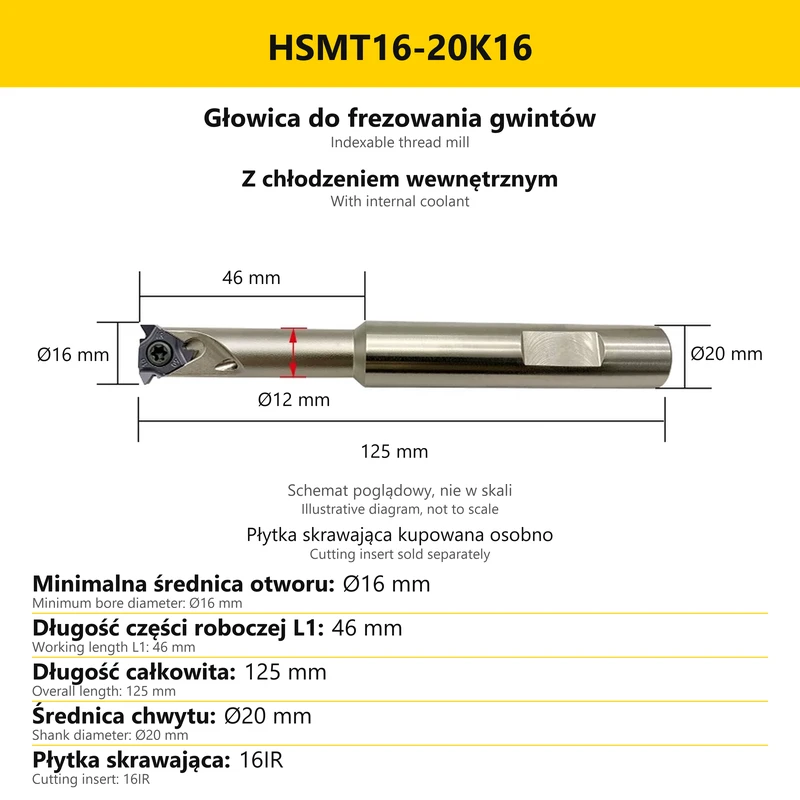
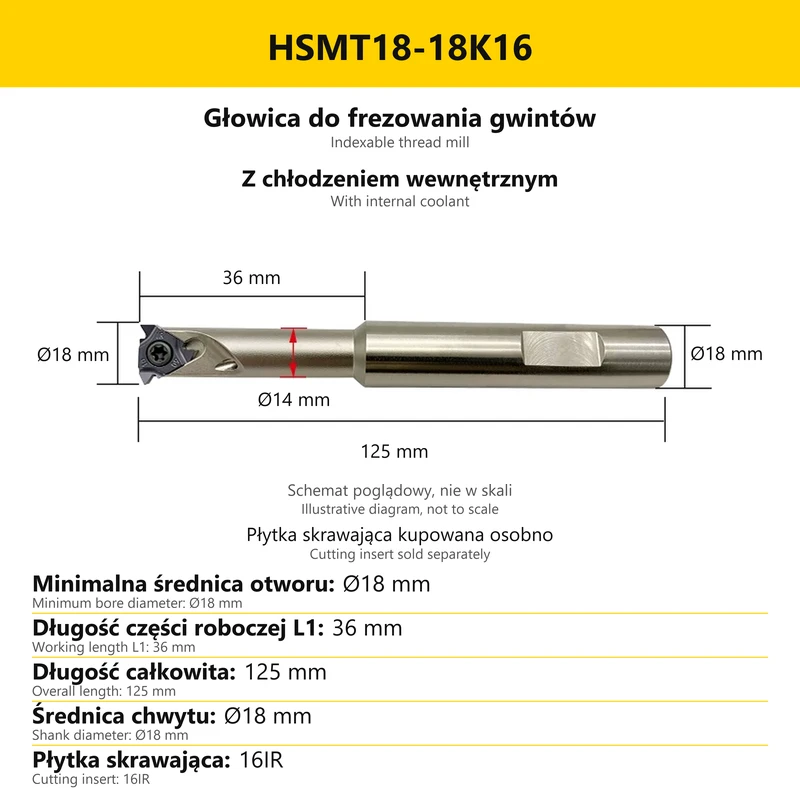
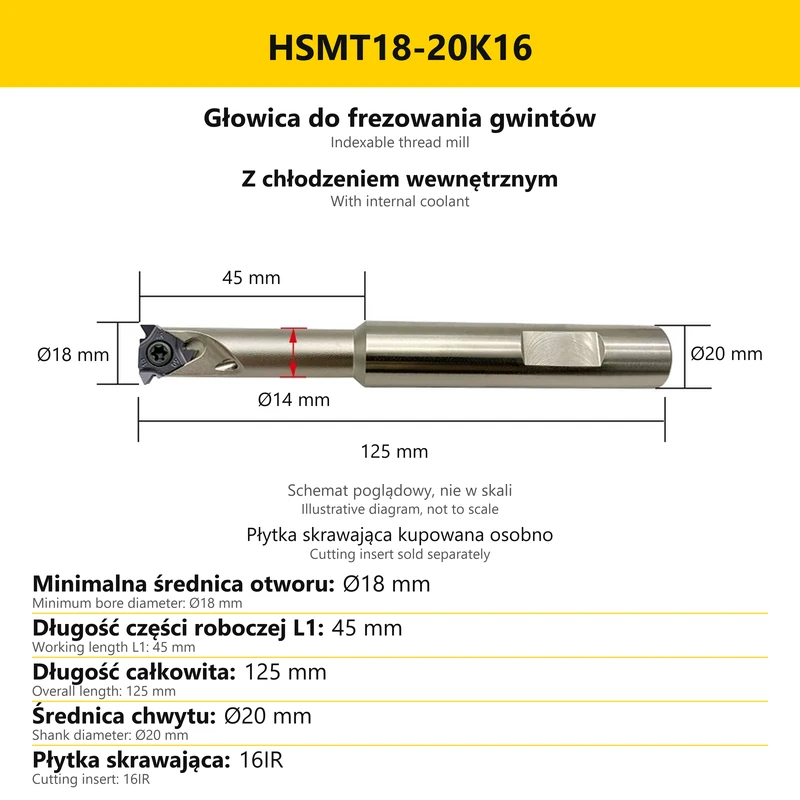
| Dmin | Minimum bore diameter | Check this dimension when selecting for an internal thread |
| L1 | Working-part length up to the body shoulder | A separate dimension from overall tool length |
| L | Overall length | Complete tool length including the shank |
| d | Shank diameter | Match the mounting diameter to the holder |
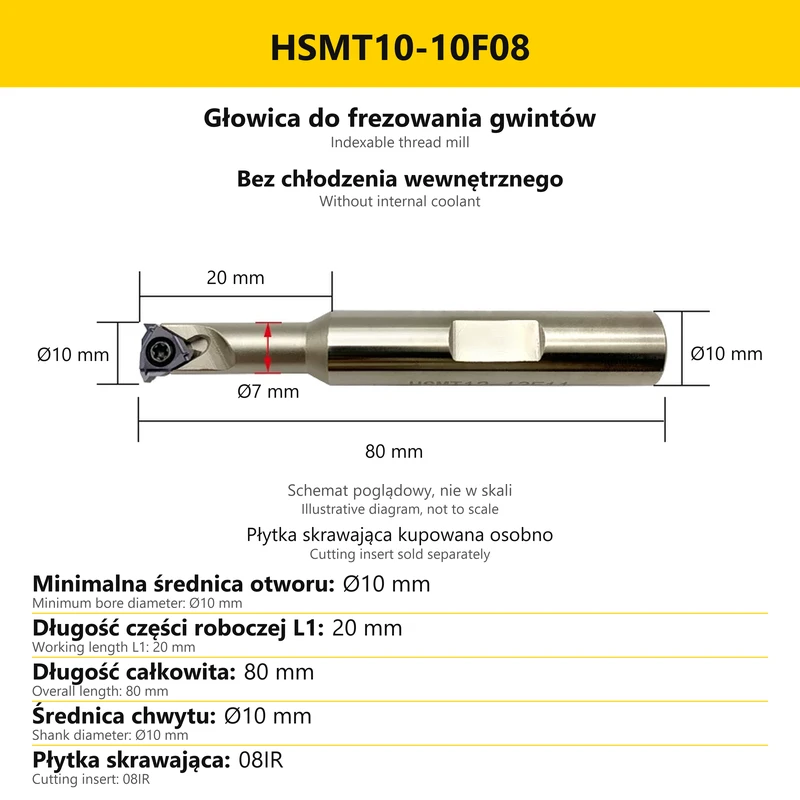
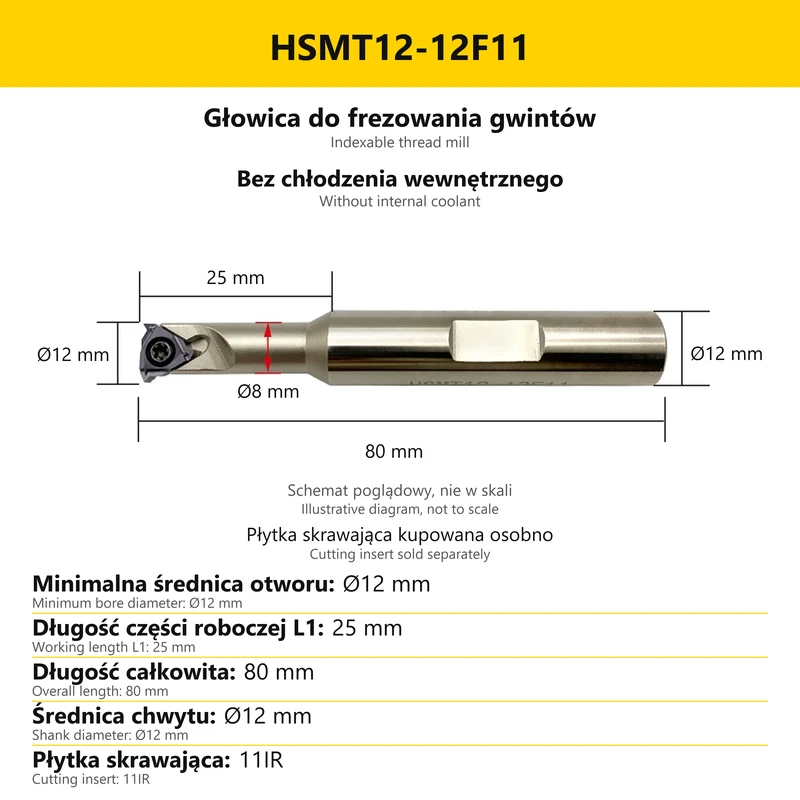
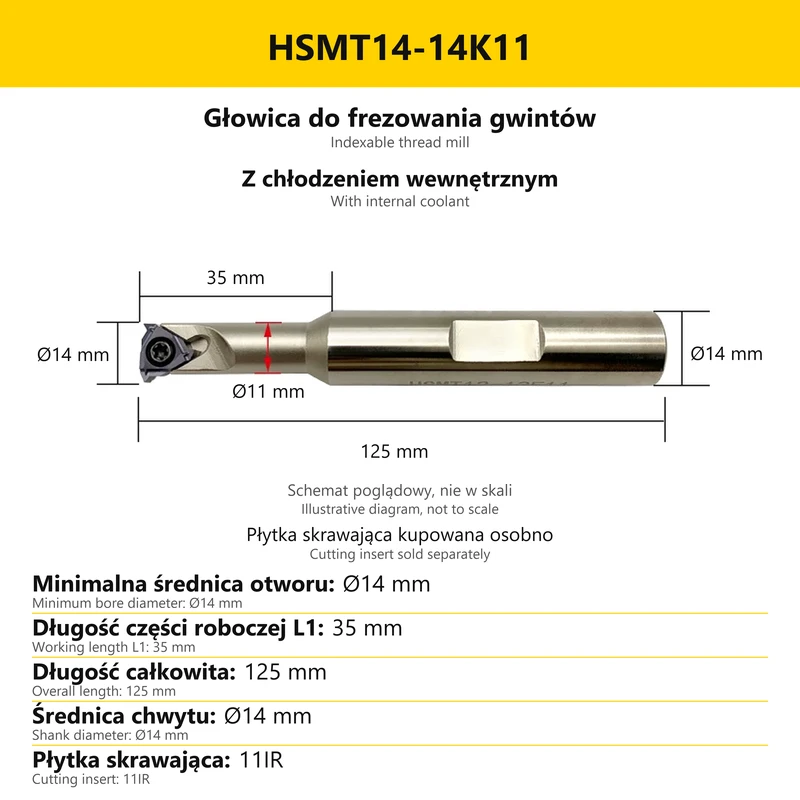
| Neck diameter | Reduced working-part diameter | The dimension shown with a separate line beside the tool photograph |
Dmin is minimum bore diameter, rather than cutting diameter or shank diameter. These quantities must not be used interchangeably. The card also shows working-part length, overall length and neck diameter so that the complete dimensions of the selected version can be compared.
Choose the size using the product option selector. The card heading and dimension-line values refer to the particular body. The diagram is illustrative, not to scale.
IR inserts and purchase contents
| Insert size | Body selection | What to check before ordering |
|---|---|---|
| 08IR | For a seat designated 08IR | Complete version, thread profile and pitch |
| 11IR | For a seat designated 11IR | Size compatibility with the particular body |
| 16IR | For a seat designated 16IR | Grade and geometry suitable for the workpiece |
| 22IR | For a seat designated 22IR | Complete insert designation and correct seating |
The sizes 08IR, 11IR, 16IR and 22IR are assigned to corresponding body options. This does not mean that one body accepts all four sizes. Use the size specified on the selected option card, then match the complete insert version to the thread and workpiece material.
The IR family designation alone does not specify the grade, coating or profile of every insert. Consider thread hand and tool-path direction together with the insert and machining program. Insert colour in the photograph is not sufficient information for ordering.
Coolant and version identification
The family includes versions without internal coolant and versions with coolant channels. The card identifies coolant construction separately for each size in Polish and English. Before ordering, compare this information with the option code and dimensions.
- The version without internal coolant does not supply coolant through body channels.
- The internal-coolant version requires coolant supplied through a suitable mounting assembly.
- Insert size does not identify coolant construction; read the selected body version.
Mist cooling or an air blast can be used when machining steel. Match the coolant arrangement to the insert and machining conditions, and treat internal channels as a construction feature of the particular body.
Mounting, runout checks and preparation
| Operation | Principle | Scope |
|---|---|---|
| Runout check before cutting | Measure runout with the tool mounted | Runout greater than 0.01 mm must be corrected before machining |
| Tool overhang | Keep projection from the holder as short as possible | Longer overhang requires reducing speed, feed or the amount of cut |
| Unusual vibration or noise | Reduce speed and the amount of cut | Adjust conditions until the machining behaviour improves |
| Cutting-parameter selection | Match the insert, workpiece and mounting | Settings do not follow from body size or the HSMT name alone |
| Machine type | CNC milling machine | The tool is not intended for bench or hand-held drilling machines |
The 0.01 mm value is a pre-machining runout check threshold. It does not state guaranteed body accuracy or finished-thread accuracy. The measurement concerns the tool in the holder being used and must be checked before cutting.
Overall tool length is not the same as projection beyond the holder. Preparing the operation includes a matching holder, the shortest practical overhang and correct insert seating. Adjust conditions if vibration or unusual cutting noise occurs.
HSMT selection questions
Is the cutting insert included?
No. An option is one body without an insert. Purchase the IR insert separately in the seat size specified on the option card.
What does Dmin mean?
It is minimum bore diameter. It must not be treated as shank diameter or cutting diameter.
Does every body have internal coolant?
No. The family contains both versions. Check coolant construction for the particular size.
Does each body accept every IR insert?
No. A body option accepts a specified 08IR, 11IR, 16IR or 22IR size. Also match the complete insert version to the thread and workpiece material.
Does 30–45 HRC describe workpiece hardness?
No. It is the hardness of the 42CrMo body. Workpiece suitability depends on the appropriate insert and cutting conditions.
Related products
-
923E-98485Bestseller

 Turning Inserts 0.00
Thread Turning Inserts 16ER 16IR 11ER 11IR 08ER 08IR 22ER 22IR (1 pc)


Bestsellers
-
Bestseller
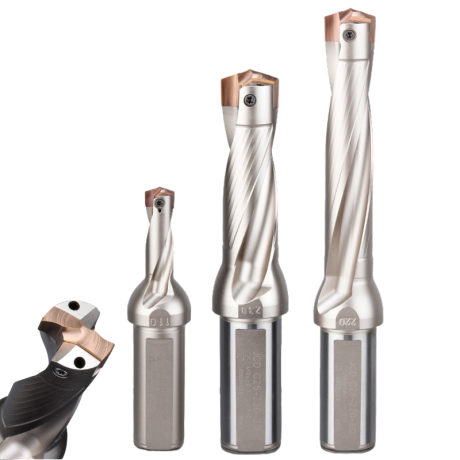
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.52Price €56.52without VAT -
Price €17.09Price €13.90without VAT
-
Price €7.07Price €5.74without VAT
-
Price €7.52Price €6.12without VAT
-
Bestseller
 Other Accessories 0.00
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.56Price €43.55without VAT -
Bestseller
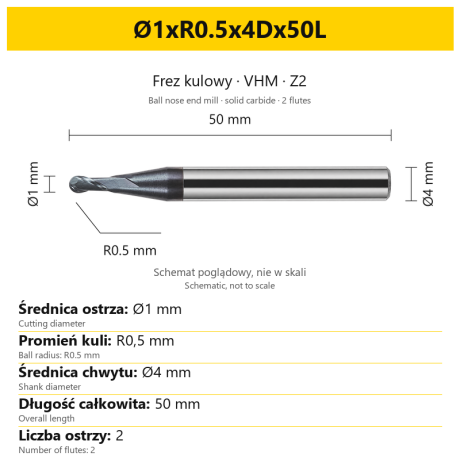 Ball Nose End Mills 0.00
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.09Price €8.21without VAT -
Bestseller
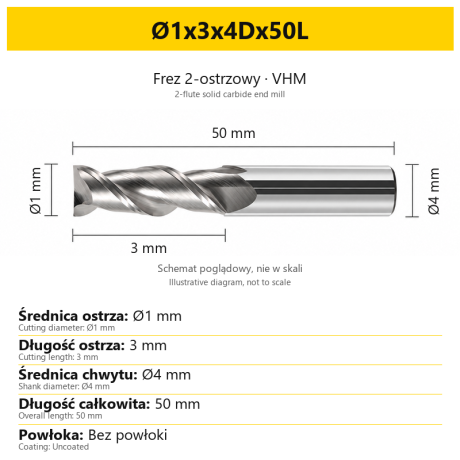 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.33Price €4.33without VAT -
Bestseller
 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.38Price €3.56without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.85Price €6.38without VAT -
Bestseller
 2-Flute End Mills 0.00
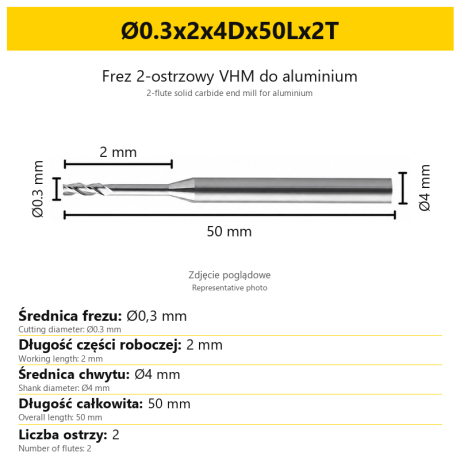
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.95Price €6.47without VAT -
Bestseller
 Ball Nose End Mills 0.00
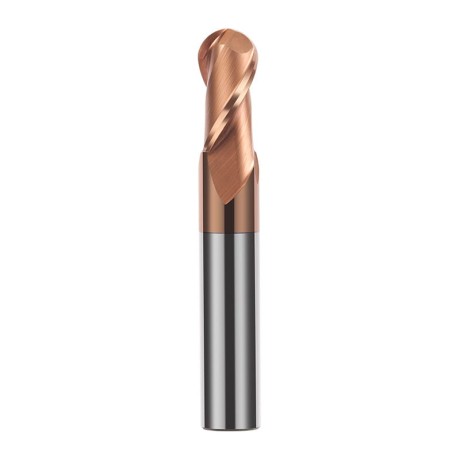
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.24Price €5.89without VAT -
Bestseller
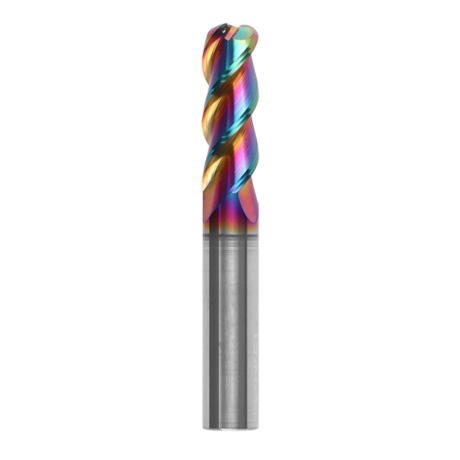
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €5.89Price €4.79without VAT -
Bestseller
 3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.08Price €4.13without VAT -
Bestseller
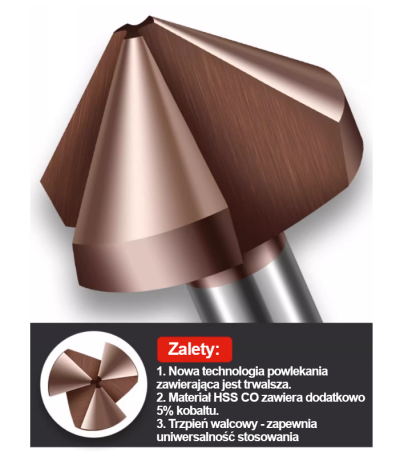 Countersinks 0.00
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.79Price €3.89without VAT -
Bestseller
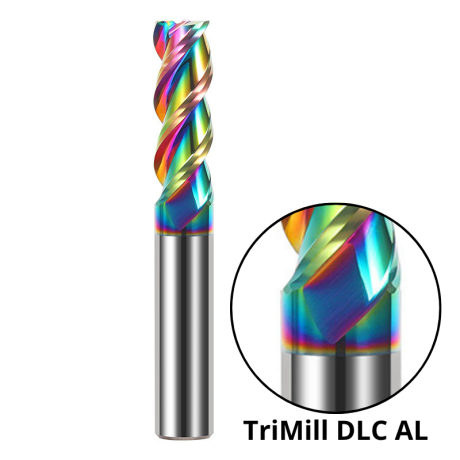
 3-Flute End Mills 0.00
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.05Price €4.10without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute HRC65 DLC Coated Carbide End Mill, U-Shaped Flute, for Aluminium | DuraEdge3 Alu
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 40 morePrice €6.73Price €5.47without VAT