







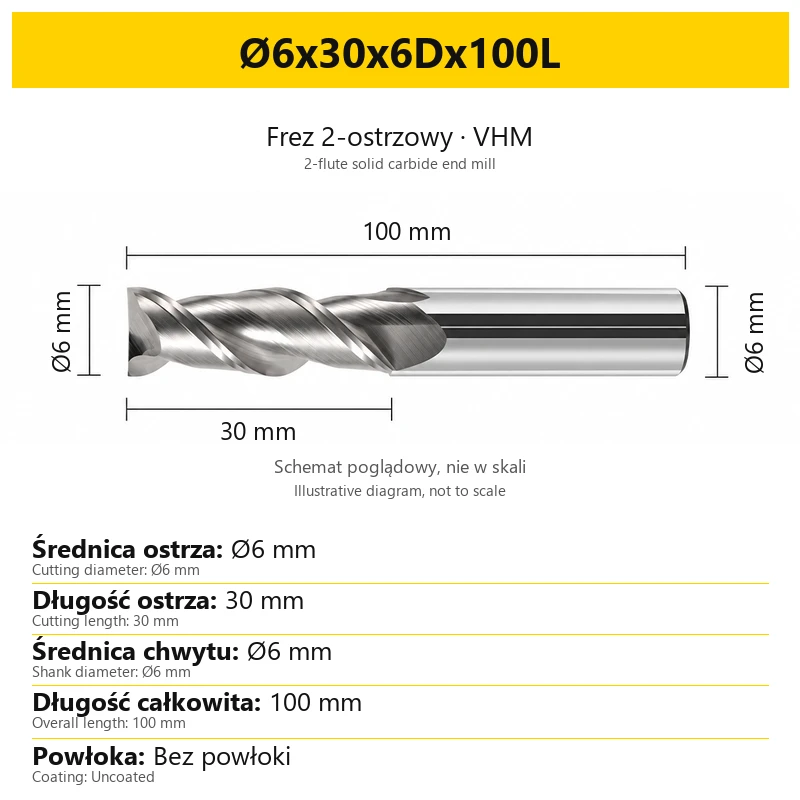

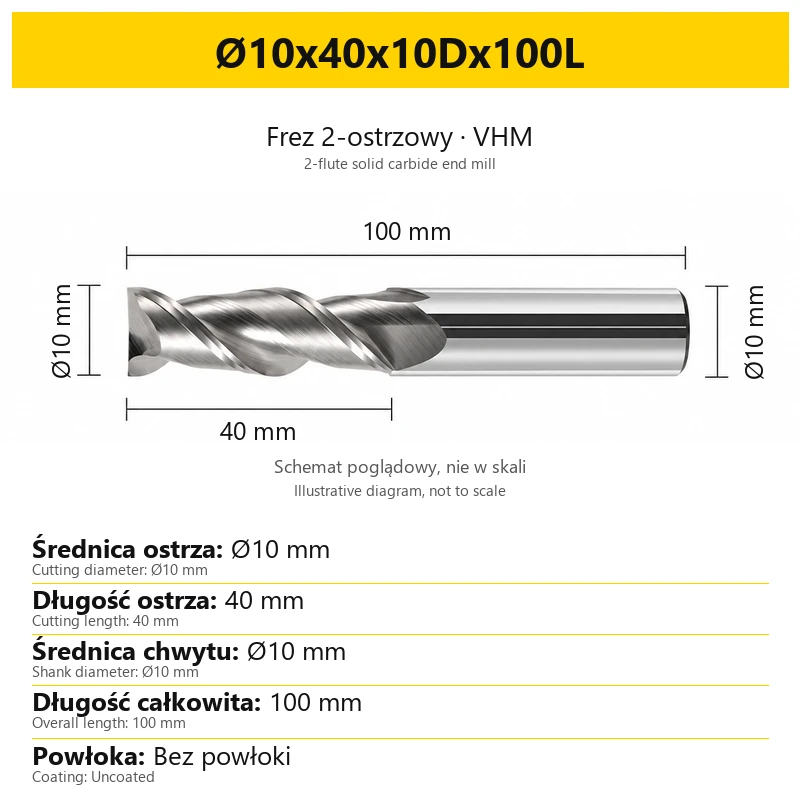
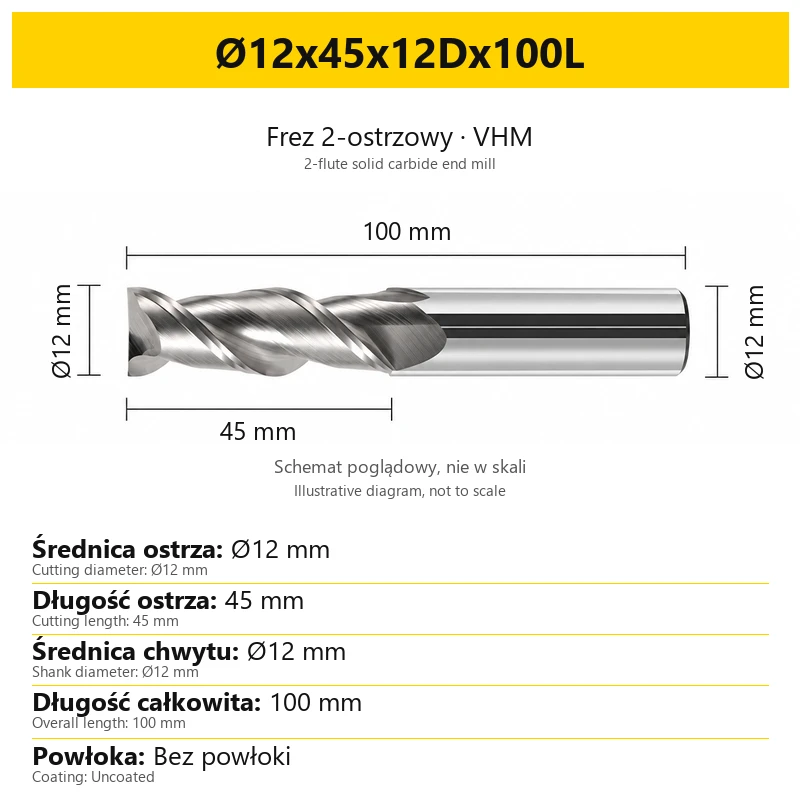
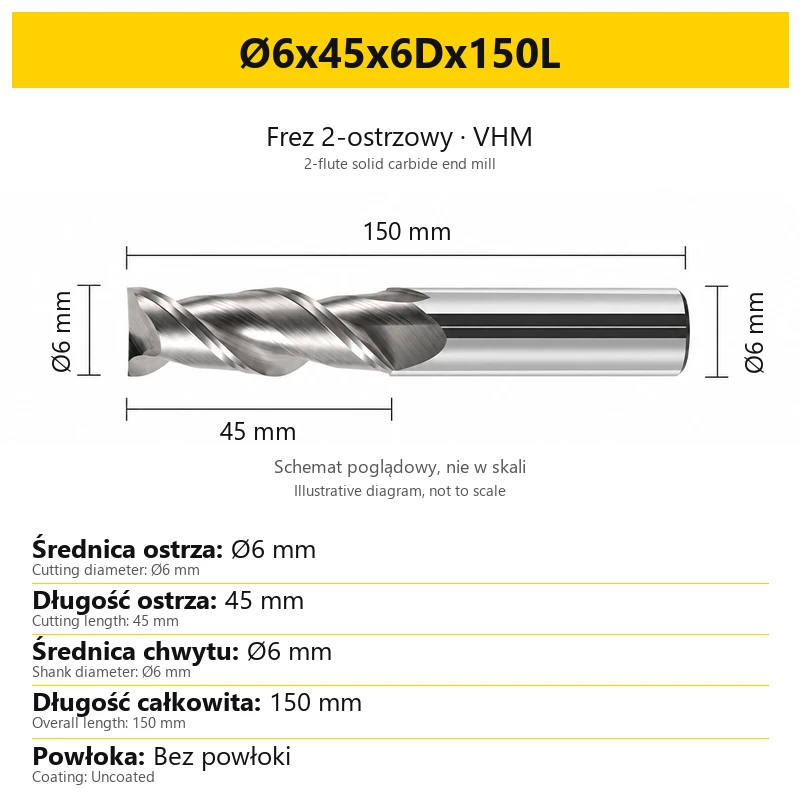


2-Flute Carbide End Mill for Aluminium
Shipping costs are not included in the price.
Shipping costs are not included in the price.
Ask about the product

The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: F6E0-701F2
Product description
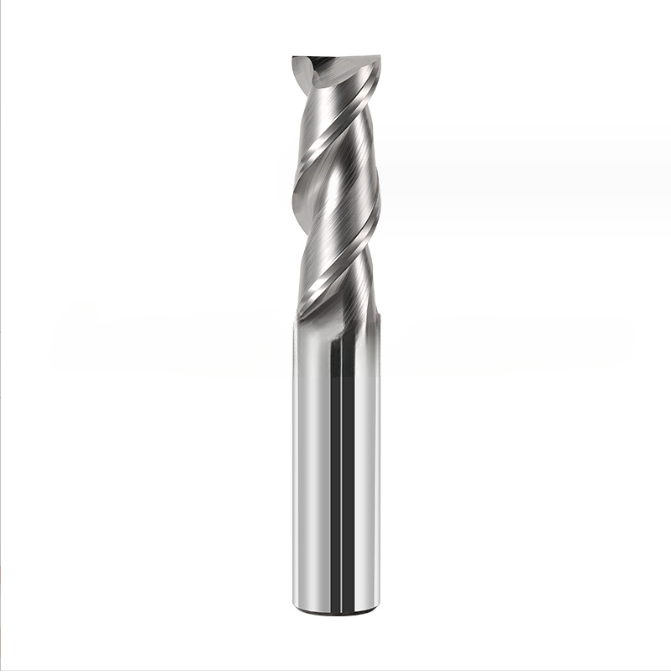
2-flute solid carbide end mill for aluminium
For aluminium and its alloys · Ø1–20 mm cutting diameters · 50–150 mm overall lengths
A monolithic solid carbide (VHM) end mill with two flutes, without coating, designed for milling aluminium and its alloys. The range includes small diameters for fine features as well as larger and extended variants for walls, slots and pockets.
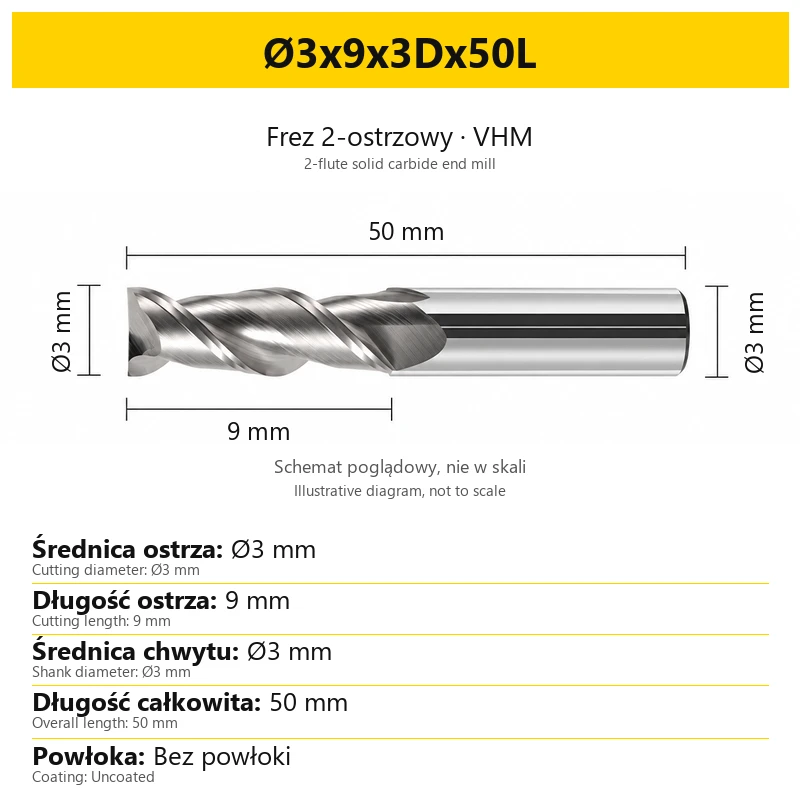
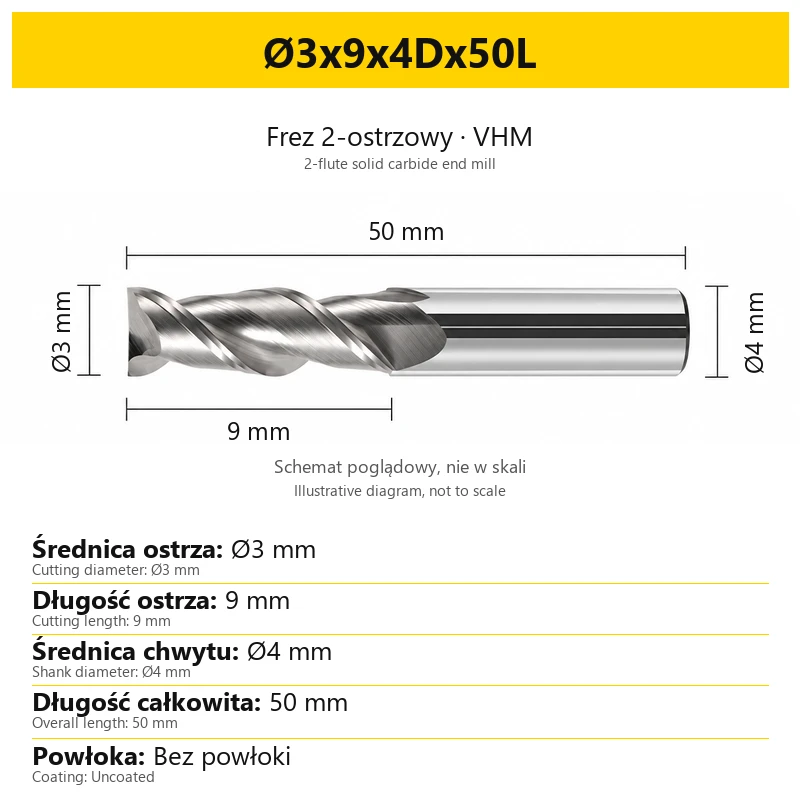
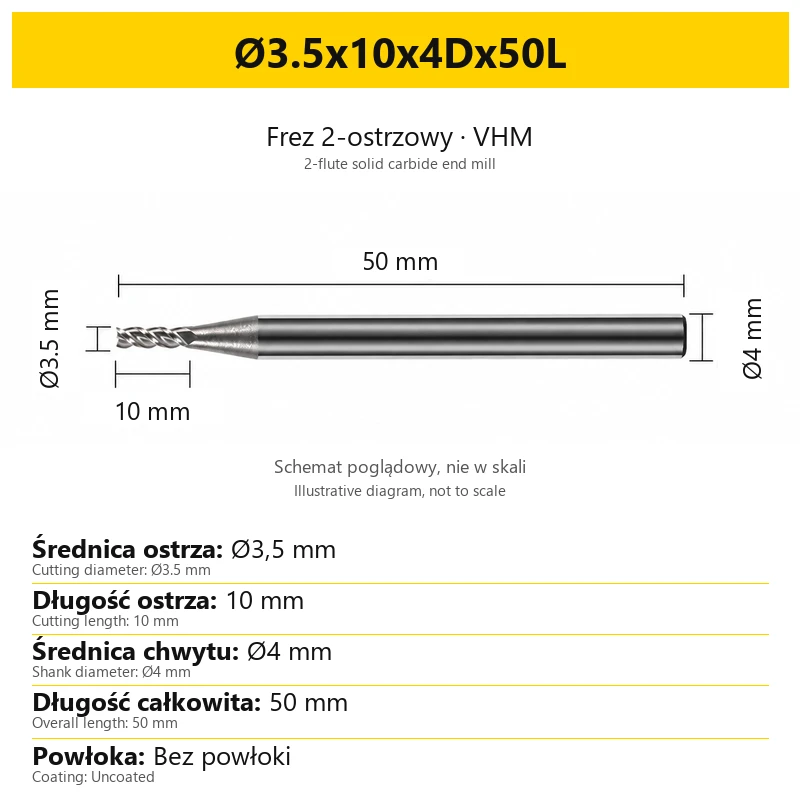
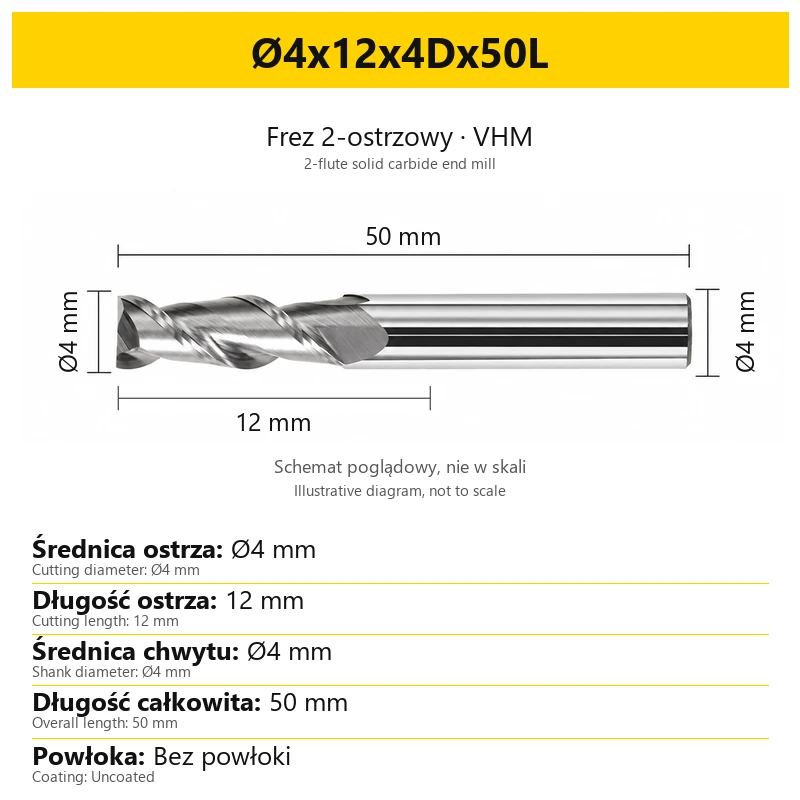
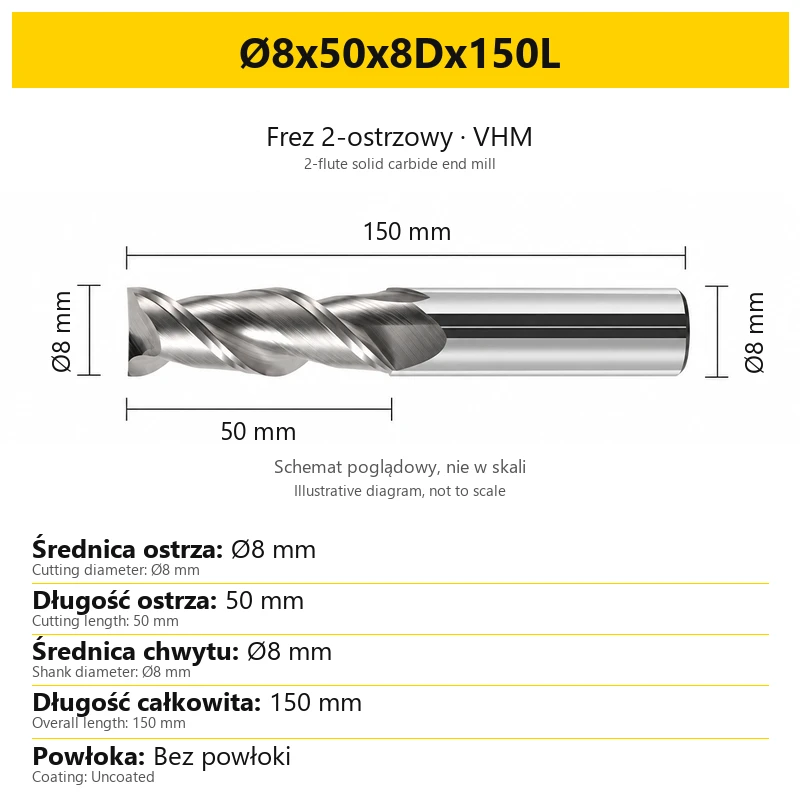
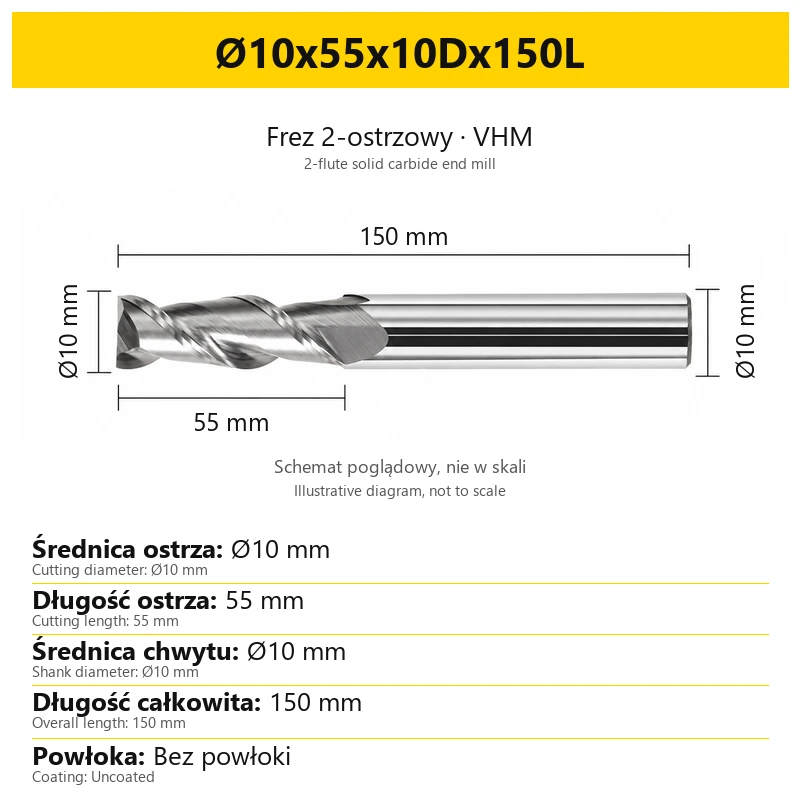
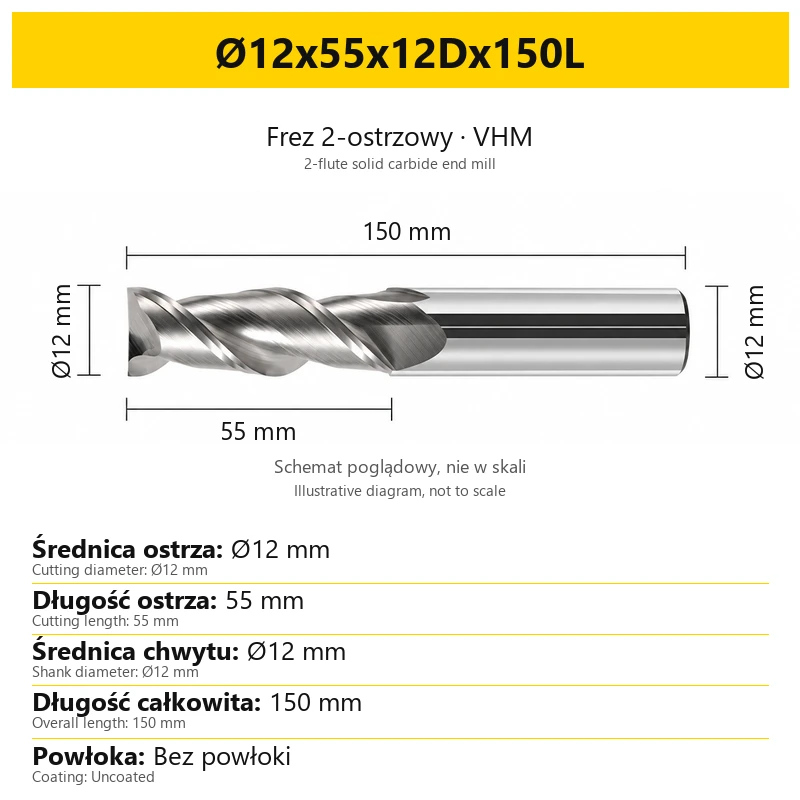
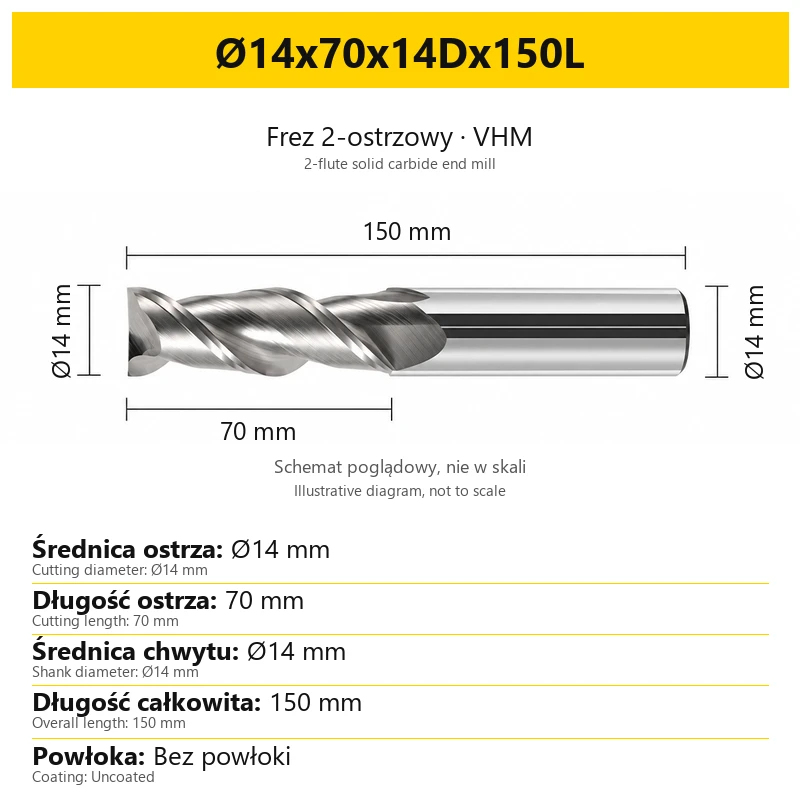
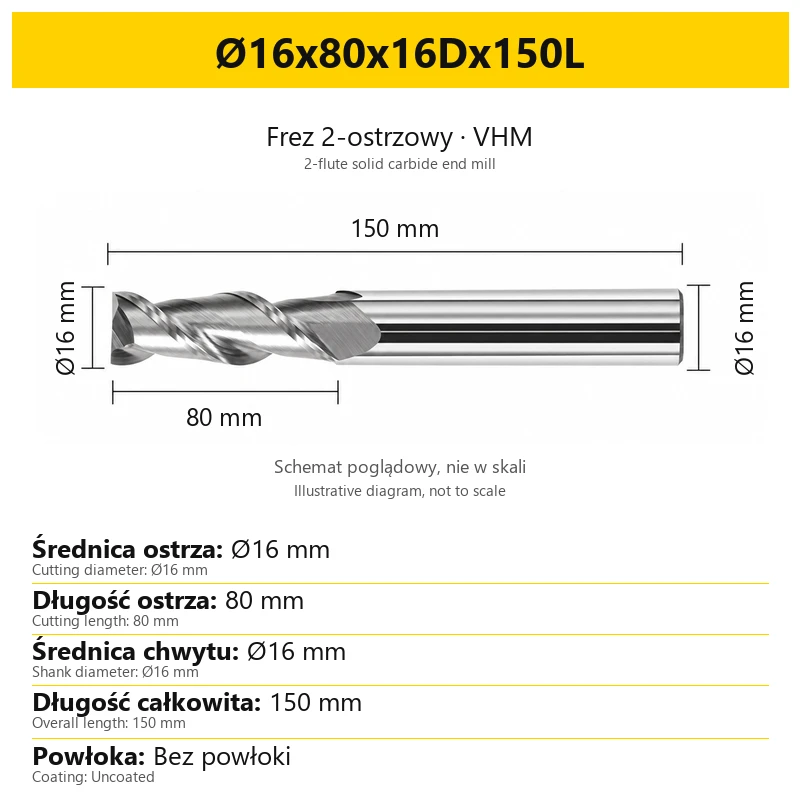
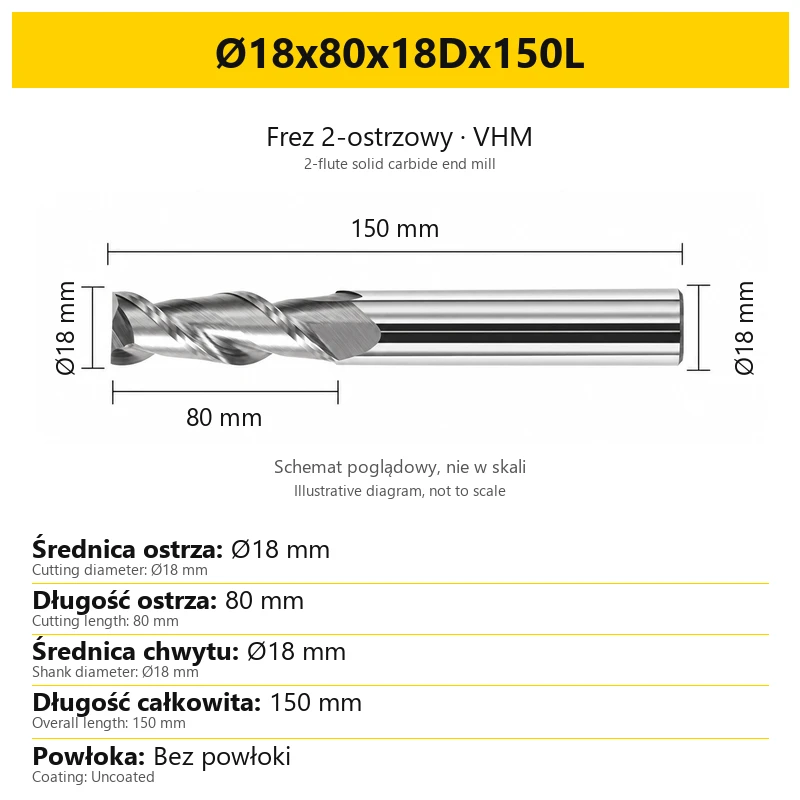
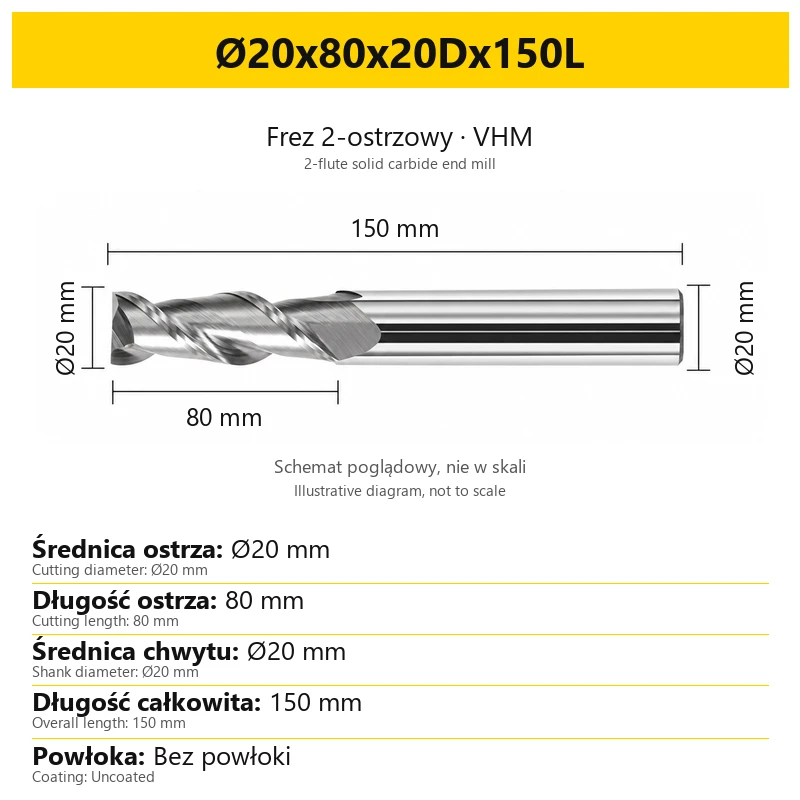
Select the variant by four dimensions: cutting diameter, cutting length, shank diameter and overall length. Check the complete designation: the same cutting diameter may be offered with a different shank or cutting length.
1. Materials and applications
| Material / task | Selection guidance |
|---|---|
| Aluminium and aluminium alloys | Set cutting conditions for the specific alloy, its condition and the operation. Provide effective chip evacuation and appropriate coolant or lubrication. |
| Fine workpiece features | Small diameters allow narrow slots and small internal corners. Consider tool runout and the spindle speed range. |
| Recessed surfaces | An extended variant can improve access. Check cutting length, tool overhang and clearance for the shank and holder. |
Applications include non-ferrous metals: aluminium and its alloys, copper and its alloys, including brass and bronze, as well as tin and zinc. Select cutting conditions separately for the material grade. One setting does not suit every listed metal.
2. Tool construction and specifications
| Parameter | Value |
|---|---|
| Tool type | Monolithic end mill |
| Tool material | VHM — solid carbide |
| Coating | Uncoated |
| Number of flutes | 2 — designated 2T / Z2 |
| Cutting diameter | Ø1–20 mm, depending on the variant |
| Cutting length | 3–80 mm, depending on the variant |
| Shank diameter | Ø3–20 mm, depending on the variant |
| Overall length | 50–150 mm, depending on the variant |
| Shank | Cylindrical |
| Helix angle | 35° |
These ranges describe the tool family. Not every diameter is available with every length. The selected variant and its card show the exact dimension combination.
3. Machining operations
| Operation | Selection guidance |
|---|---|
| Side and contour milling | Match the cutting diameter to the part geometry and the cutting length to the wall height. Check shank clearance. |
| Slot milling | Consider slot width, chip evacuation and tool load. Set the depth per pass for the workpiece material and system rigidity. |
| Pocket machining | Plan the entry method and toolpath for the available space. Prevent chip accumulation and recutting. |
| Small flat surfaces | Match stepover and stock allowance to the tool diameter and required surface finish. |
4. How to select a variant
- Select the cutting diameter. Consider slot width, internal corner radii and the available space.
- Check the cutting length. Choose the shortest cutting section that can complete the operation.
- Select the overall tool length. Use an extended tool when access requires it. Additional overhang reduces rigidity and may require a lower cutting load.
- Match the holder to the shank. The shank diameter is not always equal to the cutting diameter. Use the value identified by D when selecting a collet or holder.
- Compare the full designation. The variant selector shows current dimension combinations, prices and availability.
5. How to read the dimensions
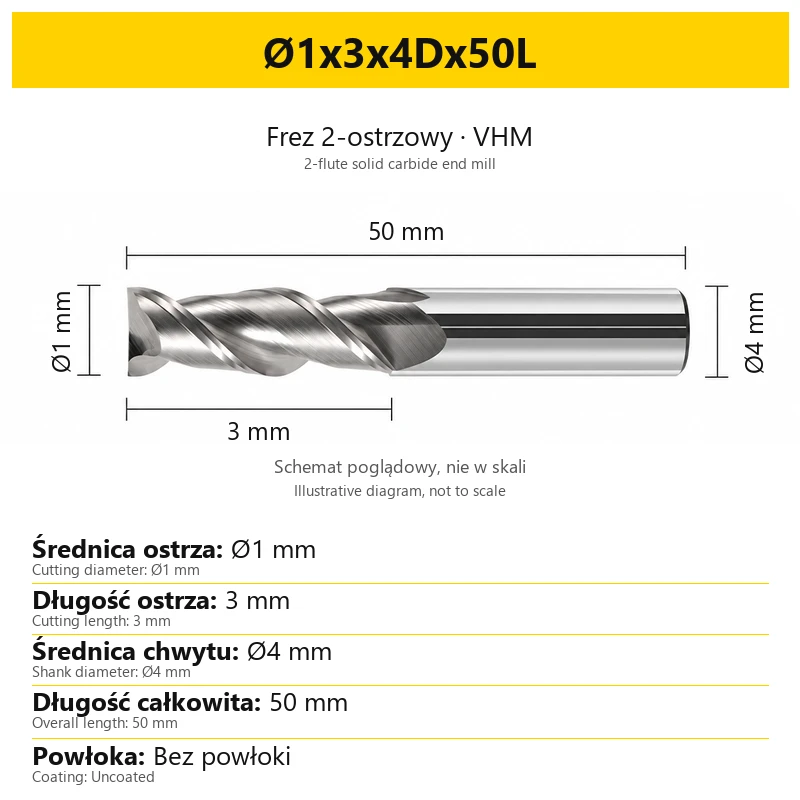
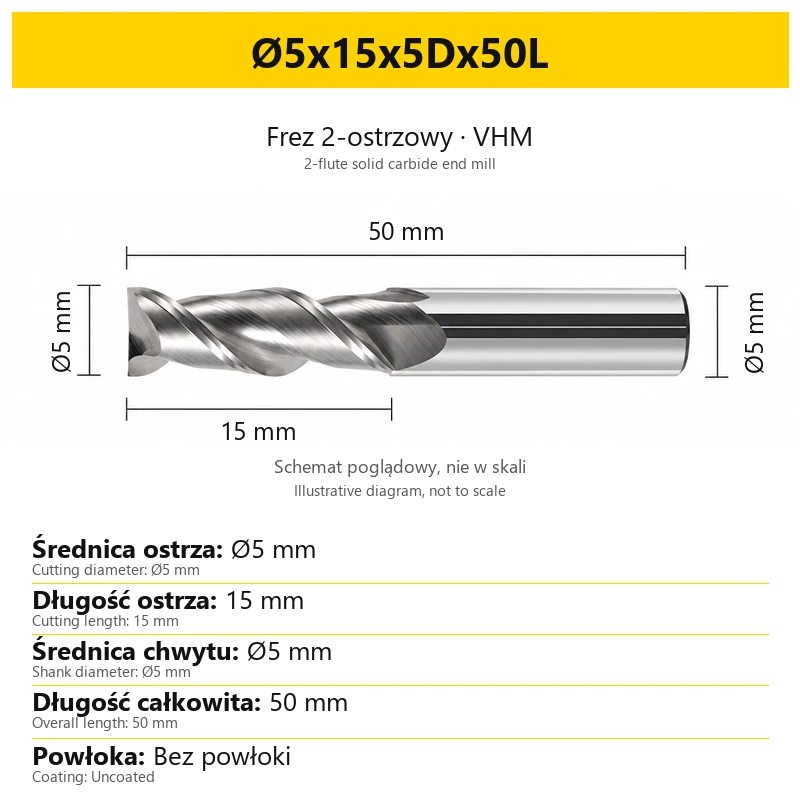
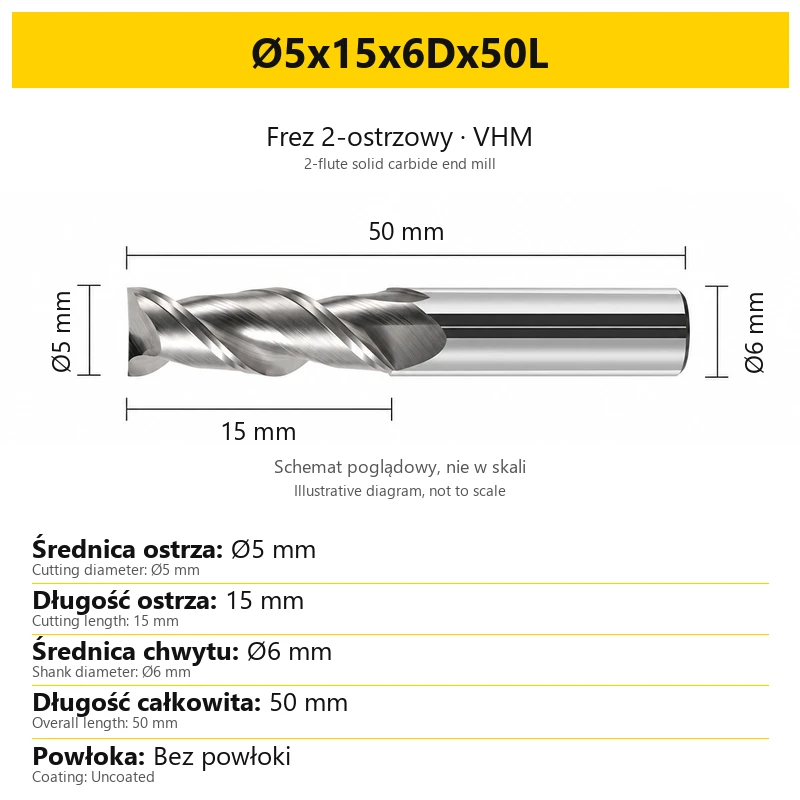
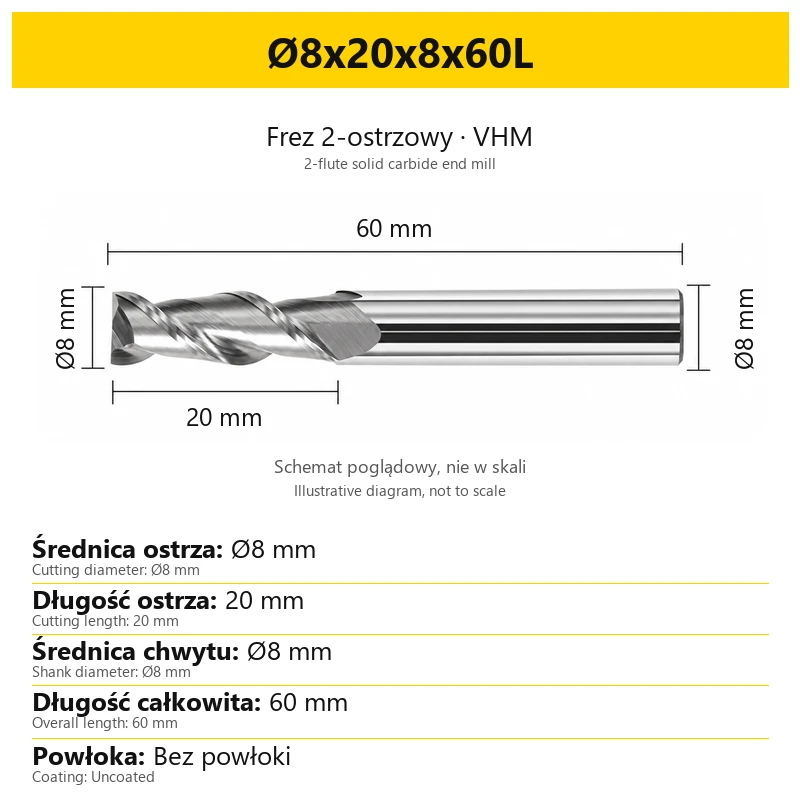
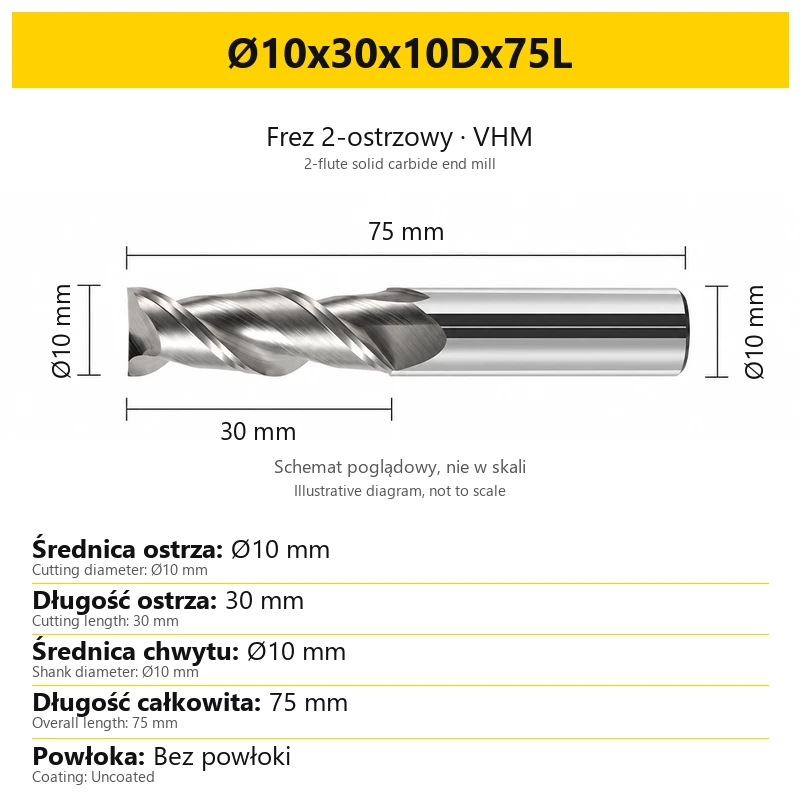
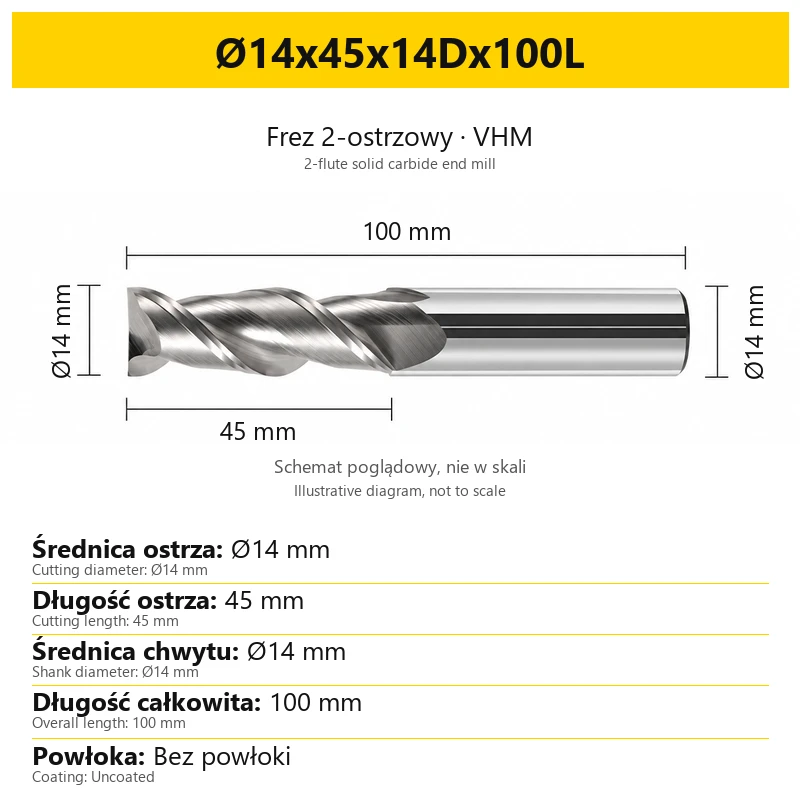
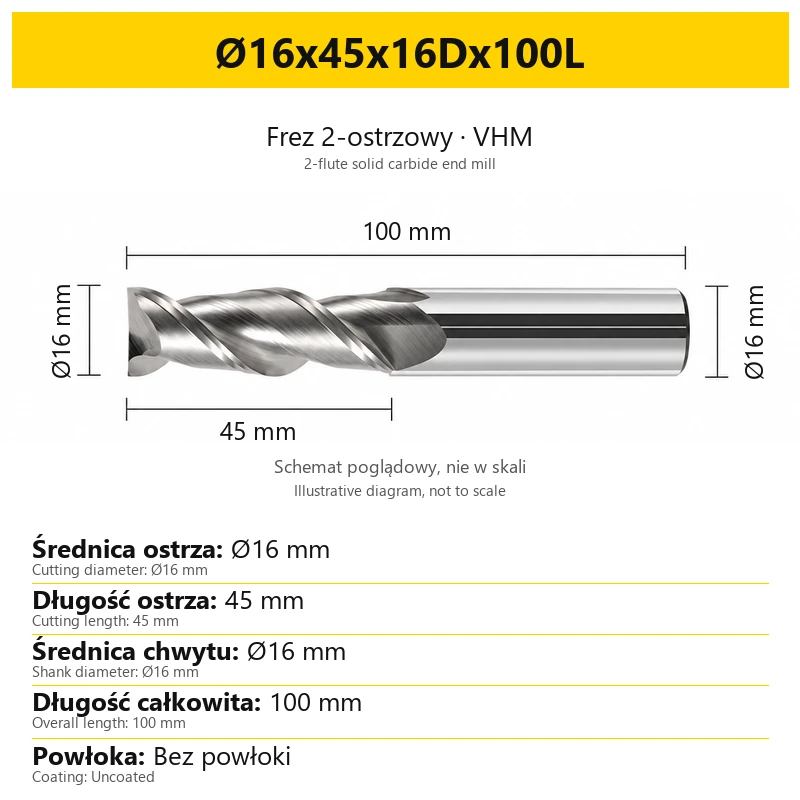
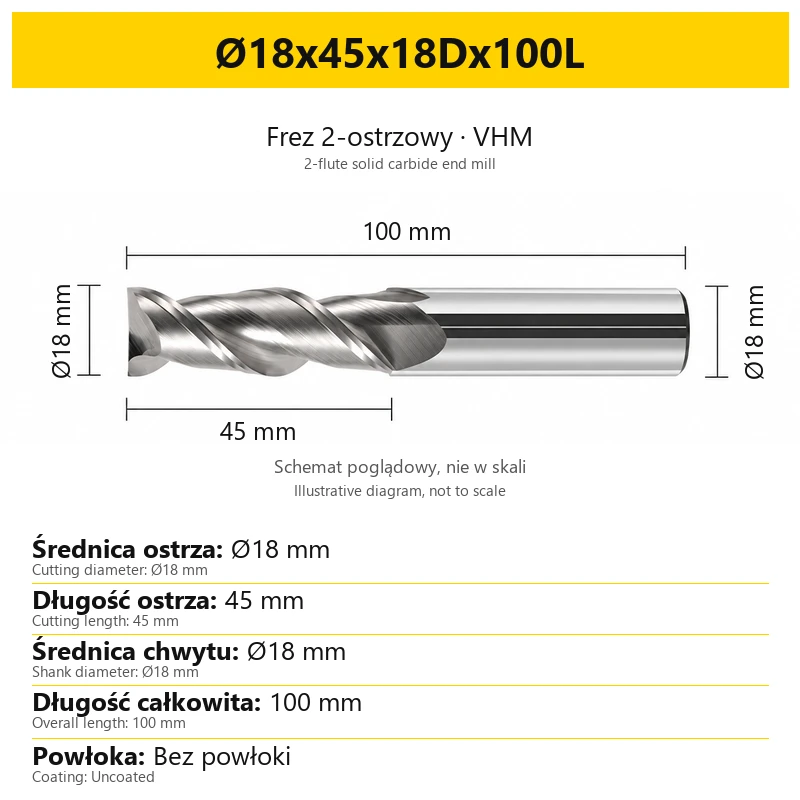
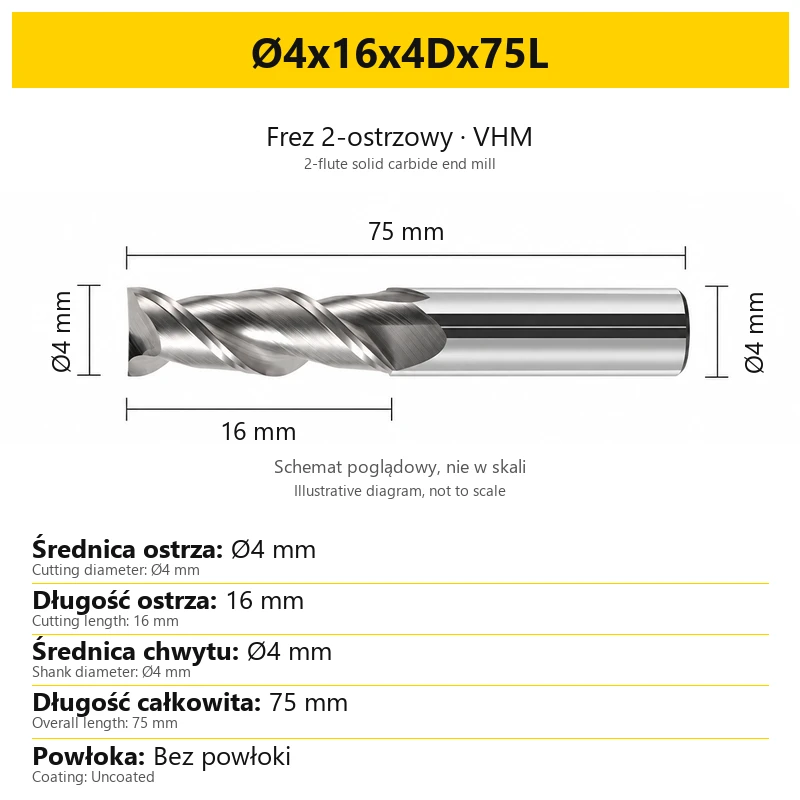
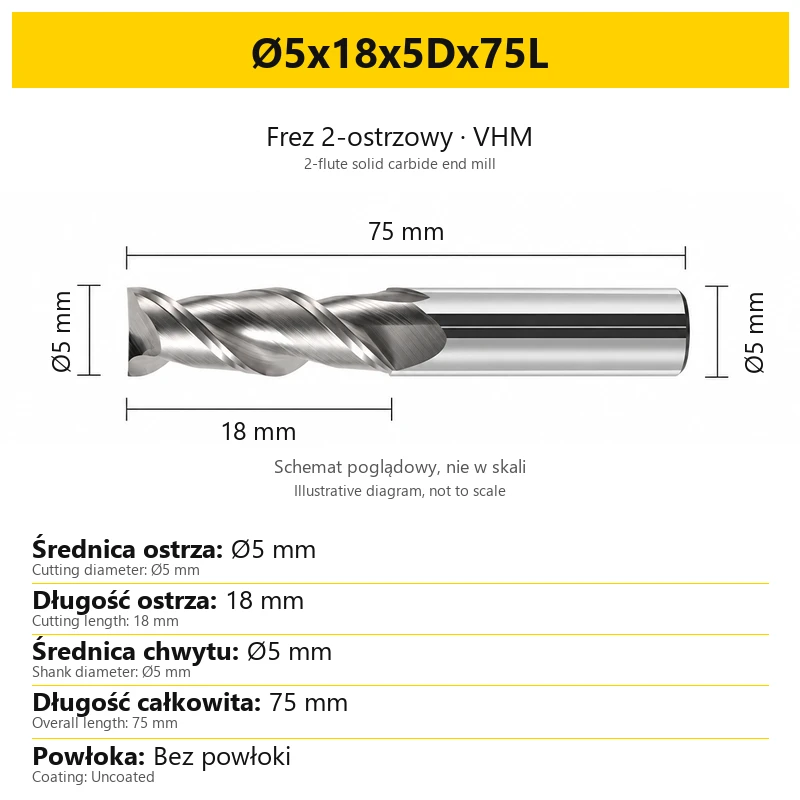
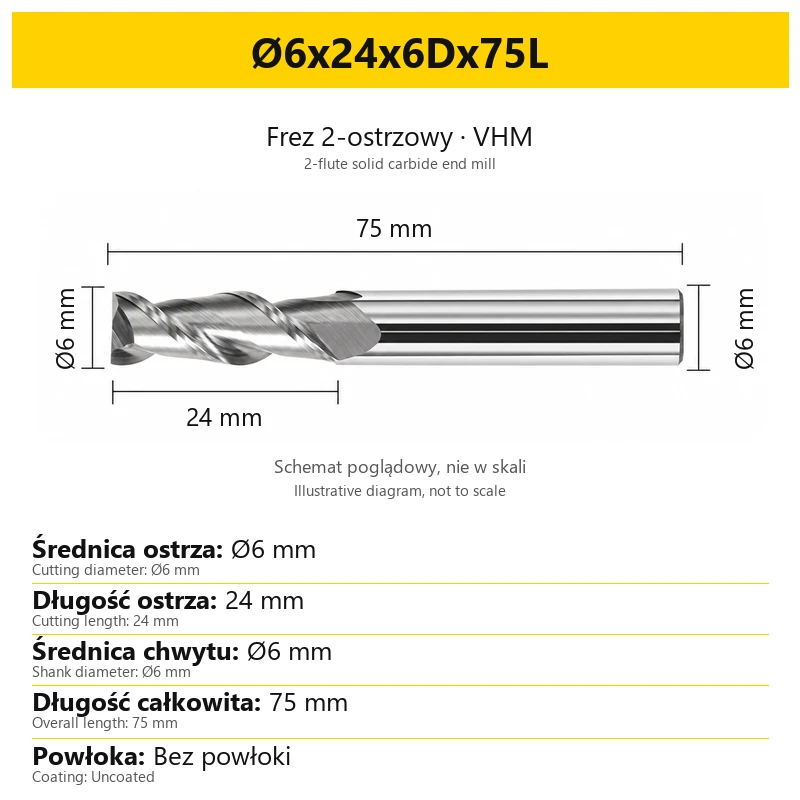
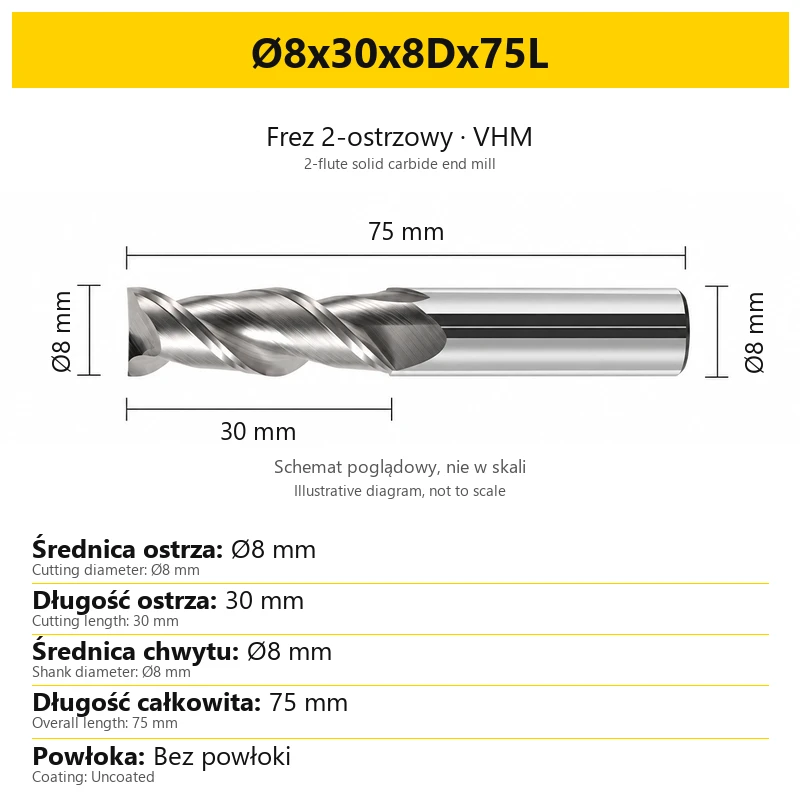
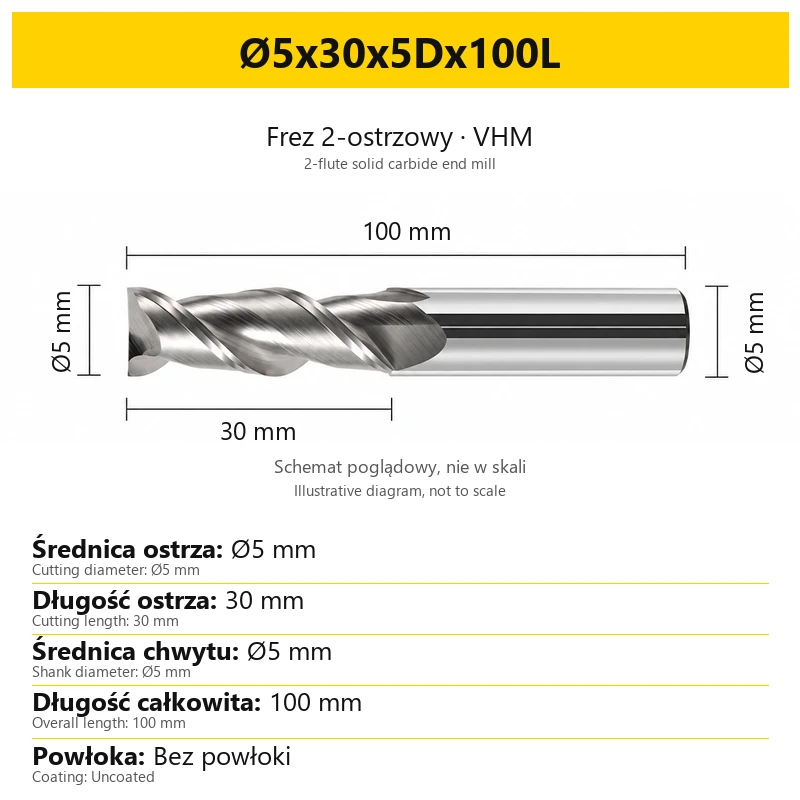
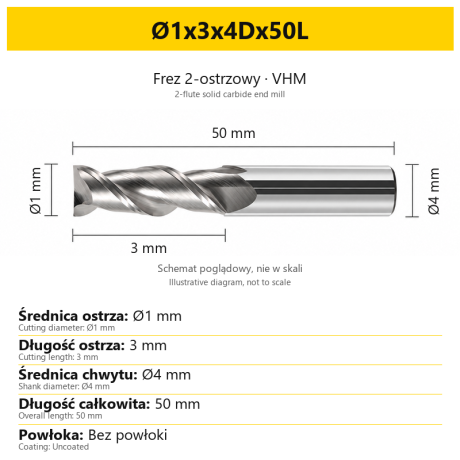
Example: Ø1x3x4Dx50L. All dimensional values are in millimetres.
| Designation element | Meaning | Example value |
|---|---|---|
| Ø1 | Cutting diameter | 1 mm |
| 3 | Cutting length — the second dimension | 3 mm |
| 4D | Shank diameter | 4 mm |
| 50L | Overall length | 50 mm |
2T or Z2 denotes two flutes. It does not specify cutting length or the number of tools in the order.
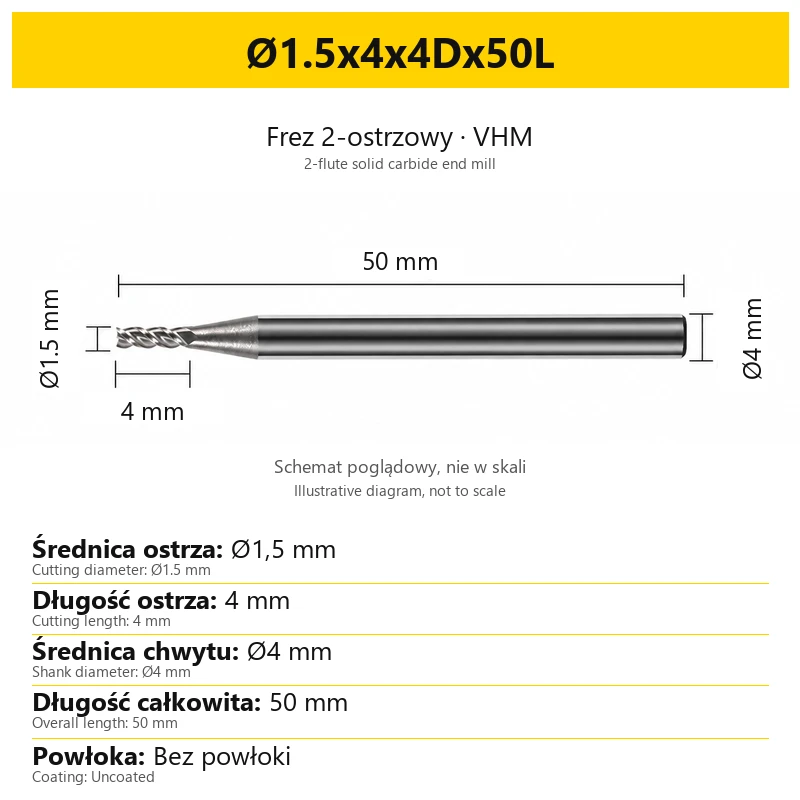
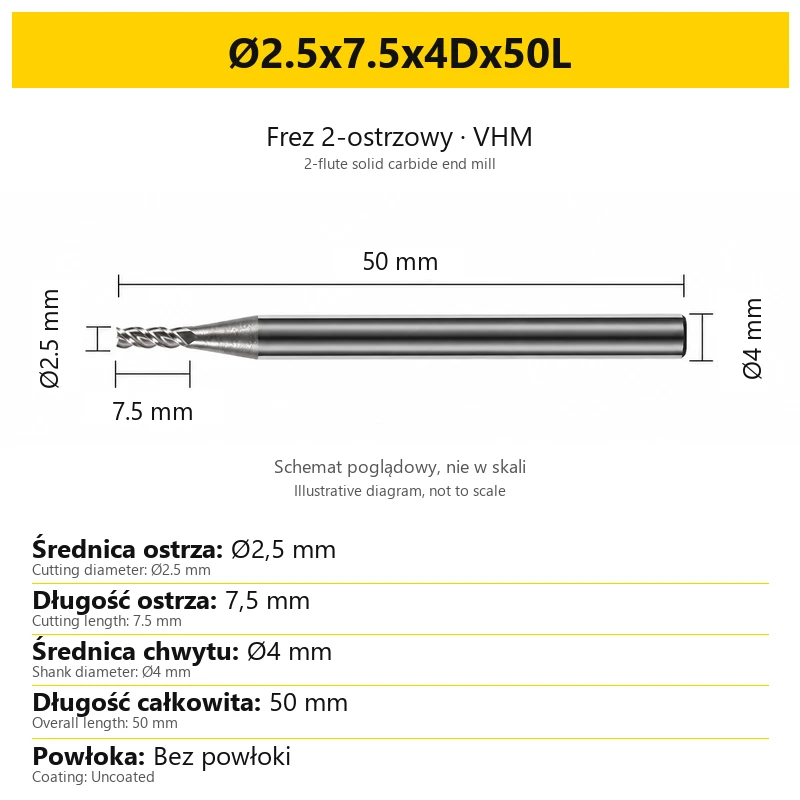
Variant cards show the tool and labelled dimensions. Select the size from the numerical values; the photograph is not a scale drawing.
6. Clamping and cutting conditions
- Keep clamping surfaces clean. Check the holder and shank condition, and seat the tool according to the holder requirements.
- Minimise runout and overhang. This is particularly important for small diameters and extended variants. Use only the projection needed for the operation.
- Provide effective chip evacuation. Match coolant or lubrication to the aluminium alloy and machine. Check for chip accumulation in pockets and slots.
- Select parameters for the complete setup. Consider the alloy, cutting diameter, two flutes, cutting length, overhang, operation and workholding rigidity.
- Respond to vibration and poor surface finish. Stop machining and check cutting edges, clamping, chip evacuation and tool load.
For spindle speed and feed selection, provide the full tool size, material grade, operation, axial and radial engagement and tool overhang. Spindle speed, feed, axial depth and radial engagement must suit the specific size and operation. Appropriate coolant or lubrication is recommended, particularly when machining aluminium.
7. What you receive
| Item | Order contents |
|---|---|
| Unit of sale | 1 uncoated 2-flute solid carbide end mill for aluminium |
| Size | The variant selected in the product selector |
The quantity field sets the number of tools of the selected size. Images showing several tools illustrate the product family and do not indicate a set.
8. Frequently asked questions
Is the shank diameter the same as the cutting diameter?
Not for every variant. For example, the variant with a 1 mm cutting diameter has a Ø4 mm shank. Select the holder by the shank diameter.
Does a 150 mm tool allow milling to a depth of 150 mm?
No. This is the overall tool length. Separately check cutting length, projection after clamping and clearance for the shank and holder.
Is a longer end mill better for every operation?
Choose the shortest variant that provides the required access and cutting length. Excessive overhang increases deflection and vibration risk.
Can cutting parameters be transferred from a short tool to an extended one?
Not automatically. Changing cutting length or overhang changes the rigidity of the setup. Verify parameters for the specific tool and clamping arrangement.
Related products
-
1670-1921ABestseller
4-Flute TiSiN Coated Carbide Corner Radius End Mill, up to 55HRC
-
19B7-502CDBestseller
 4-Flute End Mills 0.00
4-Flute Carbide End Mill VHM TiSiN Coated Roughing
-
F677-248B8Bestseller
 3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
-
EA4F-928BFBestseller
6-Flute End Mill VHM up to 60HRC - AITiN - for Steel & Stainless Steel


Bestsellers
-
Bestseller
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.86Price €56.79without VAT -
Bestseller
Kortools Adhesive + Tape CNC Workholding Kit
Yellow tape 5cm x 50m; adhesive 100g Yellow tape 5cm x 50m; adhesive 500g Yellow tape 10cm x 50m; adhesive 100g Yellow tape 10cm x 50m; adhesive 500g Green tape 5cm x 50m; adhesive 100g + 7 morePrice €44.66Price €36.31without VAT -
Price €17.18Price €13.97without VAT
-
Price €7.10Price €5.77without VAT
-
Price €7.56Price €6.14without VAT
-
Bestseller
 Other Accessories 0.00
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.82Price €43.76without VAT -
Bestseller
 Ball Nose End Mills 0.00
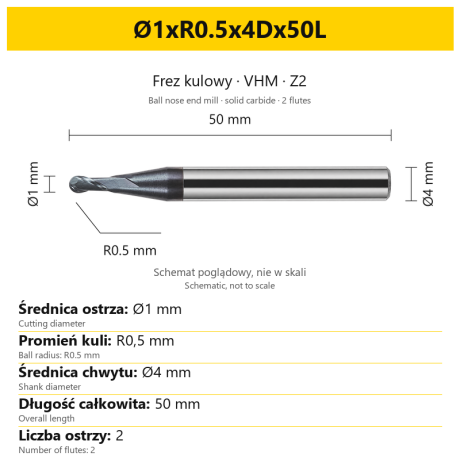
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.14Price €8.25without VAT -
Bestseller
 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.35Price €4.35without VAT -
Bestseller
 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.40Price €3.58without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.89Price €6.41without VAT -
Bestseller
 2-Flute End Mills 0.00
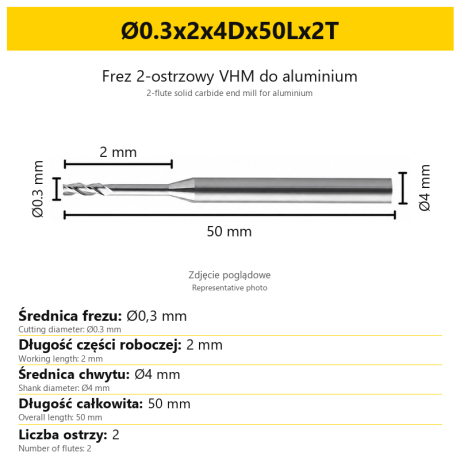
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.99Price €6.50without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.28Price €5.92without VAT -
Bestseller
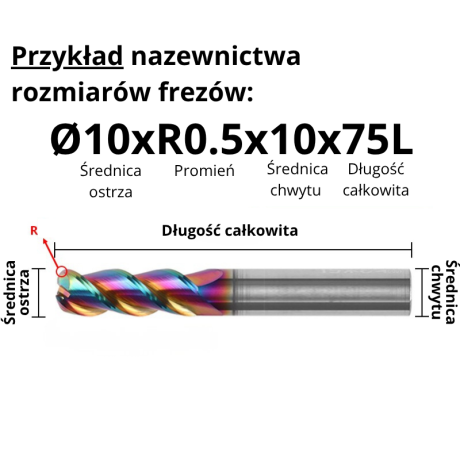
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €4.96Price €4.04without VAT -
Bestseller
3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.10Price €4.15without VAT -
Bestseller

 Countersinks 0.00
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.81Price €3.91without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.07Price €4.12without VAT


