









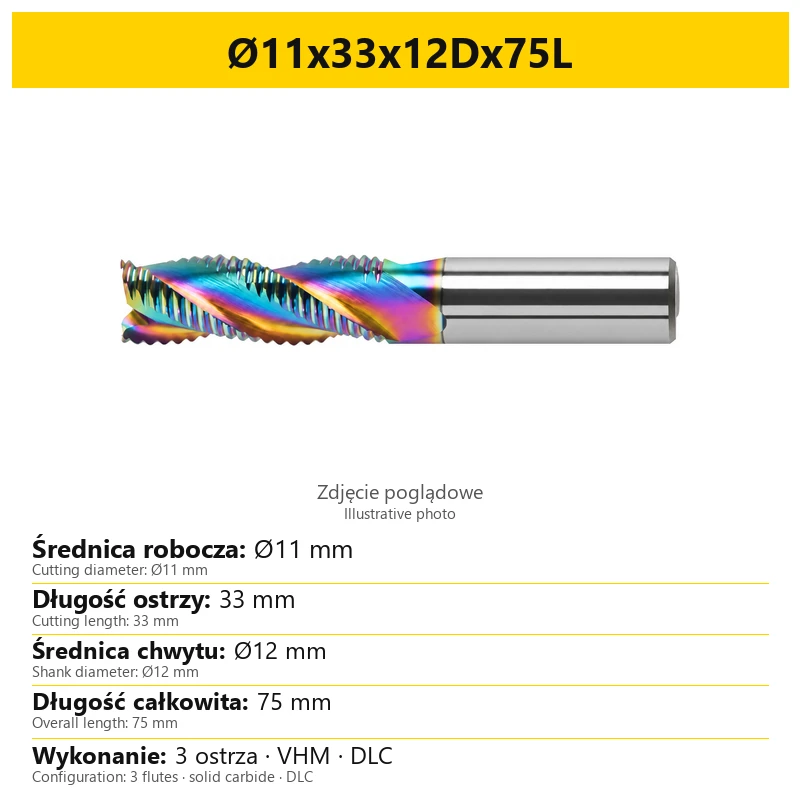
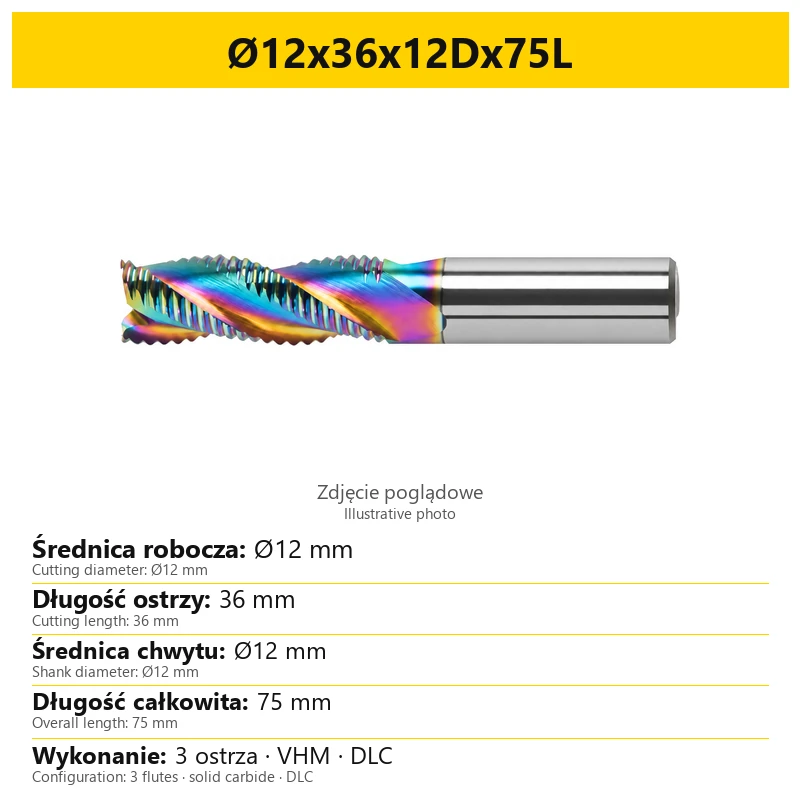
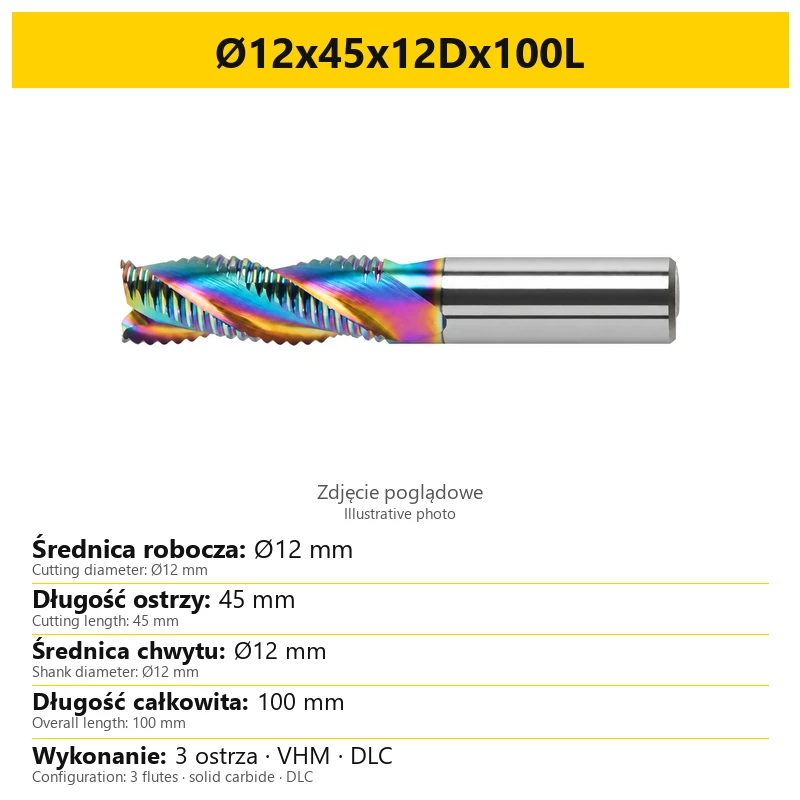


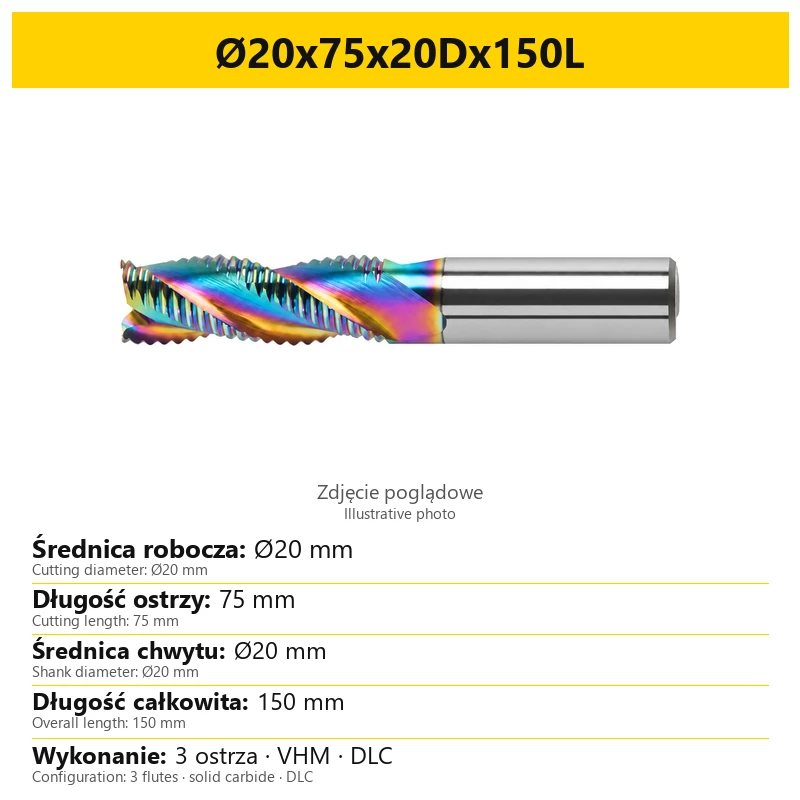


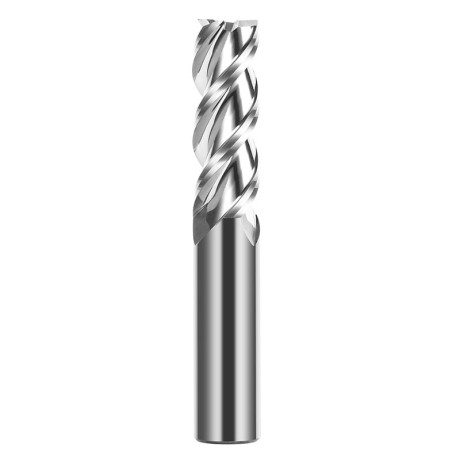
3 Flute Carbide Bit Milling Cutter with DLC Coating for Roughing
Shipping costs are not included in the price.
Shipping costs are not included in the price.
Ask about the product

The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: 9416-58270
Product description
Rough machining of aluminium, non-ferrous metals and plastics
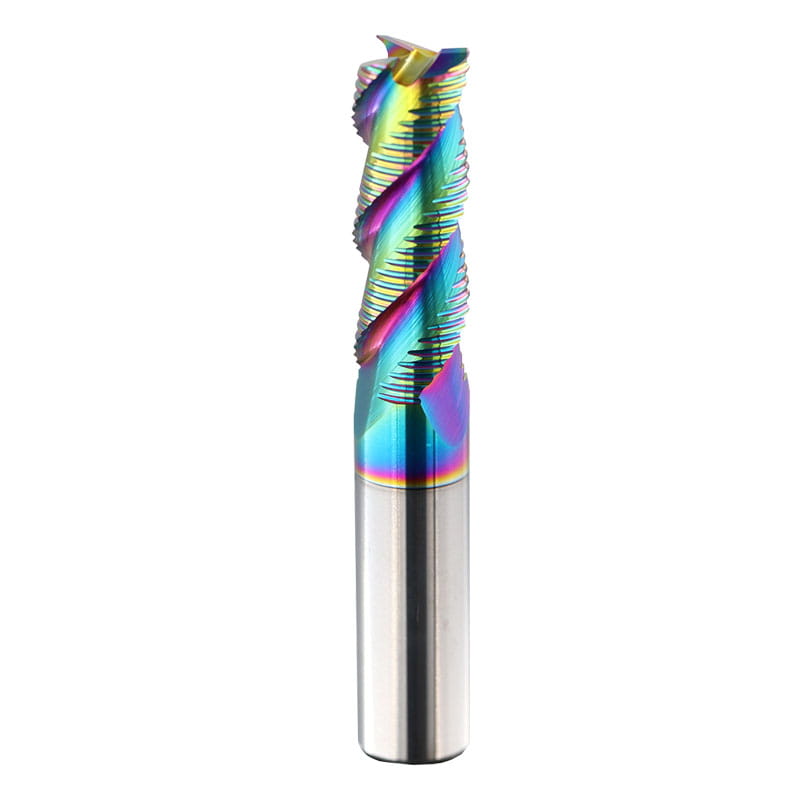
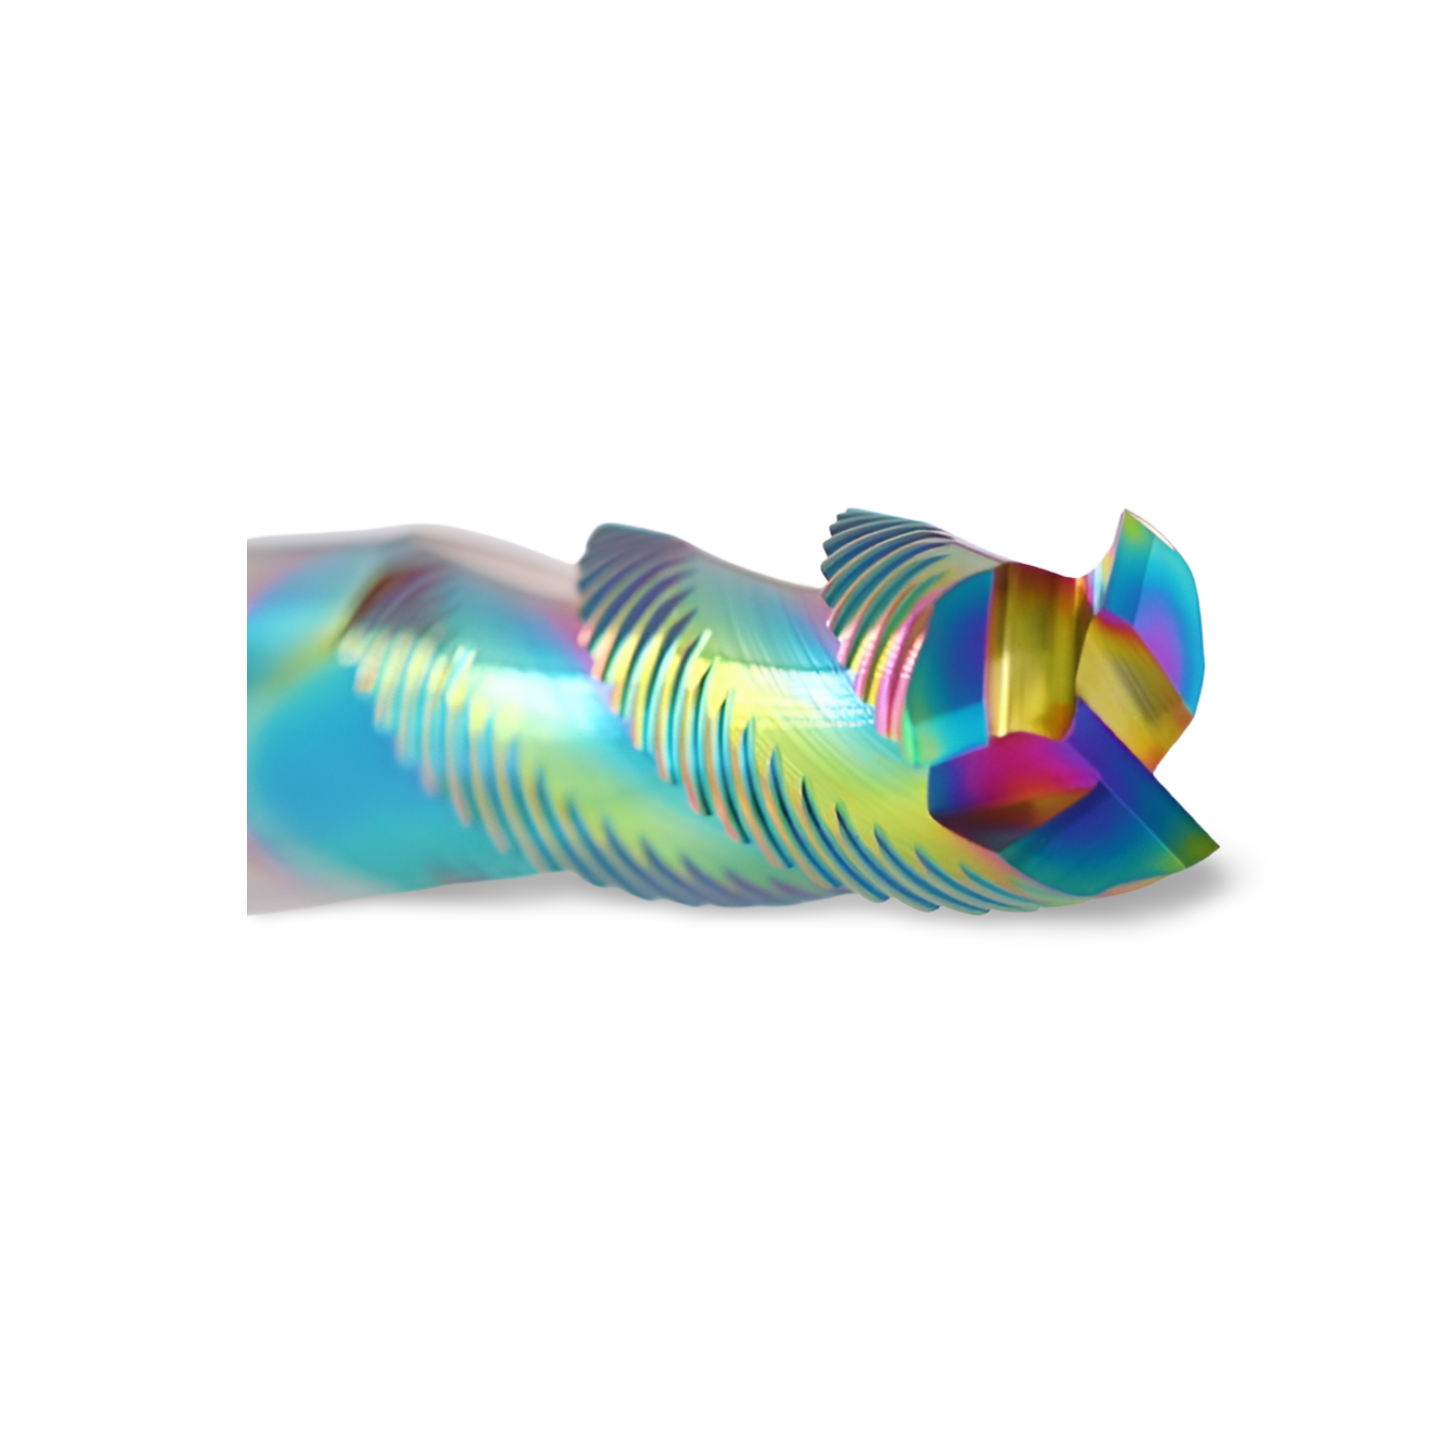
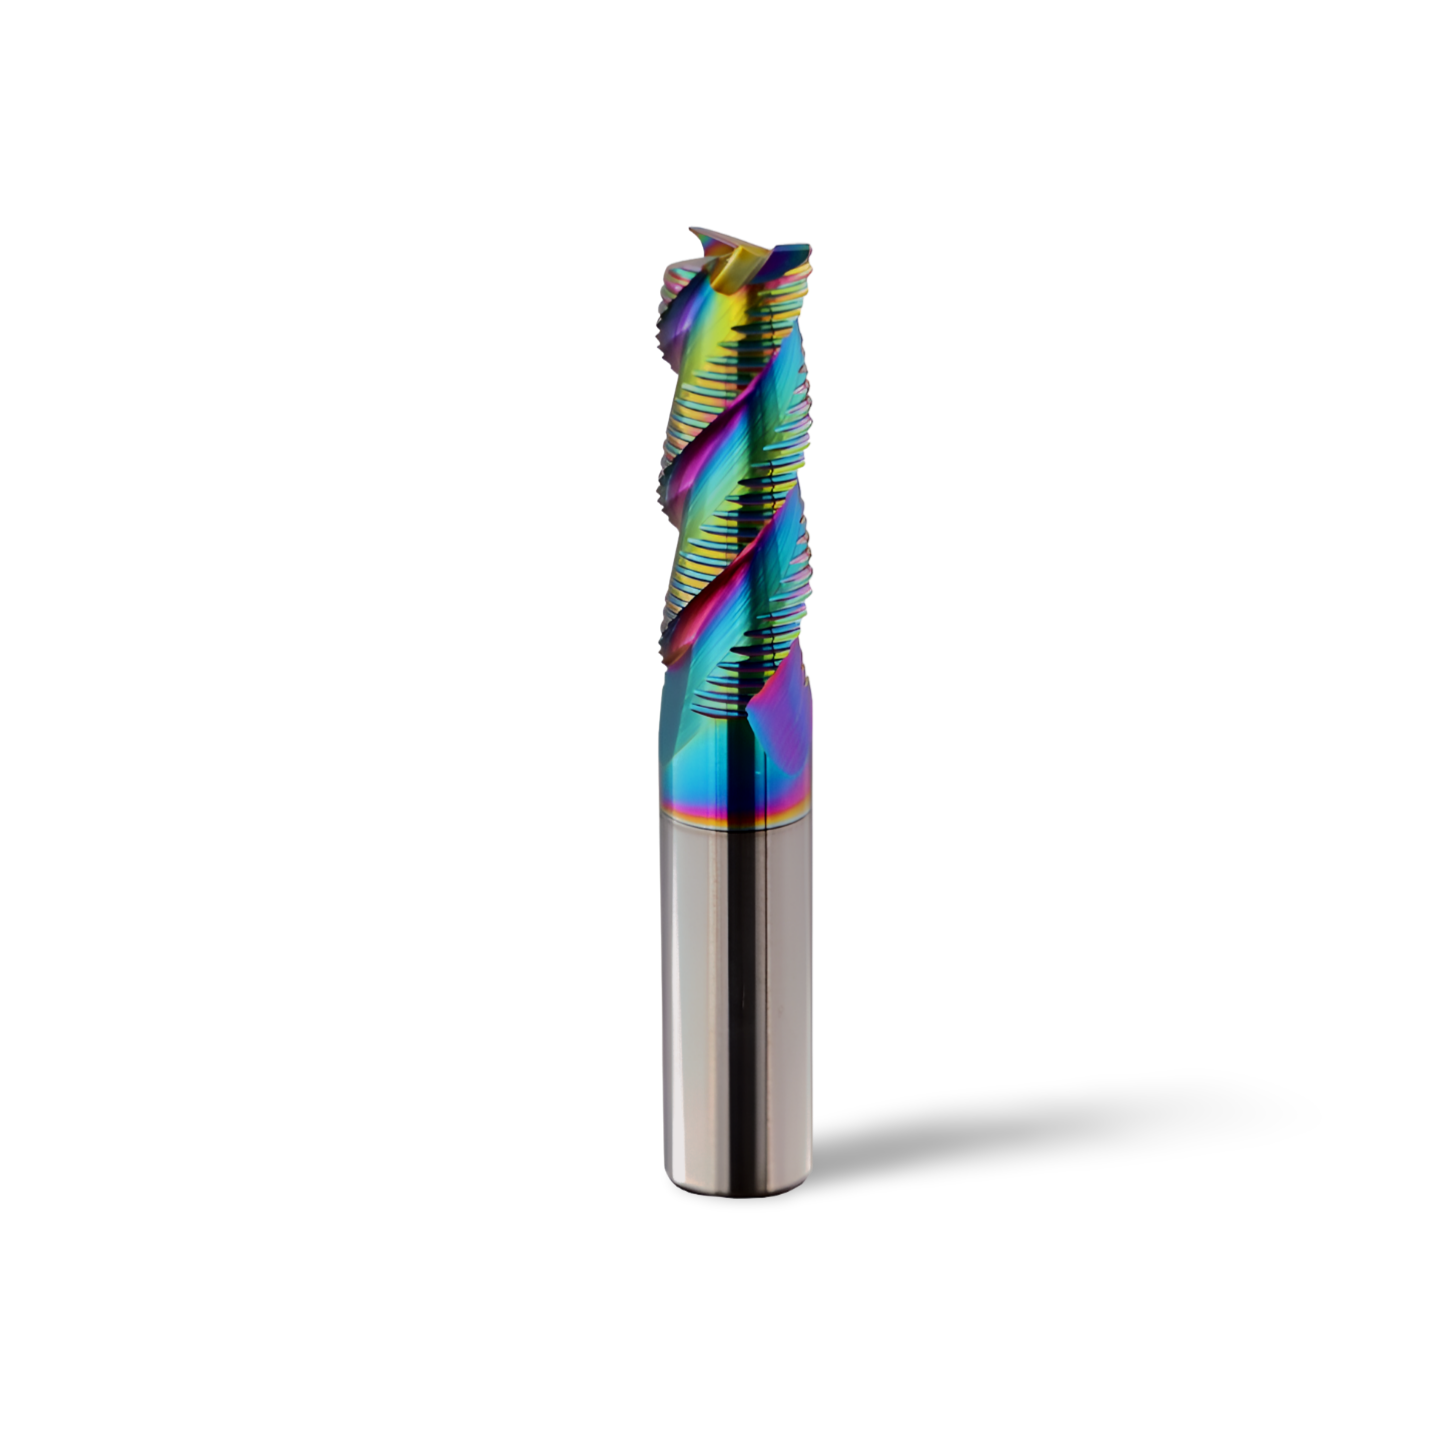
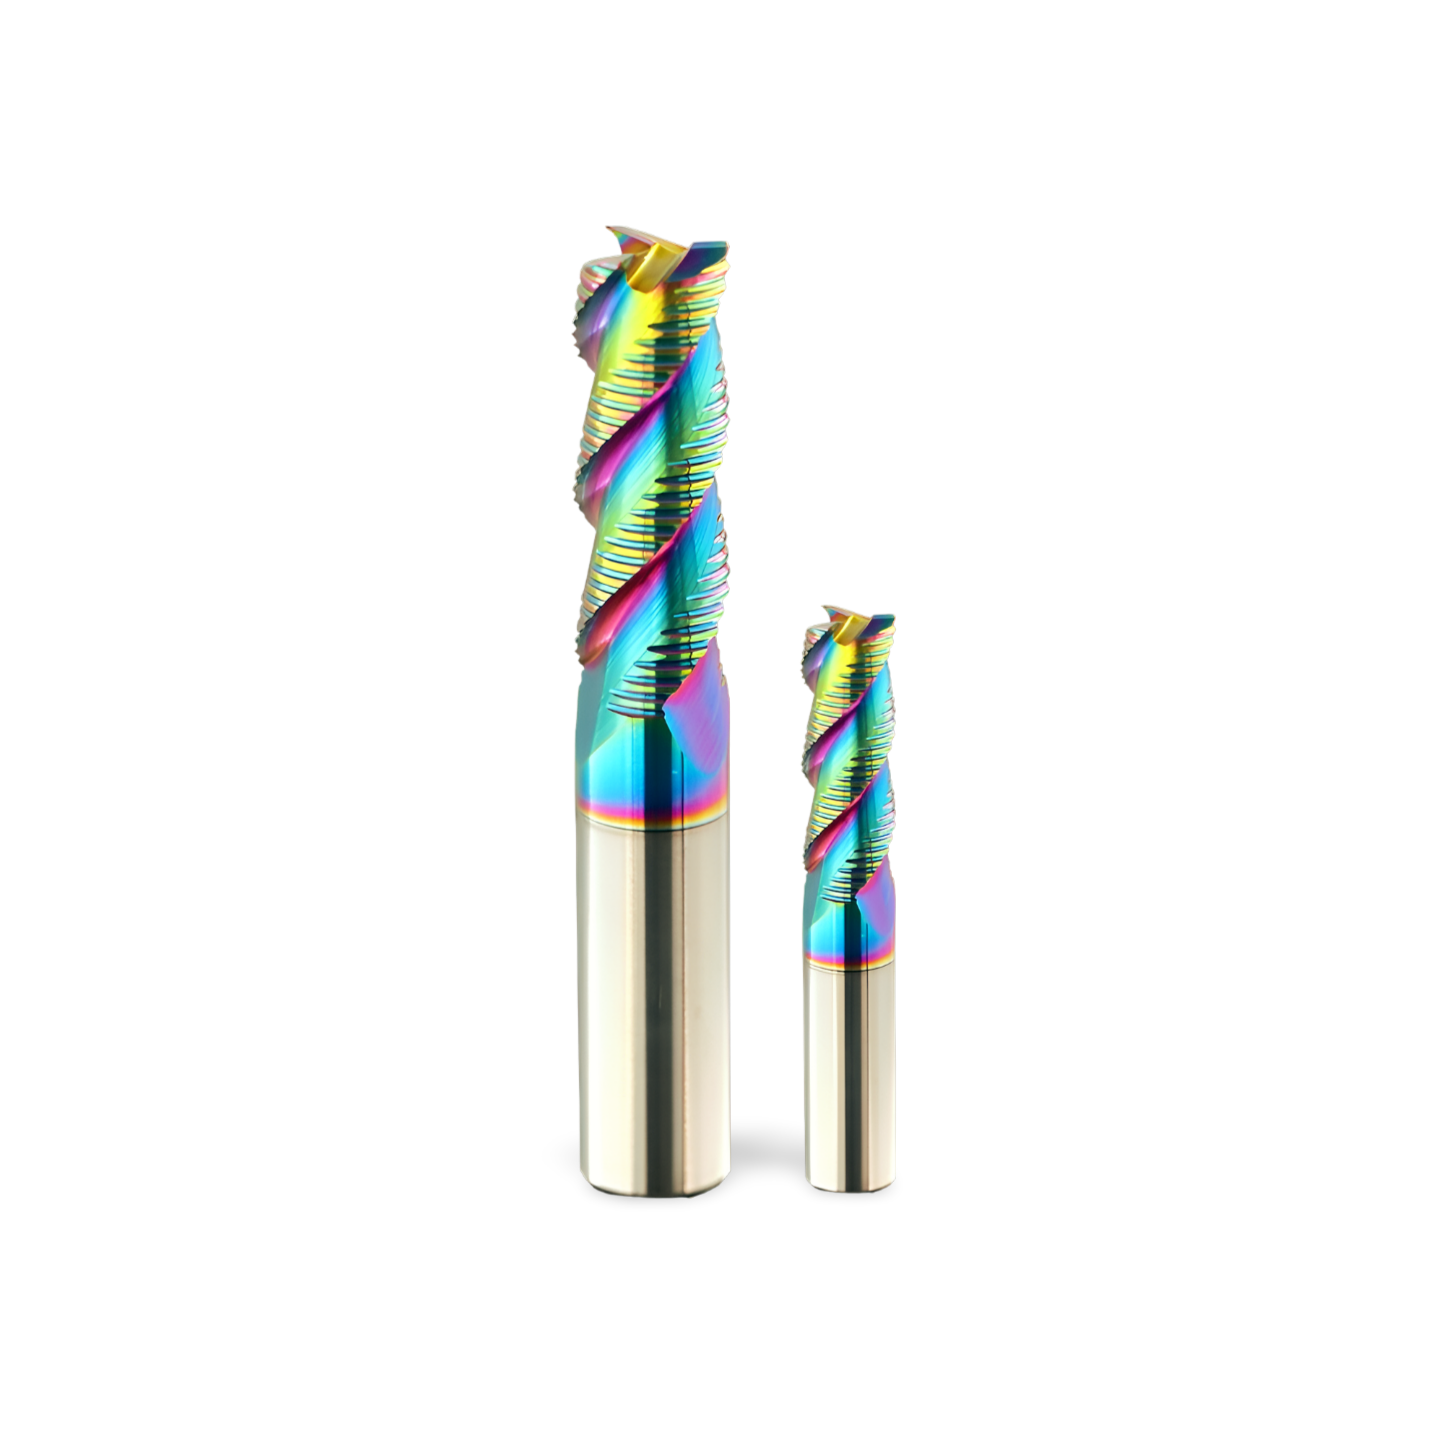
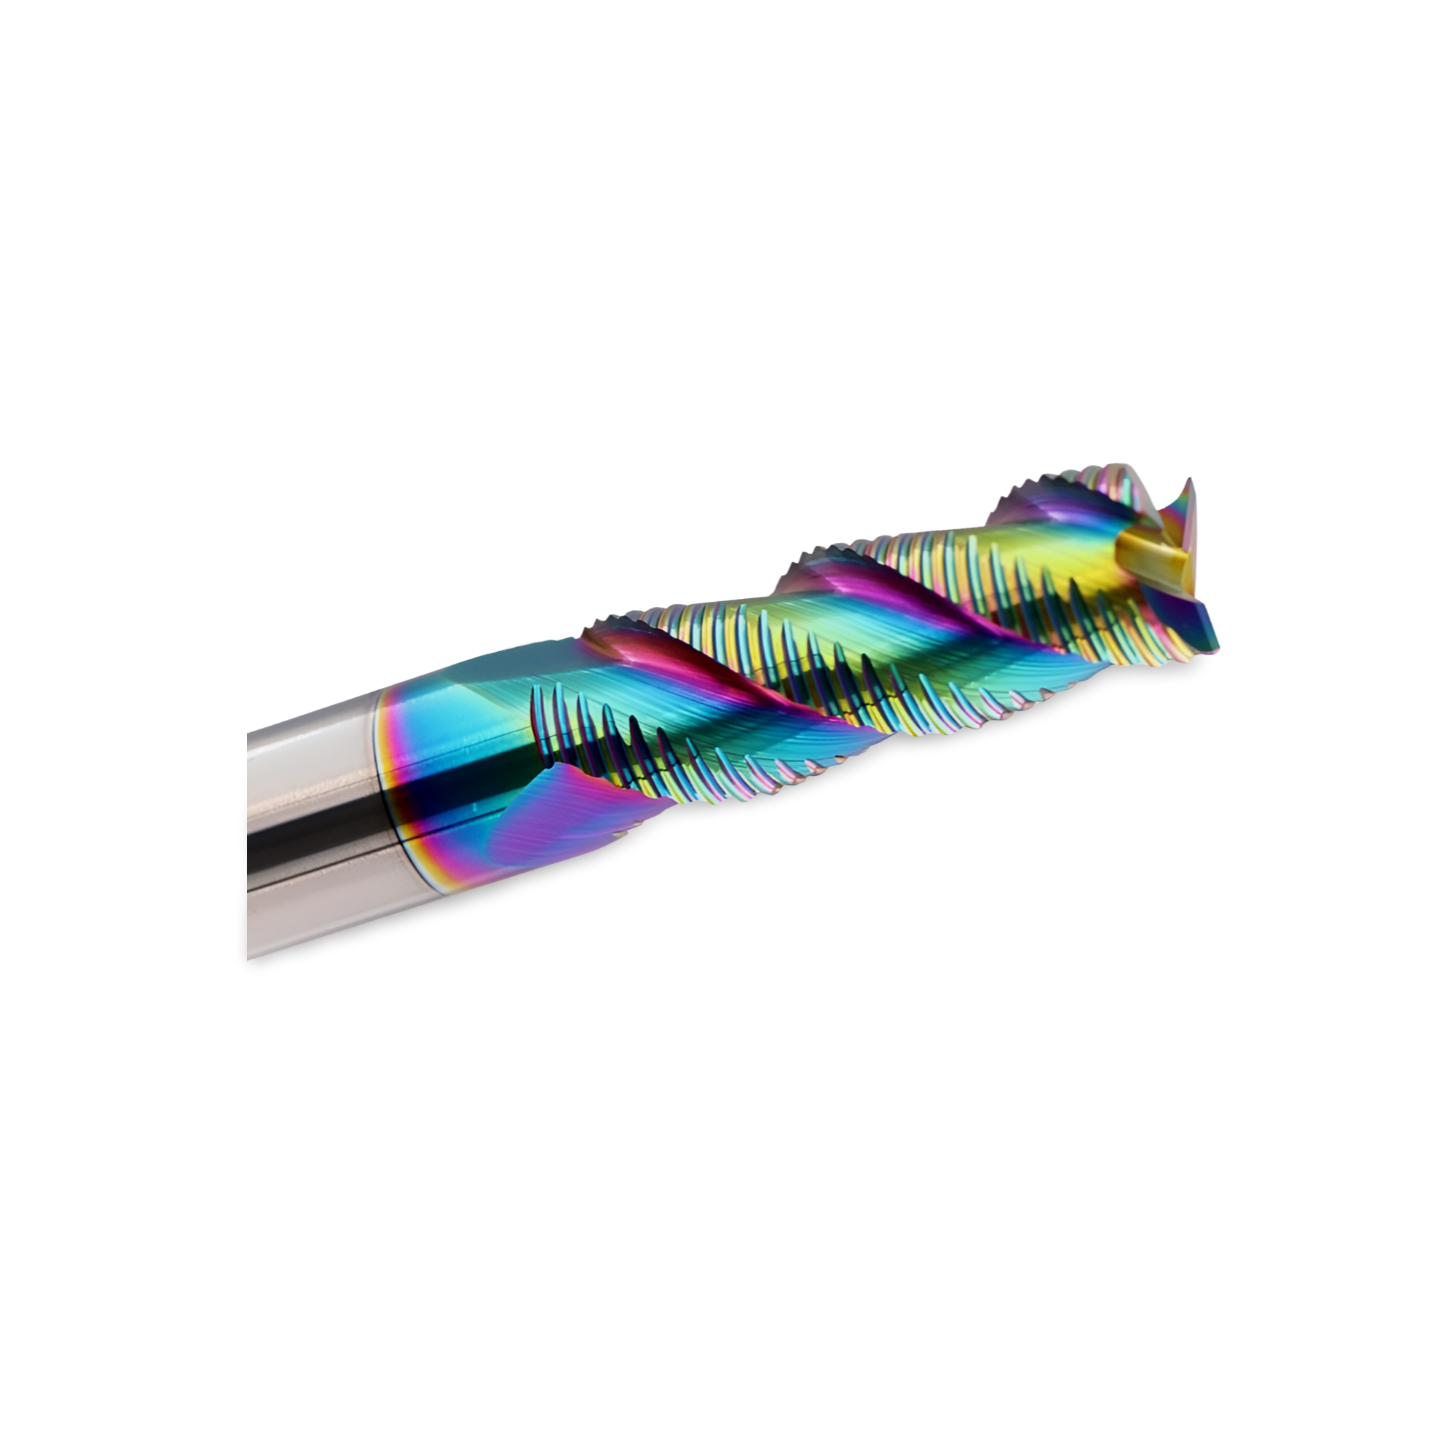
A solid carbide end mill with three serrated cutting edges and a DLC coating. The roughing geometry is designed for rough machining. Helical chip flutes, a 35° helix angle and a cylindrical shank form a tool intended for CNC milling machines and machining centres.
Applications and workpiece materials
Use the cutter for rough milling of aluminium and its alloys, other non-ferrous metals and suitable plastics. Select the cutting diameter, cutting-edge length and tool overhang to suit the workpiece and access to the cutting area.
| Material | Application |
|---|---|
| Aluminium and aluminium alloys | Rough milling of aluminium components. |
| Brass and bronze | Rough machining of non-ferrous metals. |
| Plastics | Rough milling with cutting conditions selected for the type of plastic. |
| Bakelite | Machining on a sufficiently rigid machine with suitable toolholding. |
Select the tool according to the workpiece material and operation. This is a roughing cutter; account for its intended use when planning subsequent surface finishing.
Construction and technical specifications
| Parameter | Specification |
|---|---|
| Tool type | Roughing end mill |
| Tool material | VHM — fine-grain solid carbide |
| Number of cutting edges | 3 |
| Cutting-edge geometry | Serrated / roughing |
| Helix angle | 35° |
| Coating | DLC — Diamond-Like Carbon |
| Shank | Cylindrical, with a chamfered end |
| Dimensions | Cutting diameter, cutting-edge length, shank diameter and overall length depend on the selected size. |
The helical flutes provide space for chip evacuation. The DLC coating reduces friction and wear, while the cutting section and shank have a one-piece carbide construction. The cutter features ground cutting edges and a large-core design.
Reading the size designation and selecting a variant
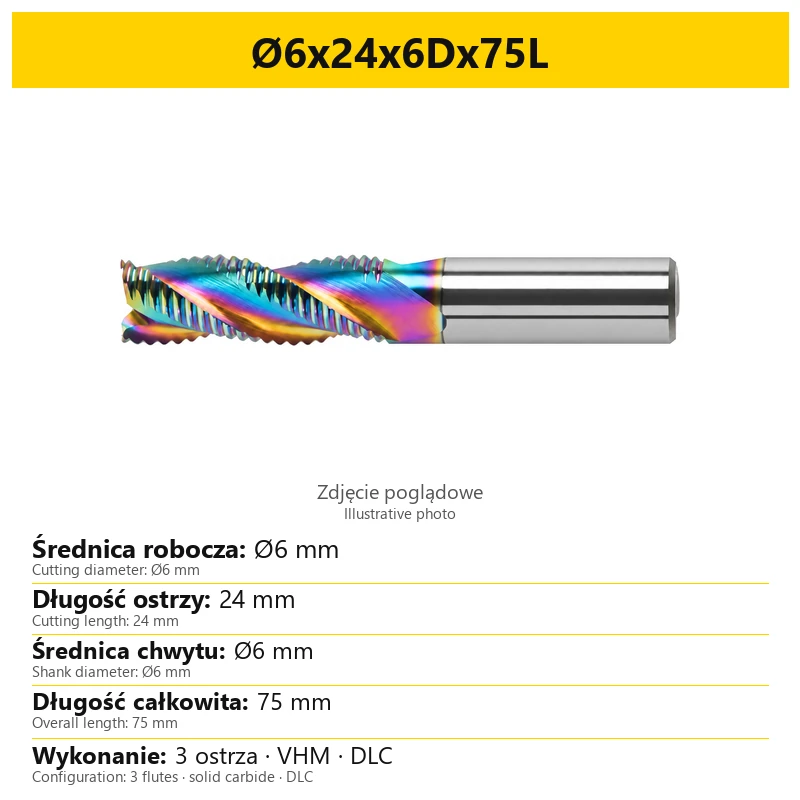
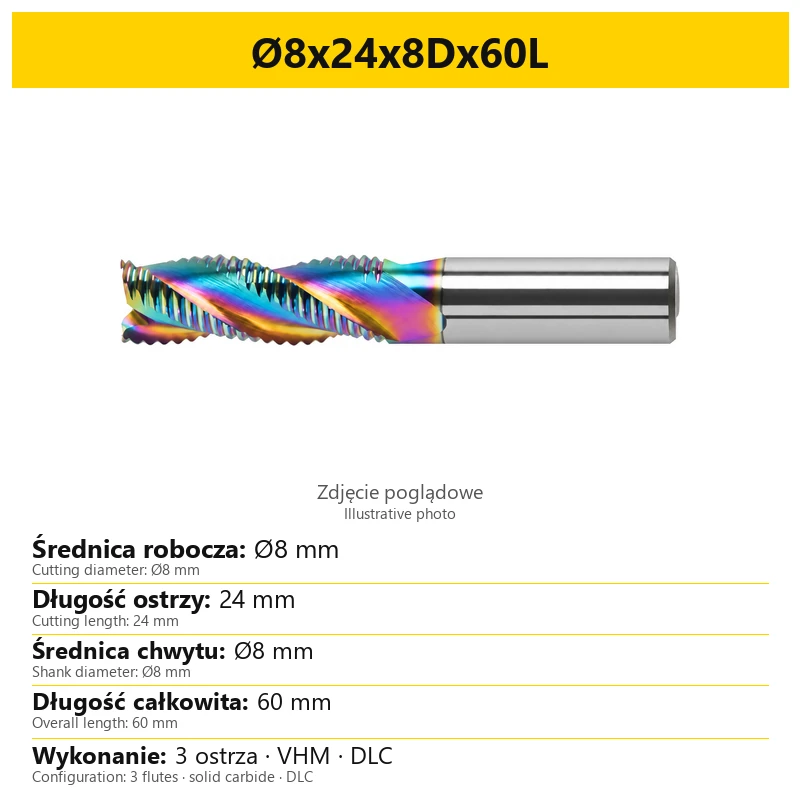
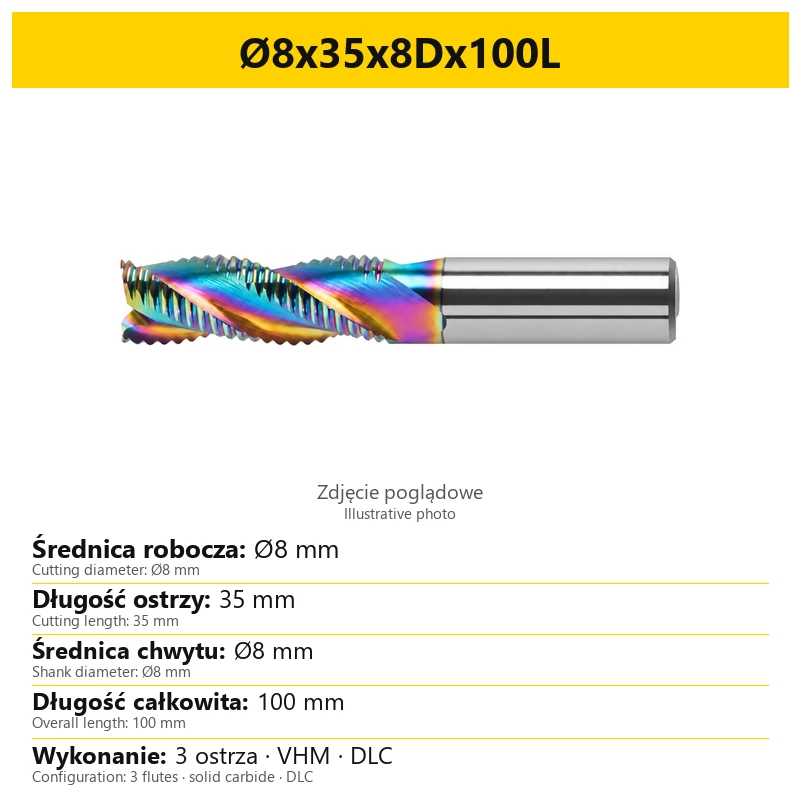
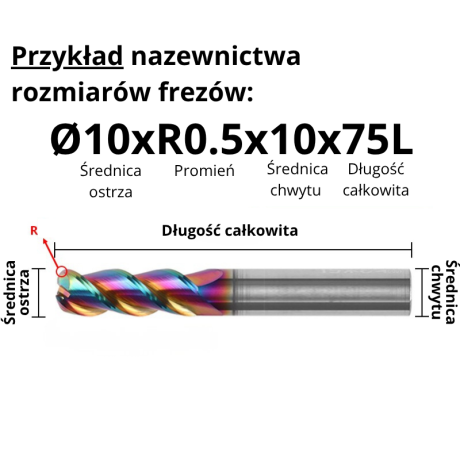
Example: Ø4x12x4Dx50L. The first number gives the cutting diameter, the second the cutting-edge length, D the shank diameter and L the overall length. All linear dimensions are in millimetres.
| Part of the designation | Meaning |
|---|---|
| Ø4 | Cutting diameter 4 mm |
| 12 | Cutting-edge length 12 mm |
| 4D | Cylindrical shank diameter 4 mm |
| 50L | Overall tool length 50 mm |
Cutting-edge length and overall length are different dimensions. Match the toolholder to the shank diameter. Do not choose the holder solely from the cutting diameter: some versions have a shank larger than their cutting section.
Available sizes are shown in the product selector. Compare the full designation and the length needed to reach the surface before selecting a variant.
Toolholding and checks before machining
- Measure tool runout. If it exceeds 0.01 mm, correct the setup before cutting.
- Keep tool overhang short. Use the shortest practical overhang that still provides access to the cutting area.
- Adjust cutting conditions for longer overhang. Reduce spindle speed, feed or the amount of material removed as appropriate.
- Use a suitable machine. The cutter is intended for CNC machining centres, CNC milling machines and engraving machines with suitable rigidity and spindle speed.
The tool is not intended for handheld drills, low-speed bench drills or unstable machines with manual feed. A rigid setup and correct toolholding are required for proper use.
Cooling, chip evacuation and operation
An air blast or coolant mist is recommended when machining aluminium. Clear chips from the cutting area and select spindle speed and feed to suit the tool diameter, workpiece material and setup.
If unusual vibration or noise occurs, reduce spindle speed and the amount of material removed, then check the tool setup. When moving to a longer cutter, select conditions for its overhang instead of automatically reusing the settings of a shorter tool.
Frequently asked questions
What makes this a roughing cutter?
It has serrated cutting edges for rough machining. This model has three cutting edges and helical chip flutes.
What does DLC stand for?
Diamond-Like Carbon — the coating used on the cutting section. It reduces friction and tool wear.
Is the shank diameter always the same as the cutting diameter?
No. Check D in the selected size designation. Some versions have a larger shank than their cutting section.
Can this cutter be used in a handheld drill?
No. It requires a sufficiently rigid machine, suitable toolholding and spindle speed matched to the operation.
Bestsellers
-
Bestseller
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.86Price €56.79without VAT -
Bestseller
Kortools Adhesive + Tape CNC Workholding Kit
Yellow tape 5cm x 50m; adhesive 100g Yellow tape 5cm x 50m; adhesive 500g Yellow tape 10cm x 50m; adhesive 100g Yellow tape 10cm x 50m; adhesive 500g Green tape 5cm x 50m; adhesive 100g + 7 morePrice €44.66Price €36.31without VAT -
Price €17.18Price €13.97without VAT
-
Price €7.10Price €5.77without VAT
-
Price €7.56Price €6.14without VAT
-
Bestseller
 Other Accessories 0.00
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.82Price €43.76without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.14Price €8.25without VAT -
Bestseller
 2-Flute End Mills 0.00
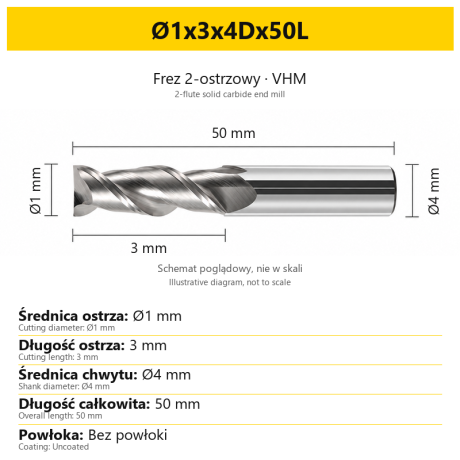
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.35Price €4.35without VAT -
Bestseller
 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.40Price €3.58without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.89Price €6.41without VAT -
Bestseller
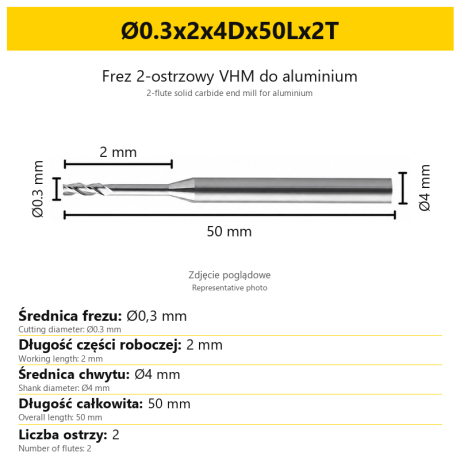 2-Flute End Mills 0.00
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.99Price €6.50without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.28Price €5.92without VAT -
Bestseller
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €4.96Price €4.04without VAT -
Bestseller
 3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.10Price €4.15without VAT -
Bestseller

 Countersinks 0.00
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.81Price €3.91without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.07Price €4.12without VAT


