
















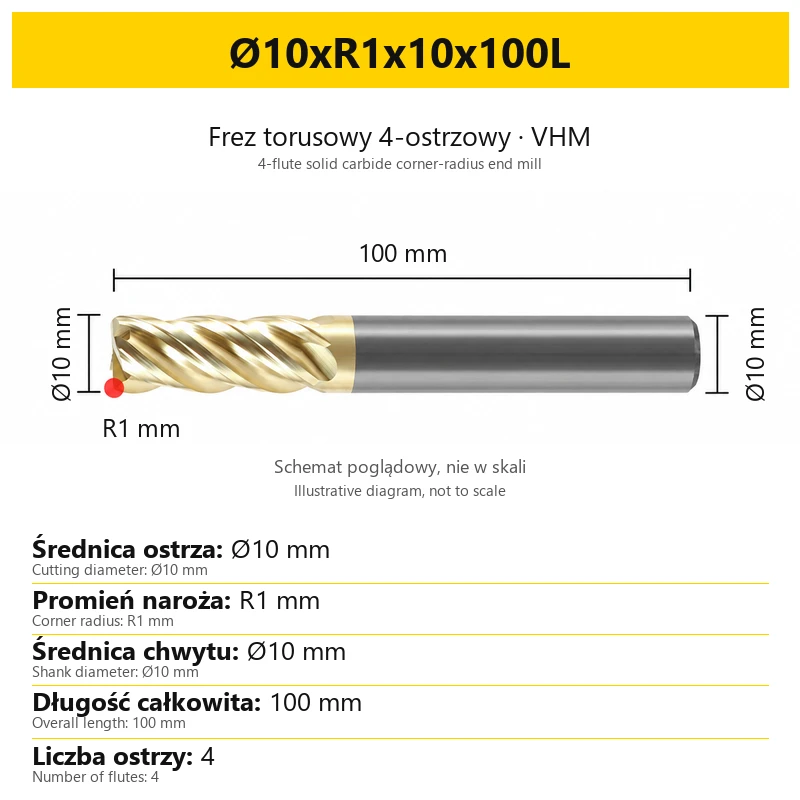
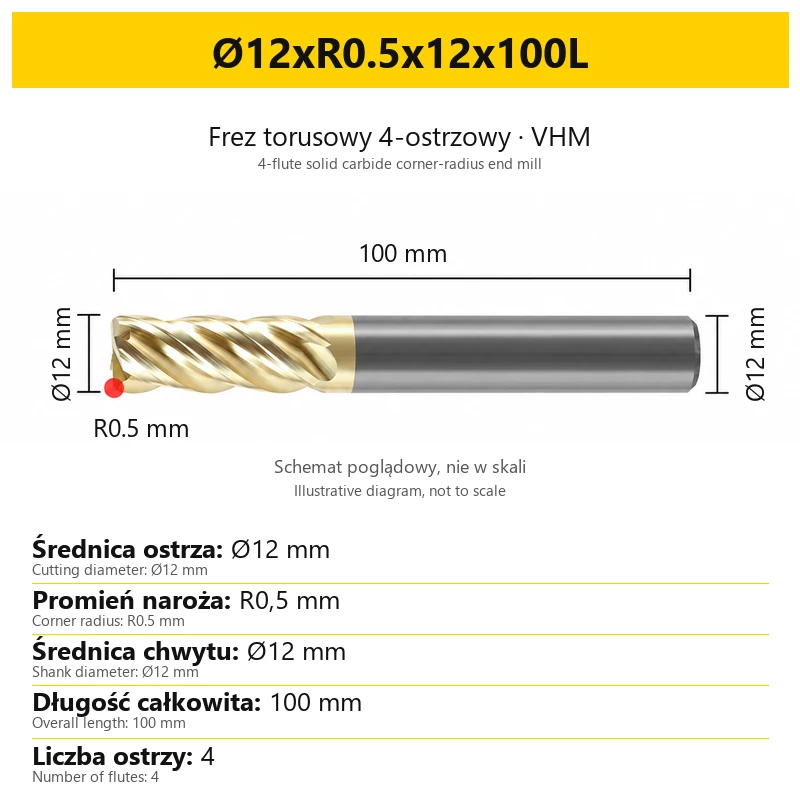


4-Flute ZrN Coated Carbide Corner Radius End Mill | VHM | VELOCITY
Shipping costs are not included in the price.
Shipping costs are not included in the price.
Ask about the product

The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: BD1F-910CB
Product description
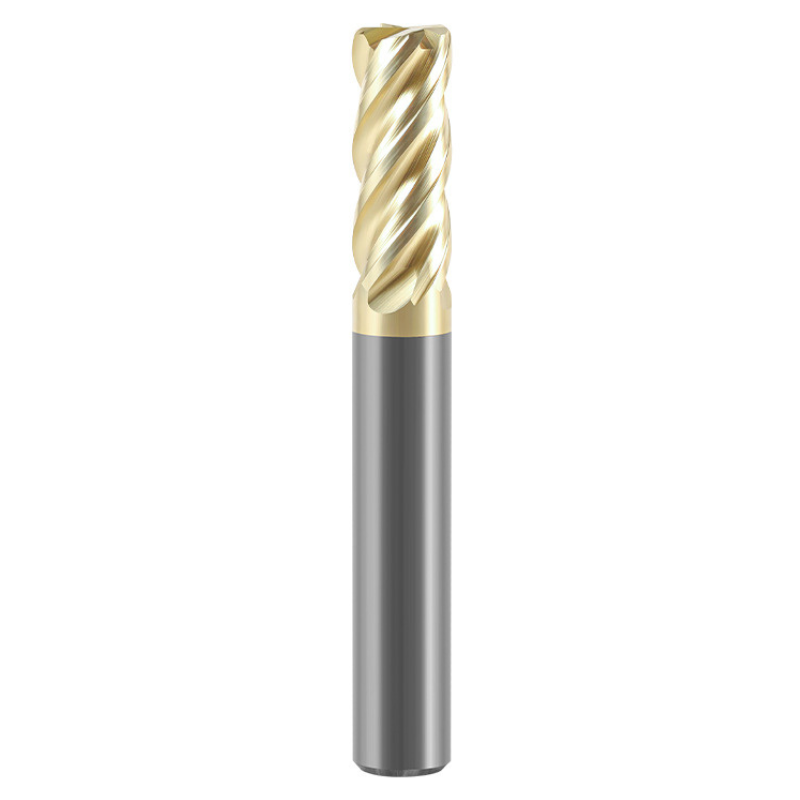
VELOCITY — 4-flute solid carbide corner-radius end mill, ZrN
Ø1–12 mm cutting diameters · R0.2 / R0.5 / R1 mm corner radii · 50–100 mm overall lengths
A monolithic solid carbide (VHM) end mill with four flutes and a ZrN coating. Rounded cutting corners connect the end face to the peripheral cutting section. The corner-radius geometry produces a radiused transition between a machined floor and wall.
Select the variant by cutting diameter, corner radius R, shank diameter and overall length. Consider all four dimensions together: an identical cutting diameter does not imply the same corner radius or tool reach.
1. Geometry and applications
| Feature / task | Selection guidance |
|---|---|
| Floor-to-wall radius | R specifies the rounded cutting corner. Match it to the required surface transition and include it in the CAM tool definition. |
| Contours, steps and pockets | Cutting diameter determines access to the machining area. Corner radius affects the shape of the surface junction, while overall length affects reach after clamping. |
| Small and recessed features | Choose the variant for the available space. Check clearance for the cutting section, shank and holder throughout the planned toolpath. |
A corner-radius end mill has rounded corners, but does not have the hemispherical end face of a ball-nose end mill. R is not half the cutting diameter. Cutting conditions must account for the workpiece material grade and condition, and the type of operation.
2. Tool construction and specifications
| Parameter | Value |
|---|---|
| Tool type | Monolithic corner-radius end mill |
| Tool material | VHM — solid carbide |
| Coating | ZrN |
| Number of flutes | 4 — designated 4T / Z4 |
| Cutting diameter | Ø1–12 mm, depending on the variant |
| Corner radius | R0.2 / R0.5 / R1 mm, depending on the variant |
| Shank diameter | Ø3–12 mm, depending on the variant |
| Overall length | 50 / 60 / 75 / 100 mm, depending on the variant |
| Shank | Cylindrical |
| Helix and flute spacing | Variable helix 39.5° / 40.5°; unequal flute spacing |
The ranges describe the tool family. Not every diameter is available with every radius and length. The selected variant and its card show the exact combination of dimensions. Flute count and helix geometry are inputs to cutting-condition selection; they do not determine spindle speed or feed on their own.
3. Machining operations
| Operation | What to check before machining |
|---|---|
| Side and contour milling | Match cutting diameter to the contour and cutting length to the wall height. Account for the corner radius at the transition to the floor. |
| Pockets and steps | Match diameter and radius to the pocket geometry. Plan entry, exit and chip evacuation from the recess. |
| Flat surfaces | Account for the corner-radius geometry, stock allowance and stepover. Program the path for the required shape and surface finish. |
| Slot milling | Check the required width and floor corner radii. Full-width engagement requires separate load selection and effective chip evacuation. |
4. How to select a variant
- Start with the cutting diameter. Check the minimum width of the machining area and contour radii in the XY plane. The corner radius R does not replace this check.
- Select the corner radius R. Compare it with the required floor-to-wall fillet. Enter the actual corner radius in the CAM tool definition.
- Check the shank diameter. It need not equal the cutting diameter. Select the collet or holder for the shank and the requirements of the clamping system.
- Choose enough length for access. Use the shortest overhang that can complete the operation. An extended variant requires a fresh assessment of rigidity and cutting load.
- Compare the full designation. In addition to the four dimensions, check cutting length and workpiece clearance. The size selector shows the available combinations.
5. How to read the dimensions
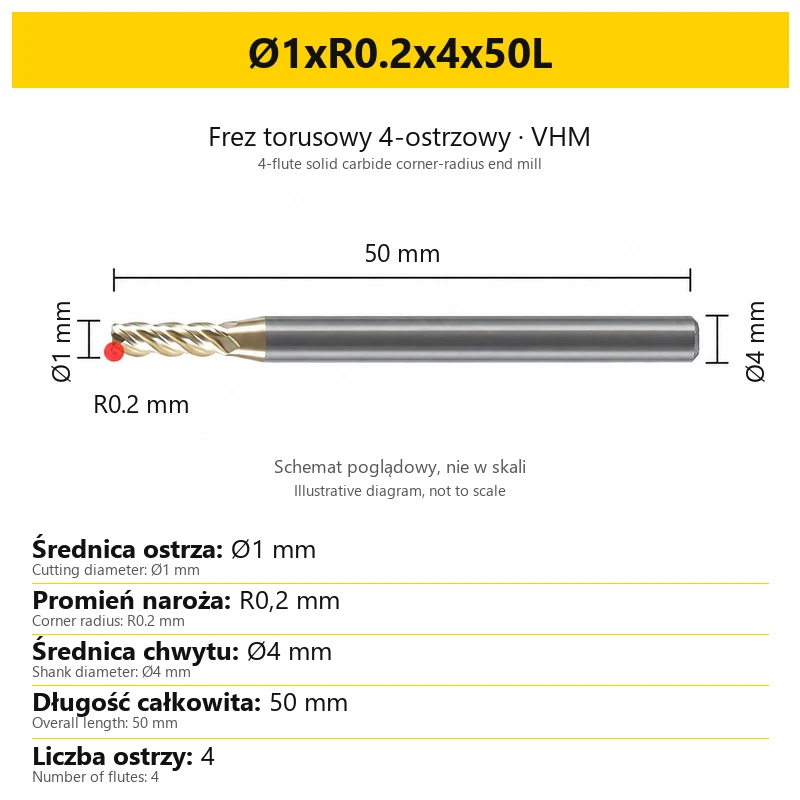
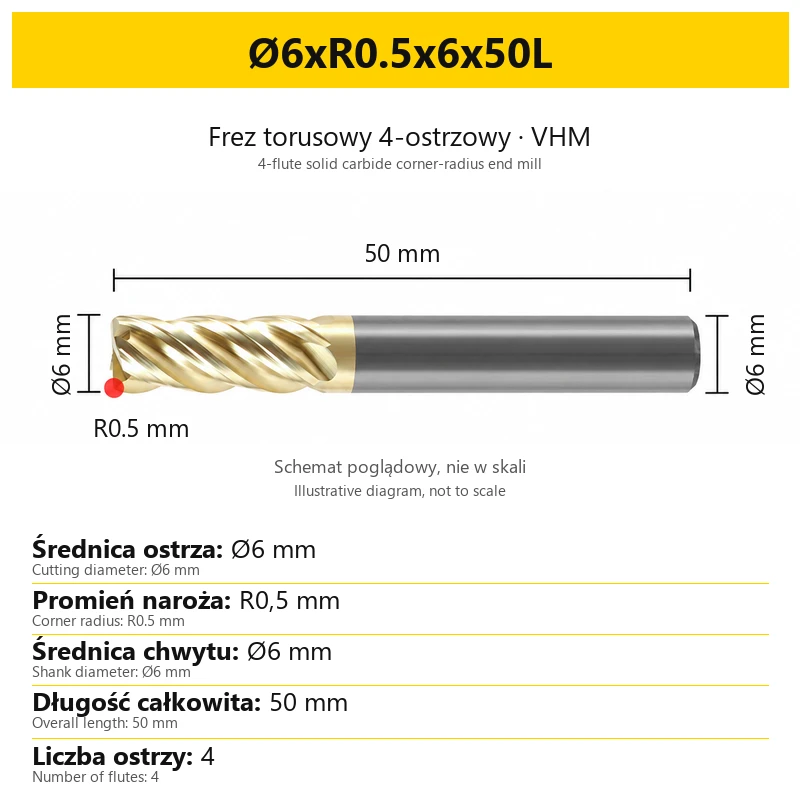
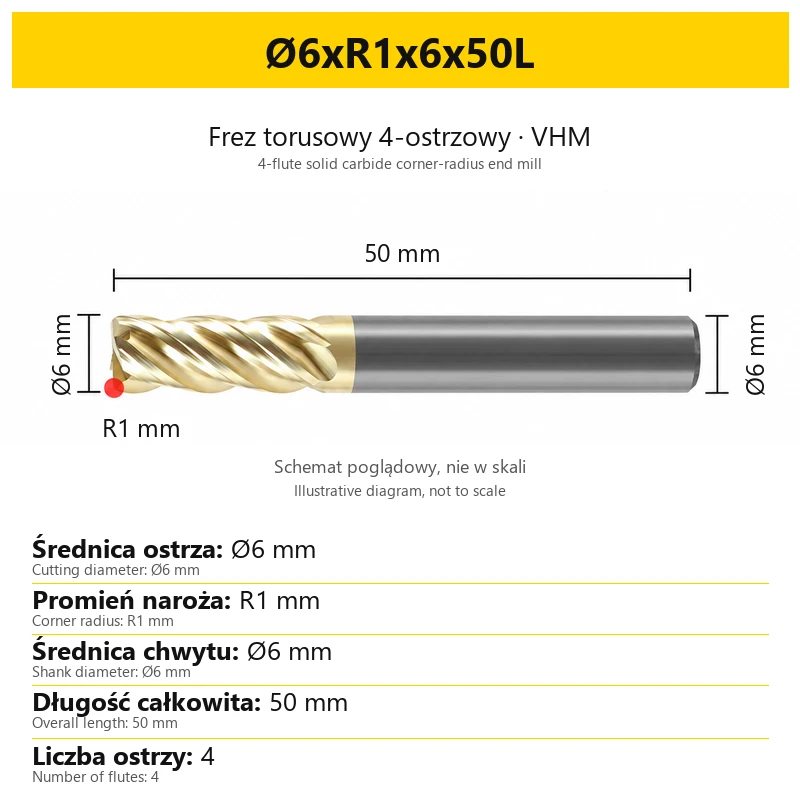
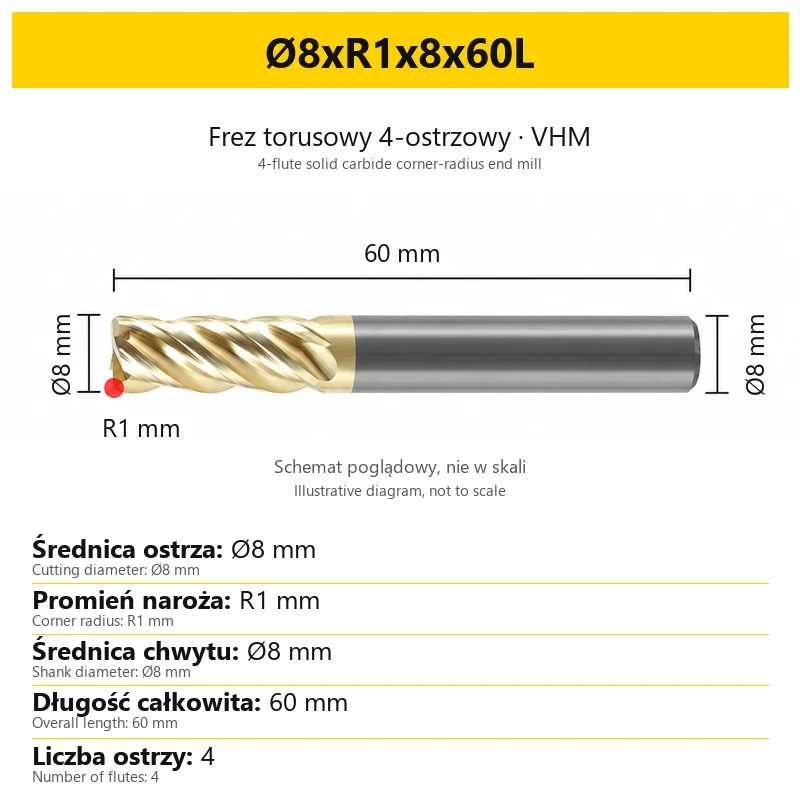
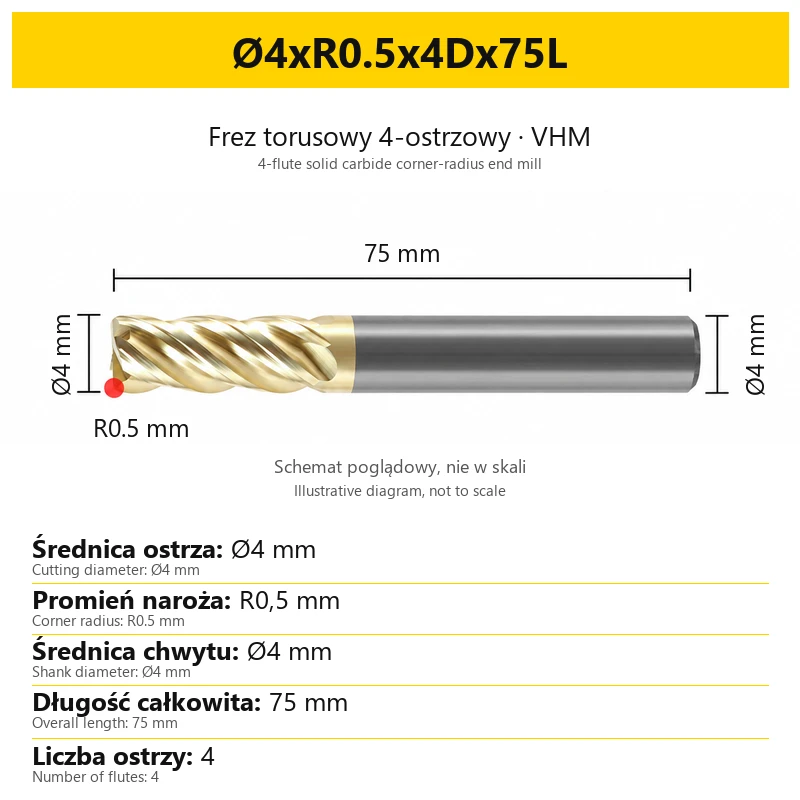
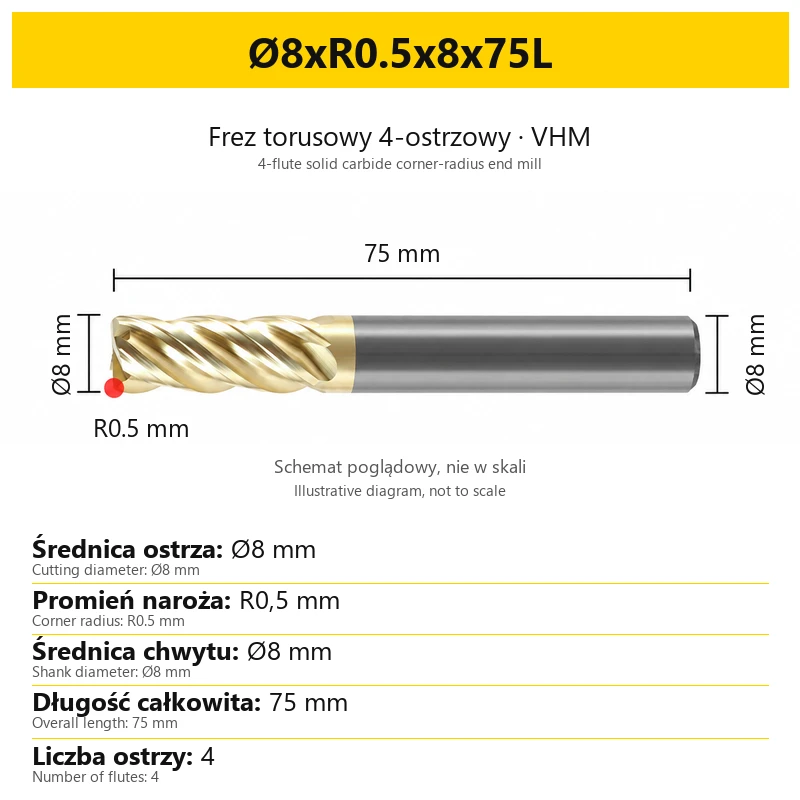
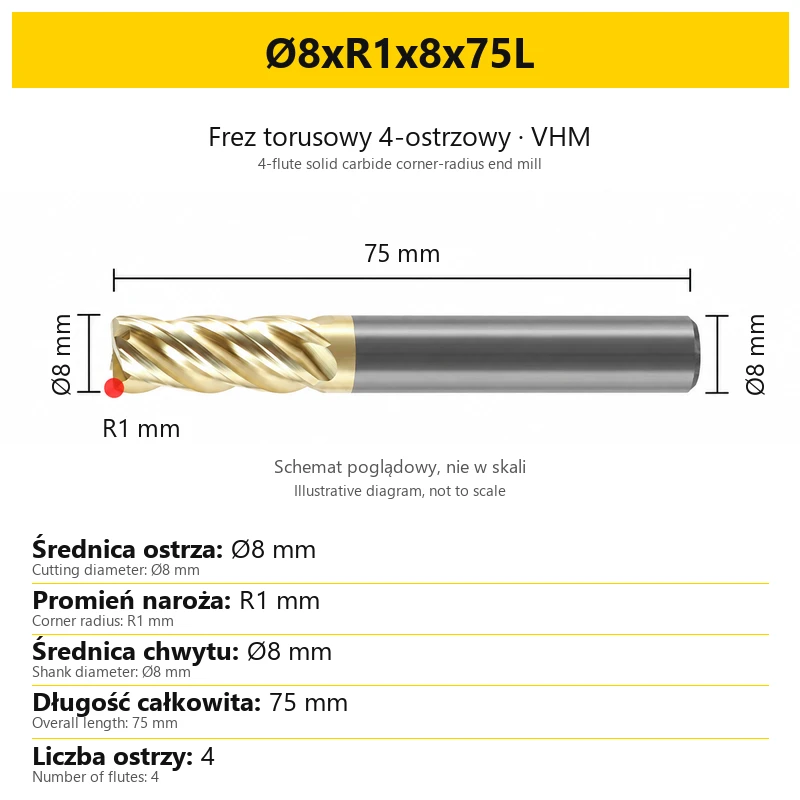
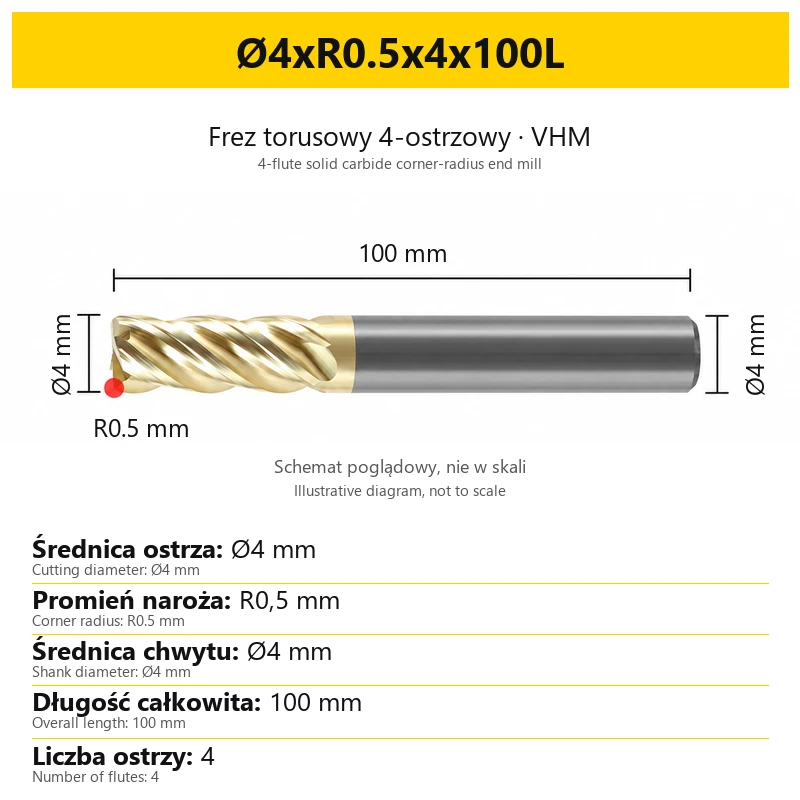
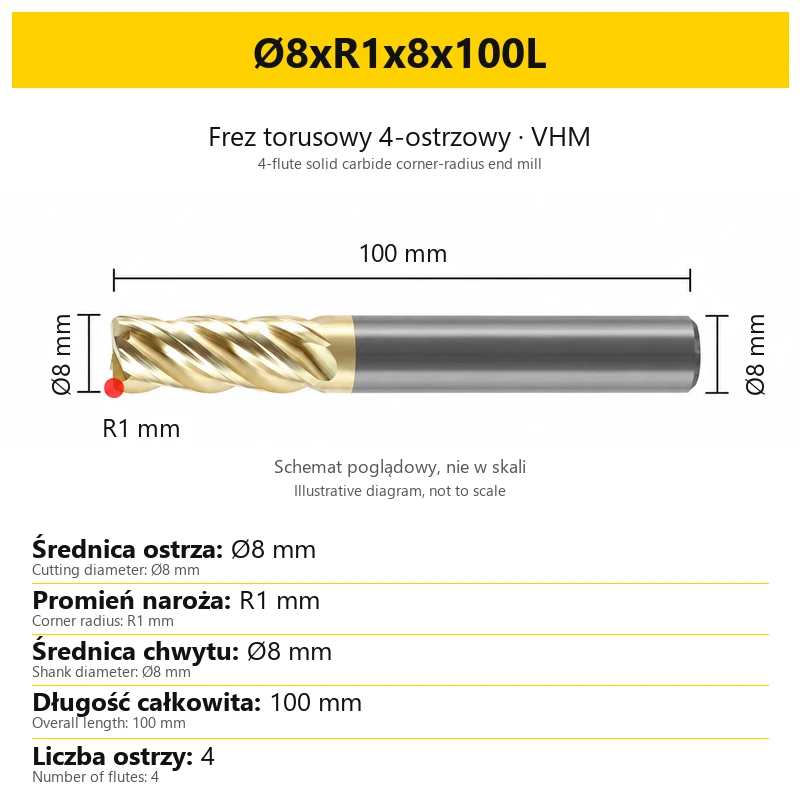
Example: Ø1xR0.2x4x50L. All dimensions are in millimetres; the dot in the code is the decimal separator.
| Designation element | Meaning | Example value |
|---|---|---|
| Ø1 | Cutting diameter | 1 mm |
| R0.2 | Cutting corner radius | 0.2 mm |
| 4 | Shank diameter | 4 mm |
| 50L | Overall tool length | 50 mm |
Some designations include the additional letter D after the shank diameter. L indicates overall length. 4T / Z4 denotes four flutes, not the number of tools supplied.
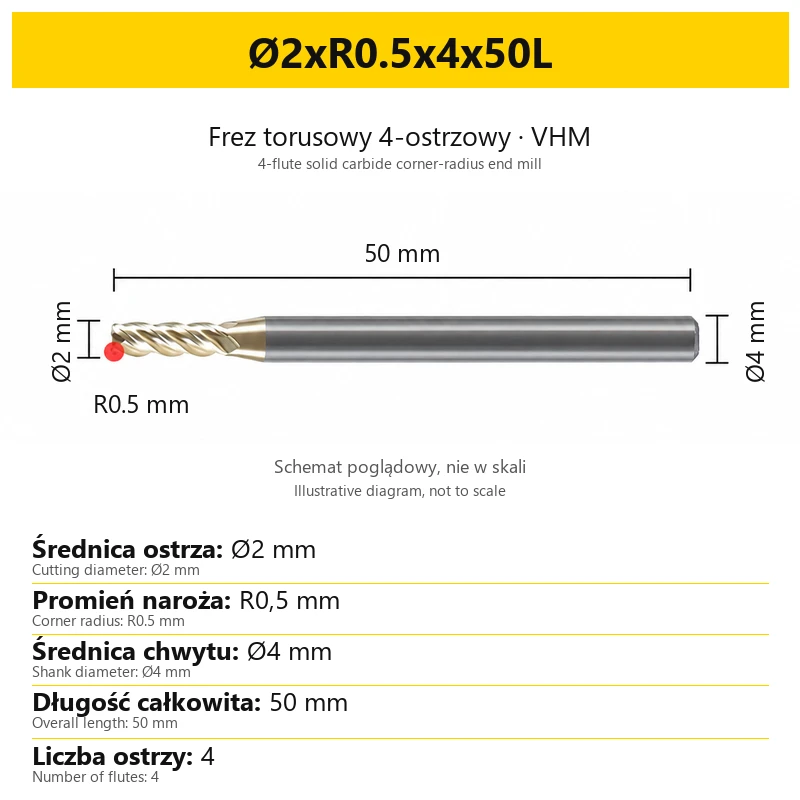
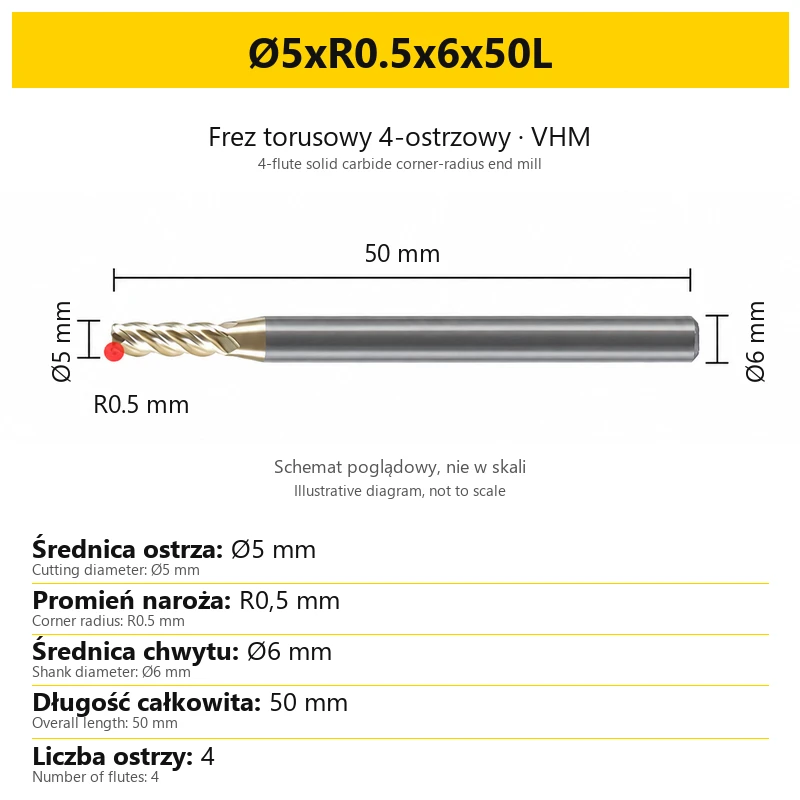
Variant cards contain an illustrative diagram and the dimensions of the selected size. Select from the numerical values; photograph proportions must not be used to measure diameter, radius or length.
6. Clamping and cutting conditions
- Check the shank and holder. Clamping surfaces should be clean and undamaged. Maintain the clamping length required by the holder.
- Minimise runout and overhang. This is especially relevant for small diameters and longer tools. Also check workholding rigidity.
- Enter the correct CAM geometry. Set cutting diameter and corner radius, then check for collisions involving the complete tool and holder assembly.
- Select speed, feed and engagement. Account for material grade and condition, diameter, four flutes, overhang and operation. Do not automatically transfer settings from a short tool to an extended one.
- Monitor chips and cutting edges. Match coolant or lubrication to the process and machine. If vibration increases or finish deteriorates, check the tool, clamping and cutting conditions.
For parameter selection, provide the full tool size, workpiece material, operation, axial and radial engagement, and overhang. Coating designation alone does not replace cutting-condition selection for the actual process.
7. What you receive
| Item | Order contents |
|---|---|
| Unit of sale | 1 VELOCITY 4-flute solid carbide corner-radius end mill with ZrN coating |
| Size | The variant selected in the product selector |
The quantity field sets the number of tools of the selected variant. Images showing multiple tools illustrate the product family and do not indicate a set.
8. Frequently asked questions
How does a corner-radius end mill differ from a ball-nose end mill?
A corner-radius end mill has rounded cutting corners at the perimeter of its end face. A ball-nose end mill has a hemispherical end face. The choice affects surface generation and the CAM tool definition.
Does R0.5 mean a 0.5 mm cutting diameter?
No. R0.5 specifies a 0.5 mm corner radius. A separate value preceded by Ø indicates the cutting diameter.
Can a 100 mm tool machine to a depth of 100 mm?
No. This is the overall tool length, including the section held in the holder. Cutting length, overhang and workpiece access are among the factors limiting machining depth.
Does shank diameter always equal cutting diameter?
No. For example, the variant with a 1 mm cutting diameter has a Ø4 mm shank. Check the shank dimension in the complete variant code when choosing the holder.
Do settings for a short variant apply to an extended one?
Not automatically. Additional overhang changes system rigidity. Verify cutting conditions for the actual tool length, clamping and operation.
Bestsellers
-
Bestseller
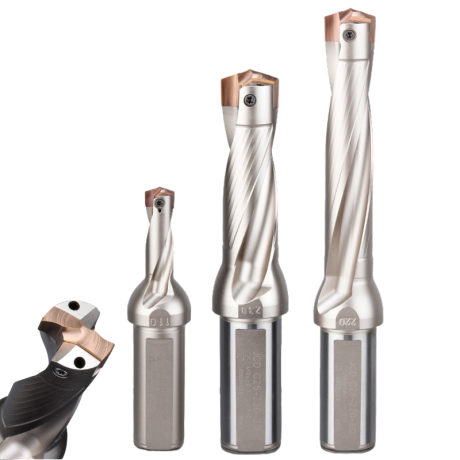
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.86Price €56.79without VAT -
Bestseller
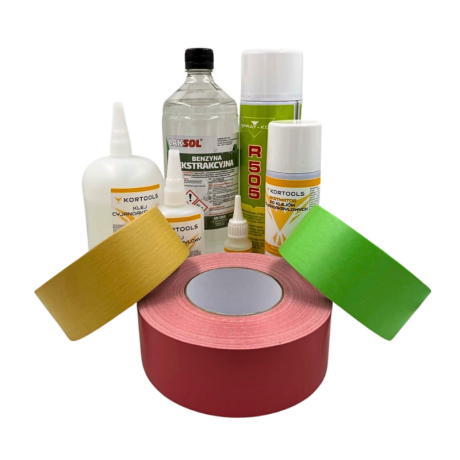
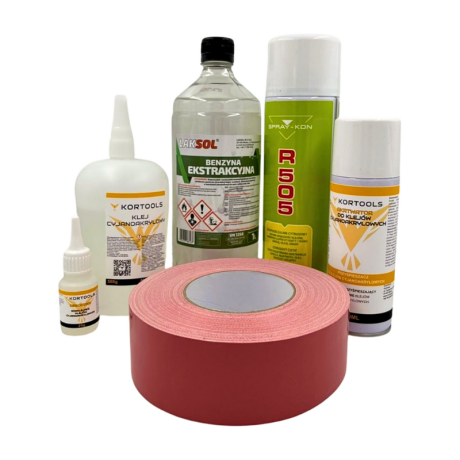
Kortools Adhesive + Tape CNC Workholding Kit
Yellow tape 5cm x 50m; adhesive 100g Yellow tape 5cm x 50m; adhesive 500g Yellow tape 10cm x 50m; adhesive 100g Yellow tape 10cm x 50m; adhesive 500g Green tape 5cm x 50m; adhesive 100g + 7 morePrice €44.66Price €36.31without VAT -
Price €17.18Price €13.97without VAT
-
Price €7.10Price €5.77without VAT
-
Price €7.56Price €6.14without VAT
-
Bestseller
 Other Accessories 0.00
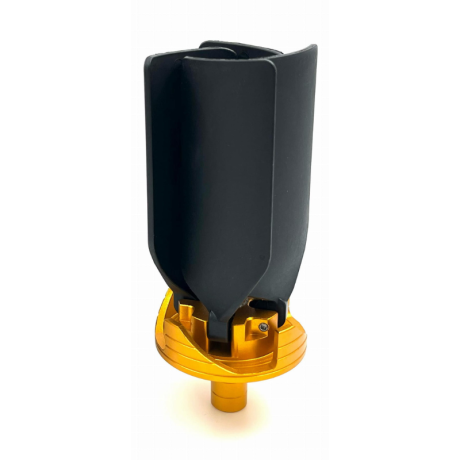
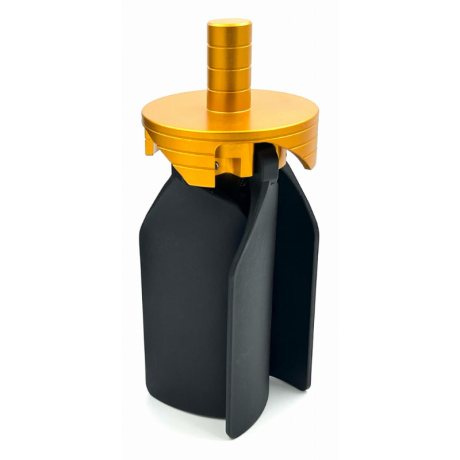
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.82Price €43.76without VAT -
Bestseller
 Ball Nose End Mills 0.00
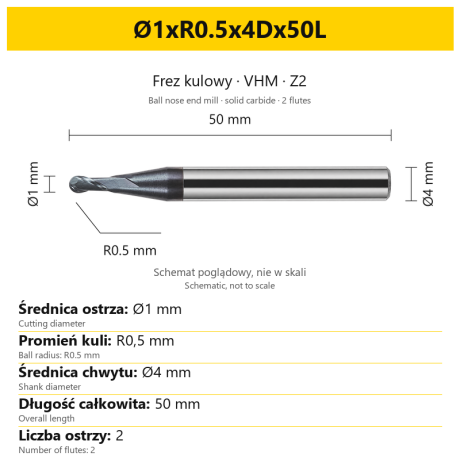
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.14Price €8.25without VAT -
Bestseller
 2-Flute End Mills 0.00
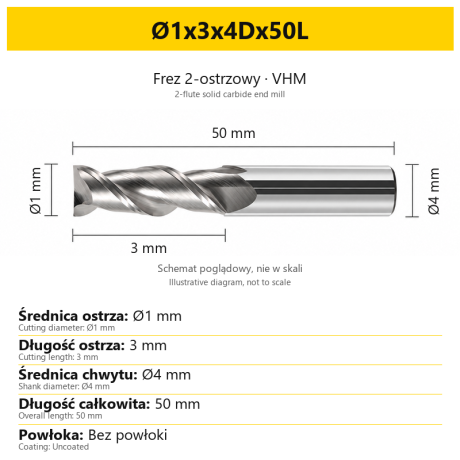
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.35Price €4.35without VAT -
Bestseller
 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.40Price €3.58without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.89Price €6.41without VAT -
Bestseller
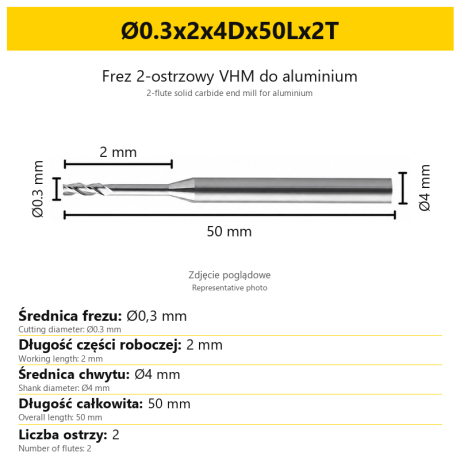 2-Flute End Mills 0.00
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.99Price €6.50without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.28Price €5.92without VAT -
Bestseller
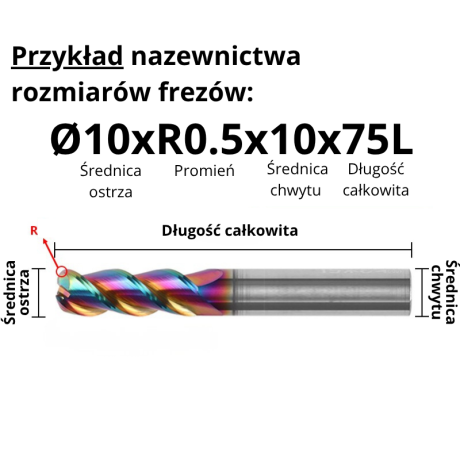
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €4.96Price €4.04without VAT -
Bestseller
 3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.10Price €4.15without VAT -
Bestseller

 Countersinks 0.00
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.81Price €3.91without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.07Price €4.12without VAT


