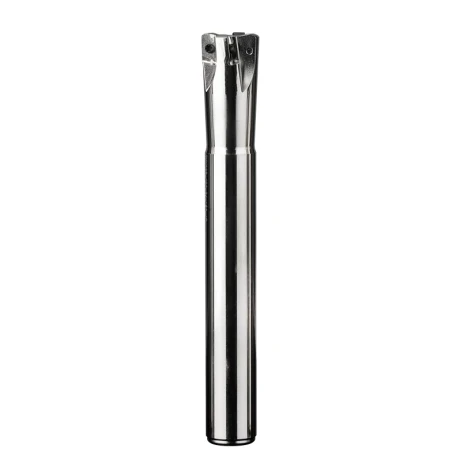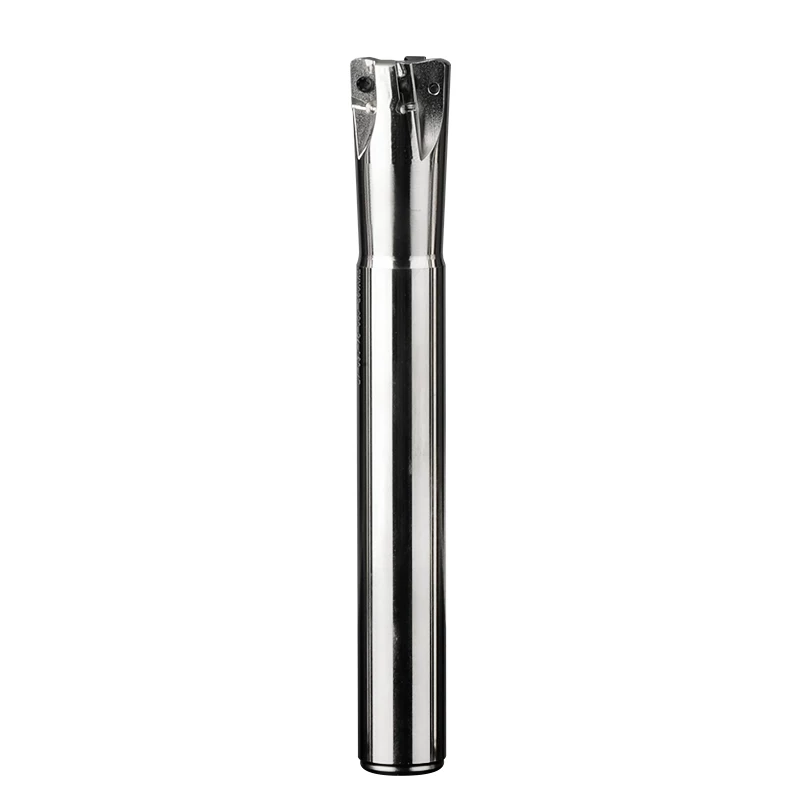
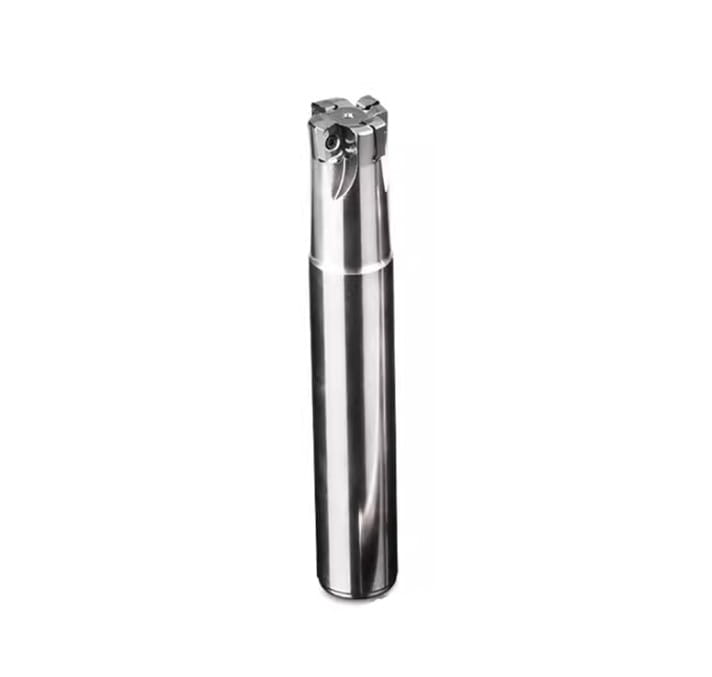
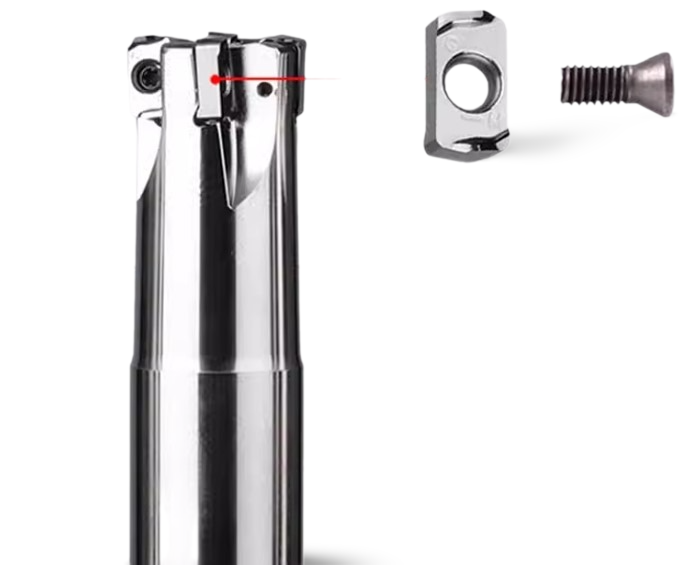
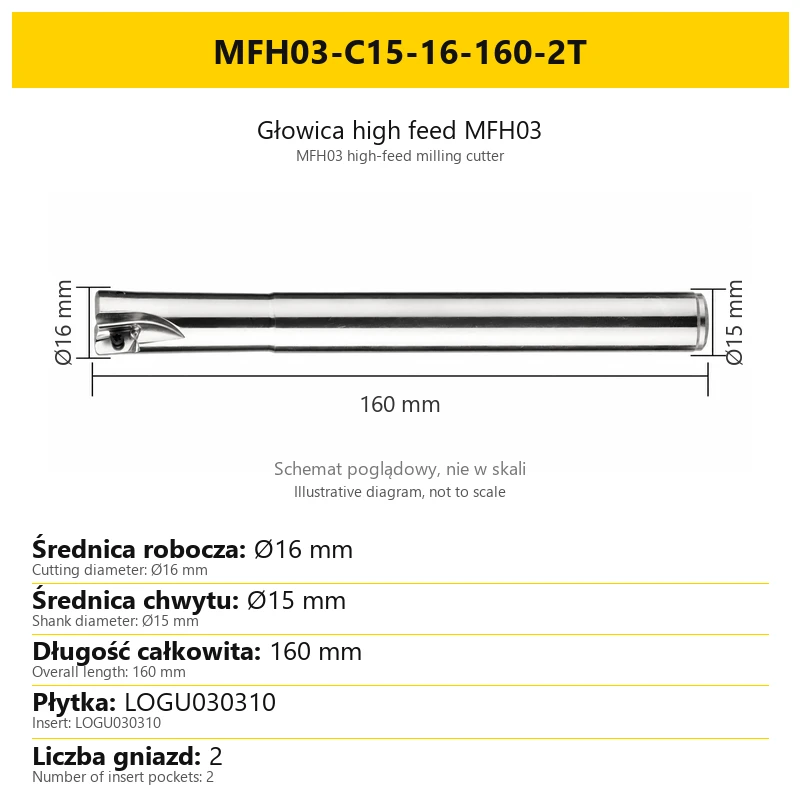
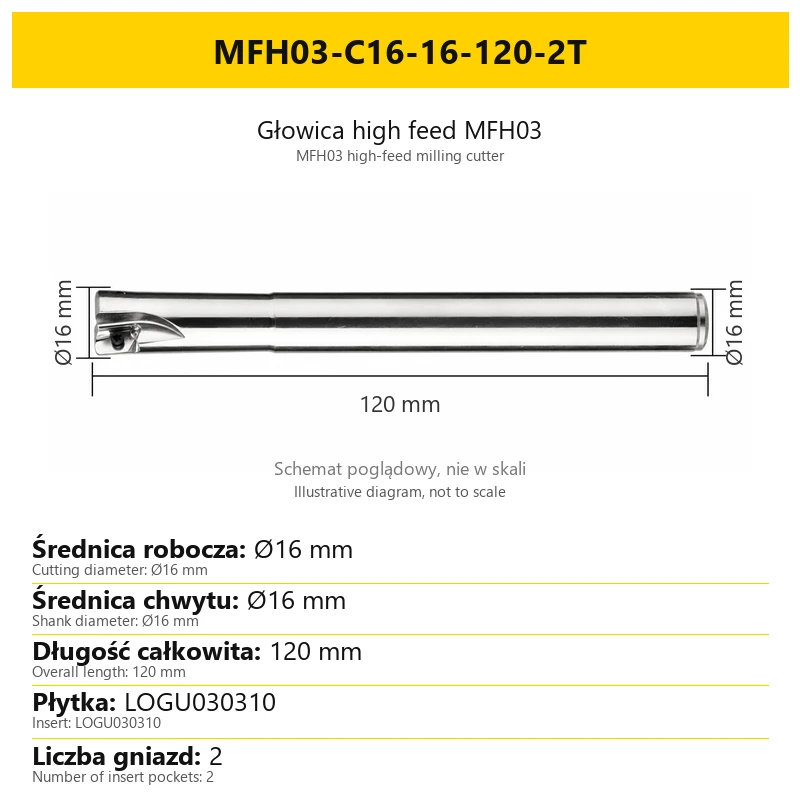
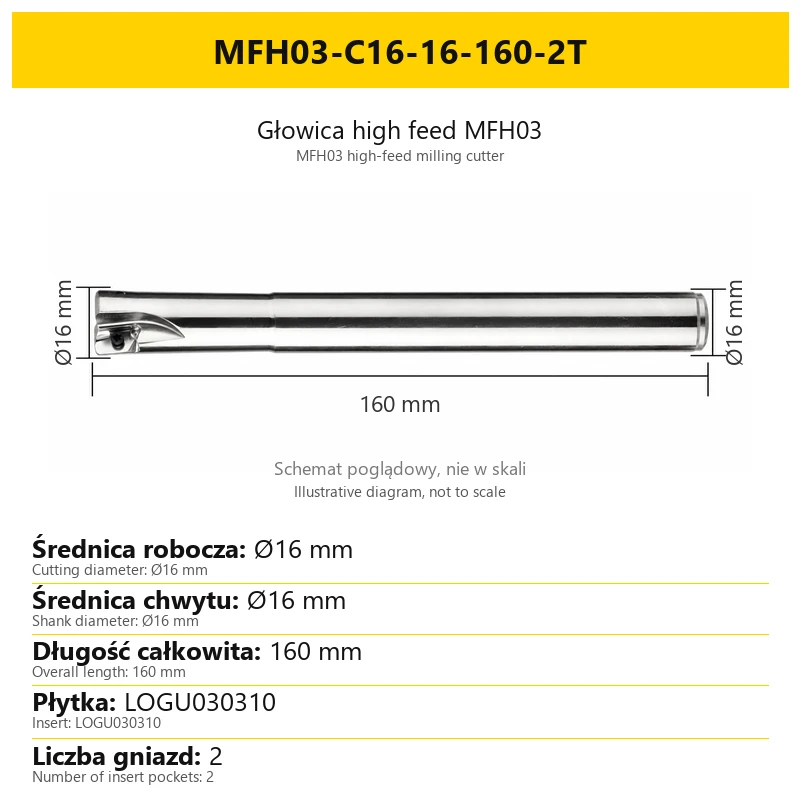
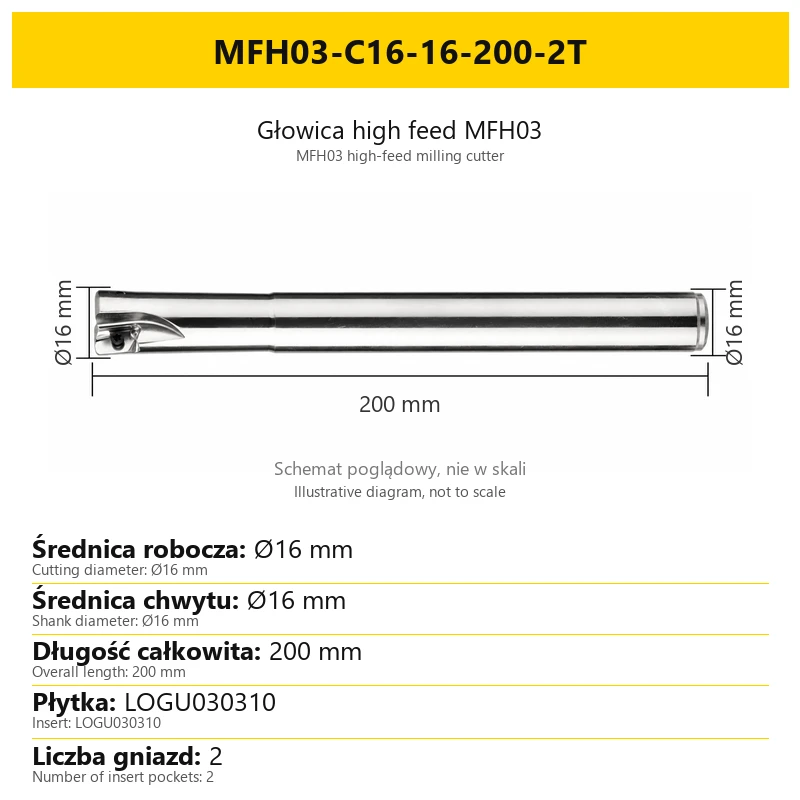
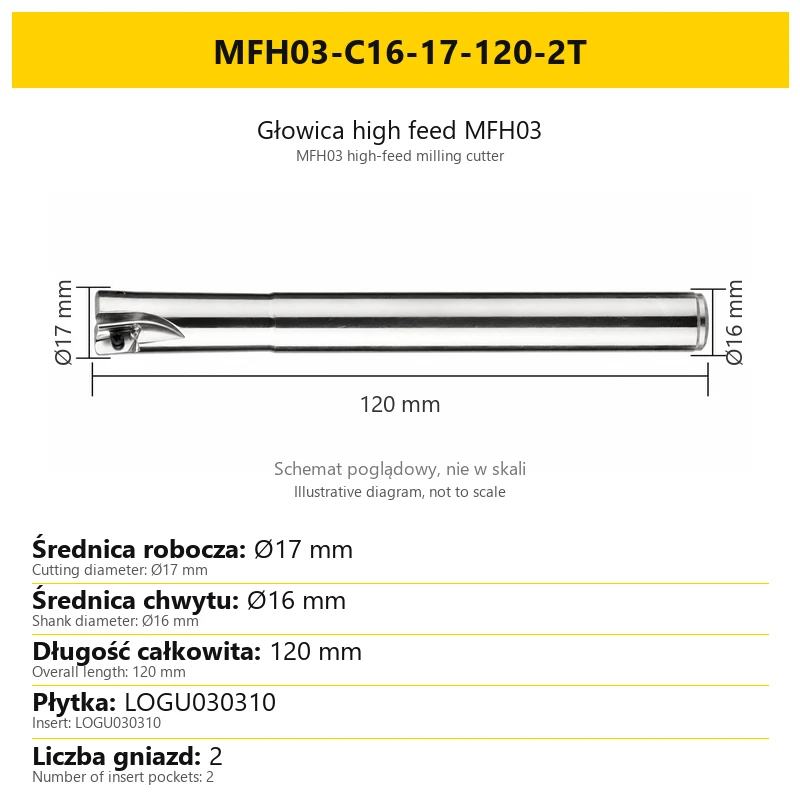
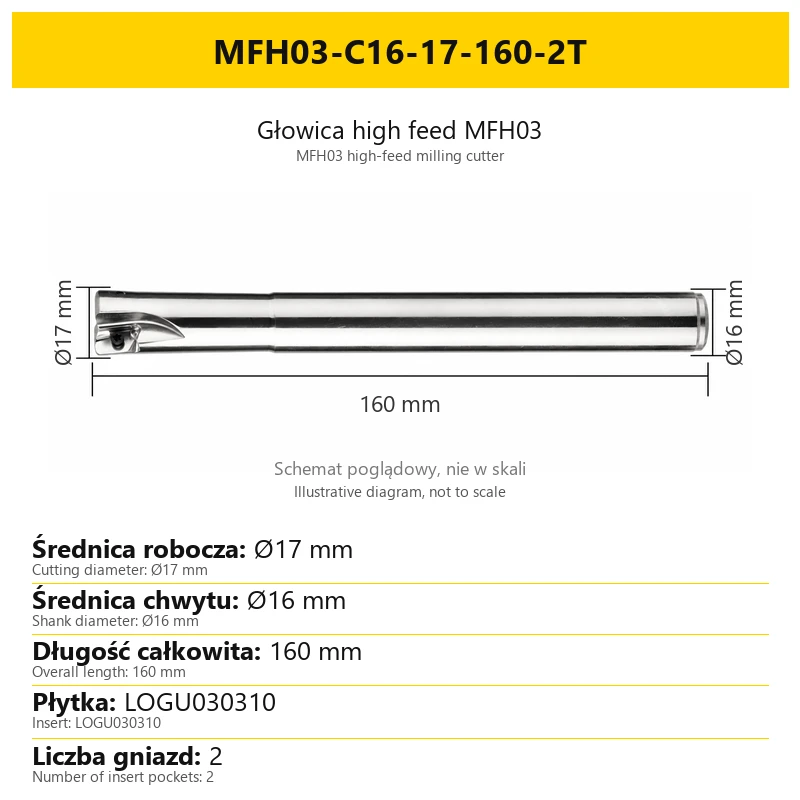
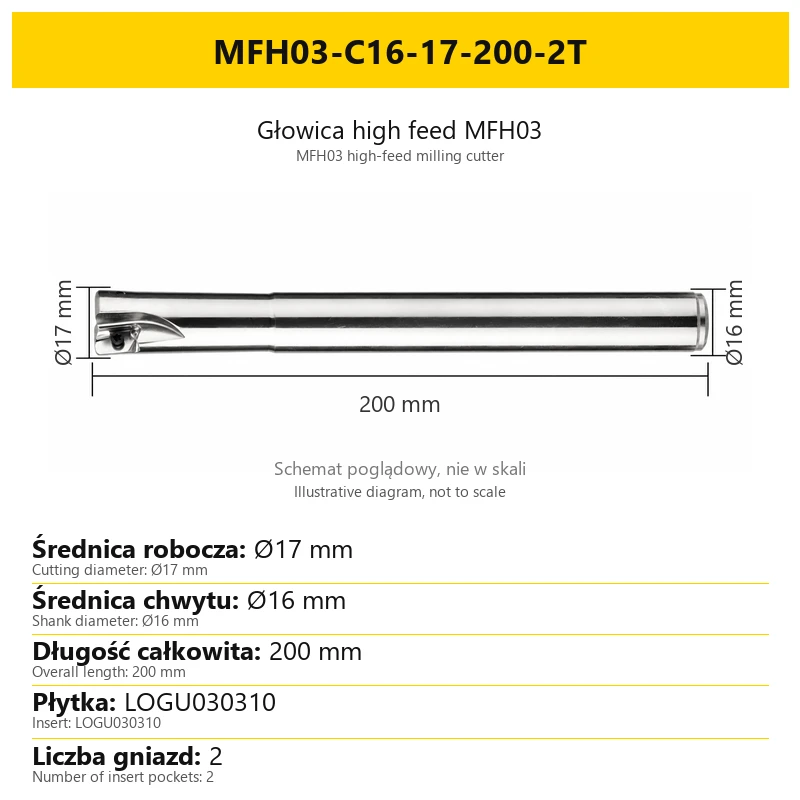
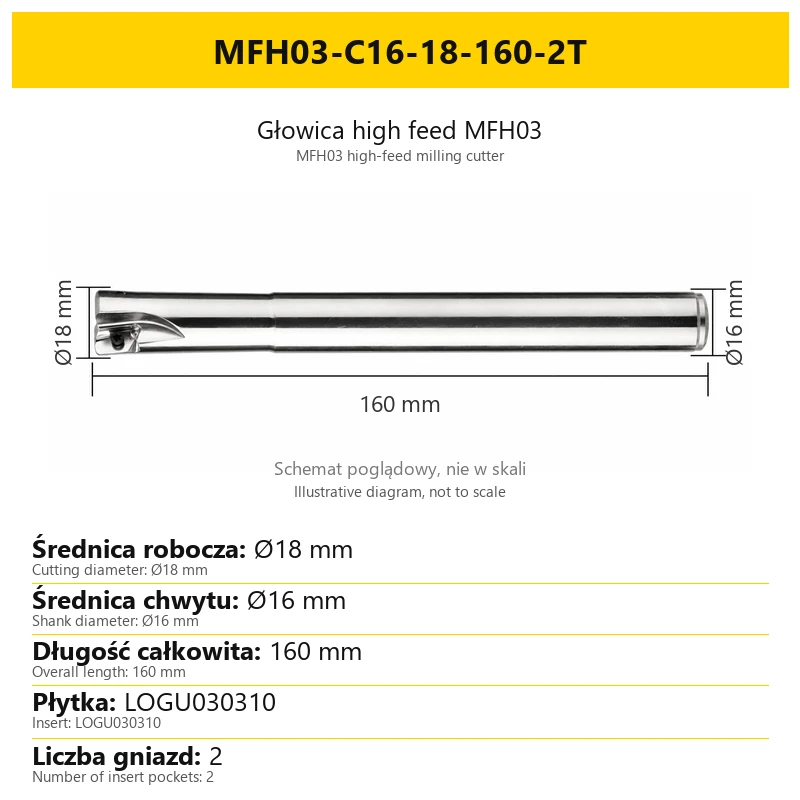
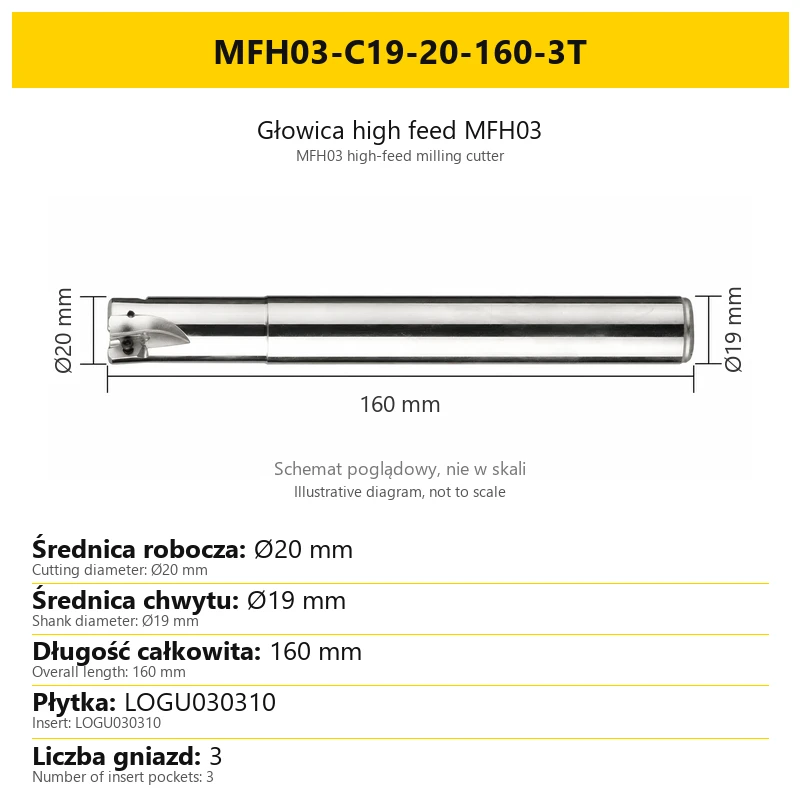
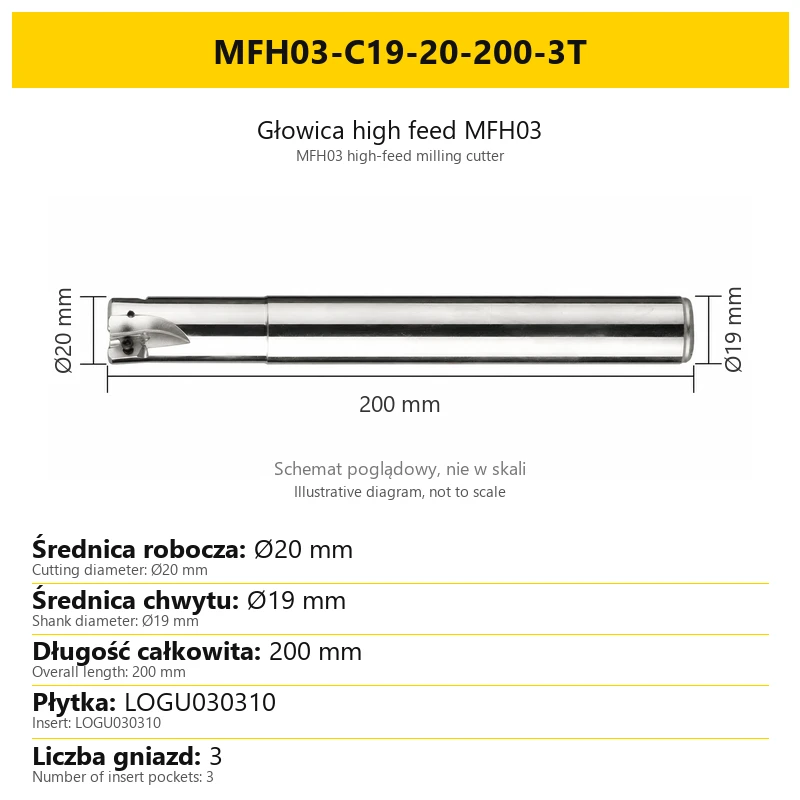
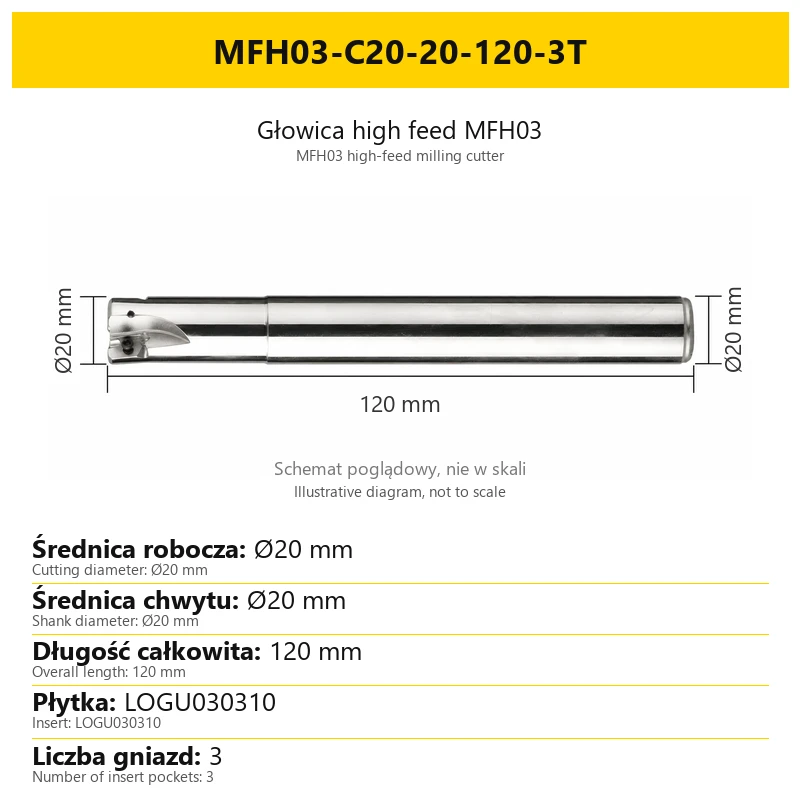
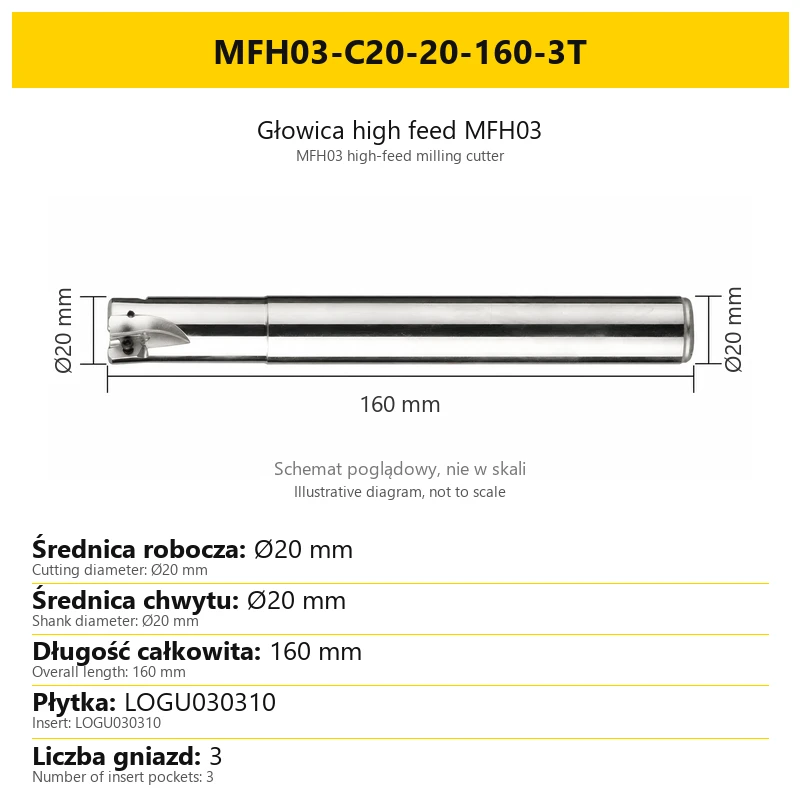
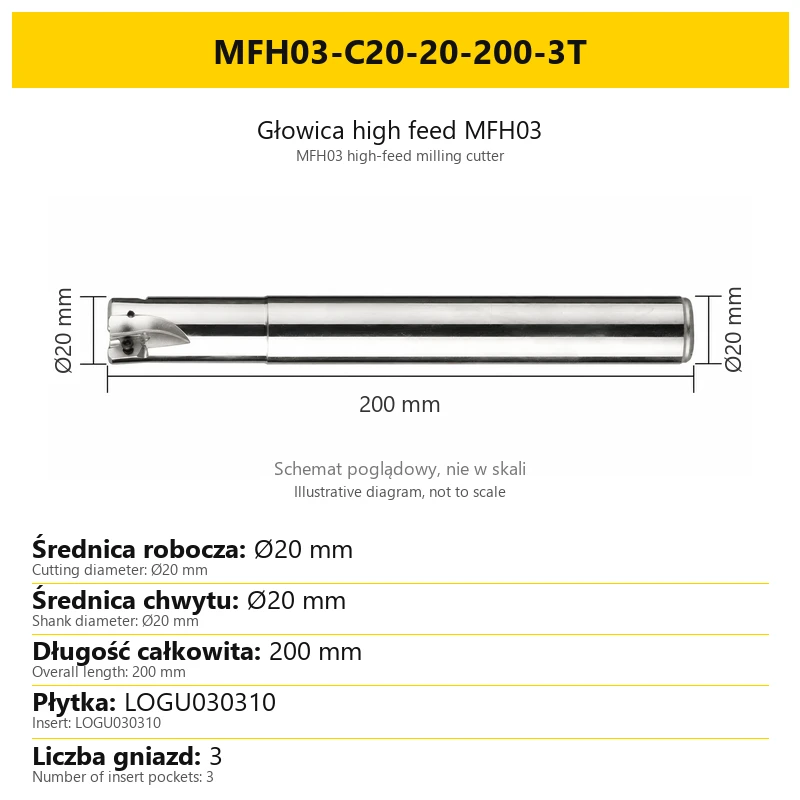
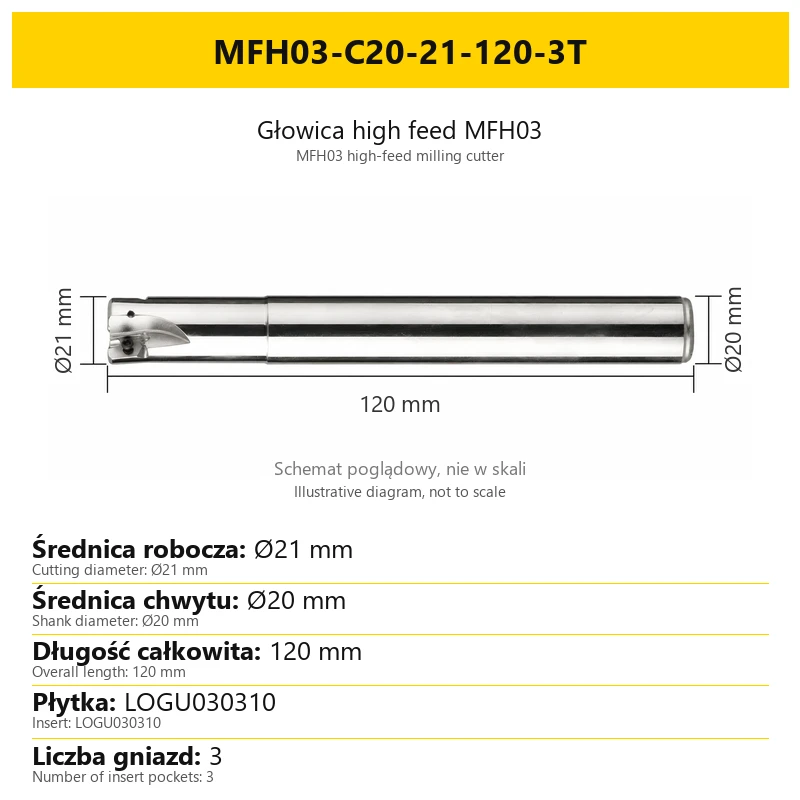
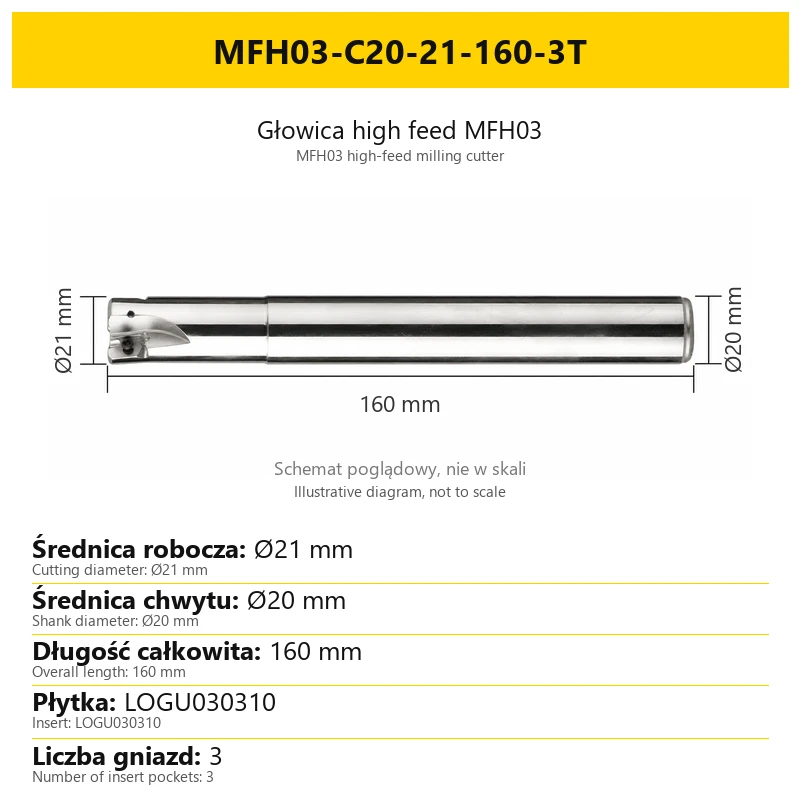
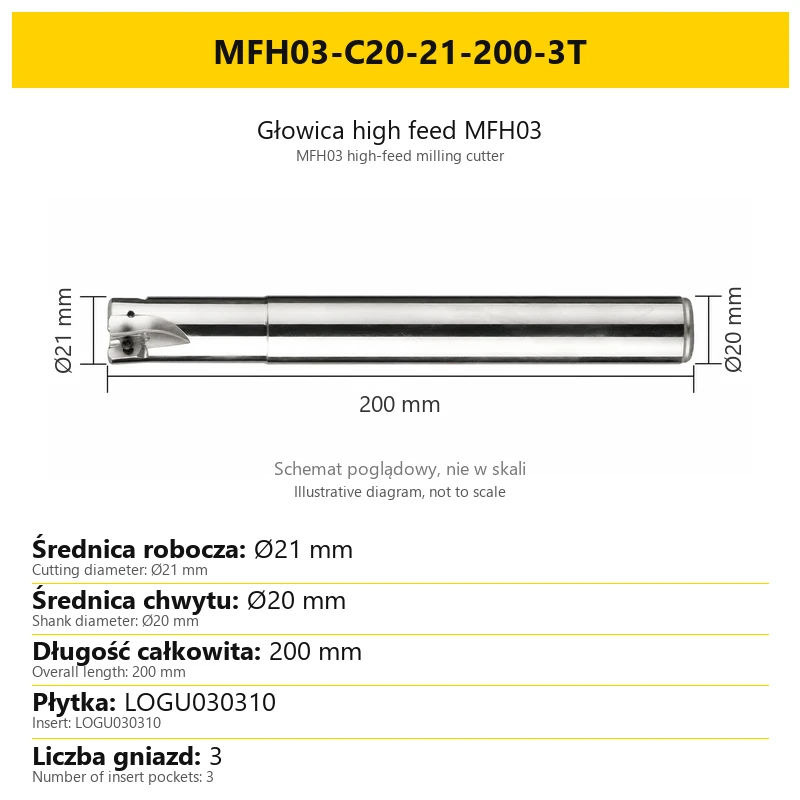
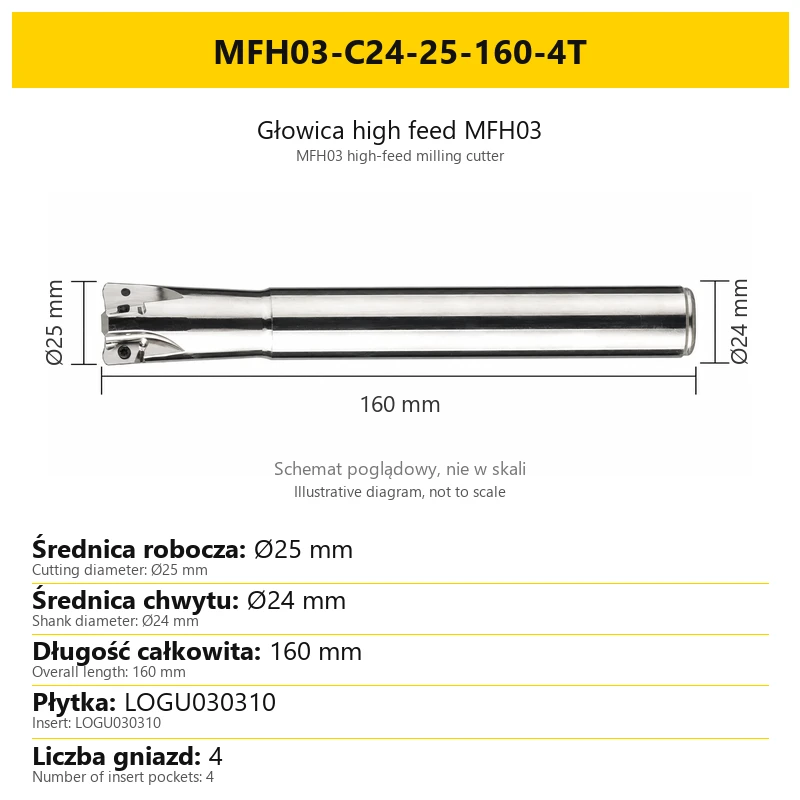
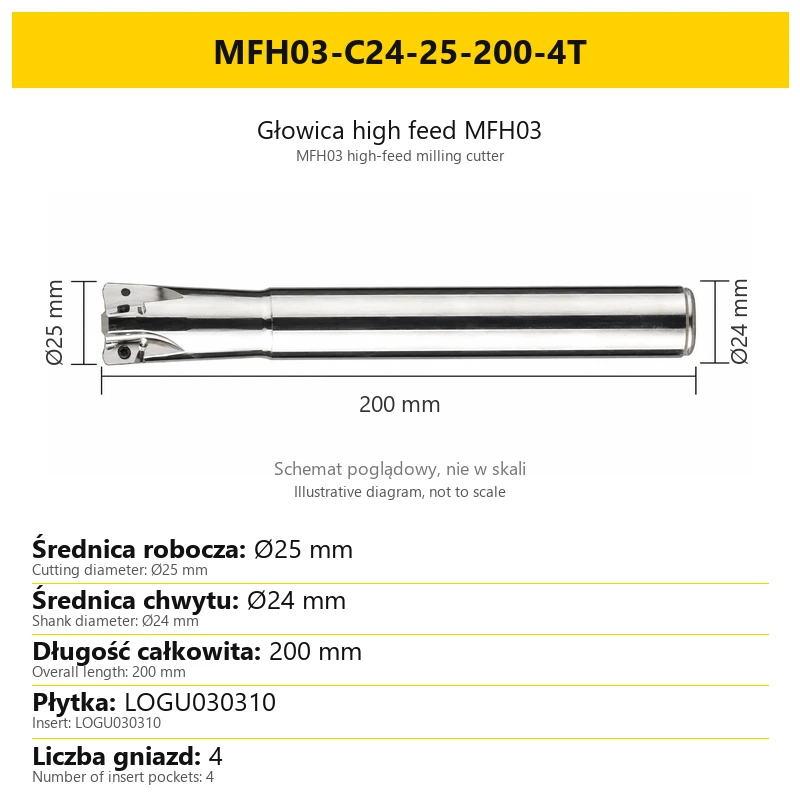
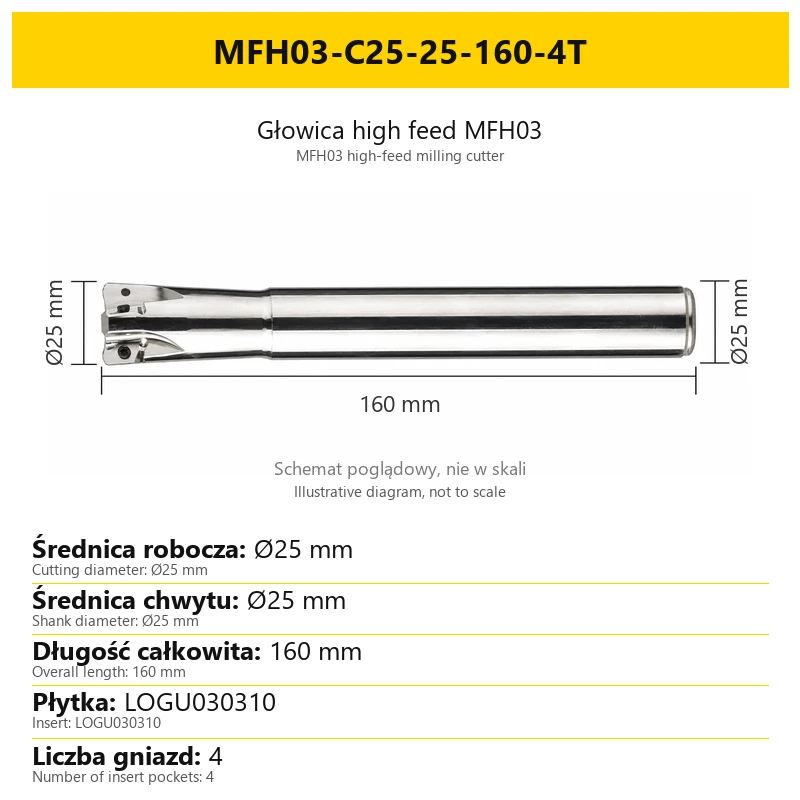
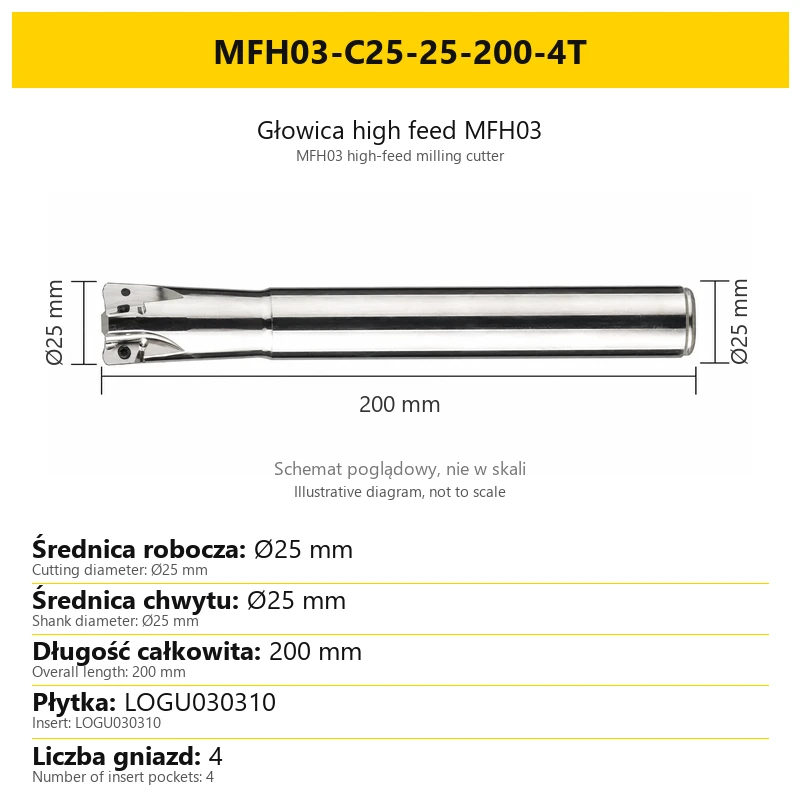
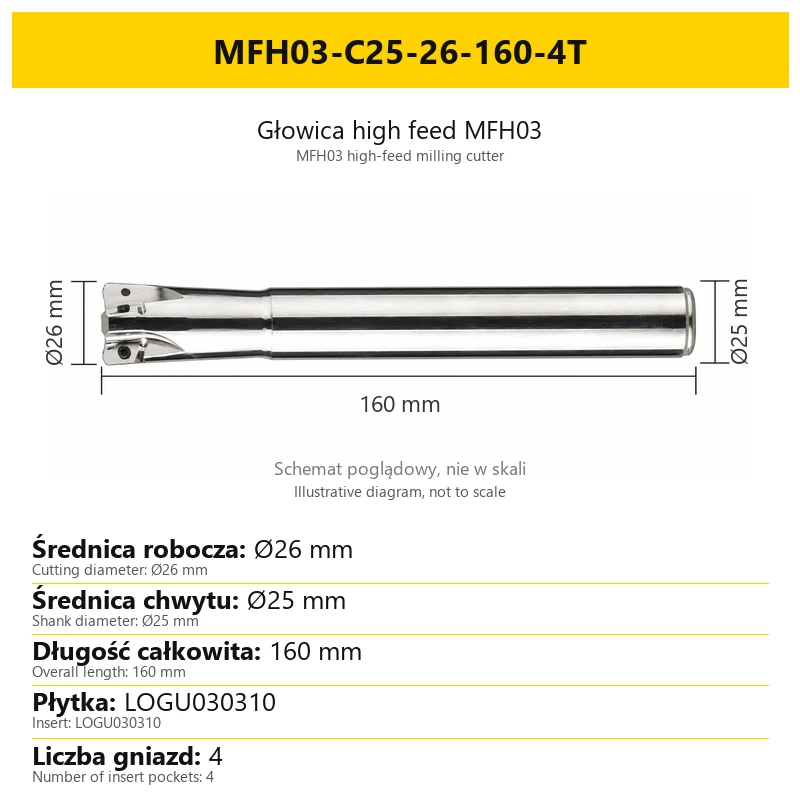
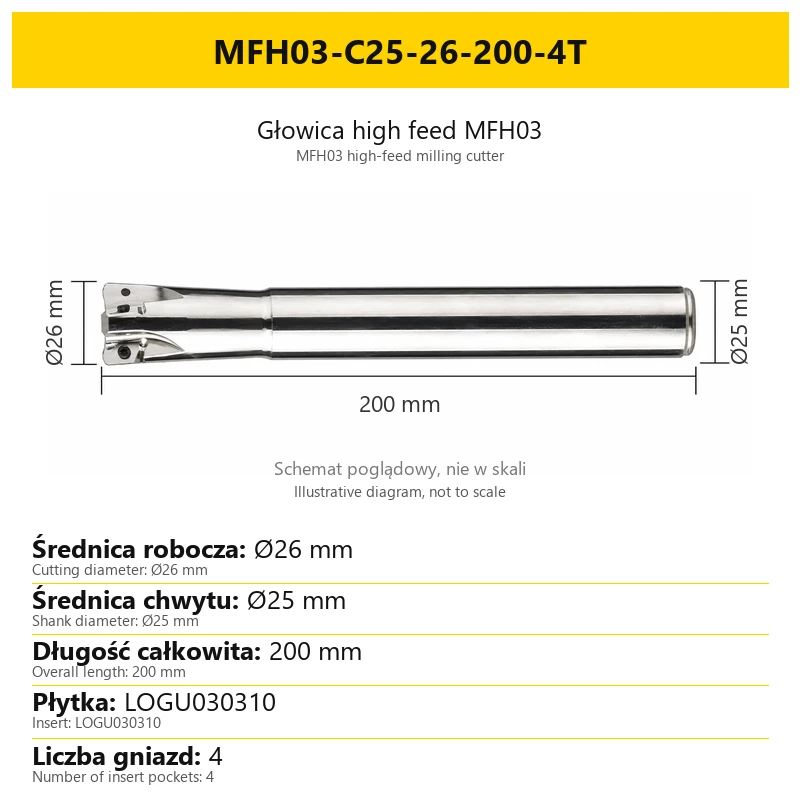
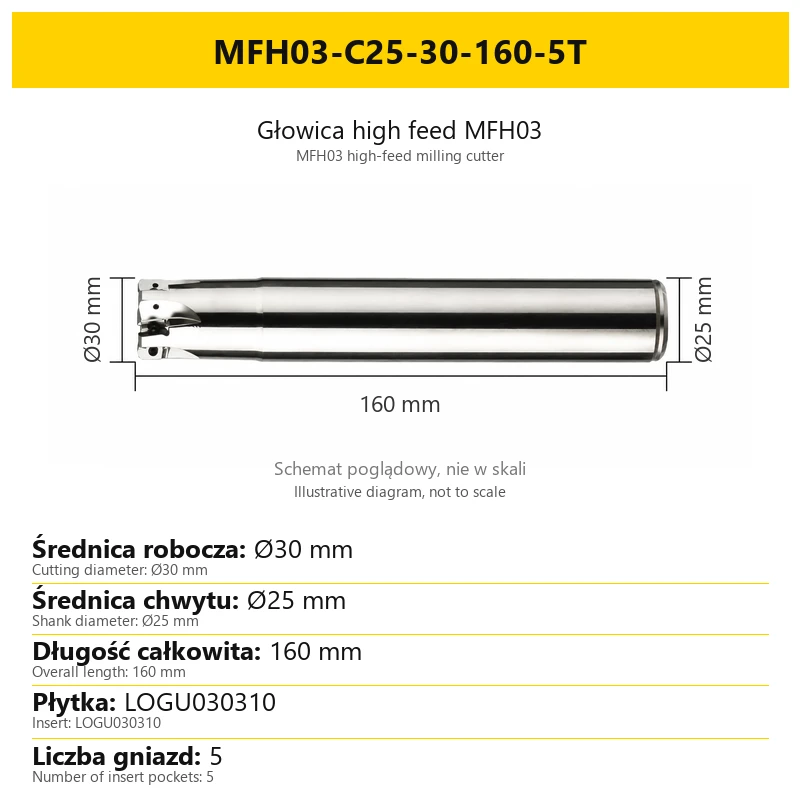
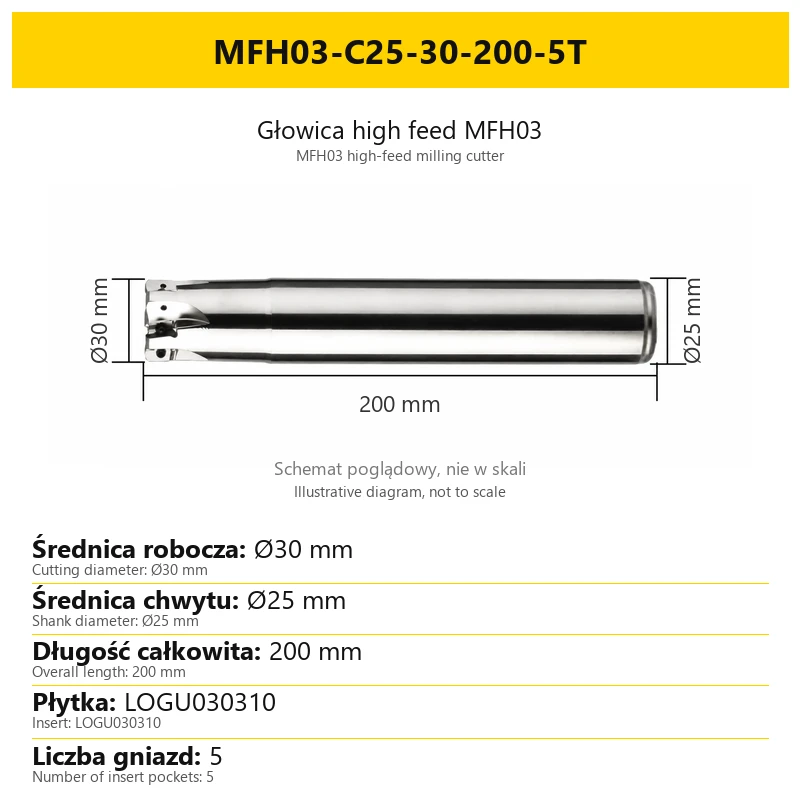
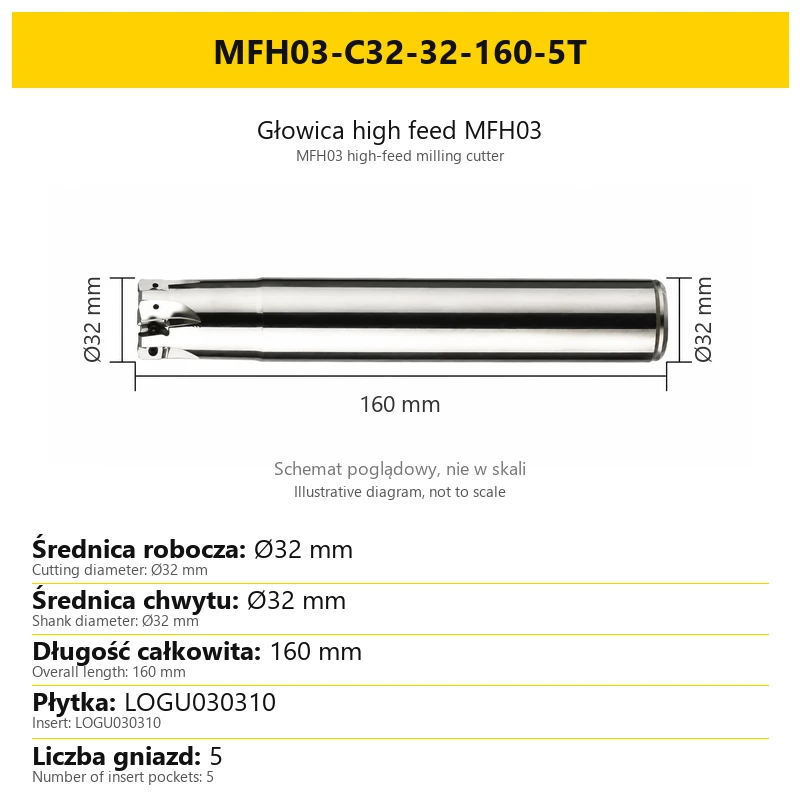
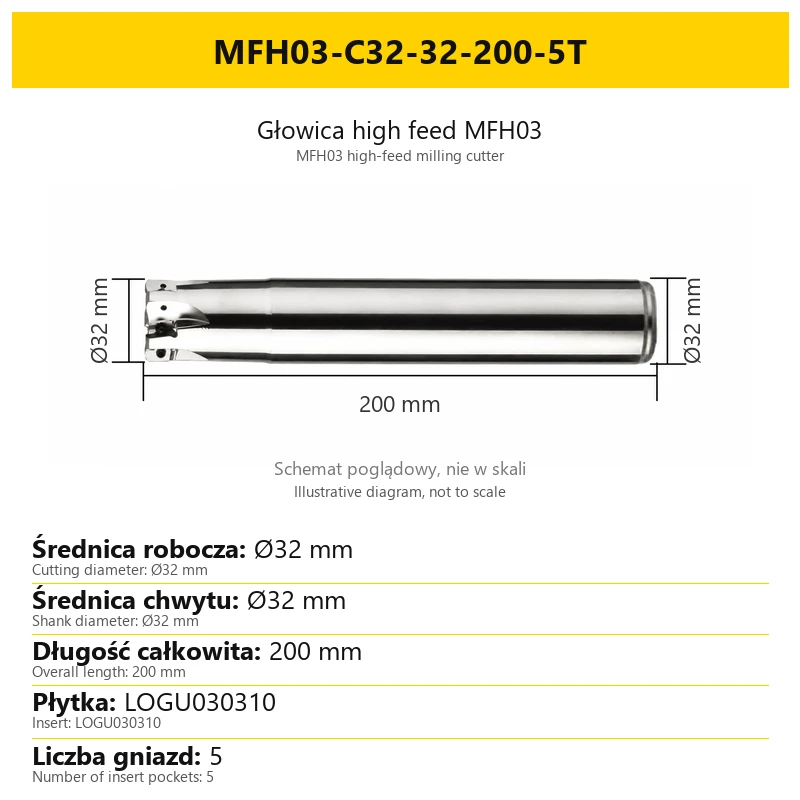
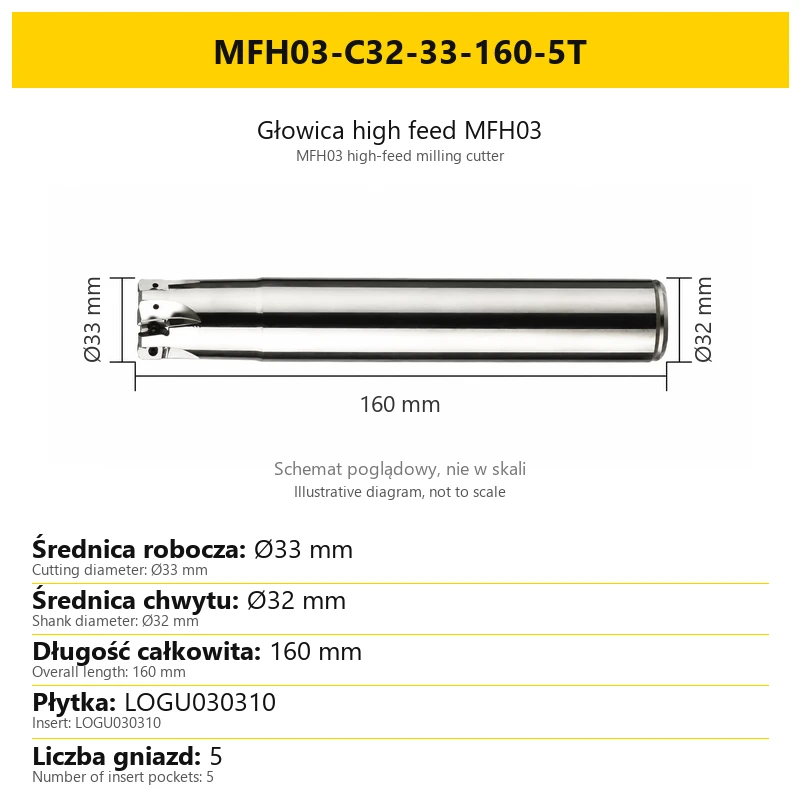
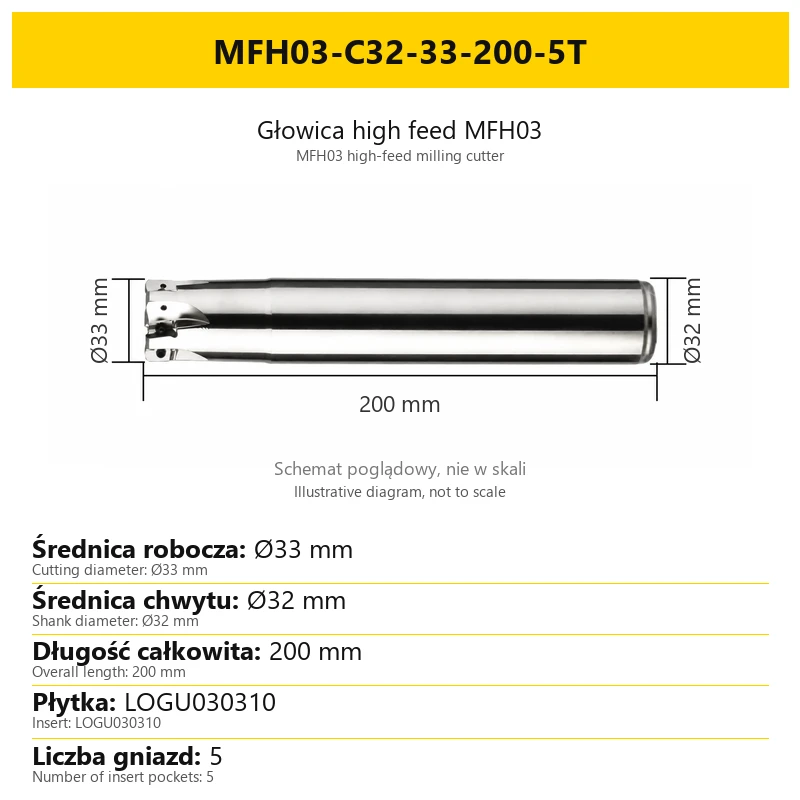
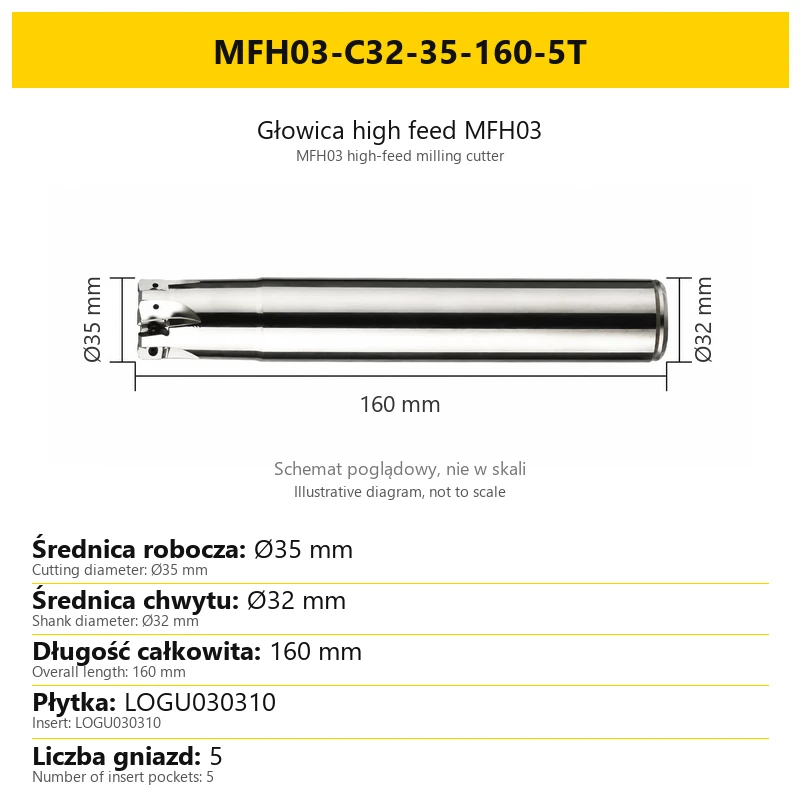
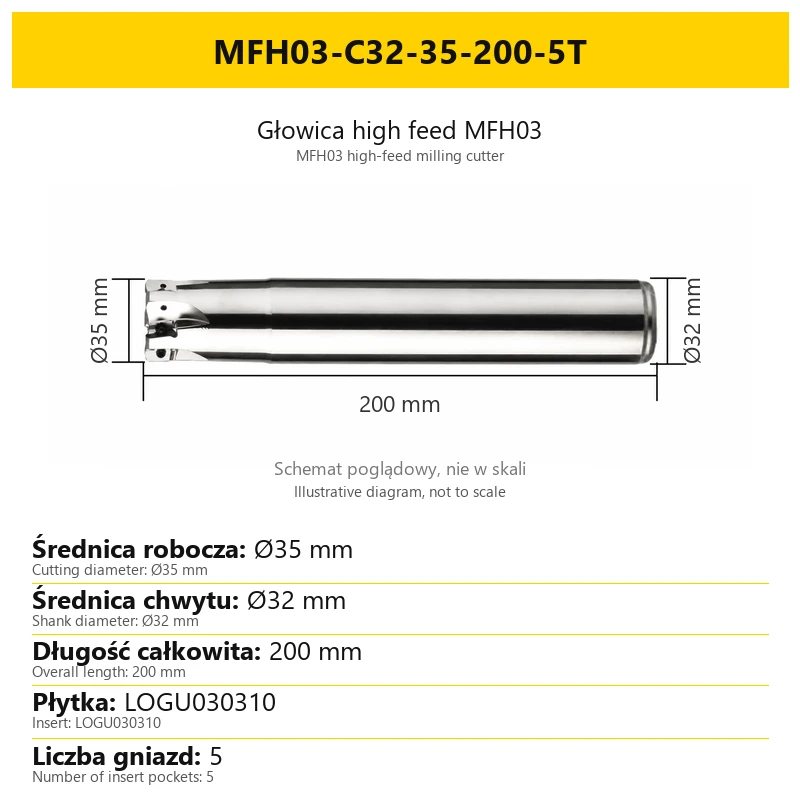


High Feed head MFH03 - for inserts LOGU030310 - cylindrical shank
Shipping costs are not included in the price.
Shipping costs are not included in the price.
Ask about the product
The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: 3115-54248
Product description
MFH03 high-feed cutter for LOGU030310 inserts
Cylindrical shank · 42CrMo body · high-feed roughing
MFH03 is an indexable milling cutter with a cylindrical shank, intended for high-feed roughing. The body uses LOGU030310 inserts. Select the required cutting diameter, shank diameter, overall length and number of insert pockets.
The family includes cutting diameters from Ø16 to Ø35 mm and overall lengths of 120, 160 and 200 mm. The exact dimensions of each version are stated in its designation and on its variant card. The body is made from 42CrMo steel and the shank is hardened.
1. Construction and technical specifications
The tool has a cylindrical shank and a cutting head with pockets for replaceable inserts. Flutes in the cutting section provide space for chip evacuation. The number of pockets depends on the selected version and is identified by the 2T, 3T, 4T or 5T suffix.
| Parameter | Specification |
|---|---|
| Family | MFH03 indexable high-feed cutter |
| Insert system | LOGU030310 |
| Tool mounting | Cylindrical shank |
| Body material | 42CrMo |
| Shank construction | Hardened |
| Cutting diameter | Ø16–35 mm, depending on the variant |
| Shank diameter | Ø15–32 mm, depending on the variant |
| Overall length | 120, 160 or 200 mm |
| Number of insert pockets | 2, 3, 4 or 5, as stated in the variant designation |
The shank and cutting diameters may differ. Use the shank diameter when selecting a toolholder and the cutting diameter when planning the toolpath. These dimensions are not interchangeable.
2. Application and the high-feed principle
MFH03 is intended for rough milling at high feed rates. High-feed machining combines a high feed per tooth with a shallow axial depth of cut. Cutting conditions must be selected for the actual insert, workpiece material and rigidity of the setup.
The high-feed designation does not specify one spindle speed or feed rate for every tool size. A change in diameter, insert count or tool overhang requires the machining conditions to be checked again.
| Process element | Selection consideration |
|---|---|
| Roughing | Removal of machining allowance in successive passes |
| High feed rate | Selected together with depth of cut and insert geometry |
| Workpiece material | Determines the required LOGU030310 insert grade and geometry |
| Chip evacuation | Consider the head flutes and the space available in the workpiece |
3. Selecting the diameter, shank and length
First check the cutting diameter needed for the operation. Then select the shank to suit the toolholder and the length needed to reach the machining area. Use the shortest practical overhang that provides the required access without collision.
| Dimension | What it describes | What to check |
|---|---|---|
| Cutting diameter | Size of the cutting section | Access to the machining area and the toolpath |
| Shank diameter | Size of the section held in the toolholder | Compatibility with the holder or collet clamping range |
| Overall length | Length from the cutting head to the end of the shank | Required reach and the length clamped inside the holder |
| Pocket count | Number of inserts working in the tool | Consistency with the designation and feed calculation |
Overall length is not the same as tool overhang. Part of the shank remains clamped in the toolholder. Check access for the complete assembly: cutting head, shank, toolholder and workpiece fixture.
The tool diagrams are illustrative. Do not measure dimensions from the image proportions; use the dimensions stated for the selected variant.
4. Reading the MFH03 designation
The size code states the family, shank diameter, cutting diameter, overall length and pocket count, in that order. The letter C relates to the shank. The final number followed by T identifies the number of cutting positions.
| Designation element | Meaning |
|---|---|
| MFH03 | Cutter family and tool system |
| C + number | Shank diameter in millimetres |
| Next number | Cutting diameter in millimetres |
| Following number | Overall length in millimetres |
| 2T / 3T / 4T / 5T | Number of insert pockets in the body |
5. LOGU030310 inserts and pocket count
Select the cutter for the LOGU030310 insert system. Before installation, check the complete insert designation, geometry and fit in the pocket. A similar external shape does not establish compatibility of another insert.
The 2T–5T designation refers to the cutting positions in the body, not the number of usable edges on a single insert. Use a consistent set of inserts when selecting or replacing them.
| Item to check | Selection rule |
|---|---|
| Insert designation | LOGU030310 system suited to the cutter pocket |
| Grade and geometry | Matched to the workpiece material and operation |
| Body population | Consistent with the pocket count in the variant code |
| Pocket and fastening | Clean seating surfaces and correctly seated inserts |
6. Mounting and preparation
- Check the selected shank diameter and choose a suitable toolholder or collet.
- Clean the shank, pockets and insert seating surfaces before assembly.
- Clamp the tool over the length required by the toolholder. Keep overhang as short as practical while retaining the required access.
- Check insert seating, fastening condition and consistency of the insert designations.
- Verify the toolpath for the complete assembly, including the toolholder and workpiece fixture.
A longer body allows the reach to be selected for the task, but the rigidity of the complete setup must be considered. Conditions suitable for a short setup are not automatically suitable for a longer overhang.
7. Selecting cutting conditions
Select cutting speed, feed and depth of cut for the installed LOGU030310 insert, workpiece material, cutting diameter and mounting conditions. Values for another insert grade or cutter are not ready-to-use settings for this version.
Use the correct number of cutting positions when calculating table feed. Changing from 2T to 3T, 4T or 5T changes the relationship between feed per tooth and feed per minute.
During initial machining, observe load, chip evacuation and cutting stability. Adjust conditions for the actual tool assembly and workpiece material instead of using one setting for the whole family.
8. Frequently asked questions
Is the shank diameter always equal to the cutting diameter?
No. The family includes versions with different shank and cutting diameters. The first number after C identifies the shank diameter; the next identifies the cutting diameter.
What does 3T or 5T mean?
It means three or five insert pockets in the body. It does not specify the number of spare inserts or the number of edges on one insert.
Does an overall length of 200 mm provide 200 mm of working reach?
No. This is the overall tool length. Actual reach also depends on the shank length clamped inside the holder and access to the workpiece.
Which inserts fit MFH03?
The cutter is intended for the LOGU030310 system. Select the complete insert designation, grade and geometry to suit the pocket and workpiece material.
How do I choose the correct variant?
Check the cutting diameter, shank diameter, required length and pocket count. Select the full code corresponding to that combination of dimensions.
Related products
-
A083-43185
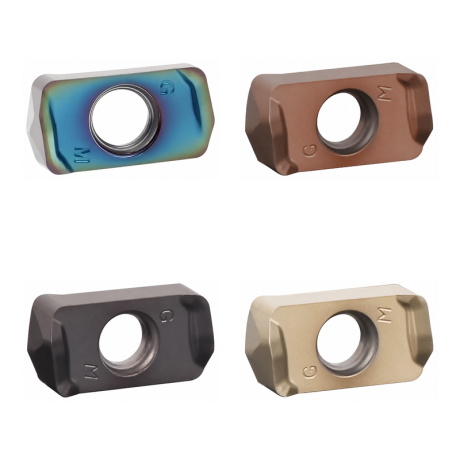
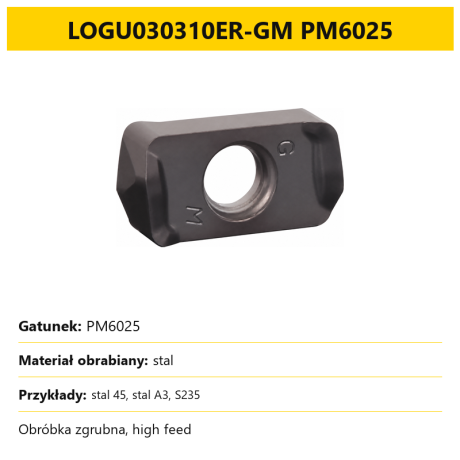 Milling Inserts 0.00
LOGU030310 ER carbide indexable inserts (10 pcs.)


Bestsellers
-
Bestseller
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.77Price €56.72without VAT -
Bestseller
Kortools Adhesive + Tape CNC Workholding Kit
Yellow tape 5cm x 50m; adhesive 100g Yellow tape 5cm x 50m; adhesive 500g Yellow tape 10cm x 50m; adhesive 100g Yellow tape 10cm x 50m; adhesive 500g Green tape 5cm x 50m; adhesive 100g + 7 morePrice €44.61Price €36.27without VAT -
Price €17.16Price €13.95without VAT
-
Price €7.09Price €5.77without VAT
-
Price €7.55Price €6.14without VAT
-
Bestseller
 Other Accessories 0.00
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.76Price €43.70without VAT -
Bestseller
 Ball Nose End Mills 0.00
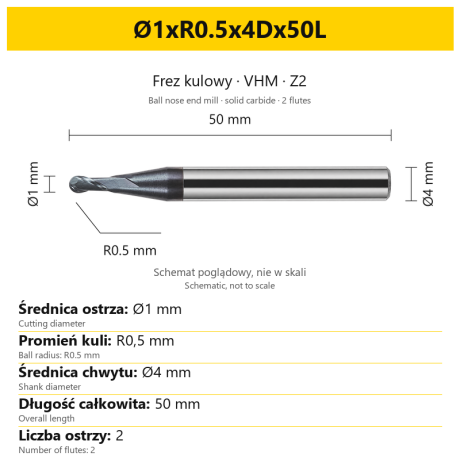
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.13Price €8.23without VAT -
Bestseller
 2-Flute End Mills 0.00
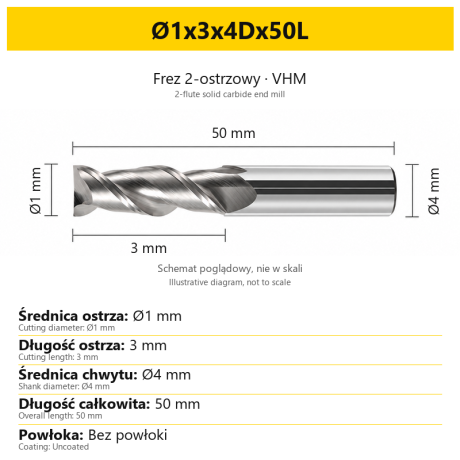
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.35Price €4.35without VAT -
Bestseller
 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.40Price €3.58without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.88Price €6.40without VAT -
Bestseller
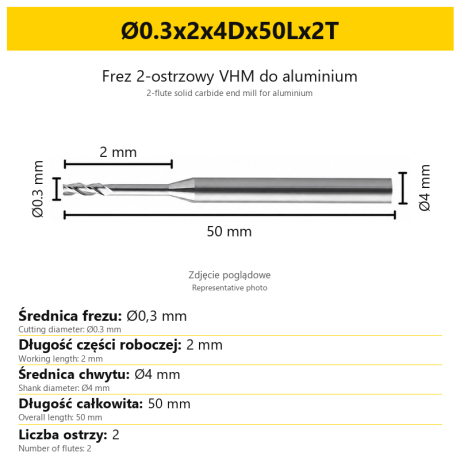 2-Flute End Mills 0.00
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.98Price €6.49without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.27Price €5.91without VAT -
Bestseller
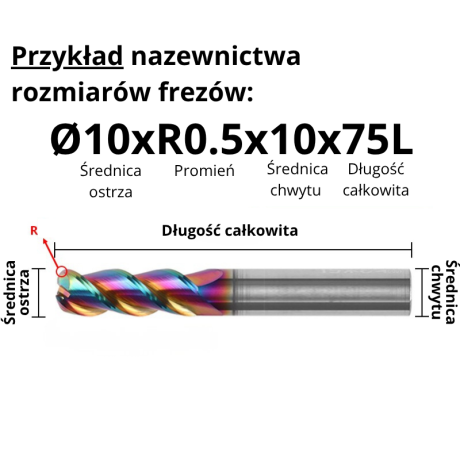
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €4.96Price €4.03without VAT -
Bestseller
 3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.09Price €4.14without VAT -
Bestseller

 Countersinks 0.00
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.80Price €3.91without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.07Price €4.12without VAT