Spiral Flute Machine Tap HSSE DIN 371/376 - TiCN
Shipping costs are not included in the price.
Shipping costs are not included in the price.

Weekly deals
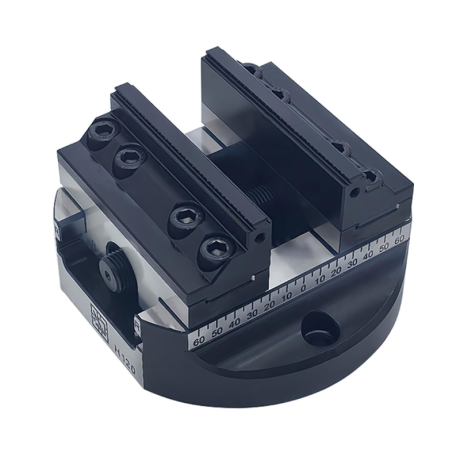
5-axis vise with hard jaws
Self-centering machine vise. Hard jaws included.
excl. VAT
Regular price:
Lowest price in the 30 days before the reduction:
Time left
Offer ends 06.11.2026 23:59. Offer applies to the vise + hard jaws bundle only.
Ask about the product

The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: 76F5-98119
Product description
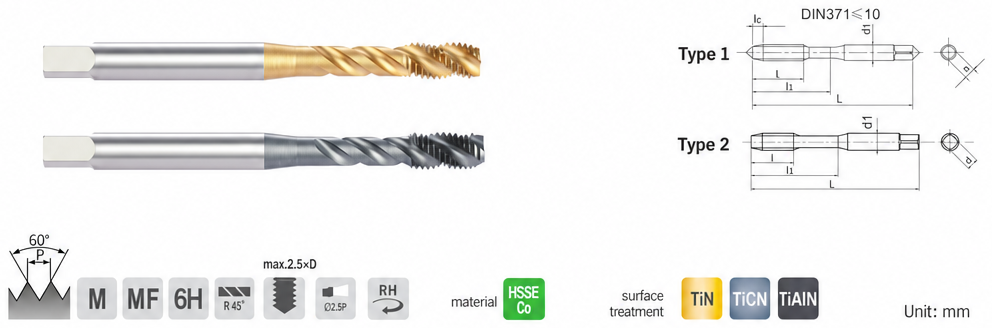
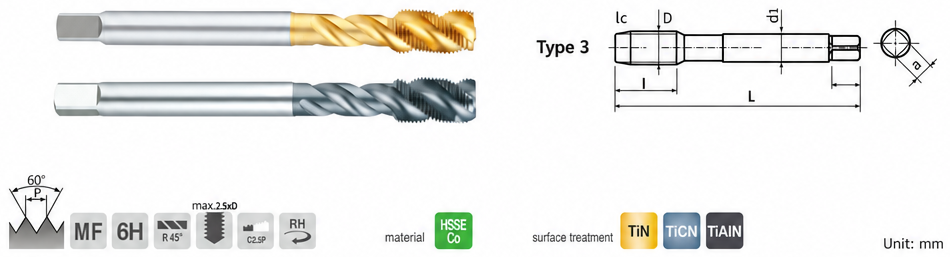
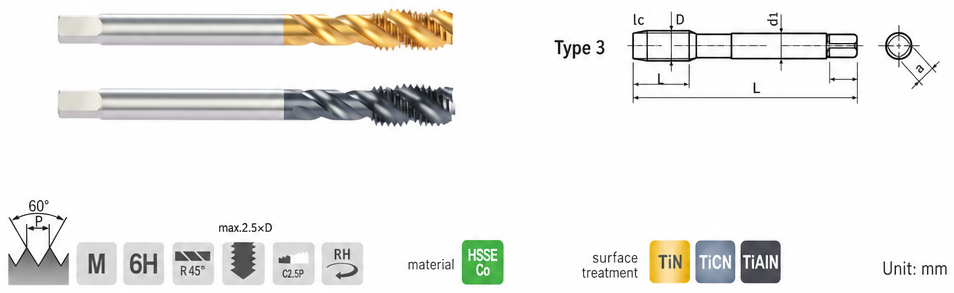
Spiral-flute machine tap made to DIN 371 / 374 / 376 (DIN 371 for M threads ≤ 10 mm, DIN 376 for M ≥ 12 mm, DIN 374 for fine threads). Intended for cutting internal metric M and metric fine MF. Spiral flutes with a helix angle of 45° (R45) carry chips back towards the shank and out of the hole, for use in blind holes. Made from HSSE (HSS-E, cobalt-alloyed high-speed steel) with a TiCN coating.
Applications
- Cutting metric M threads in blind holes
- Tapping materials that produce long chips, including ductile steel, stainless steel and aluminium
- Machining components where chips must be removed towards the hole opening
- Threads close to the bottom of a hole
The spiral flutes carry chips towards the hole opening. The tap is intended for blind holes and materials that produce long, continuous chips.
Specification
| Parameter | Value |
|---|---|
| Thread type | M (metric) and MF (metric fine) |
| Standard | DIN 371 / 374 / 376 |
| Flute geometry | Spiral flute, helix angle 45° (R45) |
| Cutting direction | Right-hand (RH) |
| Thread tolerance class | 6H |
| Material | HSSE (HSS-E, cobalt-alloyed high-speed steel) |
| Coating | TiCN (titanium carbonitride, grey-blue colour) |
| Size selection | Select the exact size from the product options. The table below gives reference dimensions for standard and metric fine MF threads. |
Reference sizes and dimensions
| Size | Standard | Pitch P (mm) | Class | Overall length L (mm) | Thread length l (mm) | Neck l₁ (mm) | Lead lᴄ | Shank d₁ (mm) | Square a (mm) | Flutes | Tap drill diameter (mm) |
|---|---|---|---|---|---|---|---|---|---|---|---|
| M2×0,4 | DIN 371 | 0,4 | 6H | 45 | 6 | 13 | 2,5×P | 2,8 | 2,1 | 3 | 1,6 |
| M2,5×0,45 | DIN 371 | 0,45 | 6H | 50 | 6 | 15 | 2,5×P | 2,8 | 2,1 | 3 | 2,1 |
| M3×0,5 | DIN 371 | 0,5 | 6H | 56 | 6 | 18 | 2,5×P | 3,5 | 2,7 | 3 | 2,5 |
| M4×0,7 | DIN 371 | 0,7 | 6H | 63 | 9 | 21 | 2,5×P | 4,5 | 3,4 | 3 | 3,3 |
| M5×0,8 | DIN 371 | 0,8 | 6H | 70 | 10 | 25 | 2,5×P | 6 | 4,9 | 3 | 4,2 |
| M6×1 | DIN 371 | 1 | 6H | 80 | 12 | 30 | 2,5×P | 6 | 4,9 | 3 | 5 |
| M8×1,25 | DIN 371 | 1,25 | 6H | 90 | 15 | 35 | 2,5×P | 8 | 6,2 | 3 | 6,8 |
| MF8×1 | DIN 371 | 1 | 6H | 90 | 15 | 35 | 2,5×P | 8 | 6,2 | 3 | 7 |
| M10×1,5 | DIN 371 | 1,5 | 6H | 100 | 18 | 39 | 2,5×P | 10 | 8 | 3 | 8,5 |
| MF10×1 | DIN 371 | 1 | 6H | 90 | 15 | 35 | 2,5×P | 10 | 8 | 3 | 9 |
| MF10×1,25 | DIN 371 | 1,25 | 6H | 100 | 18 | 39 | 2,5×P | 10 | 8 | 3 | 8,8 |
| M4×0,7 | DIN 376 | 0,7 | 6H | 63 | 9 | — | 2,5×P | 2,8 | 2,1 | 3 | 3,3 |
| M5×0,8 | DIN 376 | 0,8 | 6H | 70 | 10 | — | 2,5×P | 3,5 | 2,7 | 3 | 4,2 |
| M6×1 | DIN 376 | 1 | 6H | 80 | 12 | — | 2,5×P | 4,5 | 3,4 | 3 | 5 |
| M8×1,25 | DIN 376 | 1,25 | 6H | 90 | 15 | — | 2,5×P | 6 | 4,9 | 3 | 6,8 |
| M10×1,5 | DIN 376 | 1,5 | 6H | 100 | 18 | — | 2,5×P | 7 | 5,5 | 3 | 8,5 |
| M12×1,75 | DIN 376 | 1,75 | 6H | 110 | 21 | — | 2,5×P | 9 | 7 | 3 | 10,3 |
| M14×2 | DIN 376 | 2 | 6H | 110 | 20 | — | 2,5×P | 11 | 9 | 3 | 12 |
| M16×2 | DIN 376 | 2 | 6H | 110 | 20 | — | 2,5×P | 12 | 9 | 3 | 14 |
| M18×2,5 | DIN 376 | 2,5 | 6H | 125 | 25 | — | 2,5×P | 14 | 11 | 3 | 15,5 |
| M20×2,5 | DIN 376 | 2,5 | 6H | 140 | 25 | — | 2,5×P | 16 | 12 | 4 | 17,5 |
| M22×2,5 | DIN 376 | 2,5 | 6H | 140 | 25 | — | 2,5×P | 18 | 14,5 | 4 | 19,5 |
| M24×3 | DIN 376 | 3 | 6H | 160 | 30 | — | 2,5×P | 18 | 14,5 | 4 | 21 |
| M27×3 | DIN 376 | 3 | 6H | 160 | 45 | — | 2,5×P | 20 | 16 | 4 | 24 |
| M30×3,5 | DIN 376 | 3,5 | 6H | 180 | 35 | — | 2,5×P | 22 | 18 | 4 | 26,5 |
| M33×3,5 | DIN 376 | 3,5 | 6H | 180 | 35 | — | 2,5×P | 25 | 20 | 4 | 29,5 |
| M36×4 | DIN 376 | 4 | 6H | 200 | 40 | — | 2,5×P | 28 | 22 | 4 | 32 |
| MF6×0,5 | DIN 374 | 0,5 | 6H | 80 | 14 | — | 2,5×P | 4,5 | 3,4 | 3 | 5,5 |
| MF6×0,75 | DIN 374 | 0,75 | 6H | 80 | 14 | — | 2,5×P | 4,5 | 3,4 | 3 | 5,3 |
| MF8×0,75 | DIN 374 | 0,75 | 6H | 80 | 18 | — | 2,5×P | 6 | 4,9 | 3 | 7,3 |
| MF12×1 | DIN 374 | 1 | 6H | 100 | 15 | — | 2,5×P | 9 | 7 | 3 | 11 |
| MF12×1,25 | DIN 374 | 1,25 | 6H | 100 | 21 | — | 2,5×P | 9 | 7 | 3 | 10,8 |
| MF12×1,5 | DIN 374 | 1,5 | 6H | 100 | 21 | — | 2,5×P | 9 | 7 | 3 | 10,5 |
| MF14×1,5 | DIN 374 | 1,5 | 6H | 100 | 20 | — | 2,5×P | 11 | 9 | 3 | 12,5 |
| MF16×1,5 | DIN 374 | 1,5 | 6H | 100 | 20 | — | 2,5×P | 12 | 9 | 3 | 14,5 |
| MF18×1,5 | DIN 374 | 1,5 | 6H | 110 | 25 | — | 2,5×P | 14 | 11 | 3 | 16,5 |
| MF20×1,5 | DIN 374 | 1,5 | 6H | 125 | 25 | — | 2,5×P | 16 | 12 | 4 | 18,5 |
| MF22×1,5 | DIN 374 | 1,5 | 6H | 125 | 25 | — | 2,5×P | 18 | 14,5 | 4 | 20,5 |
| MF24×1,5 | DIN 374 | 1,5 | 6H | 140 | 28 | — | 2,5×P | 18 | 14,5 | 4 | 22,5 |
Dimensions (mm). DIN 371 = reinforced shank (M≤10), DIN 376 = reduced shank (M≥12, coarse pitch), DIN 374 = reduced shank for metric fine threads (MF). The neck length l₁ is not standardised for reduced shanks (—). Lead lᴄ (cutting taper) = 2,5×P (spiral flute R45°). Tap drill diameter = recommended drill diameter before tapping.
Selecting a coating for the workpiece material
| Coating | Application |
|---|---|
| TiN (gold) | General-purpose coating; structural, carbon and alloy steels up to approximately 900 MPa, cast iron and non-ferrous metals. |
| TiCN (grey-blue) | Harder and more abrasion-resistant than TiN; higher-strength steel, stainless steel, hardened steel up to approximately 45 HRC and ductile materials. |
| TiAlN (anthracite) | Dry machining or MQL; hard and difficult-to-machine materials, stainless steel, titanium, Inconel and cast iron. |
This product has a TiCN coating: harder and more abrasion-resistant than TiN; for higher-strength steel, stainless steel, hardened steel up to approximately 45 HRC and ductile materials.
What is the lead?
The lead is the tapered cutting section at the front of the tap. The initial thread cutting is distributed over its first few threads. A longer lead makes entry into the material easier, but the full thread ends farther from the bottom of a blind hole. Type C/E lead (cutting taper), approximately 2-3,5 threads, for tapping close to the bottom of a hole. A shorter lead allows the thread to be cut close to the bottom of a blind hole.
FAQ
Through holes or blind holes?
A spiral-flute tap carries chips towards the hole opening and is intended for blind holes.
Which coating should I choose?
TiN for general applications, TiCN for higher-strength and stainless steels, TiAlN for hard materials and dry machining.
How does HSSE differ from ordinary HSS?
HSSE (HSS-E) contains cobalt to increase hot hardness and cutting-edge durability compared with ordinary HSS.
Coolant?
Emulsion or tapping oil is recommended.
Related products
-
GWS-TICN-DIN374
 Spiral Flute Taps 0.00
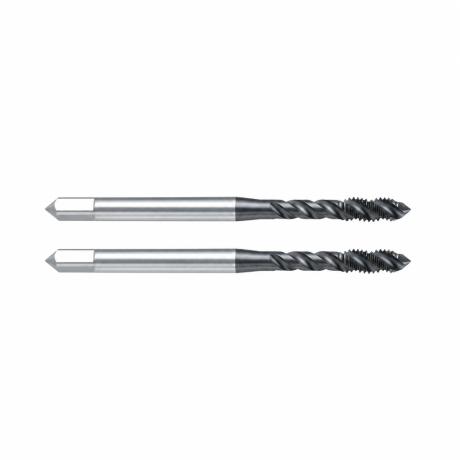
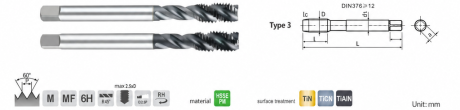
Spiral Flute Fine Pitch Machine Tap HSSE-PM DIN 374 TiCN
DIN374 M12x1,5 TiCN DIN374 M12x1,25 TiCN DIN374 M12x1 TiCN DIN374 M14x1,5 TiCN DIN374 M16x1,5 TiCN + 4 morePrice €37.38Price €30.39without VATShipping costs are not included in the price.


Bestsellers
-
Bestseller
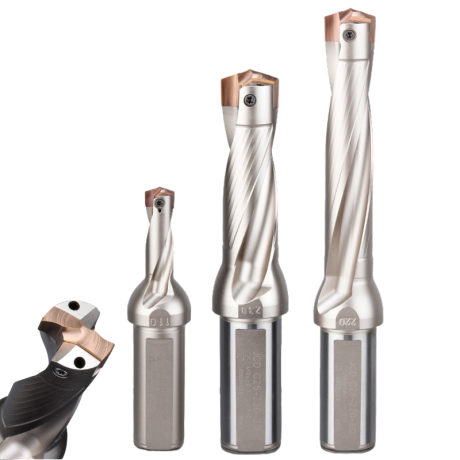
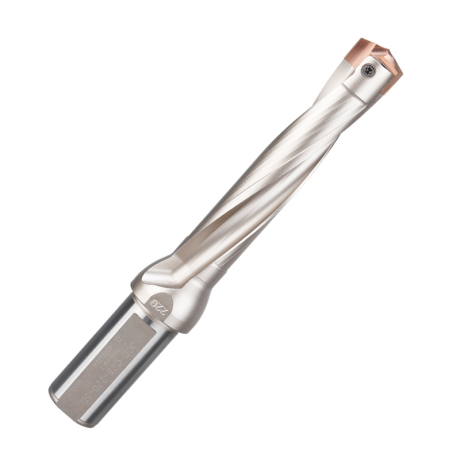
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.52Price €56.52without VAT -
Price €17.09Price €13.90without VAT
-
Price €7.07Price €5.74without VAT
-
Price €7.52Price €6.12without VAT
-
Bestseller
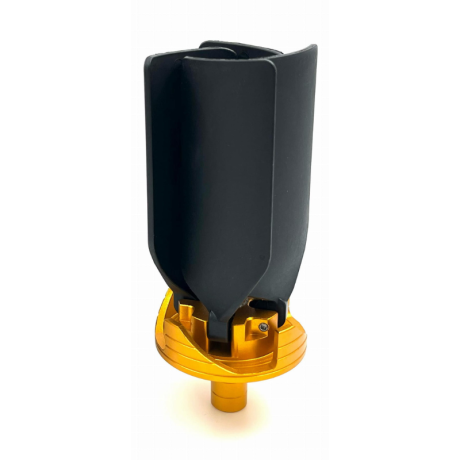
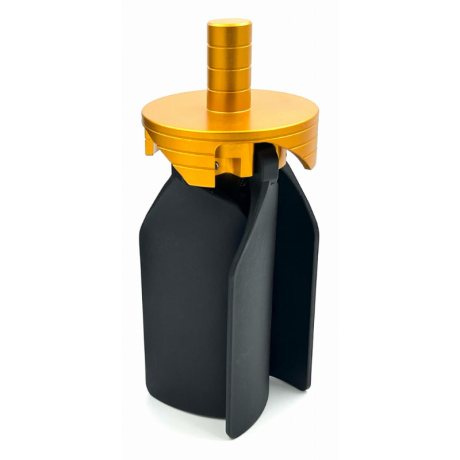 Other Accessories 0.00
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.56Price €43.55without VAT -
Bestseller
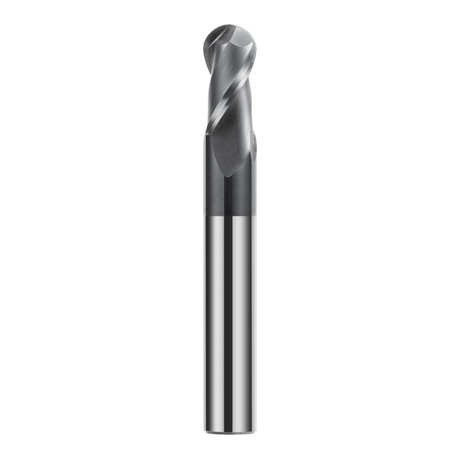
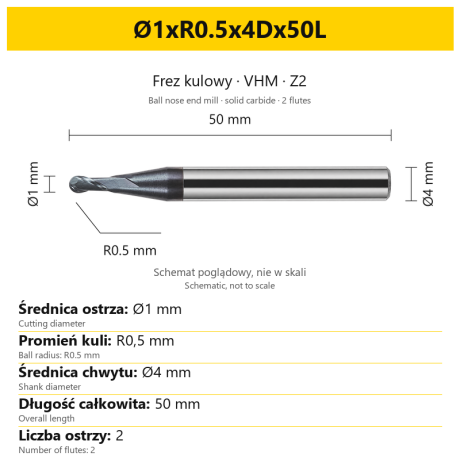 Ball Nose End Mills 0.00
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.09Price €8.21without VAT -
Bestseller
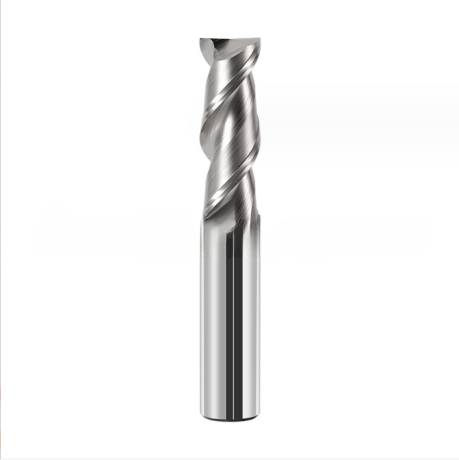
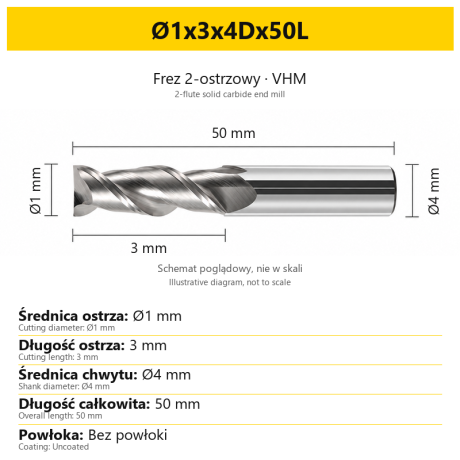 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.33Price €4.33without VAT -
Bestseller
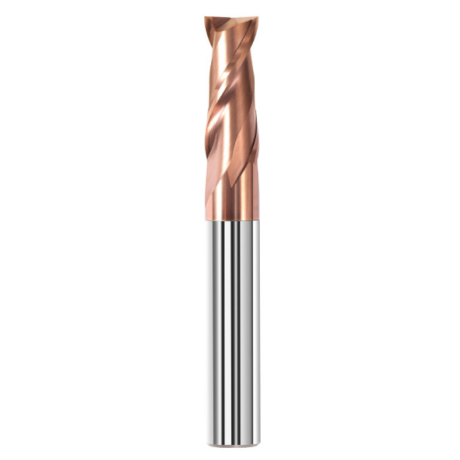
 2-Flute End Mills 0.00
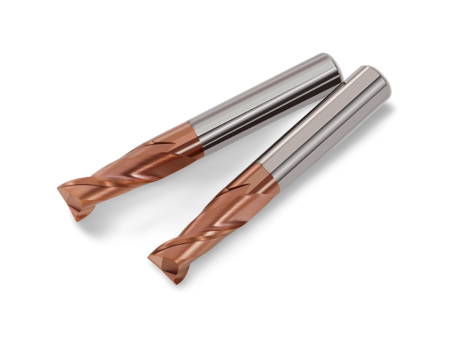
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.38Price €3.56without VAT -
Bestseller
 Ball Nose End Mills 0.00
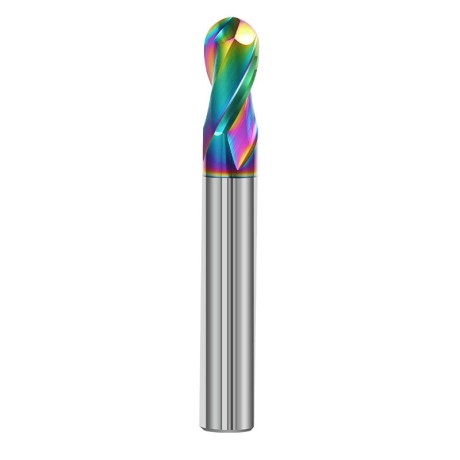
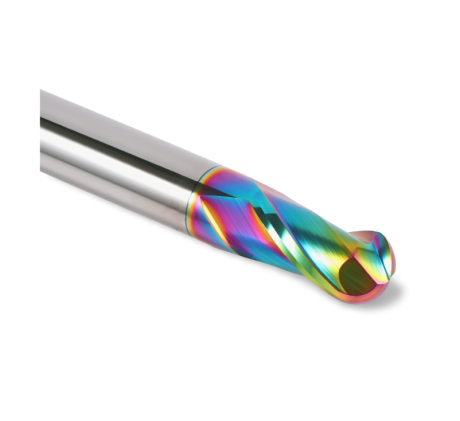
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.85Price €6.38without VAT -
Bestseller
 2-Flute End Mills 0.00
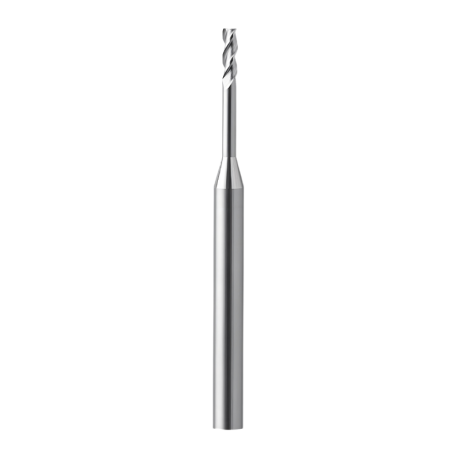
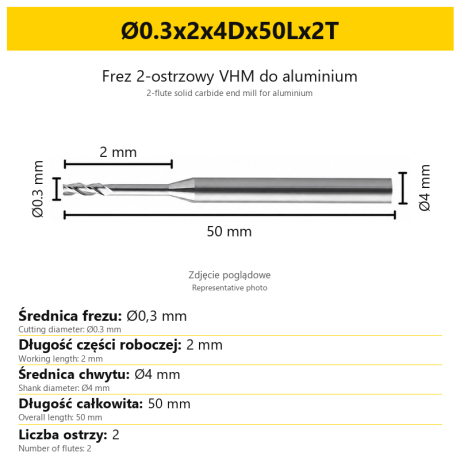
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.95Price €6.47without VAT -
Bestseller
 Ball Nose End Mills 0.00
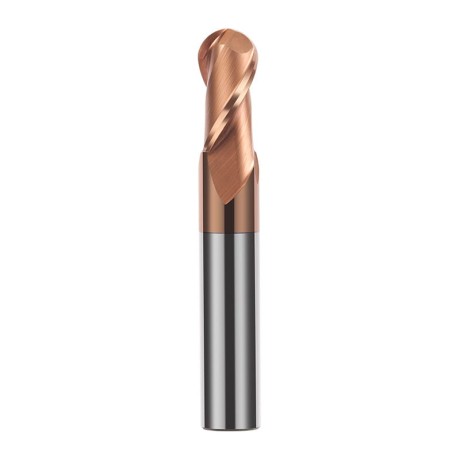
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.24Price €5.89without VAT -
Bestseller
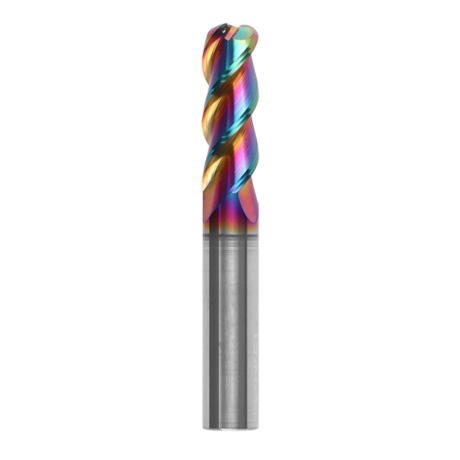
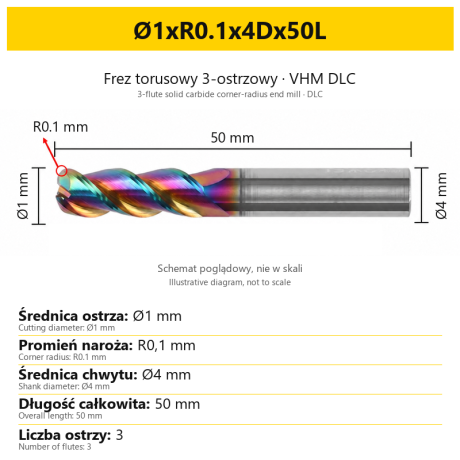
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €5.89Price €4.79without VAT -
Bestseller
 3-Flute End Mills 0.00
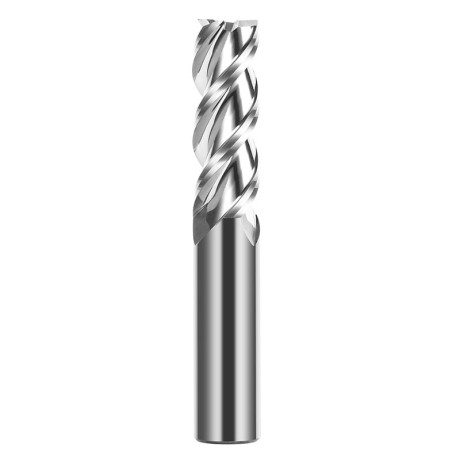
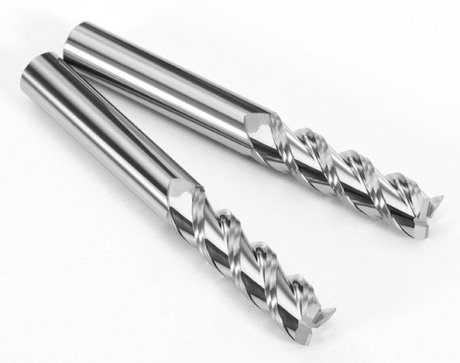
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.08Price €4.13without VAT -
Bestseller
 Countersinks 0.00
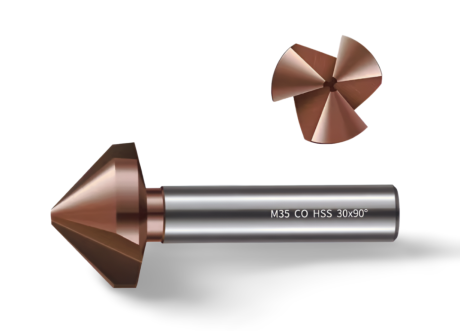
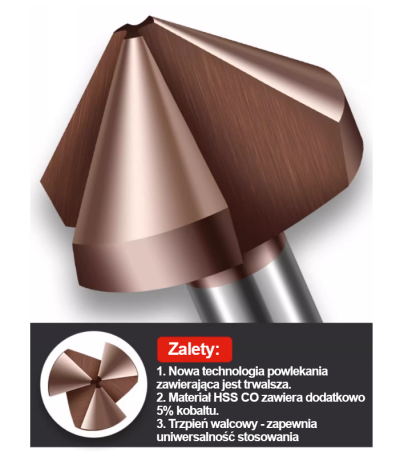
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.79Price €3.89without VAT -
Bestseller
 3-Flute End Mills 0.00
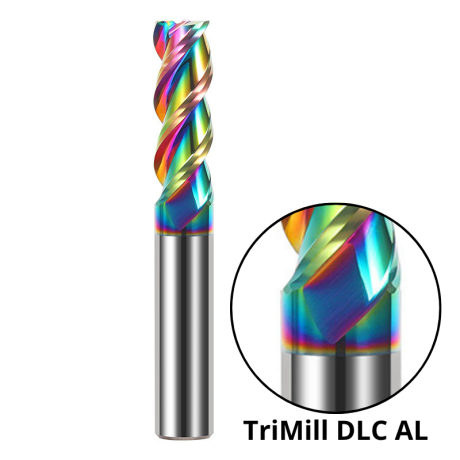
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.05Price €4.10without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute HRC65 DLC Coated Carbide End Mill, U-Shaped Flute, for Aluminium | DuraEdge3 Alu
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 40 morePrice €6.73Price €5.47without VAT