


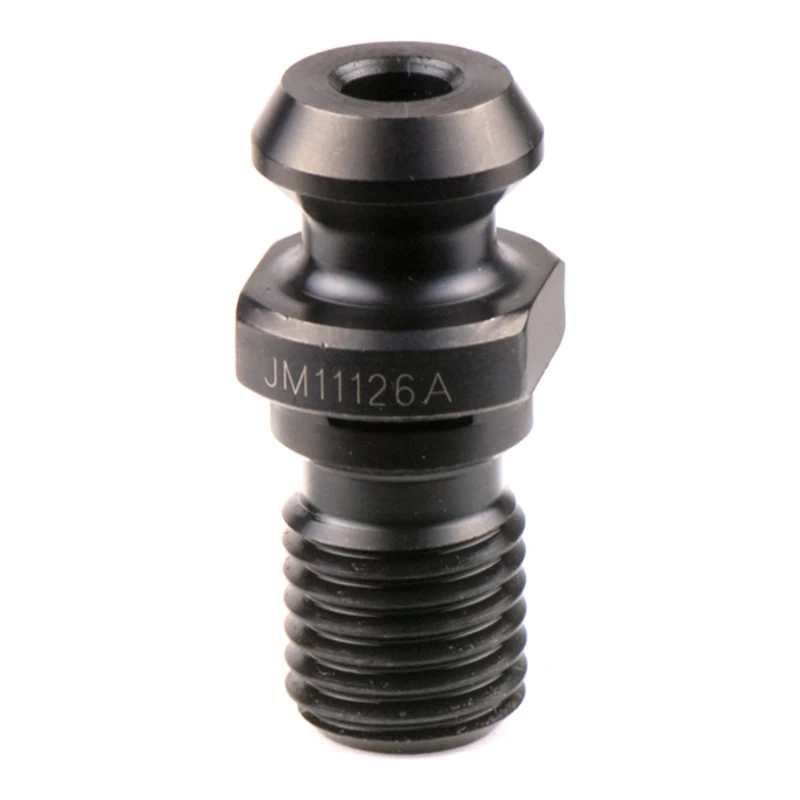
Mazak BT40/BT50 pull stud (retention knob) for JIS B 6339 tool holders, M16/M24 thread, C/CO, through bore
Shipping costs are not included in the price.
Shipping costs are not included in the price.
Ask about the product

The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: 81A7-7A6D8
Product description
1. Pull stud and geometry required by the spindle
A pull stud screws into a toolholder and its head engages the spindle gripping mechanism. Selection includes the complete head and neck profile, thread, lengths, gripping surfaces, passage and sealing arrangement.
The nominal reference geometries below are Mazak BT40 and BT50 profiles, not measurements of a specific part. Compare the required profile with the machine model and spindle-type documentation; the machine brand alone does not specify one universal stud.
2. Separate Mazak BT family
Mazak BT geometry has its own length, head and neck. It is not automatically a general BT/MAS403 profile or a pull-stud profile for Haas. A shared BT size or thread does not make these geometries interchangeable.
The required part drawing also defines head position relative to the flange and the correct gripping surface. Similar individual dimensions do not establish the complete profile.
3. Nominal reference dimensions
The table retains the complete stated nominal dimensions of this reference geometry. Lengths and diameters are in millimetres. M retains the metric thread designation without adding a pitch or thread class.
| Reference profile | M | L [mm] | L1 [mm] | D2 [mm] | D1 [mm] | D3 [mm] | D [mm] | d [mm] |
|---|---|---|---|---|---|---|---|---|
| Mazak BT40 | M16 | 44.1 | 19.1 | 18.8 | 12.45 | 22 | 17 | 7 |
| Mazak BT50 | M24 | 65.2 | 25.2 | 29 | 20.83 | 37 | 25 | 10 |
External dimensions do not assign a bore path or O-ring to a real part. Retain the symbols and measurement points of the correct drawing when comparing profiles.
4. Symbols and correct measurement points
| Symbol | Meaning only in this geometry |
|---|---|
| L | Overall length |
| L1 | Head face → support plane |
| D2 | Head diameter |
| D1 | Neck diameter |
| D3 | Flange transverse dimension |
| D | Pilot diameter beside thread |
| d | Axial-feature diameter in drawing |
L is the overall length from the head front to the end of the threaded portion. L1 runs from the head front to the flange support face; it is not the thread length.
In this BT reference D is the pilot, D1 the neck, D2 the head and D3 the transverse flange dimension. Lowercase d is an axial feature in the drawing. Do not read it as the neck diameter.
The transverse flange dimension does not automatically specify a wrench size. Retain the endpoints of each dimension line.
5. Rear 45° slope and 30° head front
The reference drawing separates two angle callouts. The 45° angle belongs to the rear gripping slope between the maximum head diameter and neck. A separate 30° callout is marked at the head front.
| Position in the drawing | Reference angle |
|---|---|
| Rear gripping slope of the head | 45° |
| Head front | 30° |
Do not substitute one surface for the other when comparing angles. A nominal drawing callout does not replace identification of the profile or measurement of a specific part.
6. Bore and sealing as separate features
Reference d is 7 mm for BT40 and 10 mm for BT50. It is the nominal diameter of the axial feature shown in the drawing; it does not prove a through passage in an actual stud.
A through passage connects both ends of the part. A blind bore ends inside it. A visible opening in the head face does not establish the bore path.
The O-ring and passage are separate features. Compare ring presence and number, groove or seal position and contact face with the machine-system requirements. C/CO codes do not replace this check and should not inherit their meaning from another family.
7. Selection for the model and spindle type
Start with the complete drawing of the stud required by the machine model and spindle type. Compare in this order:
- The correct Mazak BT or Mazak CAT family.
- The thread, thread pitch and required type.
- The head, neck, pilot and flange using their own symbols.
- The overall length and head-to-support-face distances.
- The rear gripping surface and separate head front.
- The passage and separate sealing requirements.
M16 or M24 does not specify a pitch here. Do not infer pitch from size alone or resemblance to another part. The reference does not establish compatibility with every spindle sharing that name.
8. Short FAQ
Does Mazak BT use the same stud as general BT?
Do not assume so. This reference has its own lengths and head profile; compare the complete drawing.
Does D1 identify the same feature in Mazak BT and CAT?
No. It is the neck in BT and the pilot near the thread in this CAT geometry.
Do 45° and 30° describe the same slope?
No. The 45° callout is at the rear gripping surface and 30° at the head front.
Does CO alone prove an O-ring or through passage?
Do not infer the actual passage or sealing arrangement from the code alone. Check them separately.
Related pull studs and tool holders
Compare pull stud families. The holder and stud must match the specific spindle, head profile, thread, length, bore and seal.
Other pull stud families
- BT30/BT40/BT45/BT50 pull stud (retention knob), 45°/60°/90°, through or non-through, with O-ring / without O-ring
- DIN 69872 SK30/SK40/SK50 pull stud (retention knob), through or non-through, with O-ring / without O-ring
- Pull stud (retention knob) for Haas SK40/SK50, M16/M24 thread
- ISO7388 A/B 30/40/45/50 pull stud (retention knob), M12/M16/M20/M24 thread
- CAT30/CAT40/CAT45/CAT50 pull stud (retention knob), inch thread
- OTT40/OTT50 pull stud (retention knob), M16/M24 thread
- ISO20/ISO25/ISO30 pull stud (retention knob), M8/M12 thread
- Pull stud (retention knob) for Mazak CAT40/CAT50, M16/M24 metric thread
- JIS 30P/35P/40P/45P/50P/55P pull stud (retention knob)
Tool holders
Related products
-
C74F-C524A
 Pull Studs 0.00
BT30/BT40/BT45/BT50 pull stud (retention knob) for JIS B 6339 tool holders, 45°/60°/90°, through and non-through variants, variants with O-ring
BT30-45, for JIS B 6339 holders - non-through, M12, L43 mm, angle 45° BT30-60, for JIS B 6339 holders - non-through, M12, L43 mm, angle 60° BT30-90, for JIS B 6339 holders - non-through, M12, L43 mm, angle 90° BT30C-45, for JIS B 6339 holders - through bore, M12, L43 mm, angle 45° BT30C-60, for JIS B 6339 holders - through bore, M12, L43 mm, angle 60° + 31 morePrice €3.66Price €2.98without VATShipping costs are not included in the price. -
2436-AE53C
 Pull Studs 0.00
SK30/SK40/SK50 pull stud (retention knob), DIN 69872 profile, for DIN 69871 tool holders, through and non-through variants, variants with O-ring
SK40-BO, DIN 69872 - non-through, with O-ring, M16, L54 mm SK50-A, DIN 69872 - through bore, M24, L74 mm SK50-AO, DIN 69872 - through bore, with O-ring, M24, L74 mm SK50-B, DIN 69872 - non-through, M24, L74 mm SK50-BO, DIN 69872 - non-through, with O-ring, M24, L74 mm + 6 morePrice €4.92Price €4.00without VATShipping costs are not included in the price. -
C3A6-6D925
 Pull Studs 0.00
Haas SK40/SK50 pull stud (retention knob) for DIN 69871 tool holders, M16/M24 thread, through-bore and O-ring variants
Haas SK40, for DIN 69871 holders - through bore, M16×2.0, L57.15 mm, angle 45° Haas SK50, for DIN 69871 holders - M24×3.0, L85.05 mm, angle 45° Haas SK40, for DIN 69871 holders - through bore, with O-ring, M16×2.0, L57.15 mm, angle 45°Price €5.70Price €4.64without VATShipping costs are not included in the price. -
3D23-1A5A9
 Pull Studs 0.00
Pull stud (retention knob) for DIN 69871 tool holders, ISO 7388 A/B profiles 30/40/45/50, through bore variants
ISO7388-40A, for DIN 69871 holders - through bore, M16, L54 mm ISO7388-50A, for DIN 69871 holders - through bore, M24, L74 mm ISO7388-40B, for DIN 69871 holders - through bore, M16, L44.4 mm ISO7388-50B, for DIN 69871 holders - through bore, M24, L66.55 mm ISO7388-30A, for DIN 69871 holders - M12, L44 mm, angle 15° + 3 morePrice €5.24Price €4.26without VATShipping costs are not included in the price. -
D8B1-01BFC
 Pull Studs 0.00
CAT30/CAT40/CAT45/CAT50 pull stud (retention knob) for ANSI/ASME B5.50 tool holders, inch thread, through bore variants
CAT40-A, for ANSI/ASME B5.50 holders - through bore, 5/8"-11, L38.1 mm, angle 45° CAT50-A, for ANSI/ASME B5.50 holders - through bore, 1"-8, L58.42 mm, angle 45° BT-CAT40-45C, for ANSI/ASME B5.50 holders - 5/8"-11, angle 45° BT-CAT50-90C, for ANSI/ASME B5.50 holders - 1"-8, angle 90° CAT30, for ANSI/ASME B5.50 holders - through bore, 1/2"-13, L27.94 mm, angle 45° + 1 morePrice €5.70Price €4.64without VATShipping costs are not included in the price. -
8045-7E52E
 Pull Studs 0.00
OTT40/OTT50 pull stud (retention knob), M16/M24 thread
OTT40 - through bore, M16, L53 mm OTT50 - through bore, M24, L65.1 mmPrice €6.83Price €5.55without VATShipping costs are not included in the price. -
6A89-FD6D2
 Pull Studs 0.00
ISO20/ISO25/ISO30 pull stud (retention knob), M8/M12 thread
ISO20 - M8, L26 mm ISO25 - M8, L28 mm ISO30 - M12, L44 mmPrice €4.10Price €3.33without VATShipping costs are not included in the price. -
B9B8-A4C23
 Pull Studs 0.00
Mazak CAT40/CAT50 pull stud (retention knob), M16/M24 metric thread
Mazak-CAT40 - M16, L41.25 mm, angle 45° Mazak-CAT50 - M24, L65.4 mm, angle 45°Price €7.99Price €6.50without VATShipping costs are not included in the price. -
3578-7E58B
 Pull Studs 0.00
JIS B 6339 pull stud (retention knob), profiles 30P/35P/40P/45P/50P/55P, through bore
JIS-30P, JIS B 6339 - through bore, M12, L43 mm JIS-35P, JIS B 6339 - through bore, M12, L44 mm JIS-40P, JIS B 6339 - through bore, M16, L54 mm JIS-45P, JIS B 6339 - through bore, M20, L60 mm JIS-50P, JIS B 6339 - through bore, M24, L74 mm + 1 morePrice €4.92Price €4.00without VATShipping costs are not included in the price.


Bestsellers
-
Bestseller
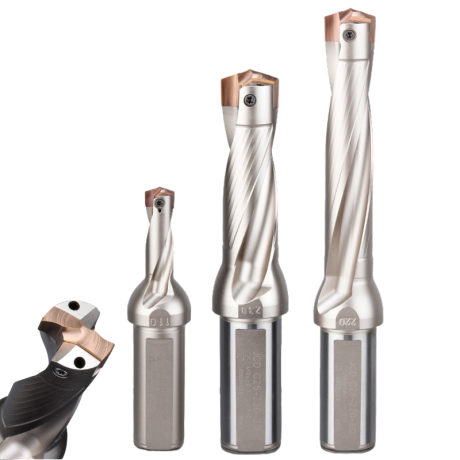
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.86Price €56.79without VAT -
Bestseller
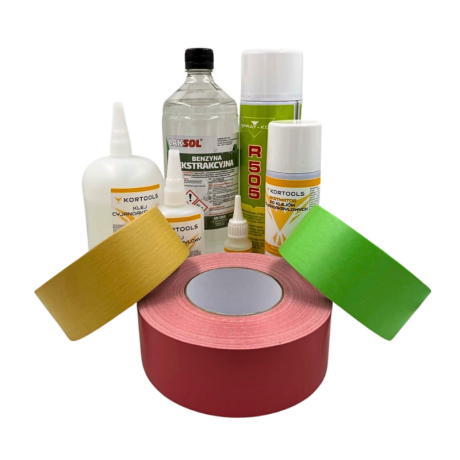
Kortools Adhesive + Tape CNC Workholding Kit
Yellow tape 5cm x 50m; adhesive 100g Yellow tape 5cm x 50m; adhesive 500g Yellow tape 10cm x 50m; adhesive 100g Yellow tape 10cm x 50m; adhesive 500g Green tape 5cm x 50m; adhesive 100g + 7 morePrice €44.66Price €36.31without VAT -
Price €17.18Price €13.97without VAT
-
Price €7.10Price €5.77without VAT
-
Price €7.56Price €6.14without VAT
-
Bestseller
 Other Accessories 0.00
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.82Price €43.76without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.14Price €8.25without VAT -
Bestseller
 2-Flute End Mills 0.00
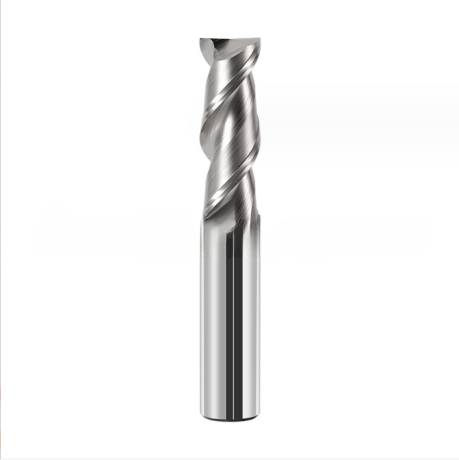
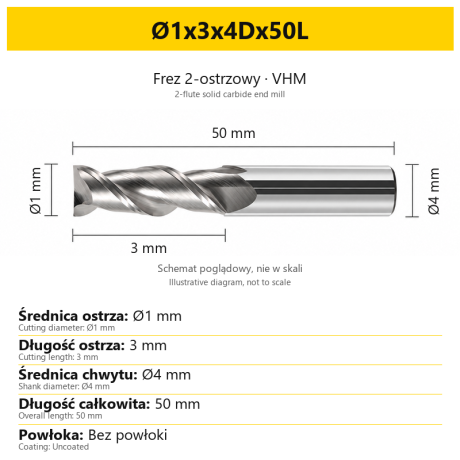
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.35Price €4.35without VAT -
Bestseller
 2-Flute End Mills 0.00
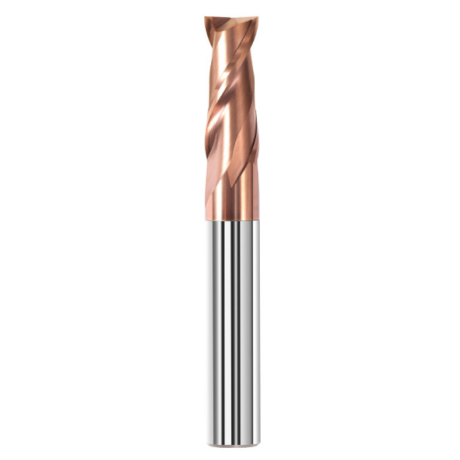
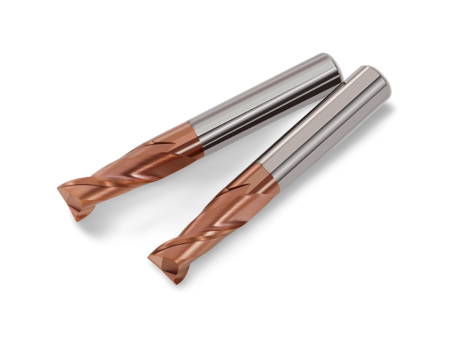
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.40Price €3.58without VAT -
Bestseller
 Ball Nose End Mills 0.00
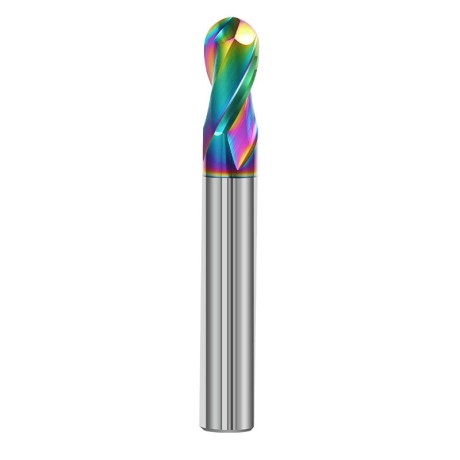
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.89Price €6.41without VAT -
Bestseller
 2-Flute End Mills 0.00
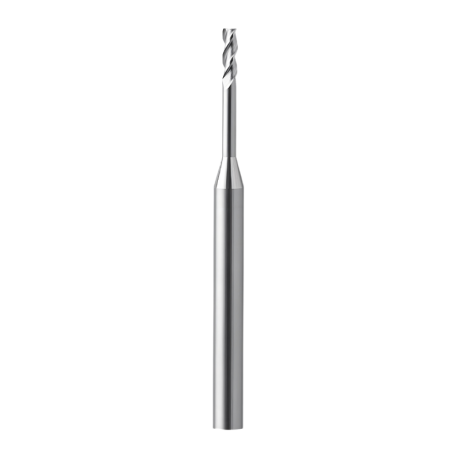
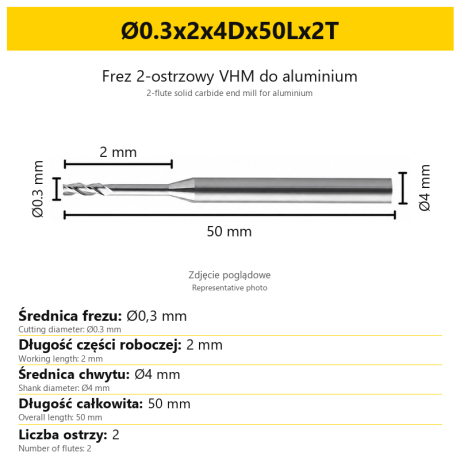
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.99Price €6.50without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.28Price €5.92without VAT -
Bestseller
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
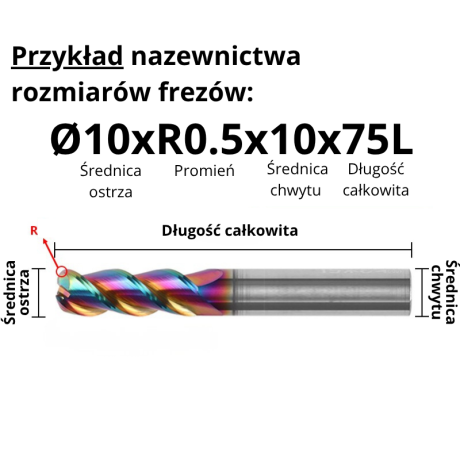
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €4.96Price €4.04without VAT -
Bestseller
 3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.10Price €4.15without VAT -
Bestseller

 Countersinks 0.00
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.81Price €3.91without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.07Price €4.12without VAT


