


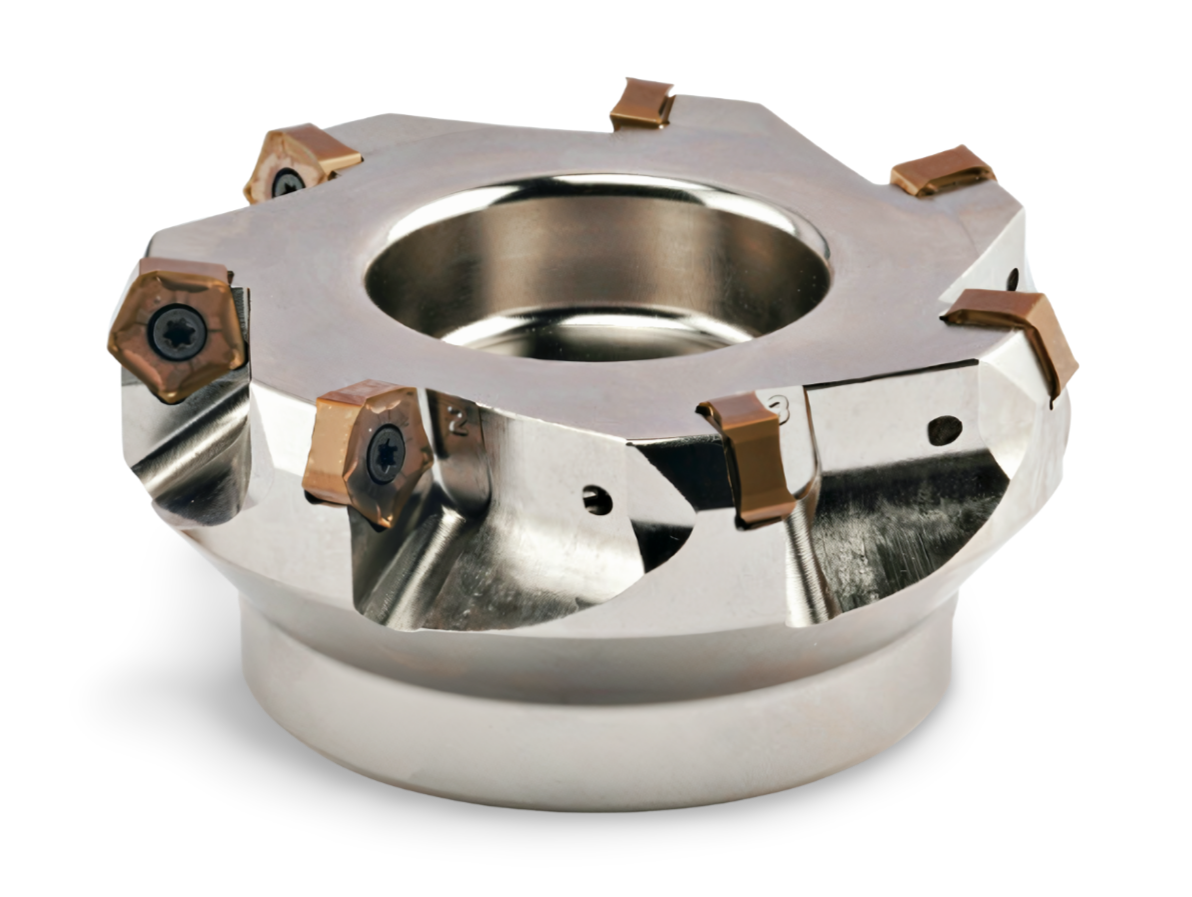
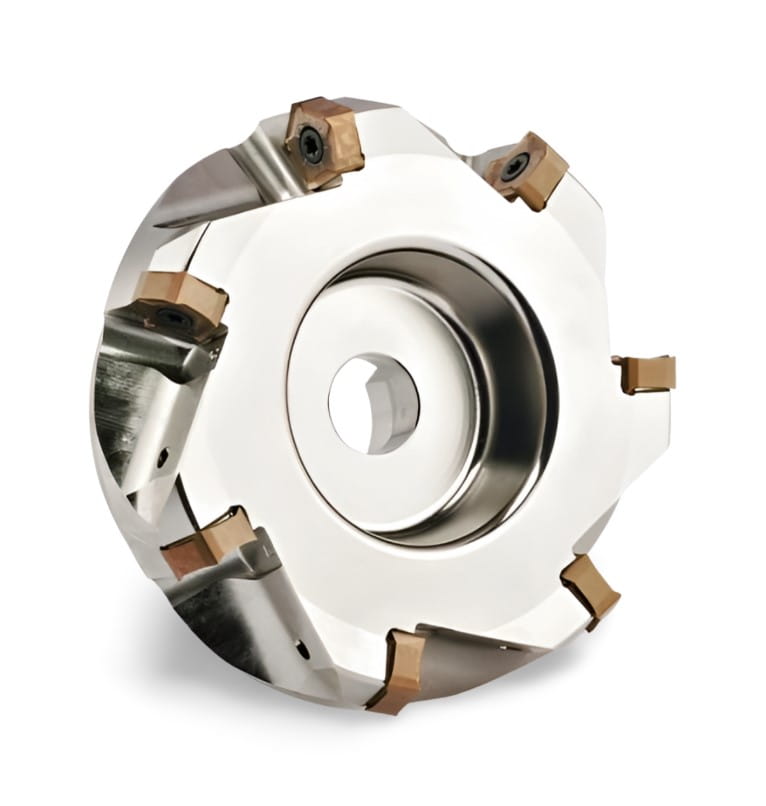
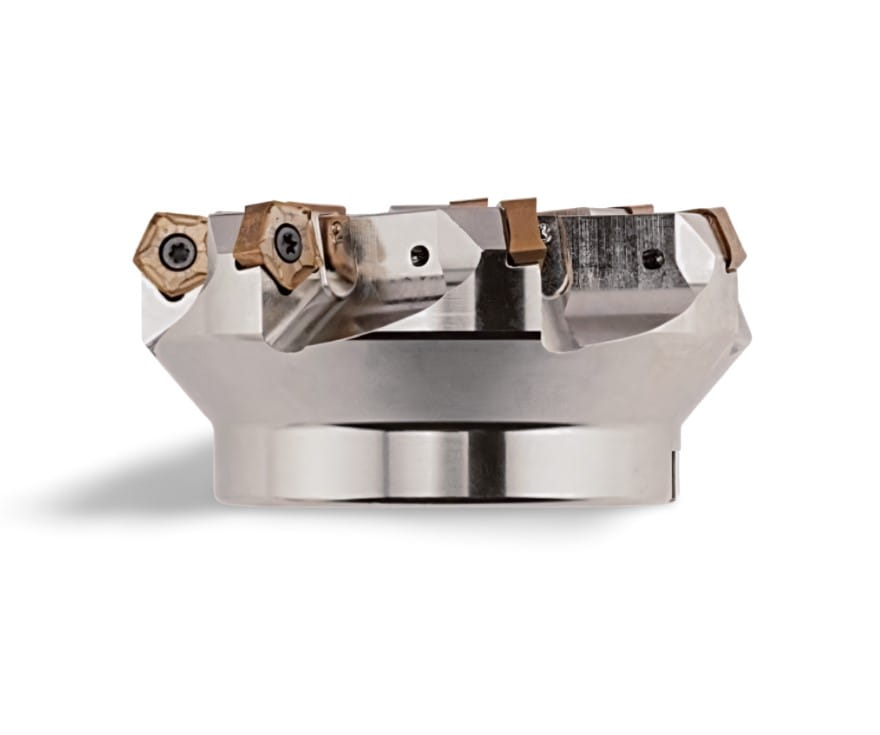
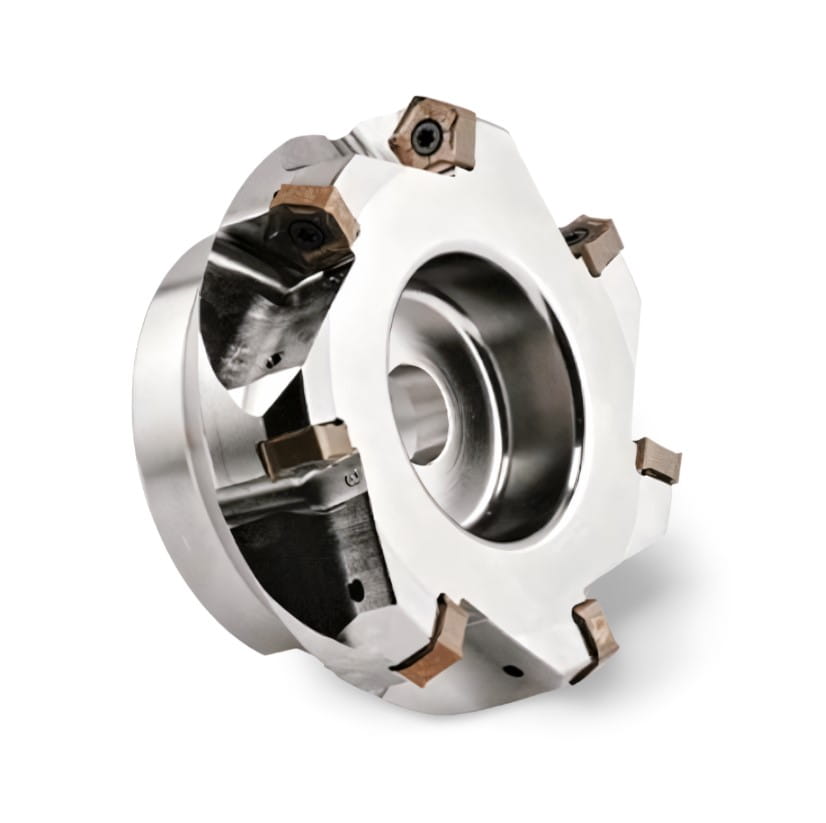
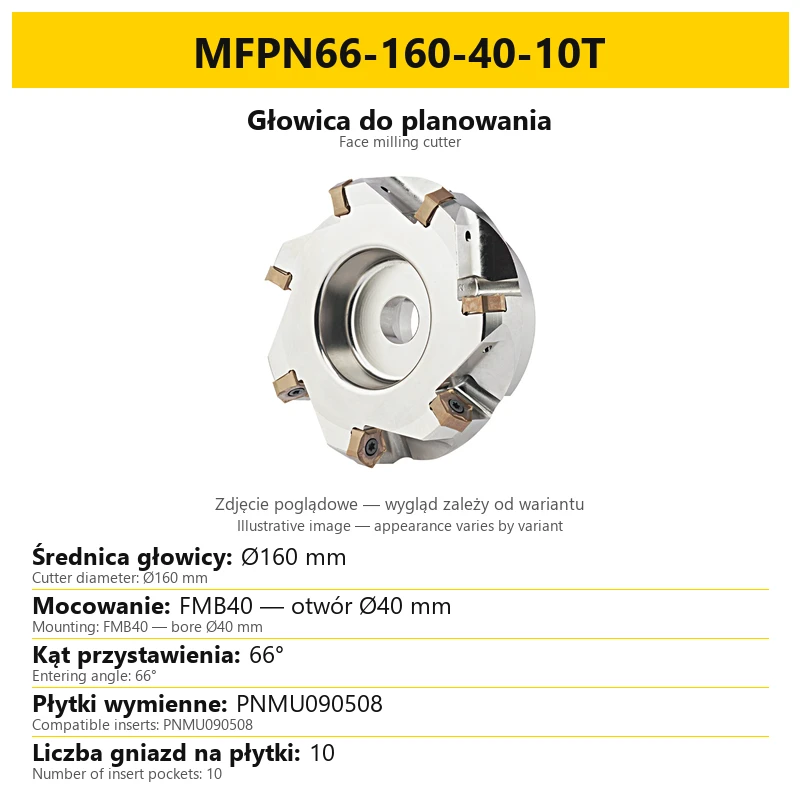
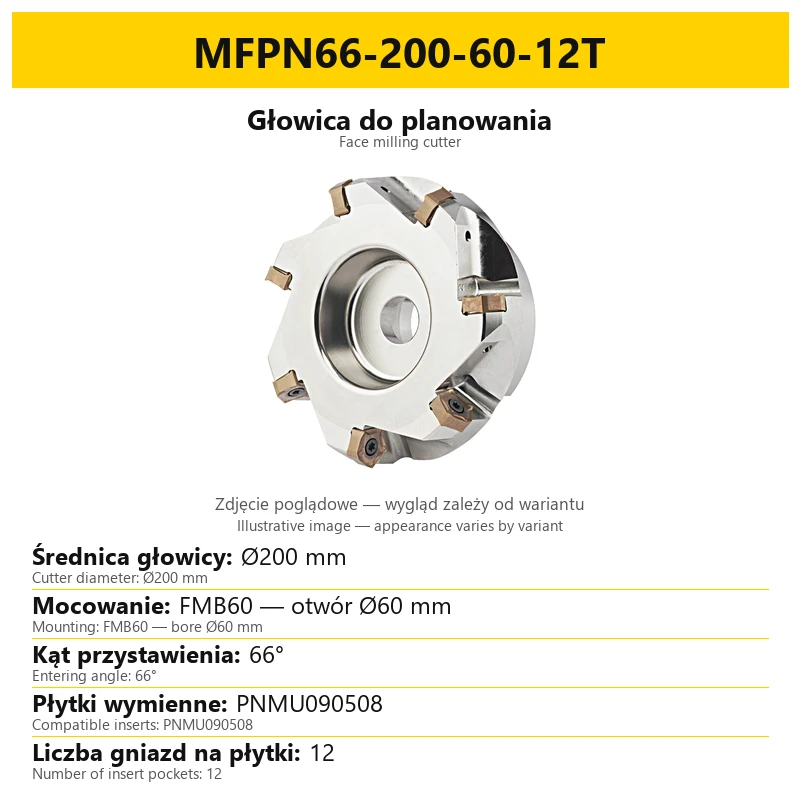
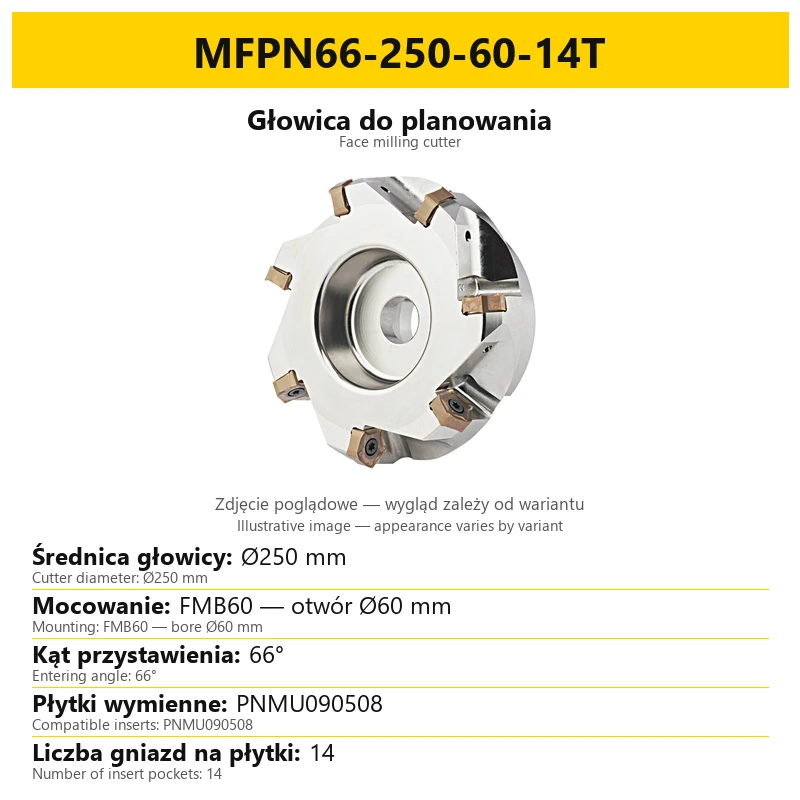


MFPN66 planning head for inserts PNMU090508 - FMB clip-on holder
Shipping costs are not included in the price.
Shipping costs are not included in the price.
Ask about the product

The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: 95FF-903C4
Product description
1. MFPN66 face milling cutter
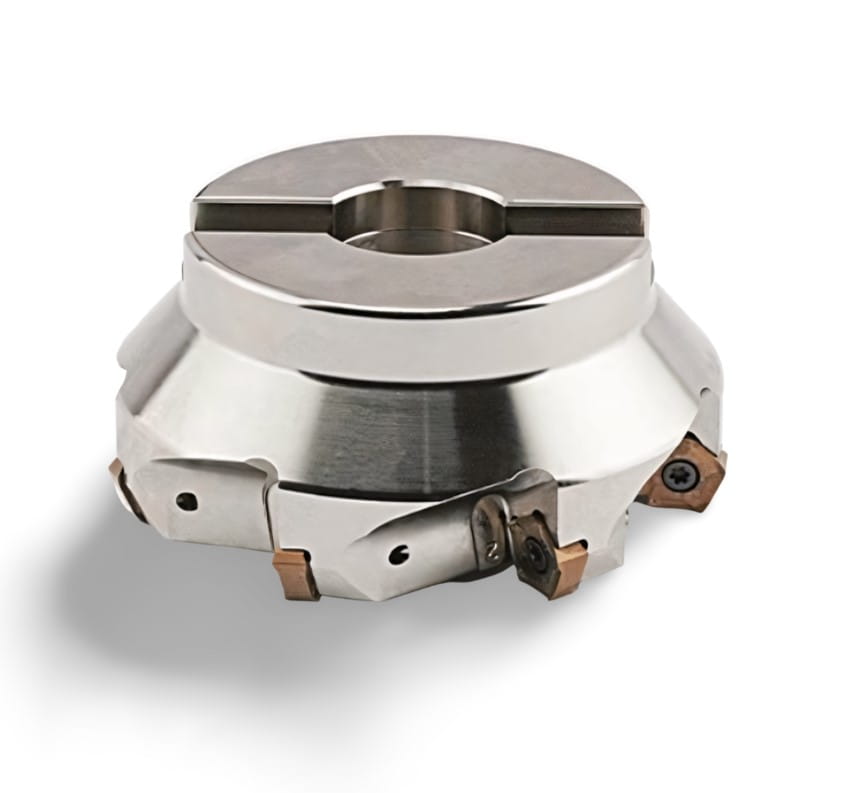
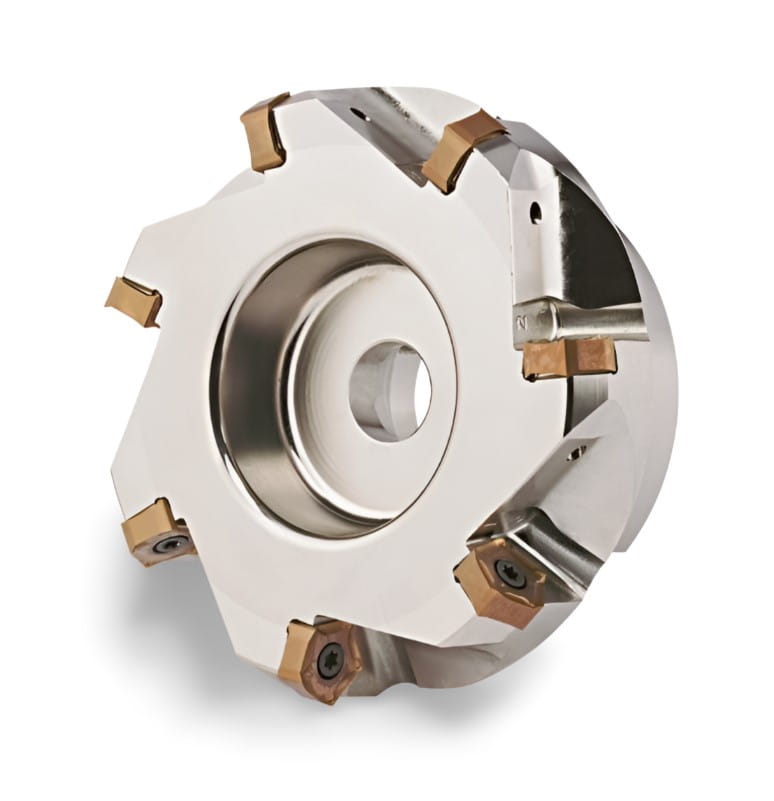
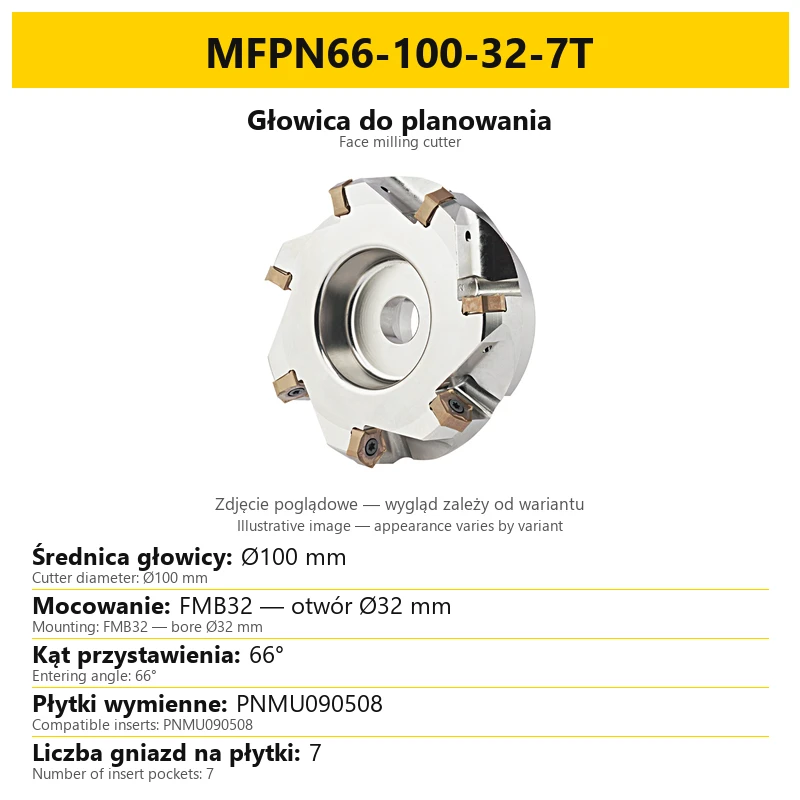
MFPN66 is an arbor-mounted face milling cutter for PNMU090508 inserts. The body is made of 42CrMo steel and has a 66° entering angle. The selected variant defines the cutter diameter, mounting bore and number of insert pockets.
| Feature | Specification |
|---|---|
| Family | MFPN66 |
| Primary operation | Facing / face milling |
| Body material | 42CrMo |
| Entering angle | 66° |
| Insert system | PNMU090508 |
| Mounting | FMB arbor mounting |
| Through-tool coolant | Not provided |
2. Applications
The cutter is intended for face milling and material removal at increased feed rates. The workpiece material and cutting conditions must be matched to the grade and geometry of the installed PNMU090508 insert. The cutter body code does not specify the insert grade.
| Operation | Application |
|---|---|
| Face milling | The primary application is machining flat surfaces with the cutter face. |
| Material removal at increased feed | Settings must be matched to the insert, workpiece, workholding and machine. |
| Plunge milling | Only under specifically selected machining conditions; not a universal operating mode for every setup. |
The feed and cutting-speed values below are starting points for trials. They do not guarantee a particular output or identical settings across all cutter sizes and materials.
3. FMB mounting and variant selection
Match the cutter to the mounting diameter of the FMB arbor. The mounting bore is a different dimension from the cutter diameter. Both are included in the selected variant code and shown on its information card.
| Parameter | Meaning when selecting |
|---|---|
| Cutter diameter | The working diameter of the tool; not the mounting diameter. |
| Mounting bore | The bore diameter corresponding to the selected FMB mounting size. |
| Number of pockets | The number of inserts when all cutter pockets are populated. |
| Coolant arrangement | This body has no through-tool coolant. Contact Kortools about a body with internal coolant passages. |
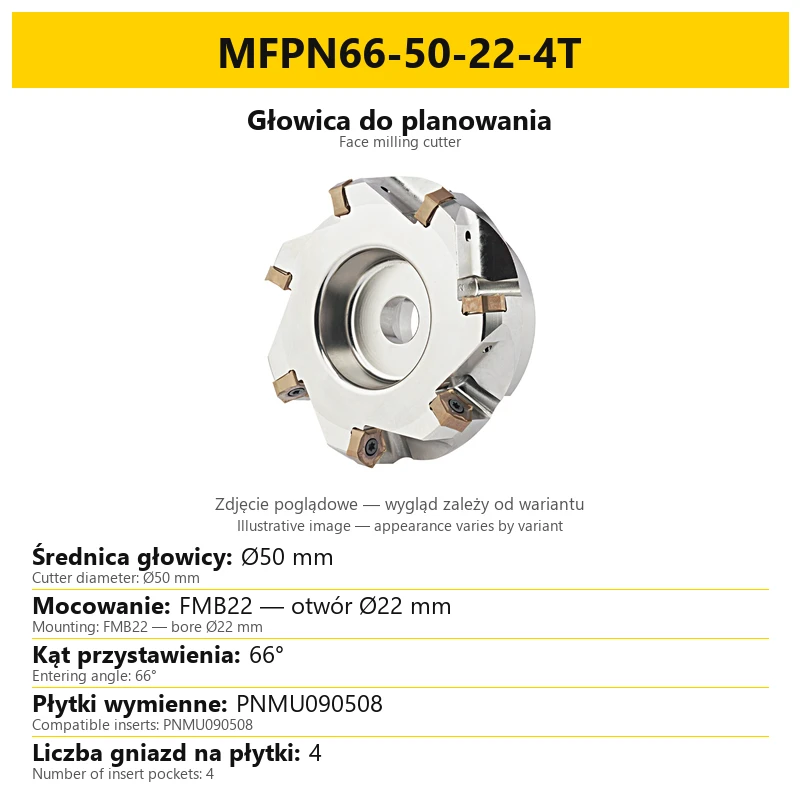
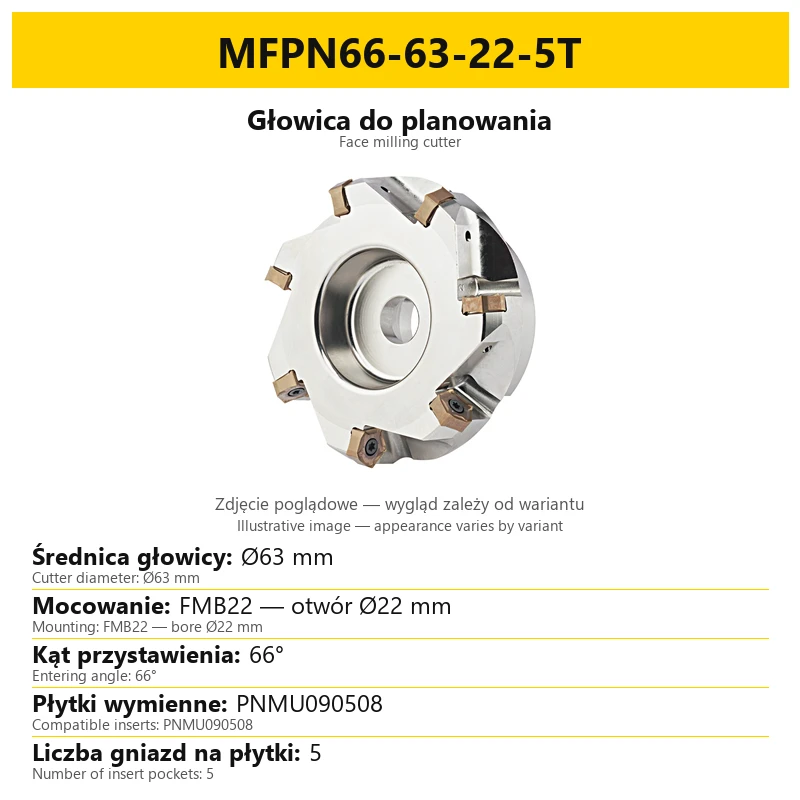
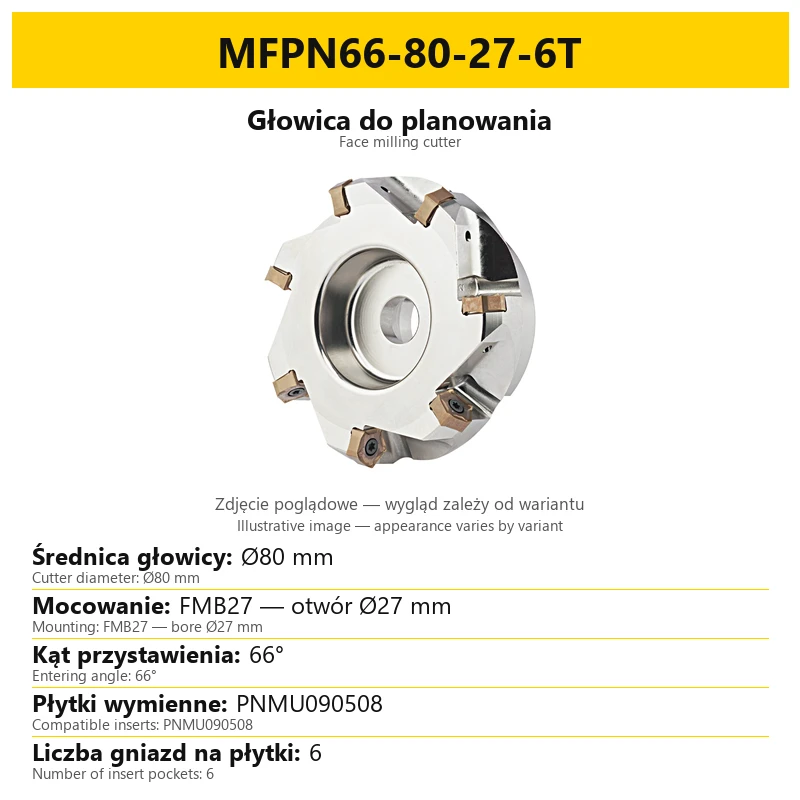
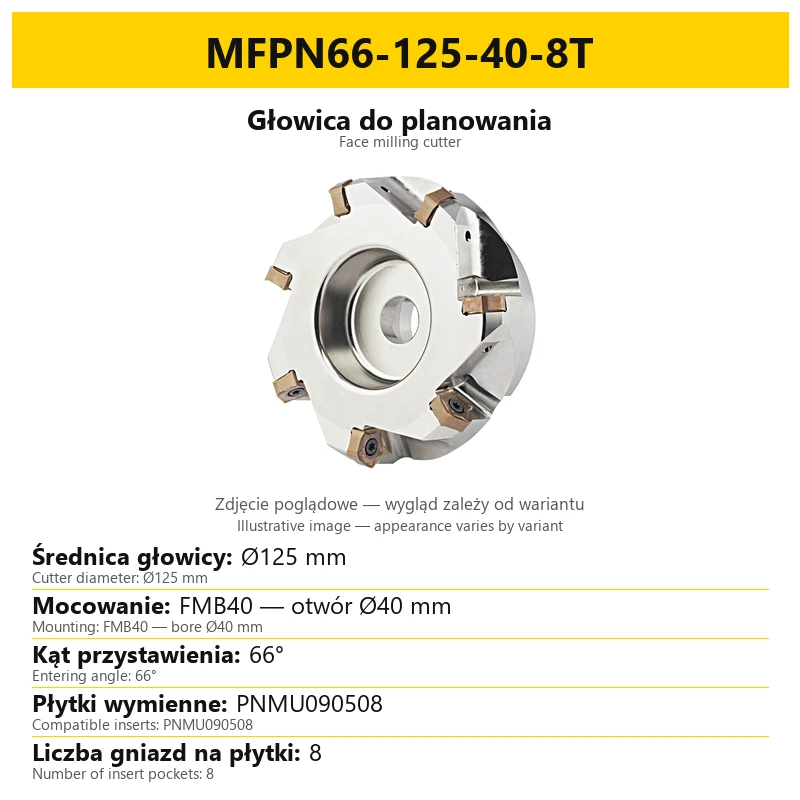
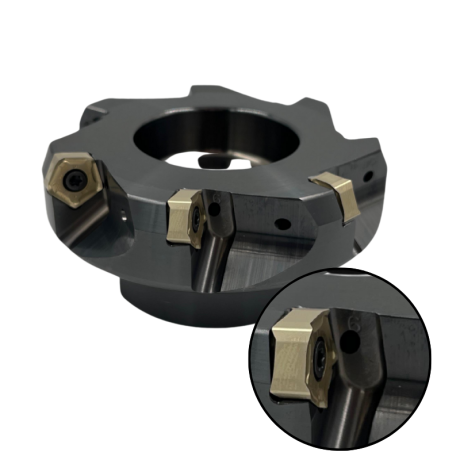
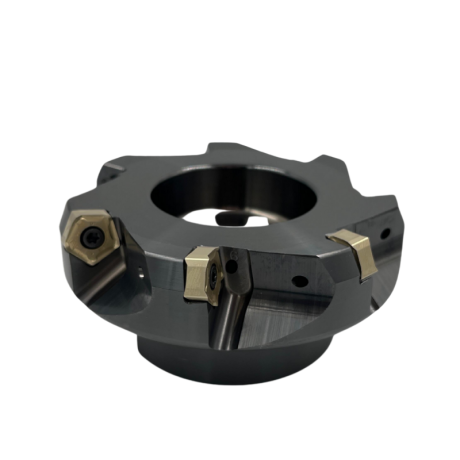
Select the required size to view its parameters. The illustrative photograph shows the MFPN66 family; the selected variant parameters define its diameter, mounting bore and pocket count.
4. Understanding the designation
The designation combines the cutter family, angle, working diameter, mounting bore and number of pockets. The final letter T refers to the number of insert pockets, not the number of cutting edges on one insert.
| Designation element | Meaning |
|---|---|
| MFPN | Cutter family |
| 66 | 66° entering angle |
| First number after the family designation | Cutter diameter in millimetres |
| Next number | Mounting bore diameter in millimetres |
| Number preceding T | Number of insert pockets in the body |
For example, 63, 22 and 5T indicate a Ø63 mm cutter, a Ø22 mm bore and five pockets. This example explains the notation; choose the required item in the variant selector.
5. Inserts and supplied accessories
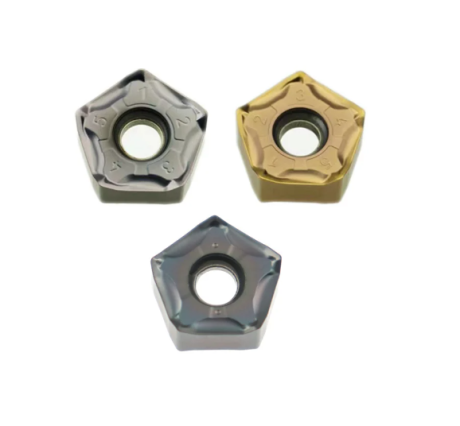
The body accepts PNMU090508 inserts. The insert is double-sided and provides 10 cutting edges. The edge count of an individual insert is separate from the cutter pocket count.
| Item | Information |
|---|---|
| Compatible insert | PNMU090508 |
| Cutting edges per insert | 10, double-sided design |
| Body | 42CrMo steel |
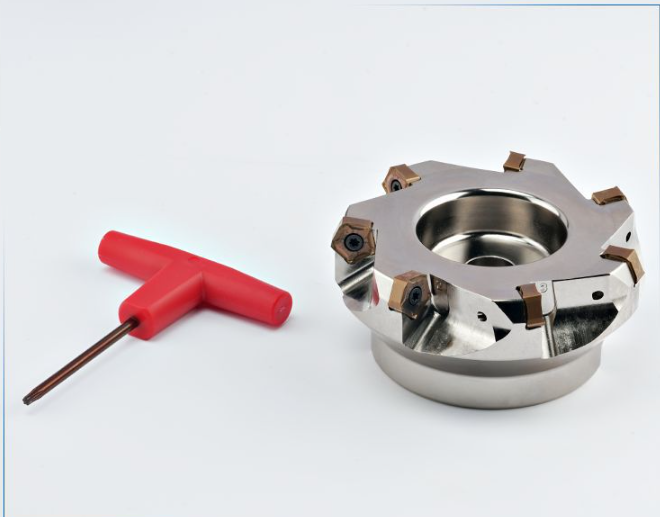
| Supplied wrench | T15 |
| Supplied screws | M4×10 mm |
Select the insert grade for the workpiece material and machining conditions. It is not specified by the cutter body designation. The installed inserts in the illustrative photograph show how they are seated; the photograph does not identify their grade or coating.
6. Cutting data — starting values
The following ranges provide starting points for machining trials. Actual settings depend on the insert grade, workpiece, holder, machine rigidity and power, workholding and coolant. Perform trials and adjust the settings to suit process stability.
| Workpiece material | Feed per tooth fz [mm/tooth] | Cutting speed Vc [m/min] |
|---|---|---|
| Carbon steel (SxxC) | 0.1–0.35 | 120–250 |
| Alloy steel (SCM and similar) | 0.1–0.35 | 100–220 |
| Die steel (SKD) | 0.1–0.4 | 80–180 |
| Austenitic stainless steel (SUS304 and similar) | 0.1–0.4 | 100–200 |
| Martensitic stainless steel (SUS403 and similar) | 0.1–0.4 | 100–200 |
| Precipitation-hardening stainless steel (SUS630 and similar) | 0.1–0.4 | 90–150 |
| Grey cast iron (FC) | 0.1–0.4 | 120–250 |
| Nodular cast iron (FCD) | 0.1–0.4 | 100–200 |
| Nickel-based alloys (Inconel and similar) | 0.1–0.35 | 20–50 |
C55 steel machining example: Vc = 250 m/min, fz = 0.4 mm/tooth, ap = 2 mm and ae = 70 mm. This is an example of machining conditions, not a universal setting for every cutter diameter or setup.
| Symbol | Quantity |
|---|---|
| Vc | Cutting speed [m/min] |
| fz | Feed per tooth [mm/tooth] |
| ap | Depth of cut [mm] |
| ae | Width of cut [mm] |
7. Selection before purchase
Check the body size, mounting arrangement and insert system together. Selection by cutter diameter alone does not account for the FMB mounting bore or the number of pockets.
| Check | Compare with |
|---|---|
| Cutter diameter | The planned operation and the selected variant parameters. |
| FMB mounting bore | The mounting diameter of your arbor. |
| Insert system | The PNMU090508 designation. |
| Pocket count | The final T designation in the selected cutter code. |
| Coolant requirement | This version has no through-tool coolant. |
If you need a different coolant arrangement or assistance with insert selection, provide the workpiece material, selected cutter code and mounting arrangement.
8. Questions and answers
Which inserts fit this cutter?
The PNMU090508 system. Select the specific insert grade for the workpiece and machining conditions.
Does T indicate the number of edges on an insert?
No. T indicates the number of pockets in the cutter. A double-sided PNMU090508 insert has 10 cutting edges.
Does the cutter have internal coolant?
This version has no through-tool coolant. Ask about a body with internal coolant passages if your application requires them.
Where can I check the selected size?
On the card assigned to the selected variant. It provides cutter diameter, mounting and pocket count; the shared photograph is illustrative.
Can the stated cutting data be used without trials?
They are starting values. Adjust them for the insert, material, machine and workholding while monitoring a trial cut.
Related products
-
CDCF-33878
 Milling Inserts 5.00
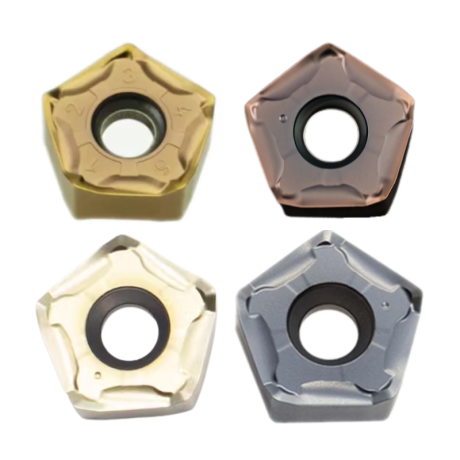
10-Edge Indexable Milling Inserts PNMU 090508 (10 pcs)
-
95FF-903C5
 Face Milling Heads 0.00
MFPN66 planning head with internal cooling for inserts PNMU090508 - FMB push-on holder


Bestsellers
-
Bestseller
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.86Price €56.79without VAT -
Bestseller
Kortools Adhesive + Tape CNC Workholding Kit
Yellow tape 5cm x 50m; adhesive 100g Yellow tape 5cm x 50m; adhesive 500g Yellow tape 10cm x 50m; adhesive 100g Yellow tape 10cm x 50m; adhesive 500g Green tape 5cm x 50m; adhesive 100g + 7 morePrice €44.66Price €36.31without VAT -
Price €17.18Price €13.97without VAT
-
Price €7.10Price €5.77without VAT
-
Price €7.56Price €6.14without VAT
-
Bestseller
 Other Accessories 0.00
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.82Price €43.76without VAT -
Bestseller
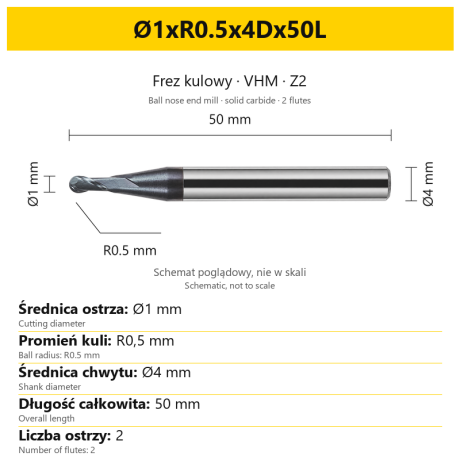 Ball Nose End Mills 0.00
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.14Price €8.25without VAT -
Bestseller
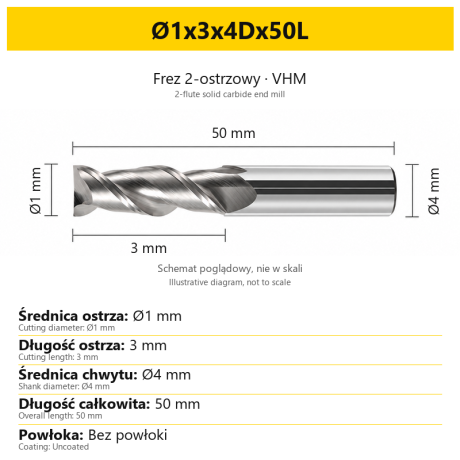 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.35Price €4.35without VAT -
Bestseller
 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.40Price €3.58without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.89Price €6.41without VAT -
Bestseller
 2-Flute End Mills 0.00
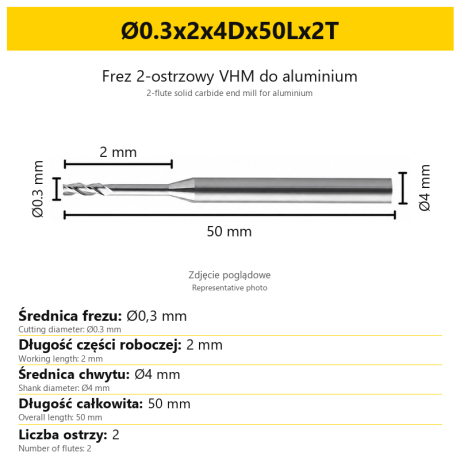
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.99Price €6.50without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.28Price €5.92without VAT -
Bestseller
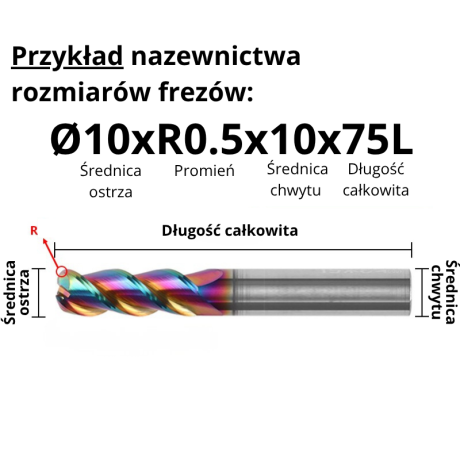
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €4.96Price €4.04without VAT -
Bestseller
 3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.10Price €4.15without VAT -
Bestseller

 Countersinks 0.00
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.81Price €3.91without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.07Price €4.12without VAT


