













Thread Milling Cutter M0.8-M20 - Multi-Flute TiSiN
Shipping costs are not included in the price.
Shipping costs are not included in the price.
Ask about the product

The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: C9D9-33819
Product description
Metric threads M2–M30 • fixed pitch • cylindrical shank
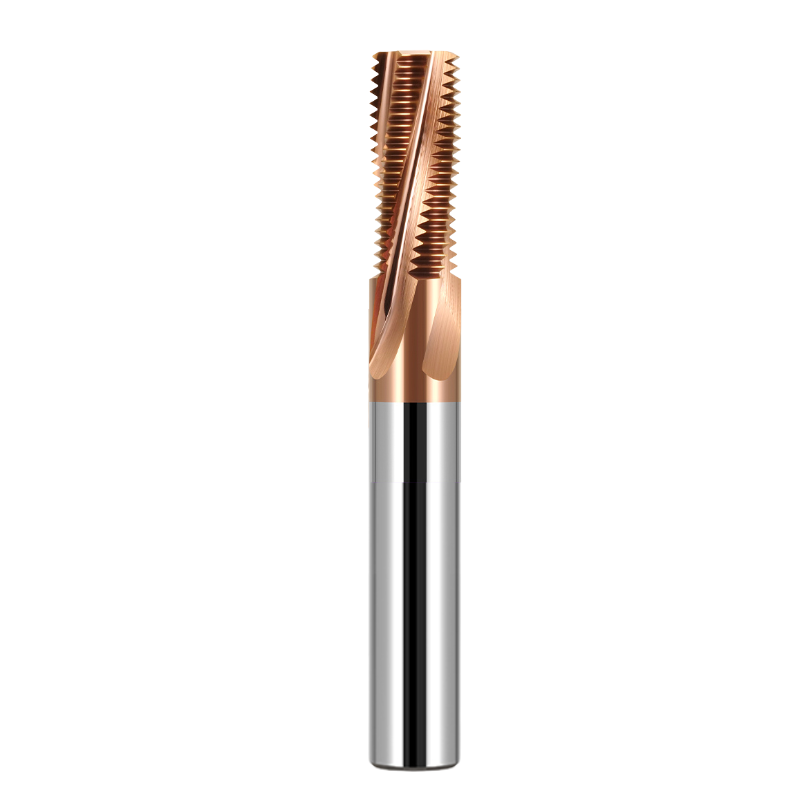
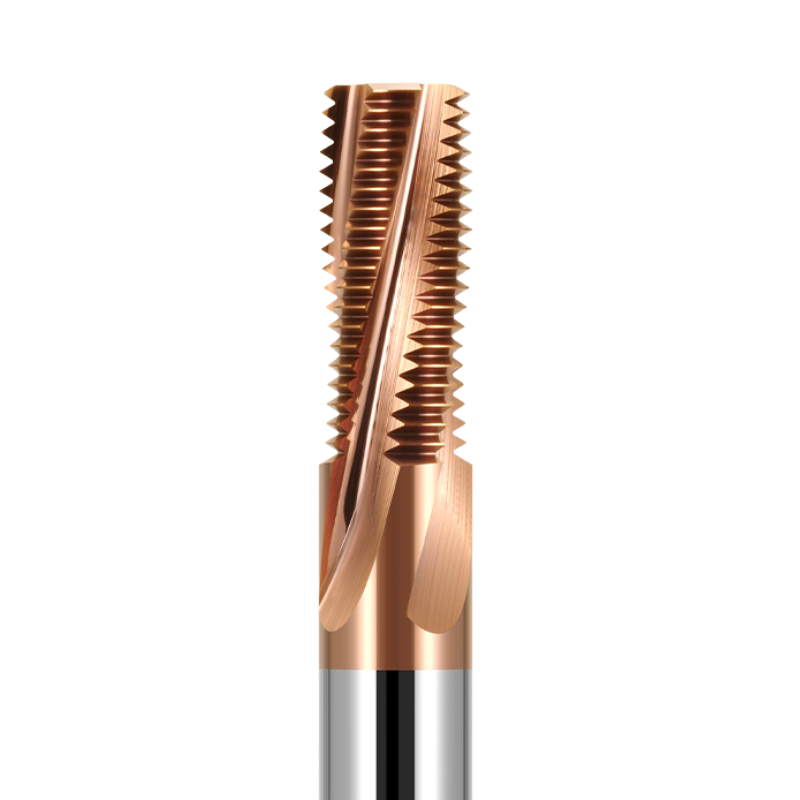
A TiSiN-coated solid carbide cutter for milling metric threads on CNC machines. The working section carries a sequence of thread-forming profiles along the tool axis. Their spacing matches the pitch of the selected variant. This full-profile design is intended for efficient production of repeated threads, including batch manufacturing.
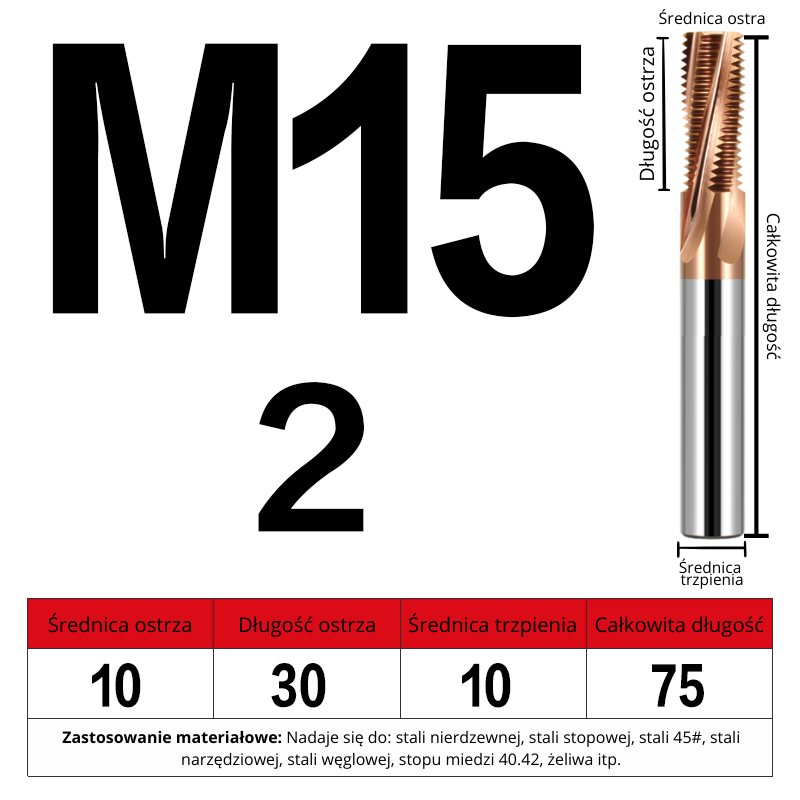
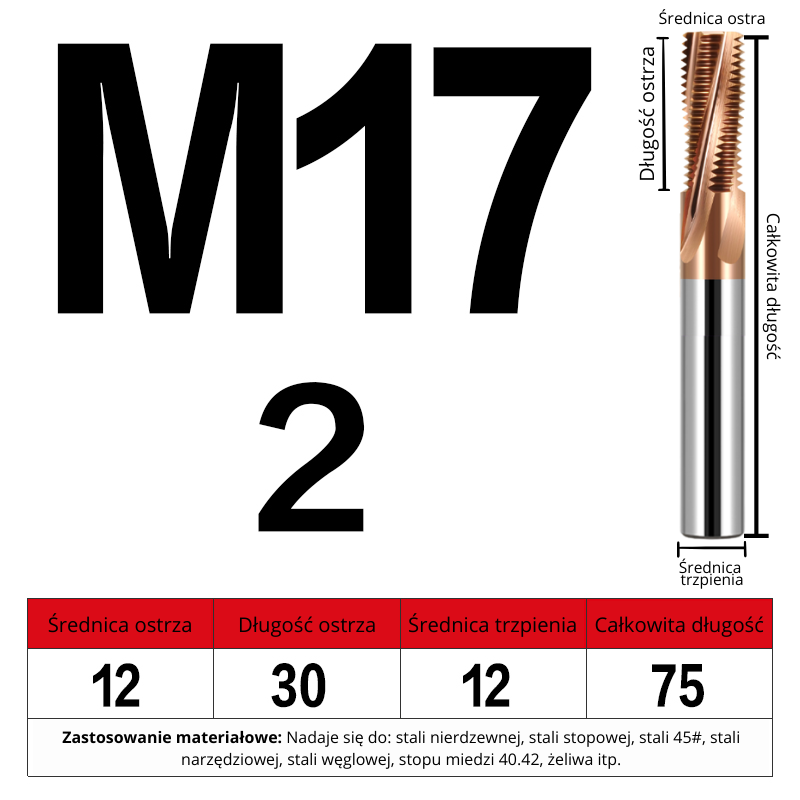
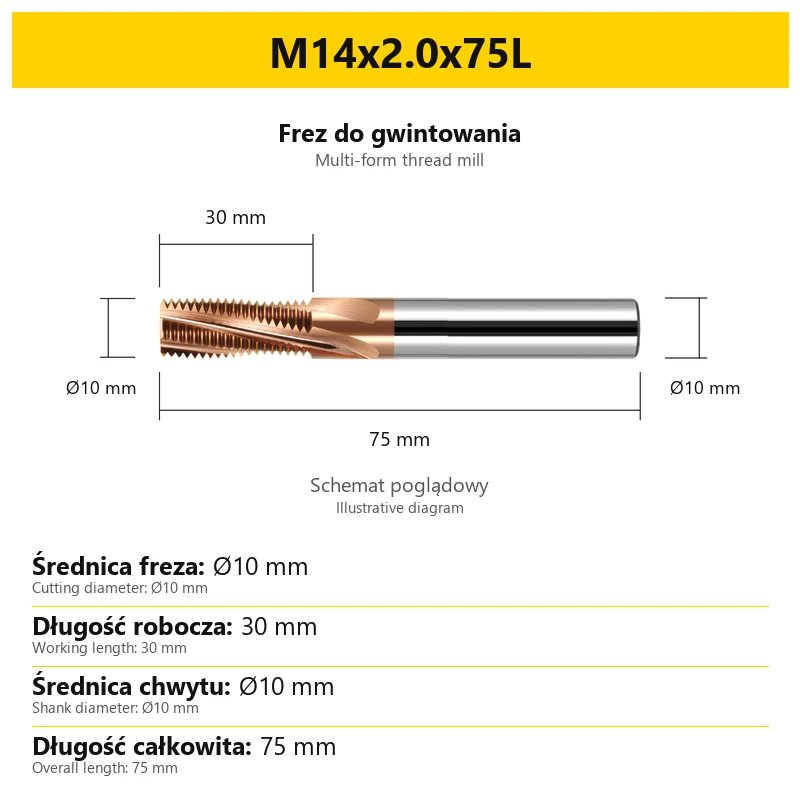
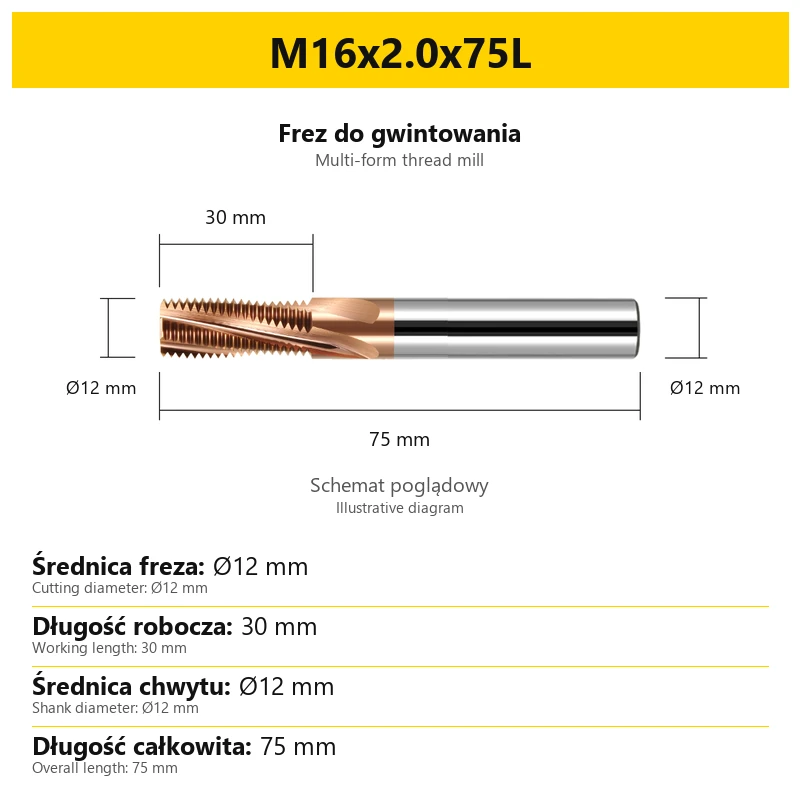
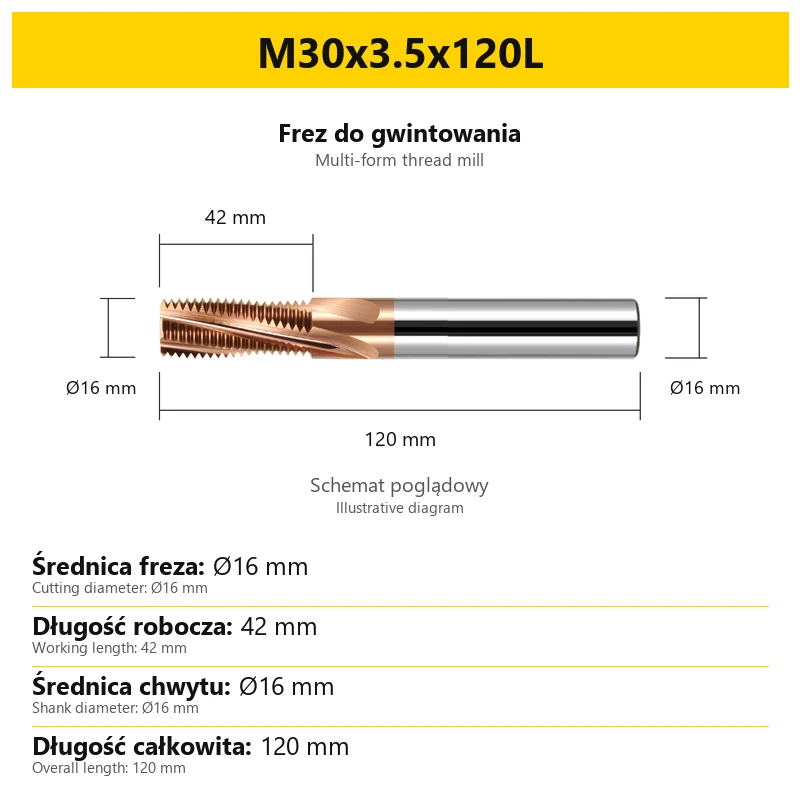
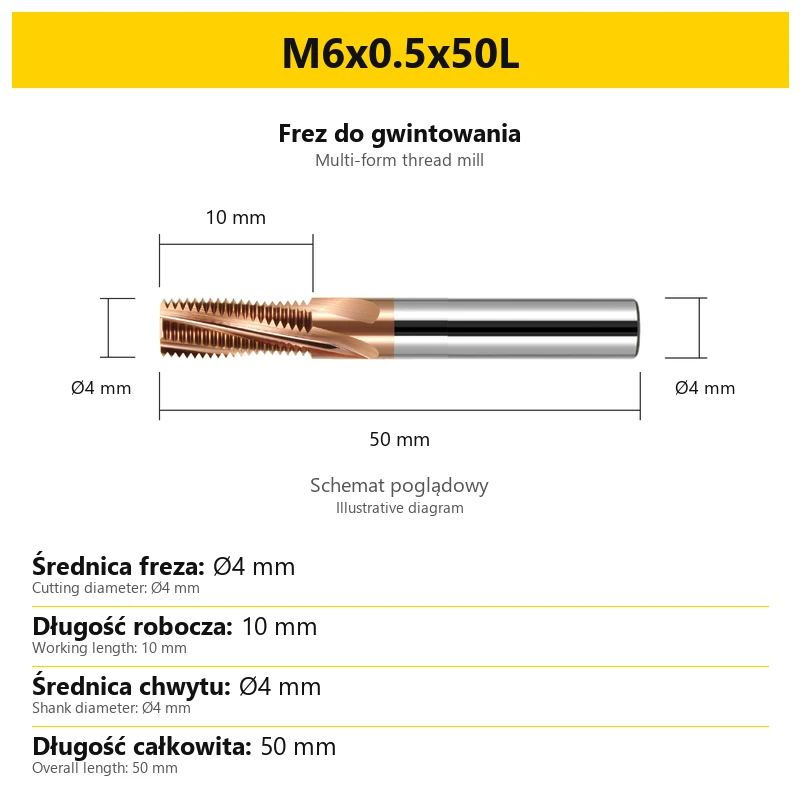
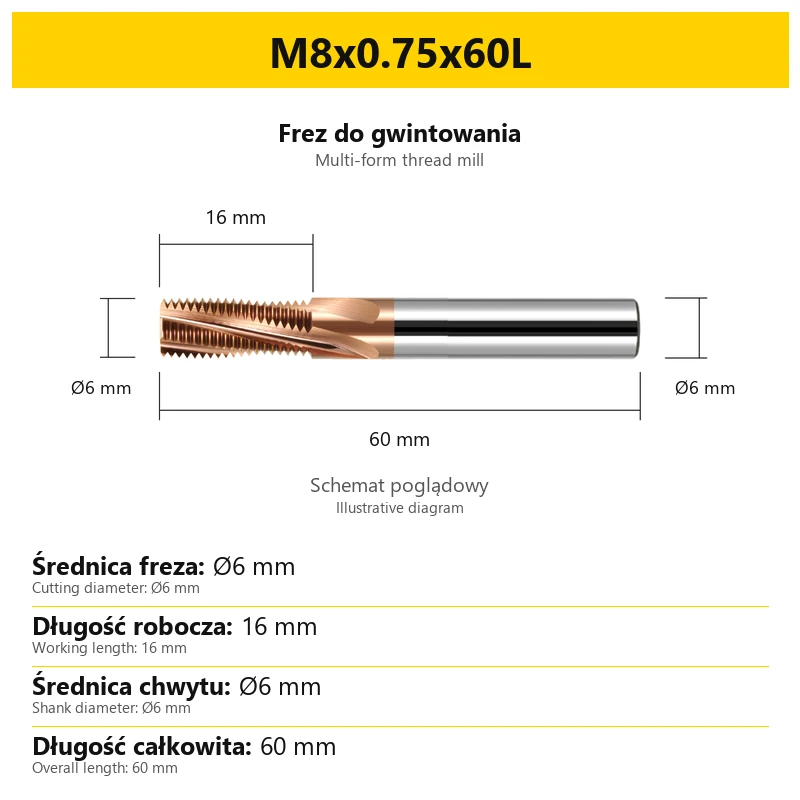
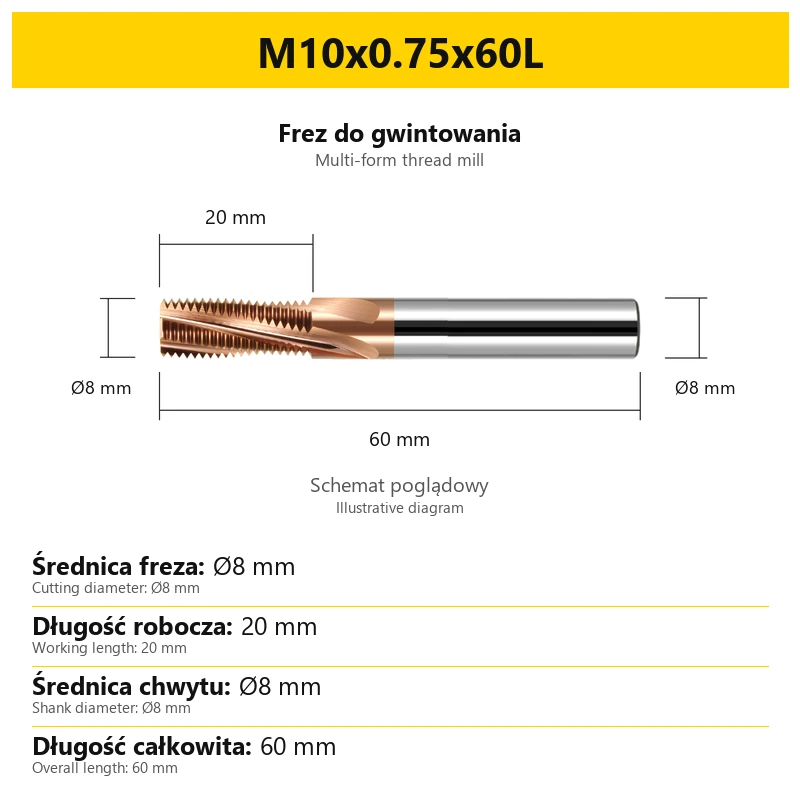
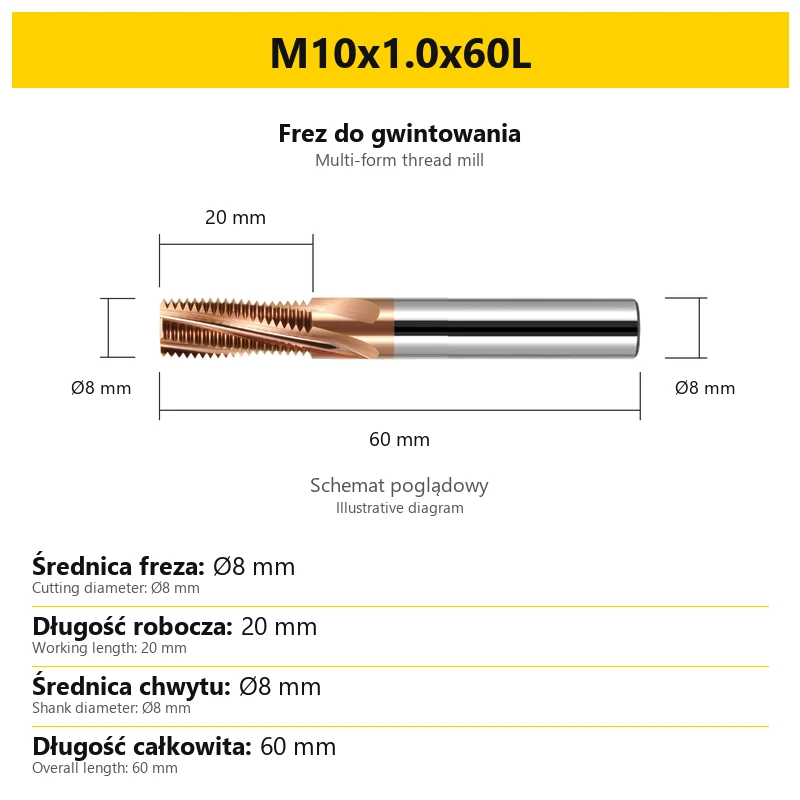
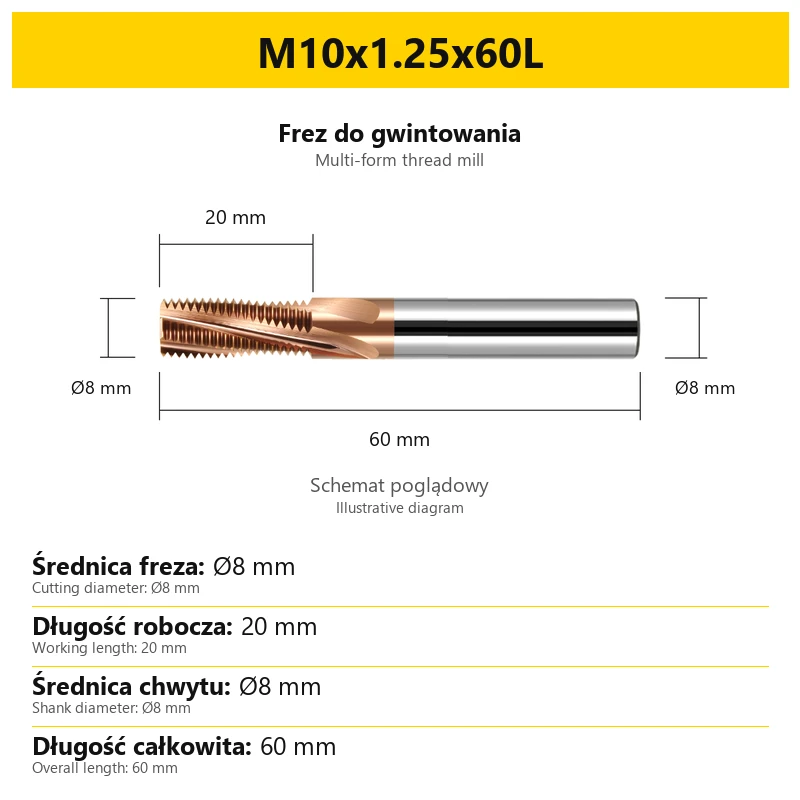
Select the variant by thread designation, pitch and required tool dimensions. The range includes different cutting and shank diameters and overall lengths from 50 to 120 mm. Each size card provides four dimensions for checking access and toolholding.
Construction and operation
| Parameter | Specification |
|---|---|
| Tool type | Multi-form, full-profile thread mill |
| Tool material | VHM — solid carbide |
| Coating | TiSiN |
| Thread type | Metric M |
| Designation range | M2–M30; available diameter and pitch combinations depend on the selected variant |
| Pitch | Fixed for each variant; 0.4 to 3.5 mm across the range |
| Shank | Cylindrical, Ø4–Ø16 mm depending on size |
| Overall length | 50–120 mm depending on variant |
Full-profile construction means multiple consecutive thread forms along the working section. The multi-form designation describes this axial arrangement. It does not state the number of flutes around the circumference. Distinguish the thread-forming section from the shank held in the toolholder.
Fixed thread pitch
Pitch is a physical feature of the cutter geometry. Select a matching tool variant for a different pitch. Changing a value in the CNC program does not change the spacing of the cutting profiles. Compare the complete designation with the component drawing, even when two cutters share the same M size.
The thread is produced as the tool follows a helical path. The machine and program must support the required interpolation, and the cutter geometry must match the thread being machined. Select the number of passes and cutting conditions for the material and working-section load; full-profile construction does not specify one universal pass count for every component.
Applications and workpiece materials
The TiSiN version is intended for thread milling in steel and cast-iron components. Its application range also includes stainless steel and titanium alloys. Consider the material grade, condition and thread requirements when choosing the size and cutting conditions.
| Material group | Application range |
|---|---|
| Carbon and alloy steels | Carbon steels, including 45#, and alloy steels, including chromium-molybdenum steels. |
| Tool and mould steels | Threads in tooling, mould and die components. |
| Stainless steel and titanium alloys | Thread machining with conditions adapted to the specific grade. |
| Cast iron | Thread milling in cast-iron components. |
For batch production, select the cutter for a repeated thread designation and a controlled machining process. Cutting diameter, working length and tool overhang affect the choice of operating conditions. Do not transfer parameters between different sizes solely because they have the same coating.
How to read the size code
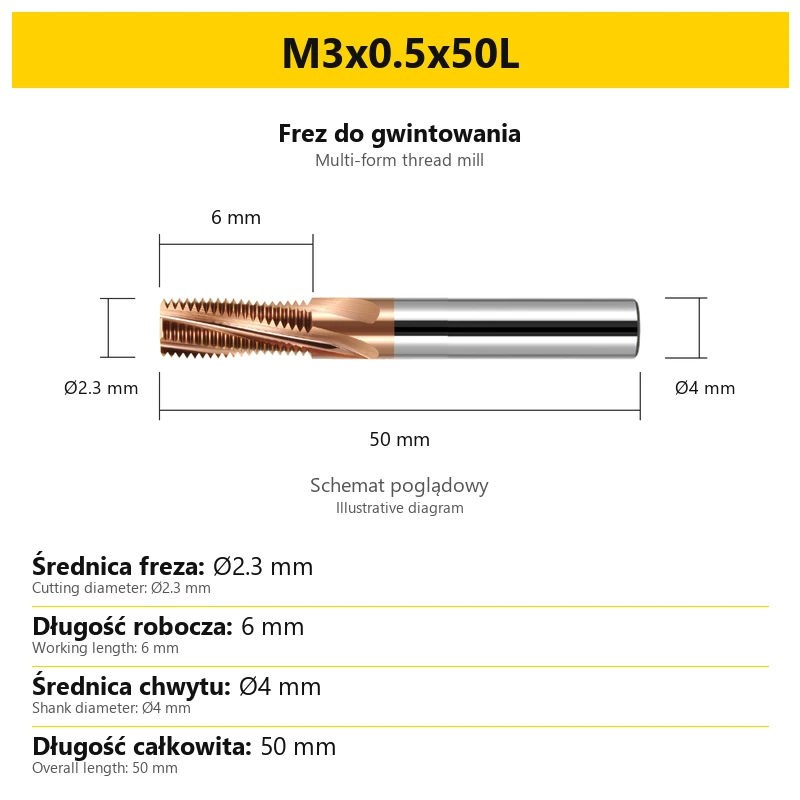
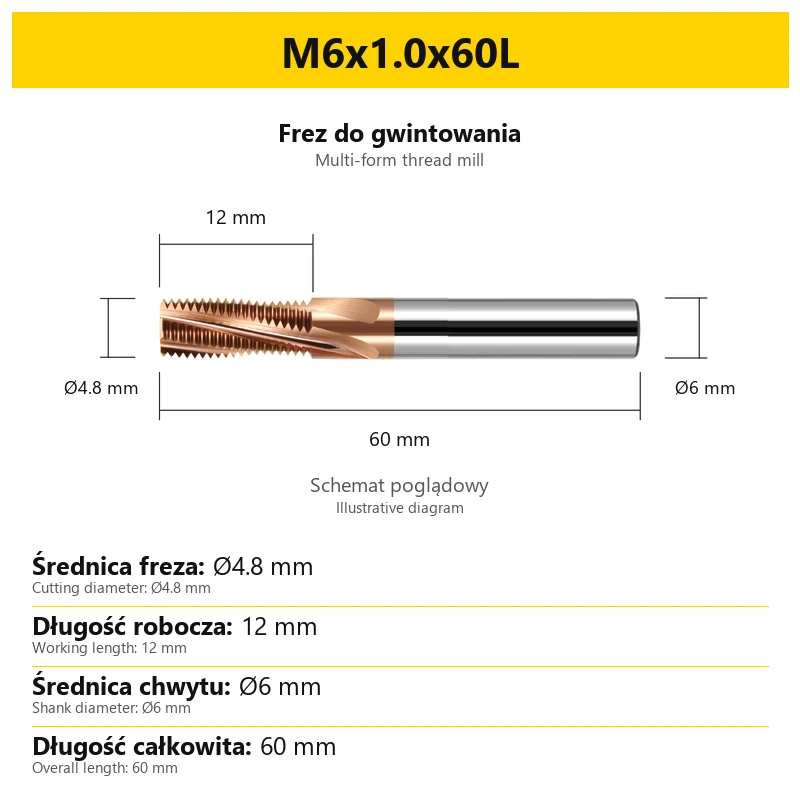
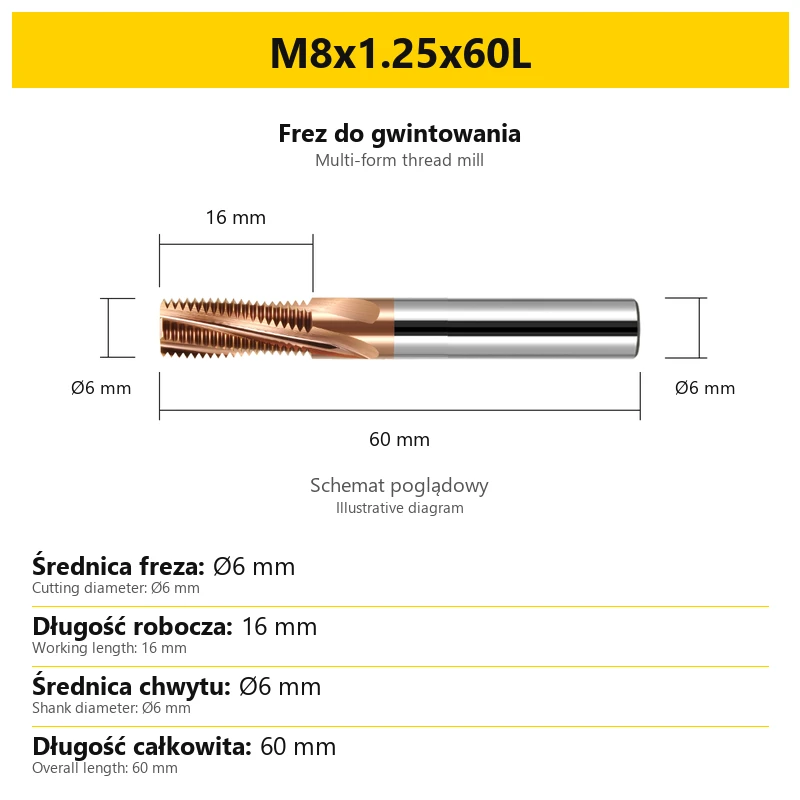
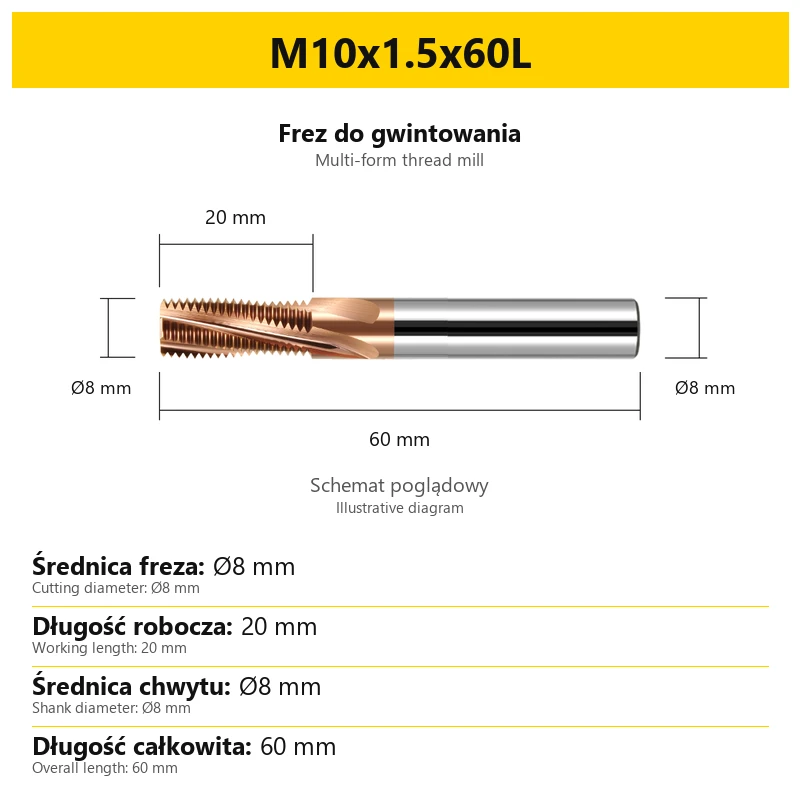
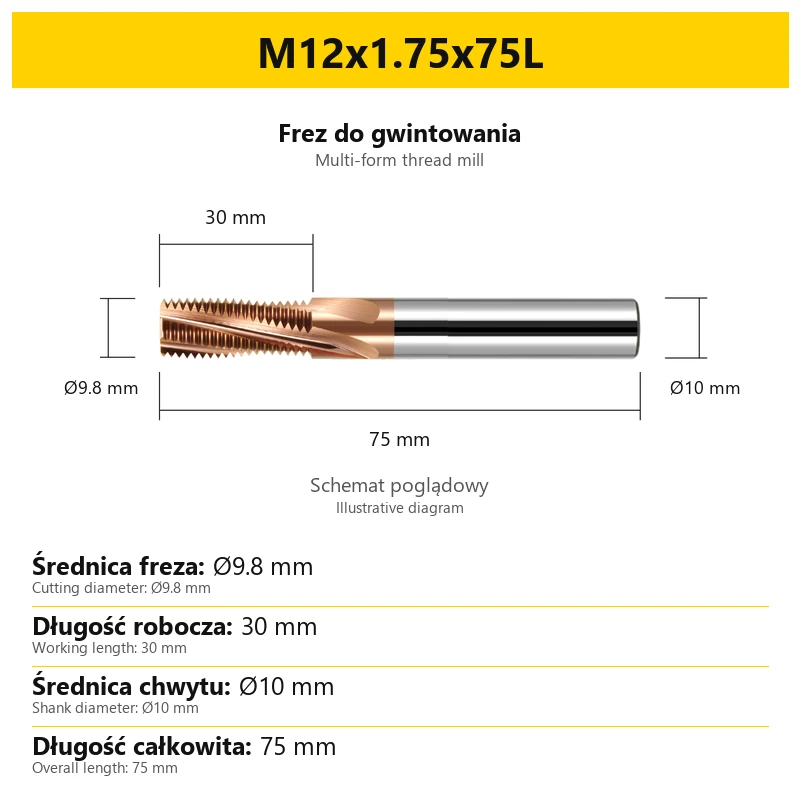
Example: M3x0.5x50L. The code states the thread size, thread pitch and overall tool length. A dot is the decimal separator. Linear dimensions on the variant cards are expressed in millimetres.
| Code element | Meaning |
|---|---|
| M3 | Metric thread with a nominal diameter of 3 mm |
| 0.5 | Thread pitch of 0.5 mm |
| 50L | Overall cutter length of 50 mm |
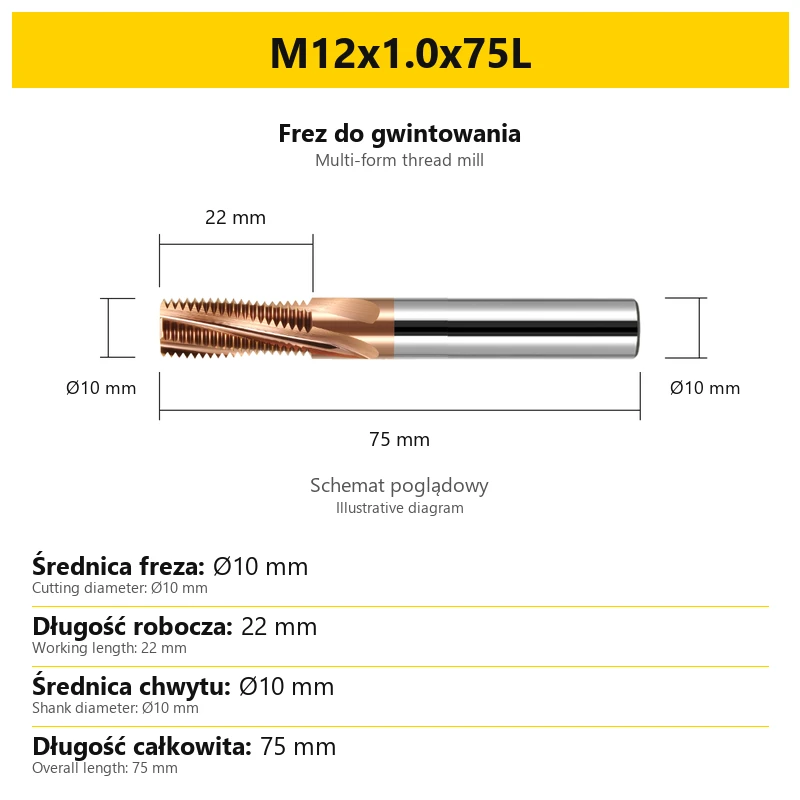
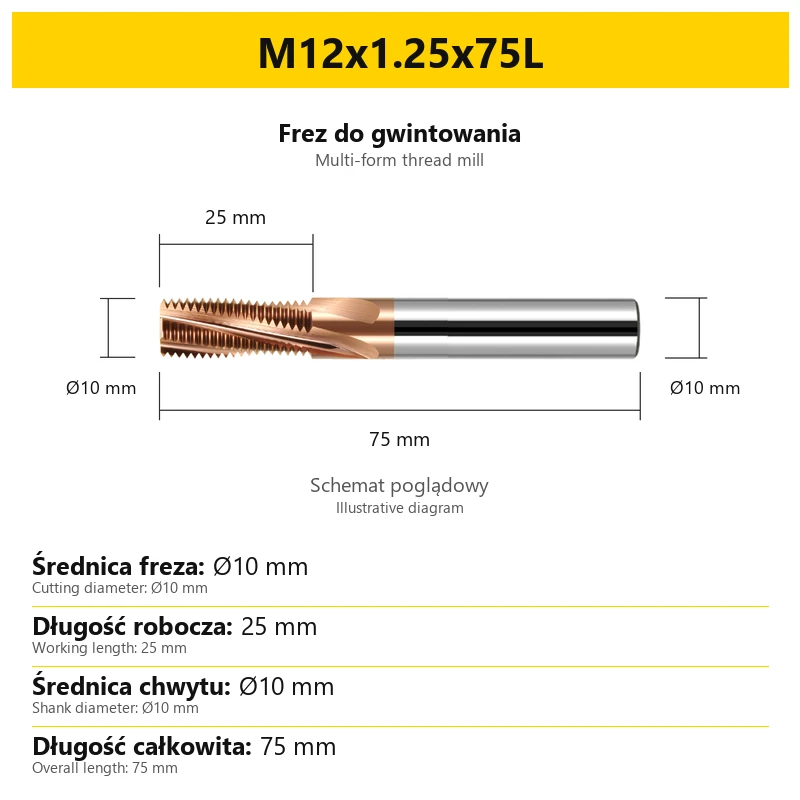
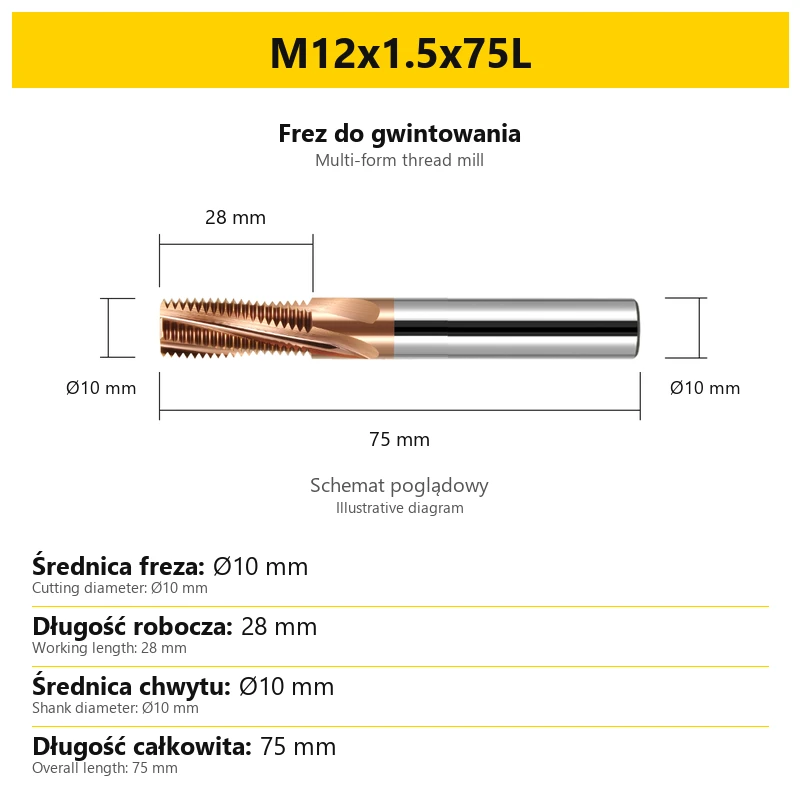
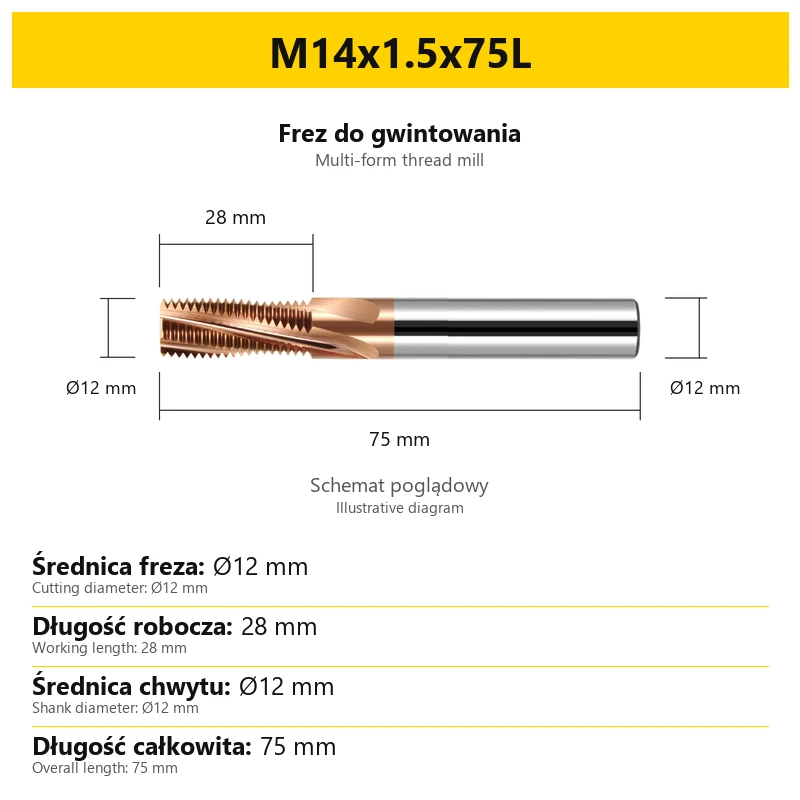
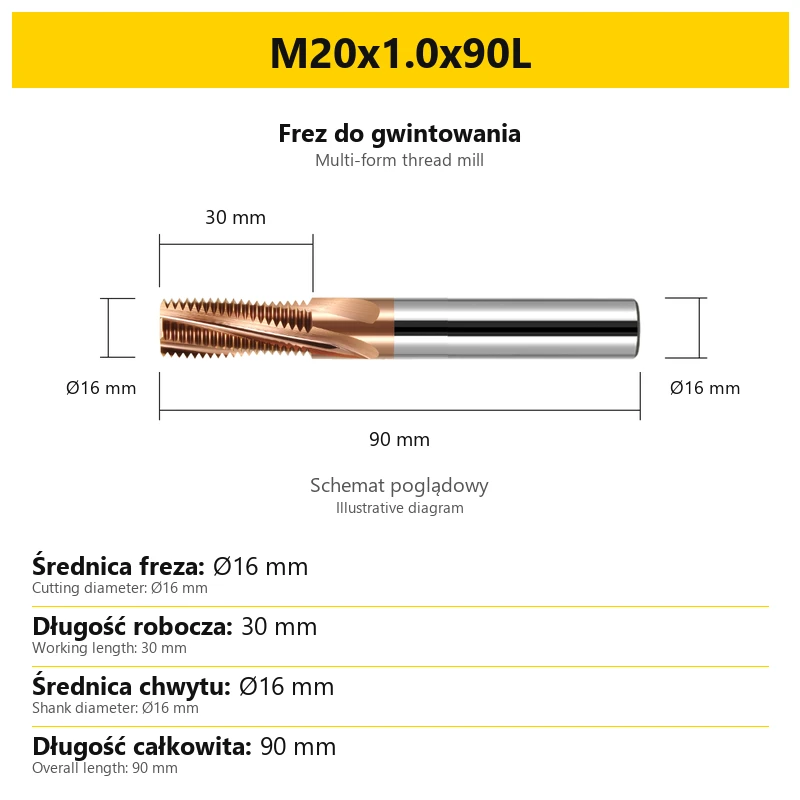
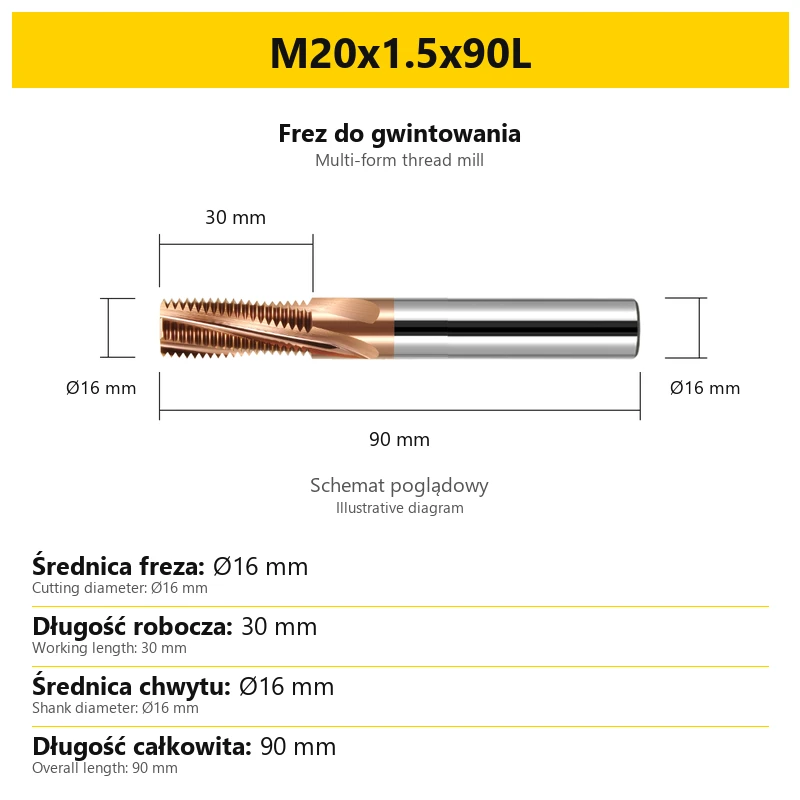
For this example, the cutting diameter is Ø2.3 mm, the working length is 6 mm and the shank diameter is Ø4 mm. The number after M is neither the cutting diameter nor the toolholding diameter. Read each dimension separately.
Dimensions on the variant card
| Dimension | Use during selection |
|---|---|
| Cutting diameter | Diameter of the cutting section. Use it to check access to the thread area and prepare the tool path. |
| Working length | Length of the thread-forming section. Consider it when checking the required thread length and space for entry and exit. |
| Shank diameter | Toolholding diameter. Select the holder to match this dimension independently of the M designation. |
| Overall length L | Length of the complete cutter, including the shank. It is not the permissible thread depth. |
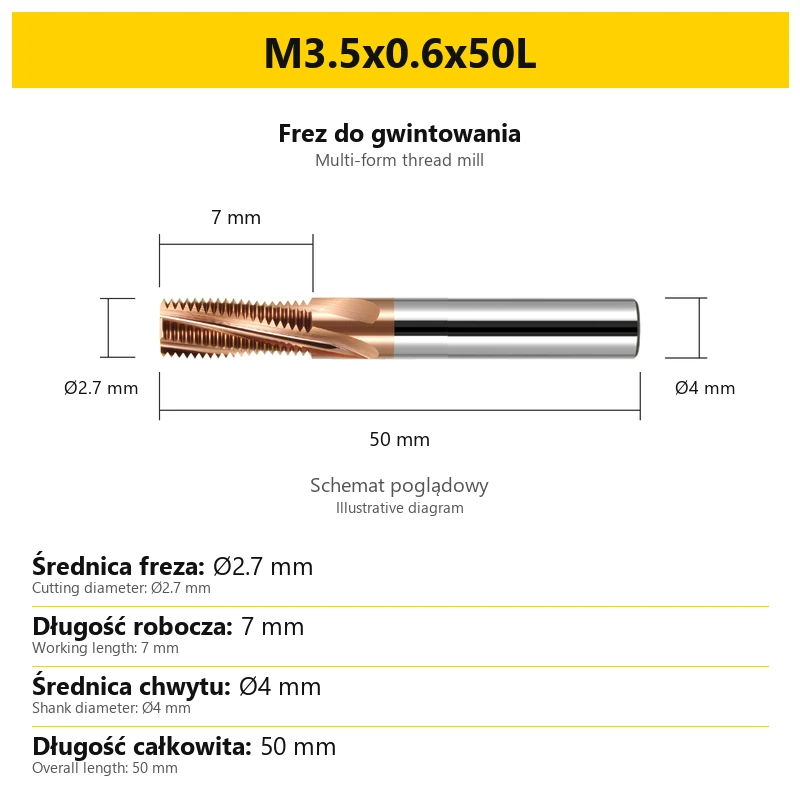
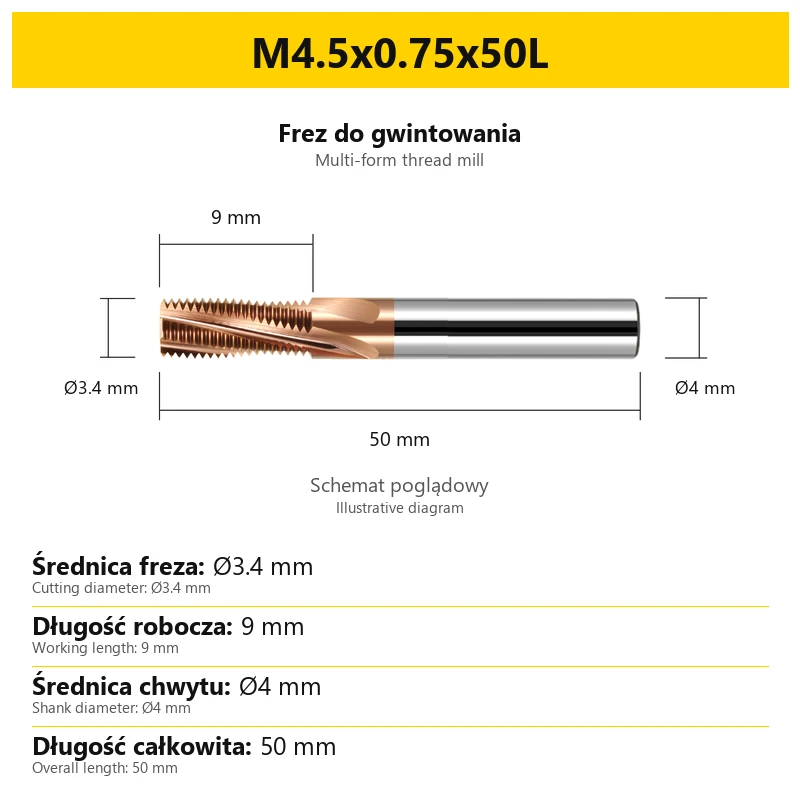
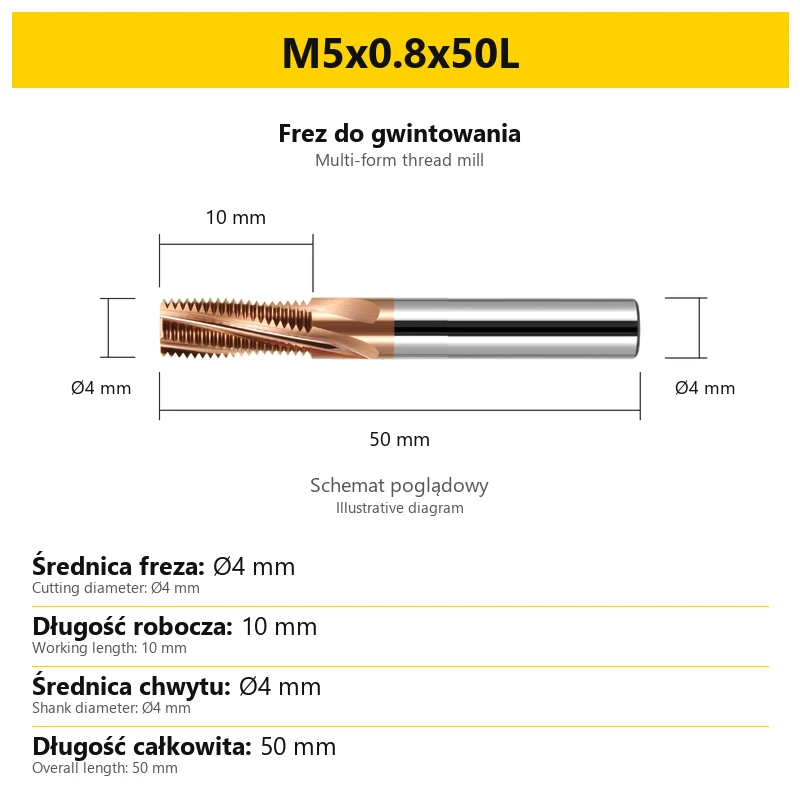
The image on the card is illustrative: the values assigned to the selected variant define its dimensions. Across the range, cutting diameters extend from Ø1.54 to Ø16 mm and working lengths from 4 to 42 mm. The range does not contain every possible combination of these values.
Selecting a variant for the component
- Read the thread diameter and pitch. Choose a variant matching both values on the component drawing.
- Compare the working length with the task. Check the thread length, entry and exit space and possible working-section collisions.
- Check the shank diameter. Select the correct toolholding size and allow for the holder dimensions.
- Select overall length for access. Keep the overhang as short as the operation allows.
A longer tool does not necessarily have a proportionally longer thread-forming section. For example, 120L states the overall tool length; working length is specified separately. Compare the complete card before choosing a size instead of relying on one number in the name.
Toolholding and machining preparation
- Check the cutter and holder. Clean the clamping surfaces, inspect the cutting edges and check runout after mounting.
- Verify the program. Check the pitch, cutter diameter, helical path and entry and exit movements.
- Check clearances. Account for the working section, shank, holder and component geometry throughout the operation.
- Select suitable conditions. Consider the material, cutting diameter, working length, overhang and setup rigidity.
After machining the first component, inspect the thread using the inspection method specified for the part. If vibration or surface deterioration occurs, check toolholding, runout, chip removal and tool load before continuing the batch.
Frequently asked questions
Can pitch be changed through the program alone?
No. The spacing of the profiles on this cutter is fixed. A different pitch requires a variant with matching geometry.
Does the M designation specify shank diameter?
No. M identifies the nominal thread size. Shank diameter is given in a separate row on the card.
Does 120L mean a thread length of 120 mm?
No. It is the complete tool length. Assess usable reach from the working section, toolholding and component geometry.
Does full-profile specify a flute count?
No. It describes multiple thread forms along the cutter axis, not the number of flutes around its circumference.
Product safety
Manufacturer
Kortools Kamil Henkelman
Tysiąclecia 41B
41-933 Bytom, Poland
Responsible person in the EU
Kamil Henkelman
TYSIĄCLECIA, 41B
41-933 Bytom, Poland
Related products
-
07B7-296CFBestseller
 Thread Mills 0.00
Thread Milling Cutter M0.8-M20 - Single Flute TiSiN
-
07B7-296CF_2Bestseller
 Thread Mills 0.00
Thread Milling Cutter M0.8-M20 - Single Flute DLC


Bestsellers
-
Bestseller
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.86Price €56.79without VAT -
Bestseller
Kortools Adhesive + Tape CNC Workholding Kit
Yellow tape 5cm x 50m; adhesive 100g Yellow tape 5cm x 50m; adhesive 500g Yellow tape 10cm x 50m; adhesive 100g Yellow tape 10cm x 50m; adhesive 500g Green tape 5cm x 50m; adhesive 100g + 7 morePrice €44.66Price €36.31without VAT -
Price €17.18Price €13.97without VAT
-
Price €7.10Price €5.77without VAT
-
Price €7.56Price €6.14without VAT
-
Bestseller
 Other Accessories 0.00
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.82Price €43.76without VAT -
Bestseller
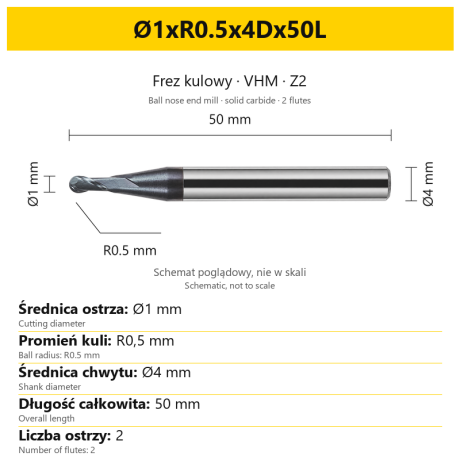 Ball Nose End Mills 0.00
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.14Price €8.25without VAT -
Bestseller
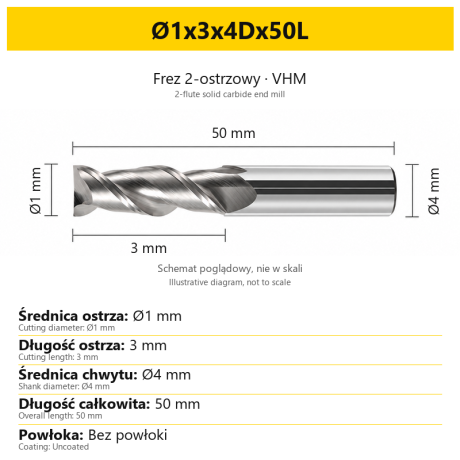 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.35Price €4.35without VAT -
Bestseller
 2-Flute End Mills 0.00
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.40Price €3.58without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.89Price €6.41without VAT -
Bestseller
 2-Flute End Mills 0.00
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.99Price €6.50without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.28Price €5.92without VAT -
Bestseller
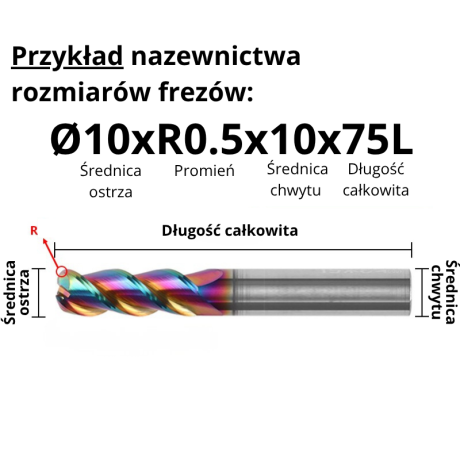
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €4.96Price €4.04without VAT -
Bestseller
 3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.10Price €4.15without VAT -
Bestseller

 Countersinks 0.00
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.81Price €3.91without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.07Price €4.12without VAT


