


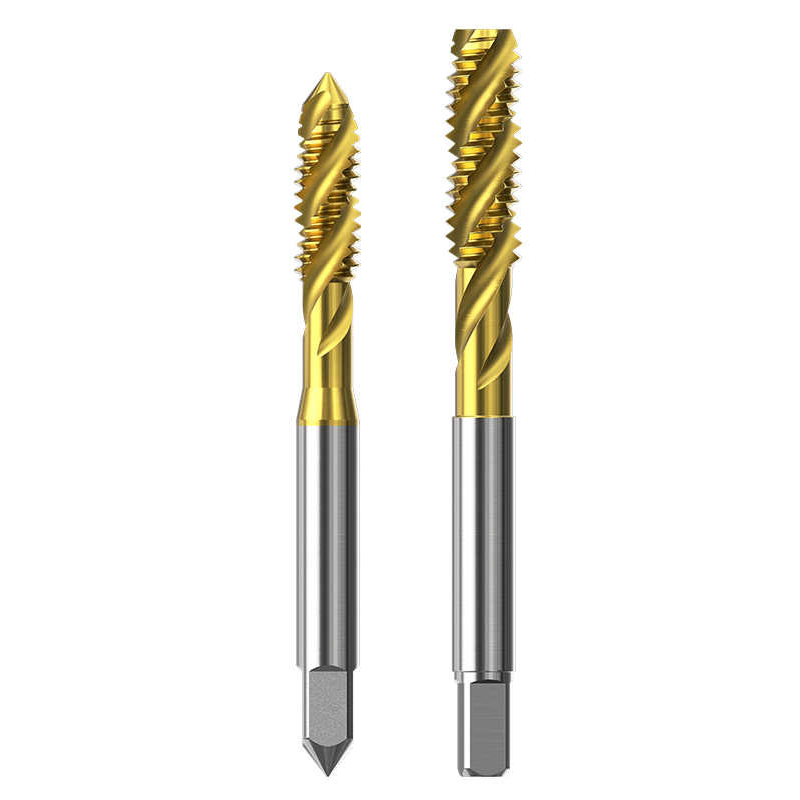
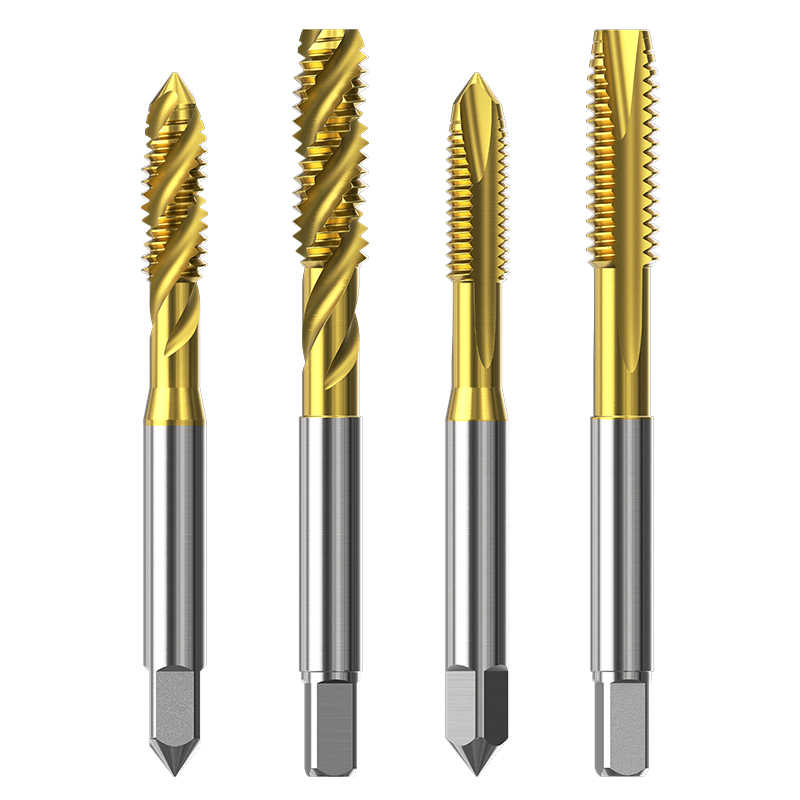
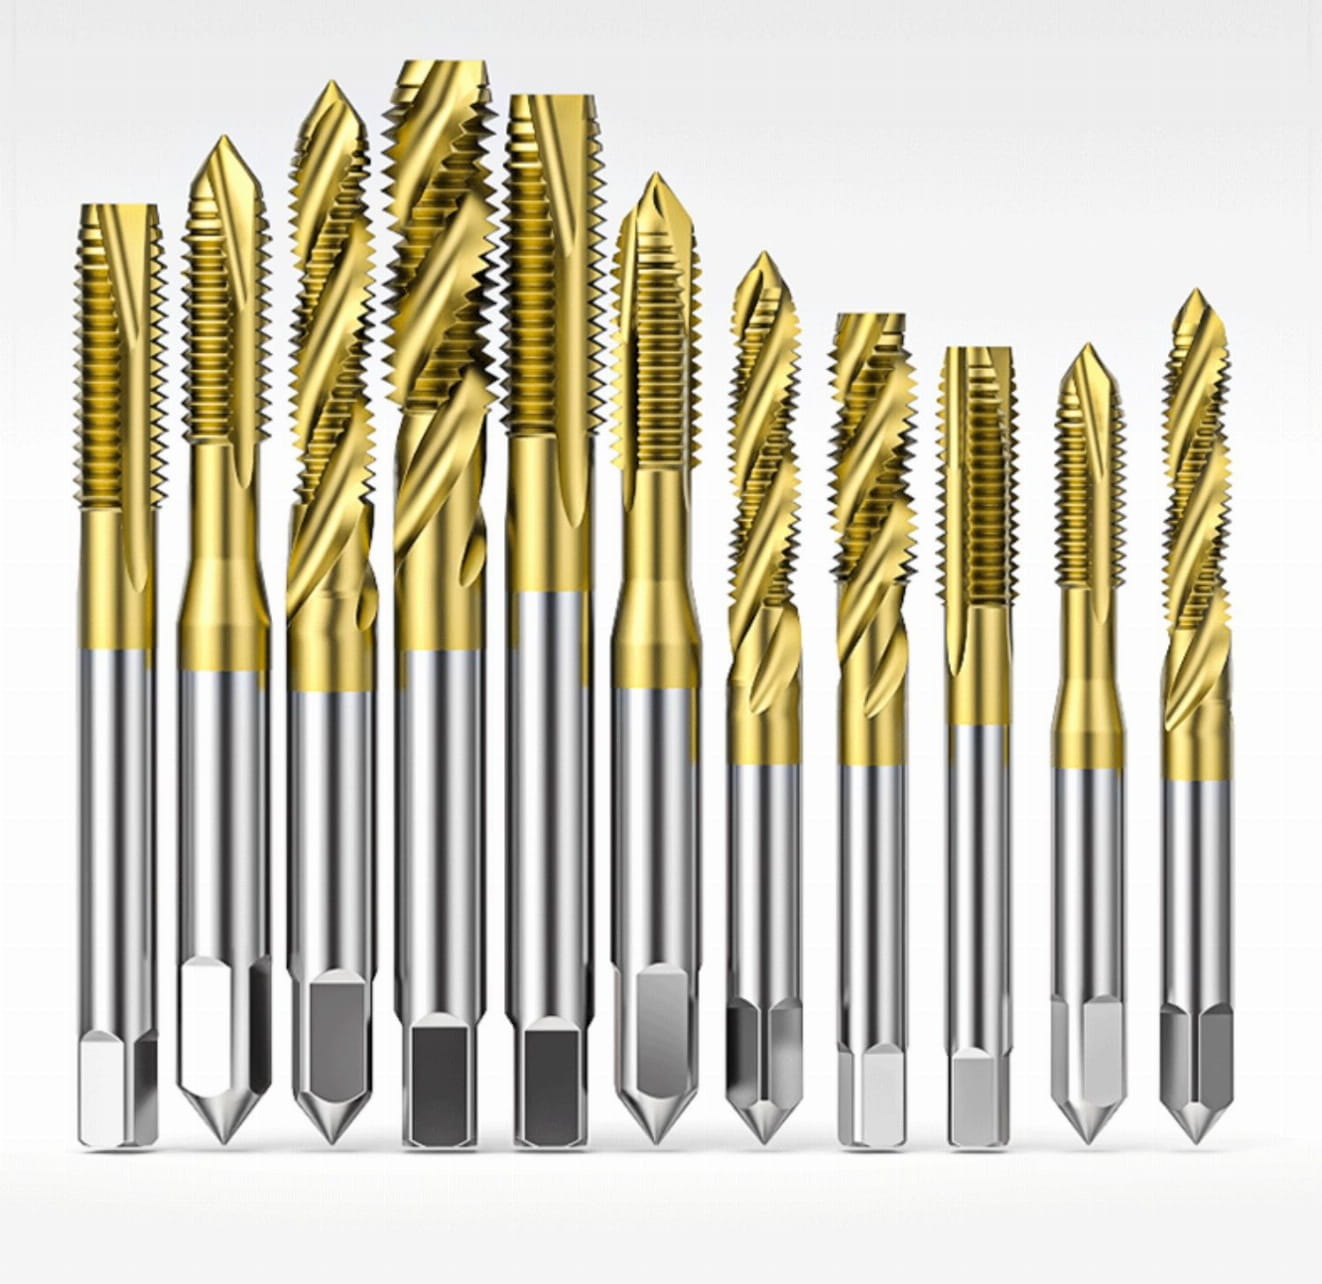



Spiral Flute Machine Tap HSSE - TiN Coated M2-M30 ISO
Shipping costs are not included in the price.
Shipping costs are not included in the price.
Ask about the product

The administrator of personal data is Kortools. We process it to respond to your inquiry. More information regarding the processing of personal data can be found in privacy policy.
Select a product variant:
Individual variants may differ in price
Product code: 0E7E-8579B
Product description
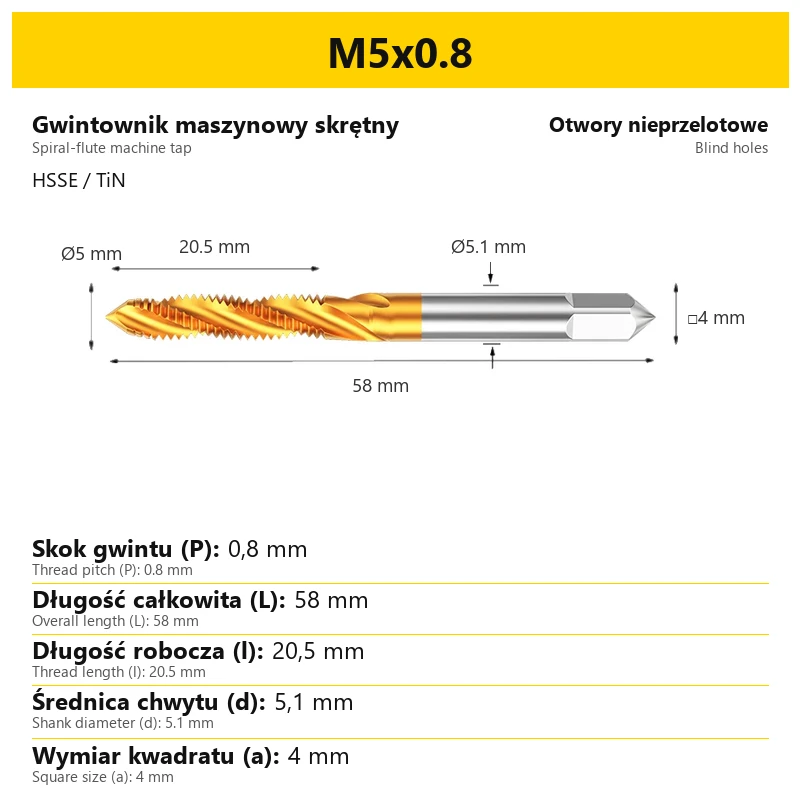
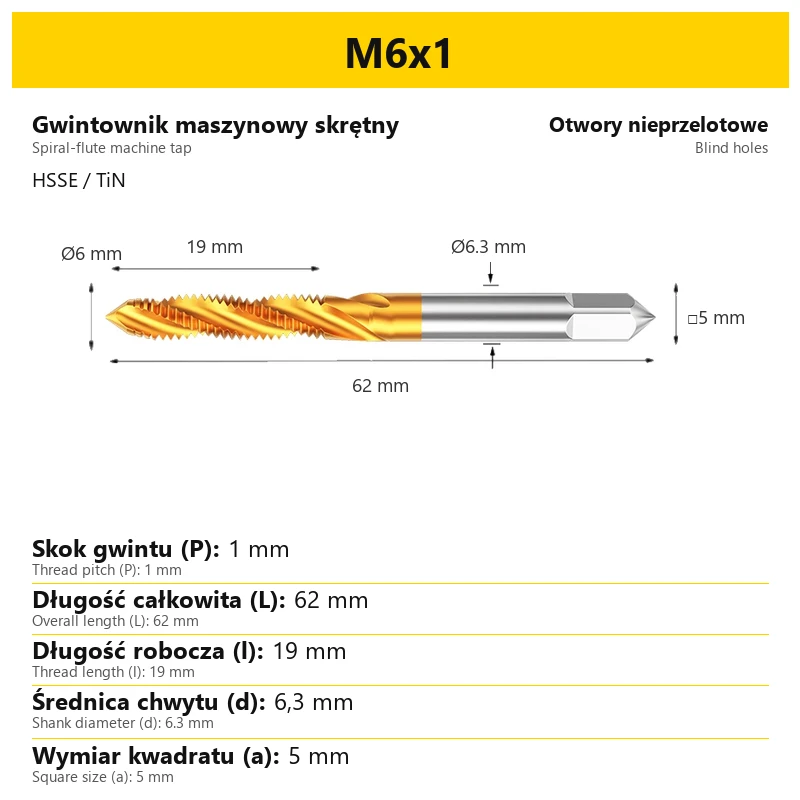
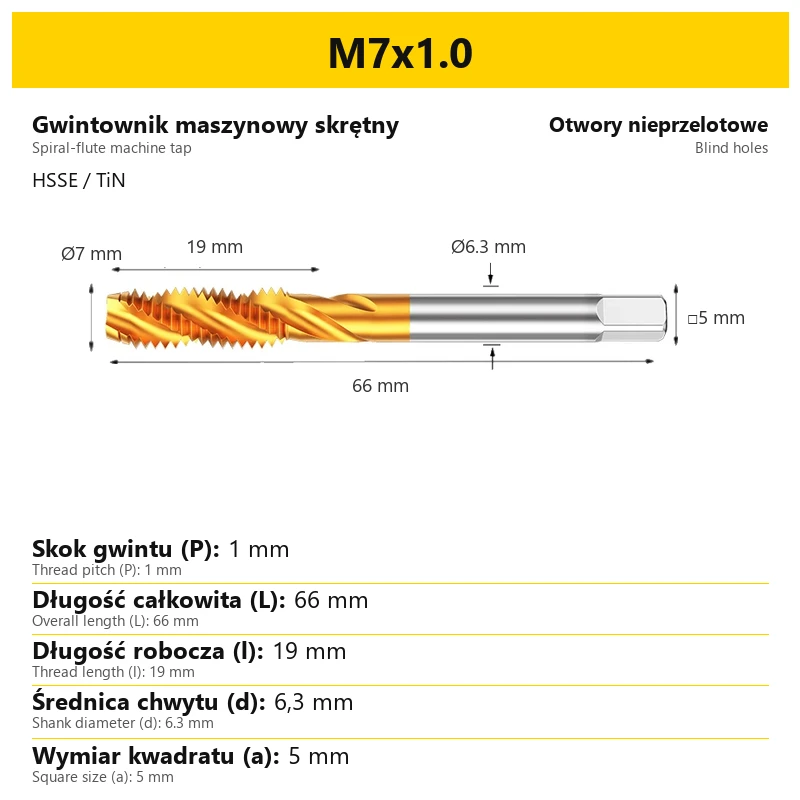
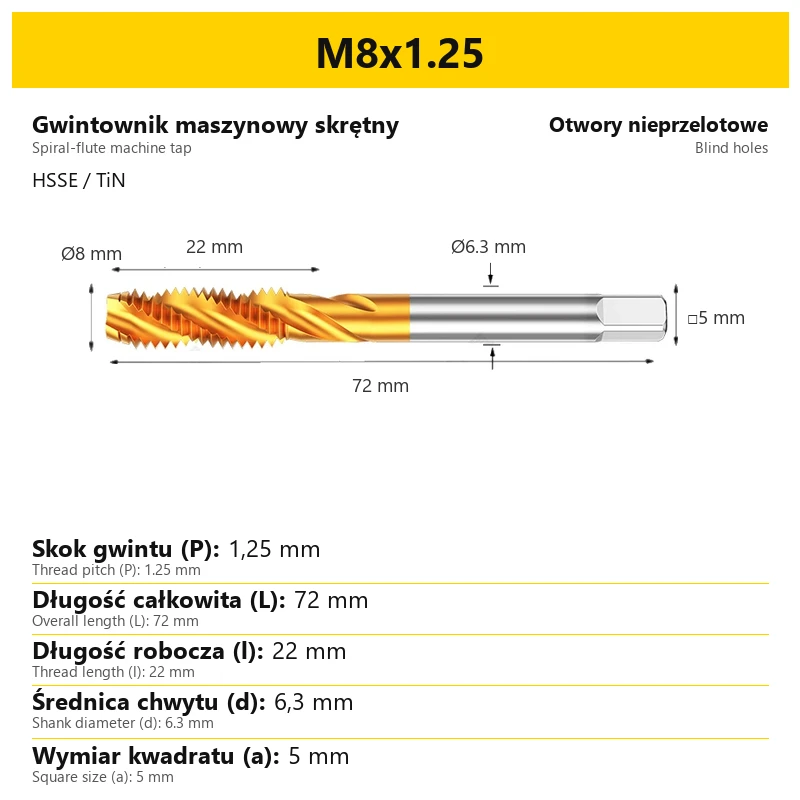
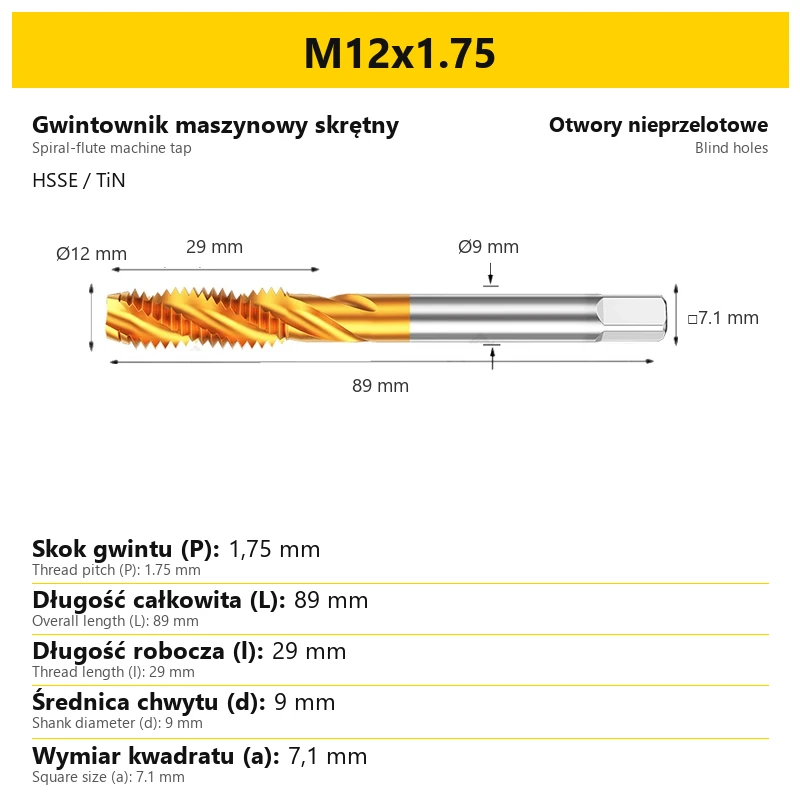
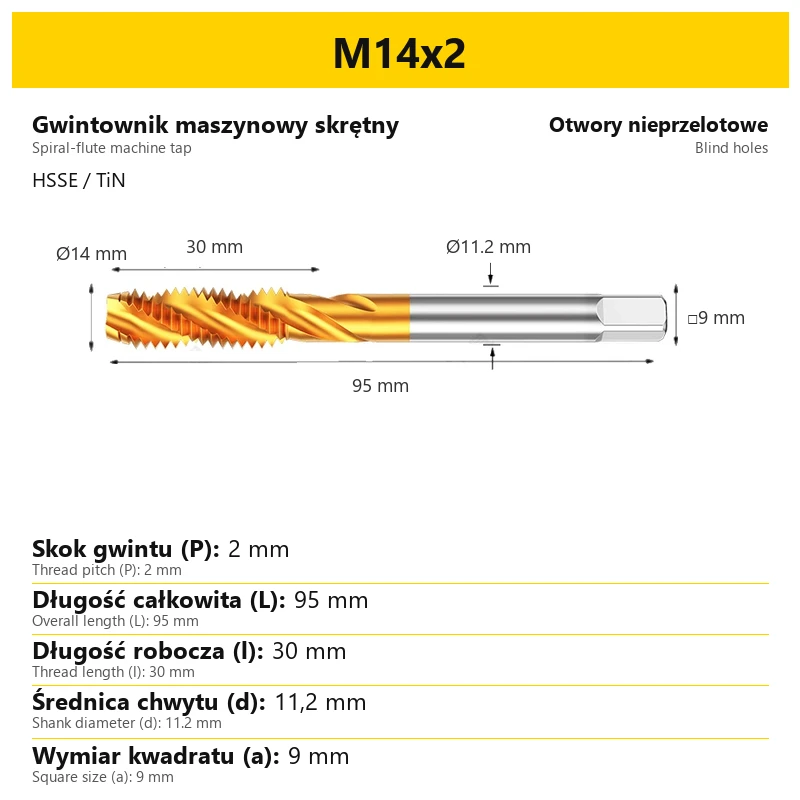
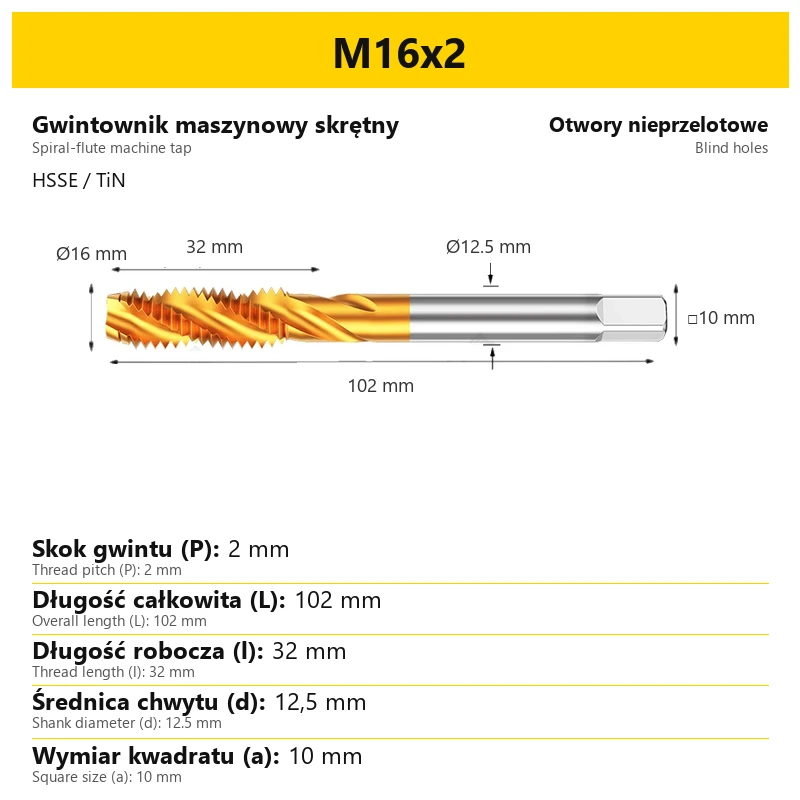
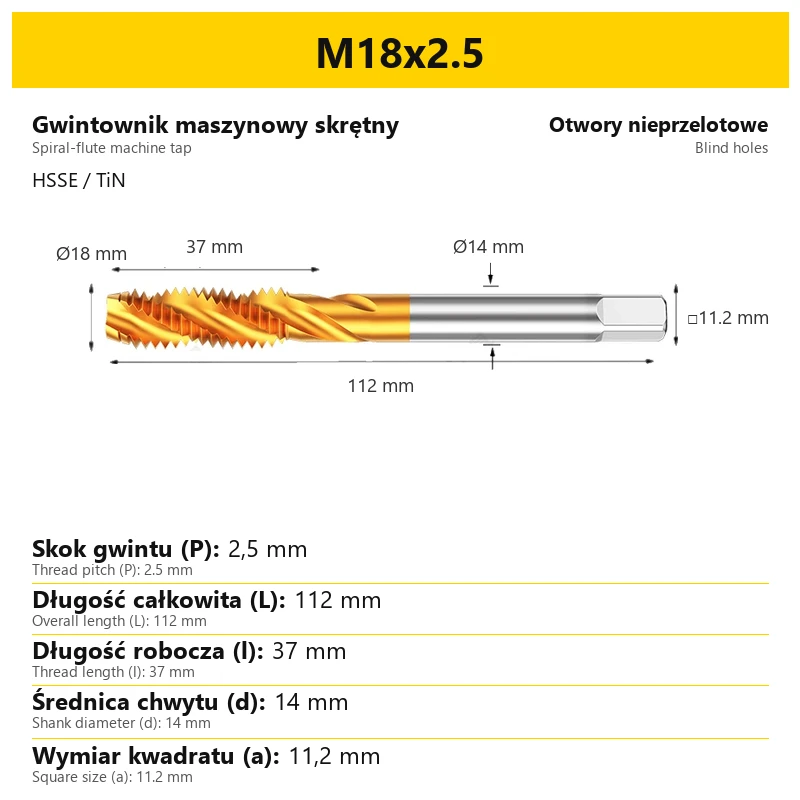
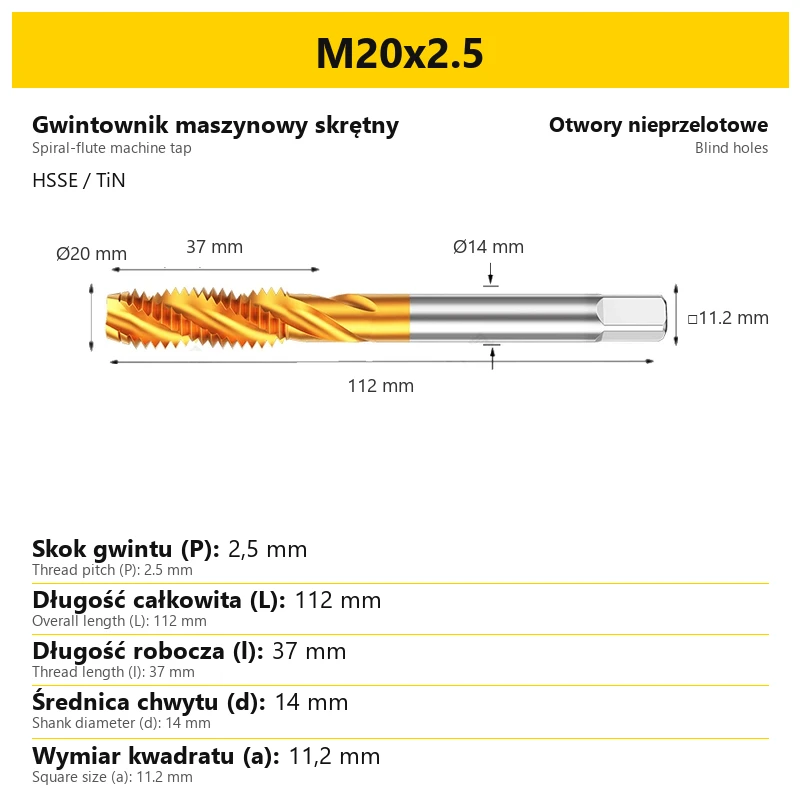
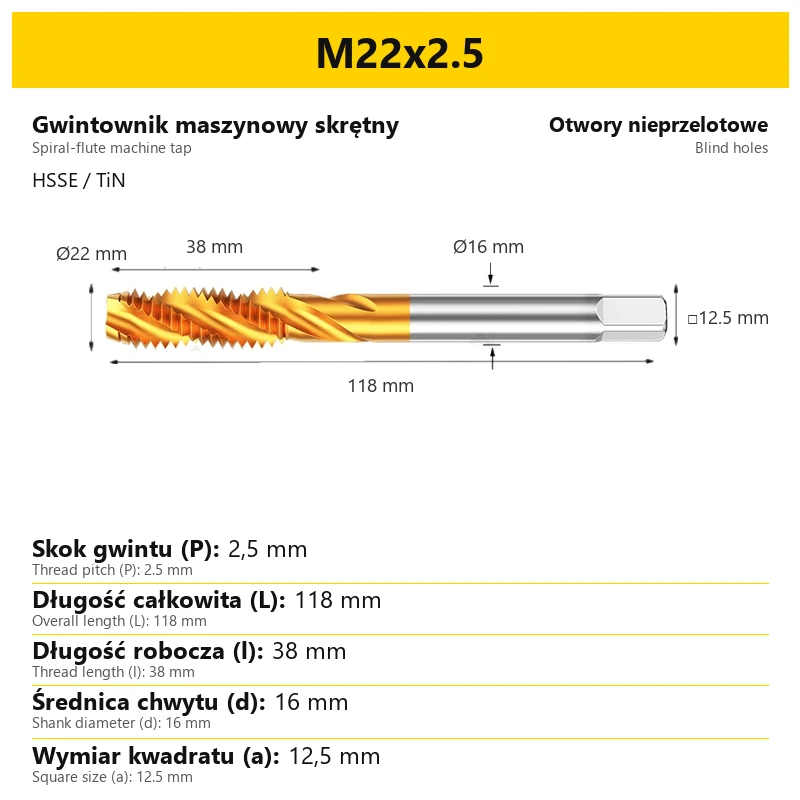
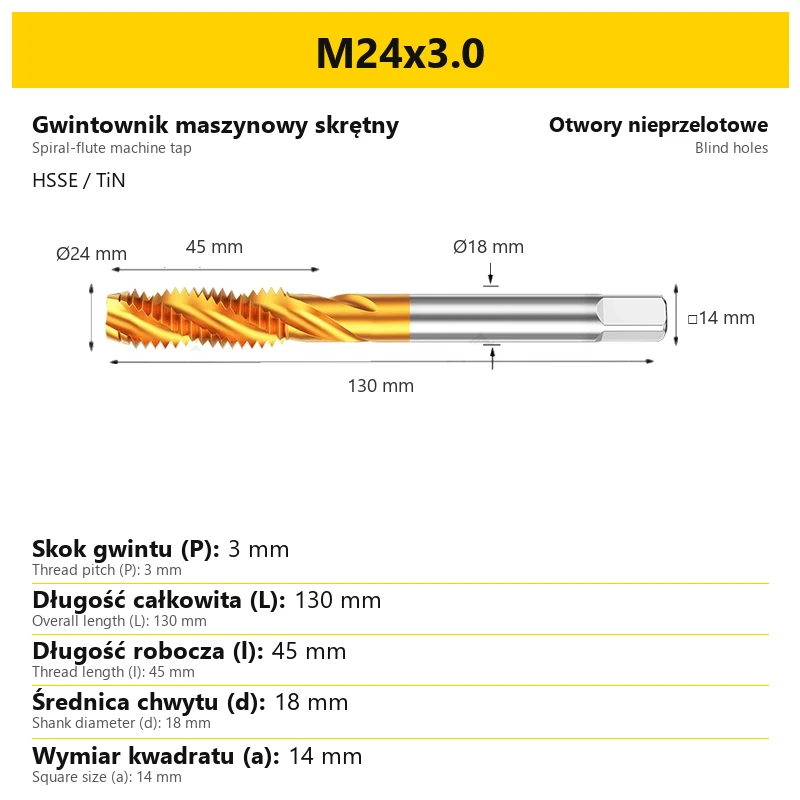
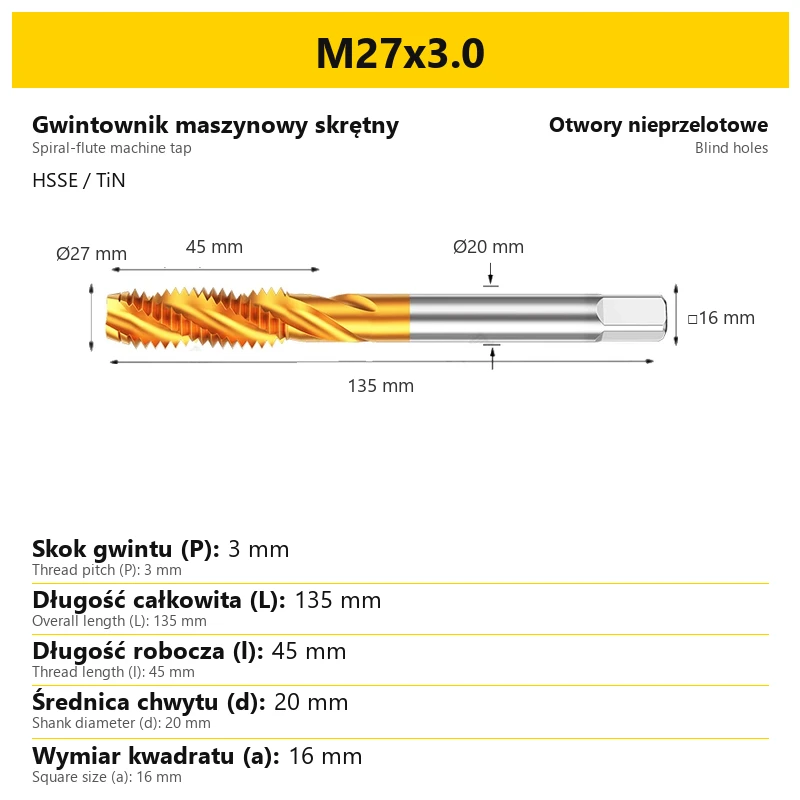
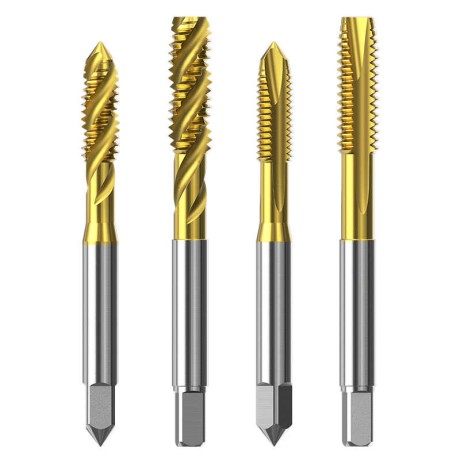
Machine tap for cutting metric threads in steel and stainless steel. The spiral-flute SP version is intended for blind holes.
Technical specifications
- Material: HSSE — cobalt-alloyed high-speed steel
- Coating: TiN — titanium nitride
- Thread type: Metric M
- Application: Blind holes
- Threading depth range: Up to 3 × D
- Sales unit: 1 piece
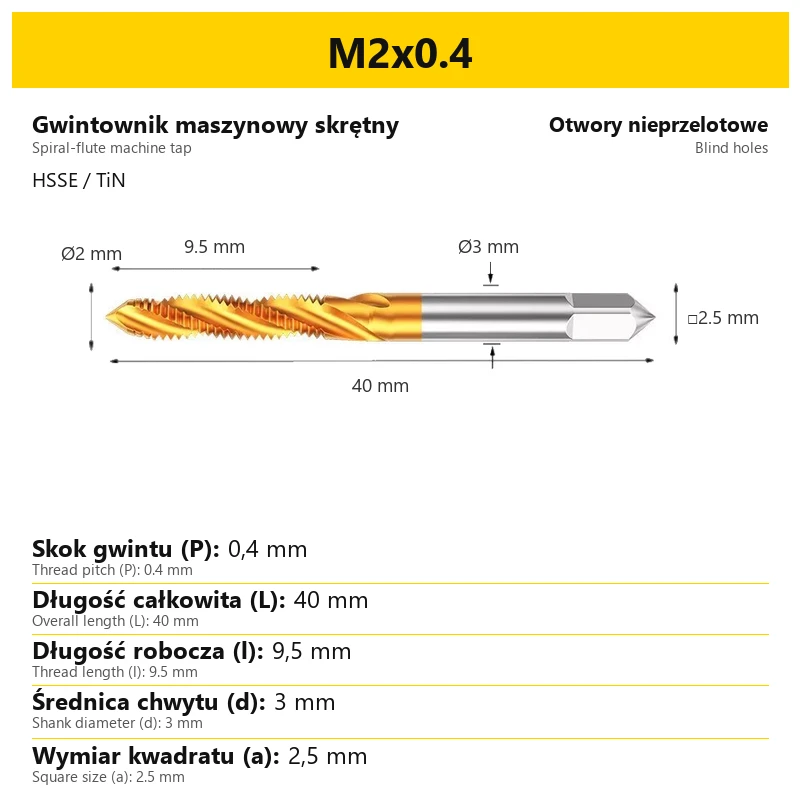
Variant dimensions
| Size | Pitch P [mm] | Overall length L [mm] | Thread length l [mm] | Shank d [mm] | Square a [mm] |
|---|---|---|---|---|---|
| M2x0.4 | 0.4 | 40 | 9.5 | Ø3 | 2.5 |
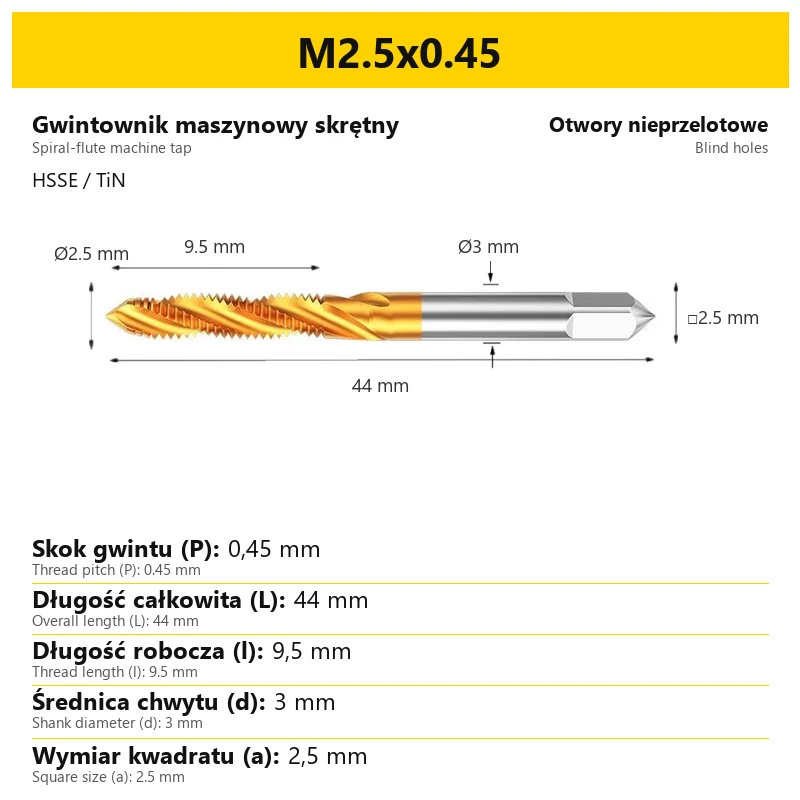
| M2.5x0.45 | 0.45 | 44 | 9.5 | Ø3 | 2.5 |
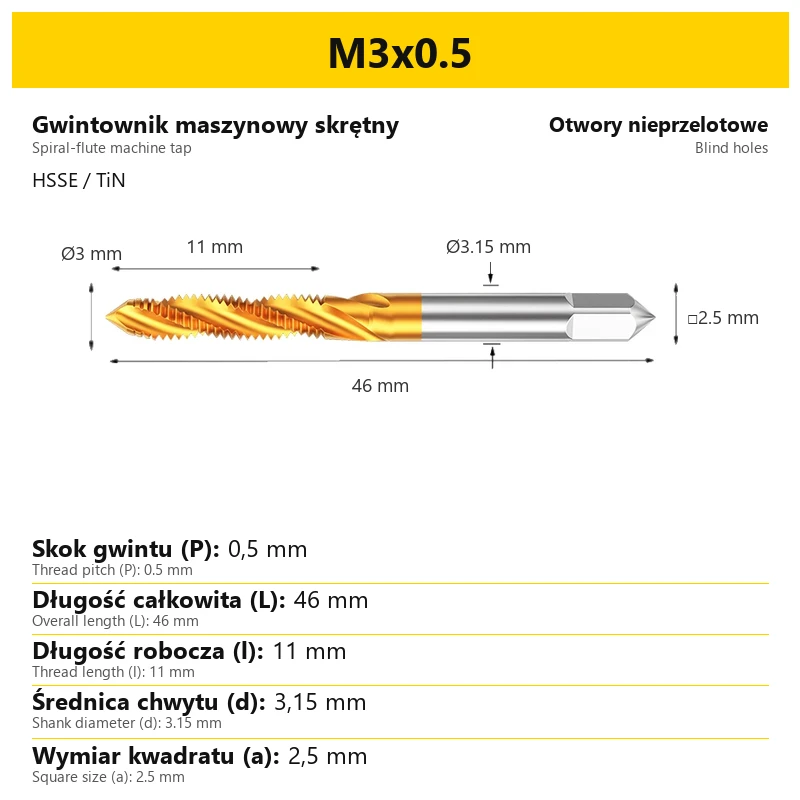
| M3x0.5 | 0.5 | 46 | 11 | Ø3.15 | 2.5 |
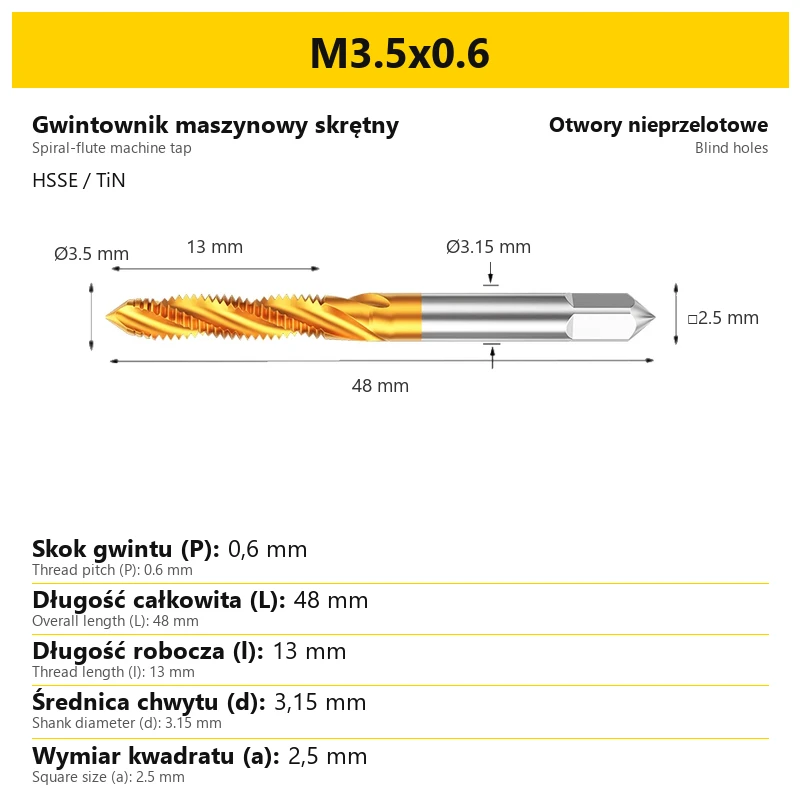
| M3.5x0.6 | 0.6 | 48 | 13 | Ø3.15 | 2.5 |
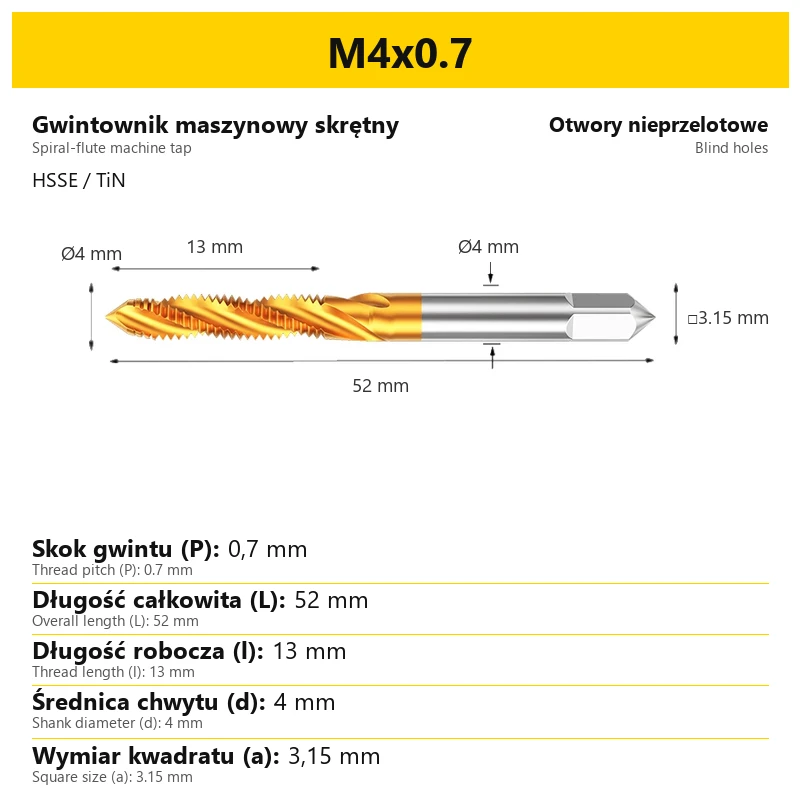
| M4x0.7 | 0.7 | 52 | 13 | Ø4 | 3.15 |
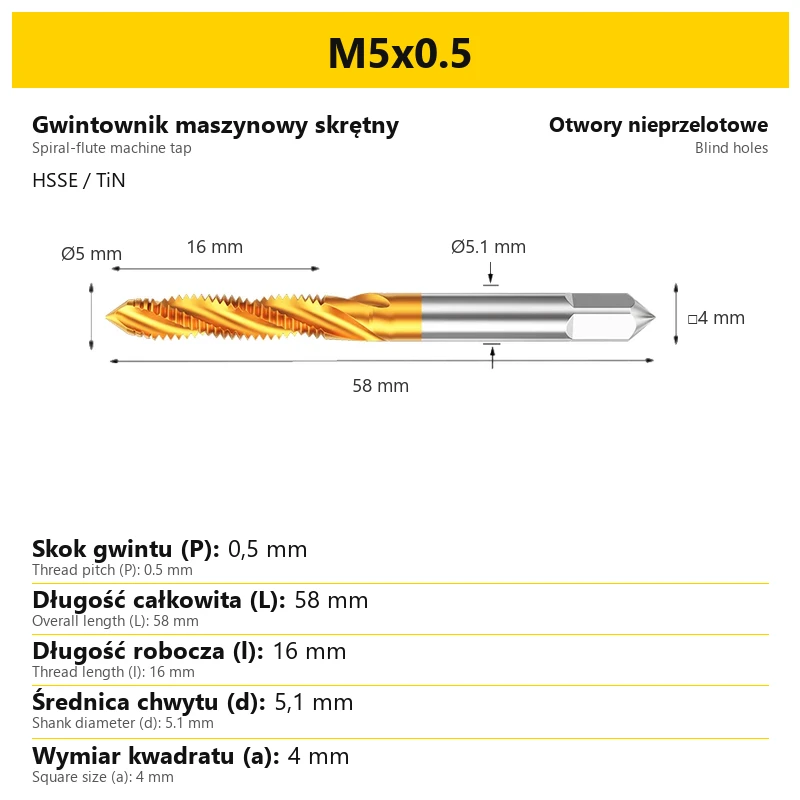
| M5x0.5 | 0.5 | 58 | 16 | Ø5.1 | 4 |
| M5x0.8 | 0.8 | 58 | 20.5 | Ø5.1 | 4 |
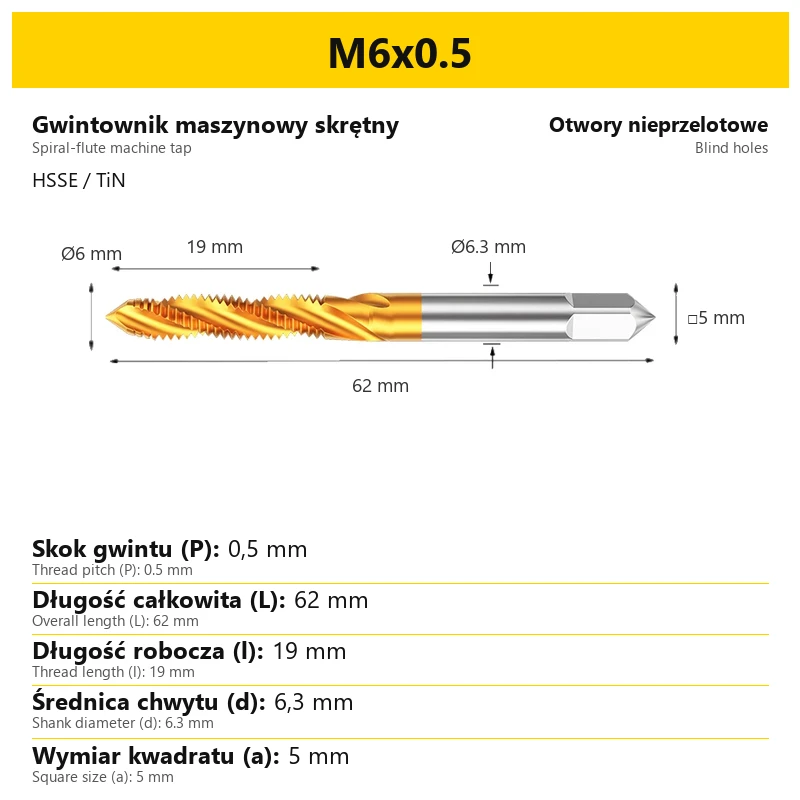
| M6x0.5 | 0.5 | 62 | 19 | Ø6.3 | 5 |
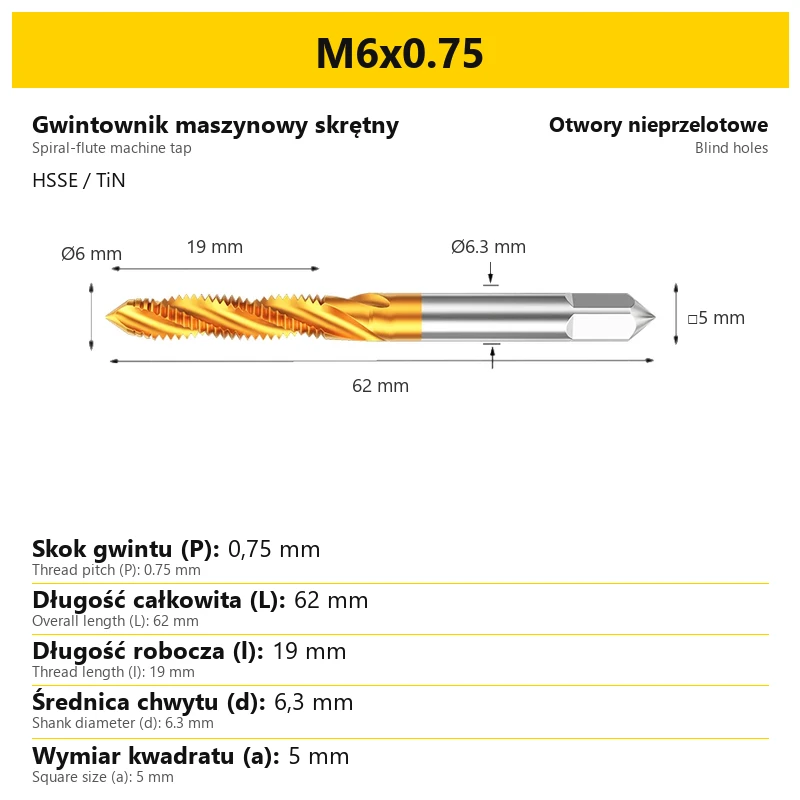
| M6x0.75 | 0.75 | 62 | 19 | Ø6.3 | 5 |
| M6x1 | 1 | 62 | 19 | Ø6.3 | 5 |
| M7x1.0 | 1 | 66 | 19 | Ø6.3 | 5 |
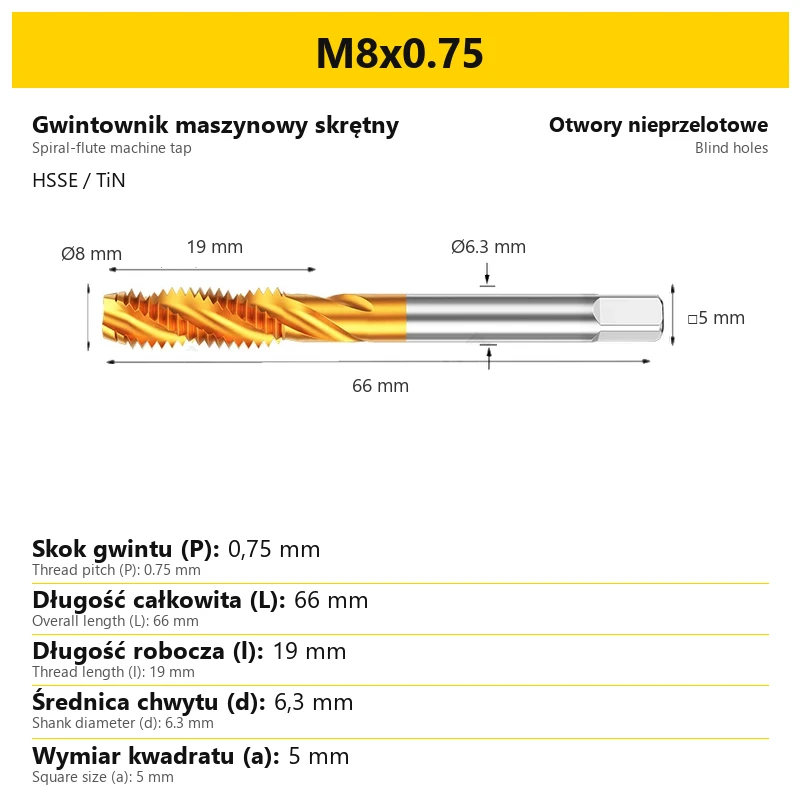
| M8x0.75 | 0.75 | 66 | 19 | Ø6.3 | 5 |
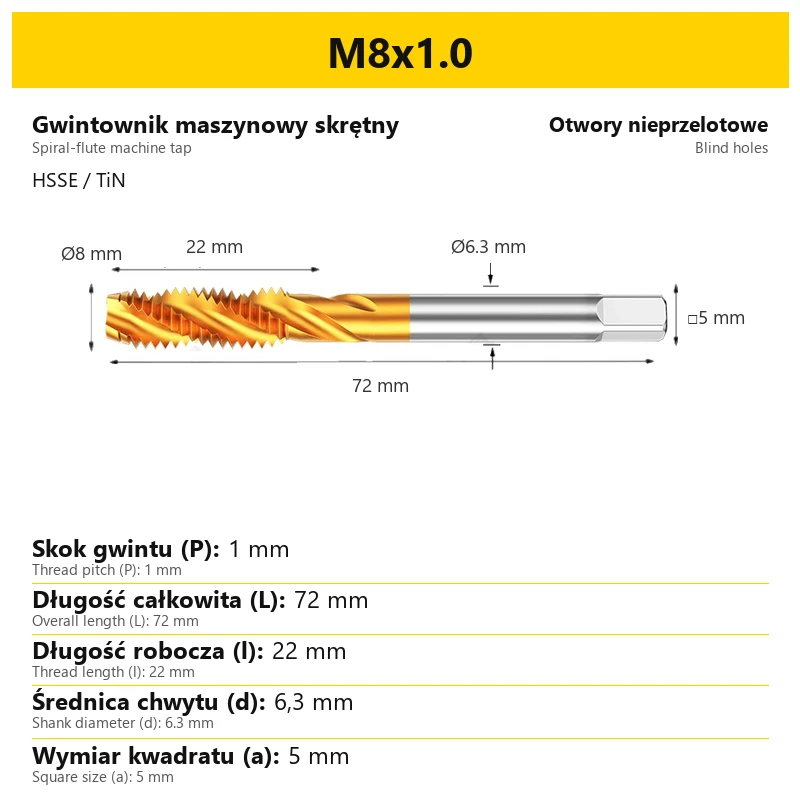
| M8x1.0 | 1 | 72 | 22 | Ø6.3 | 5 |
| M8x1.25 | 1.25 | 72 | 22 | Ø6.3 | 5 |
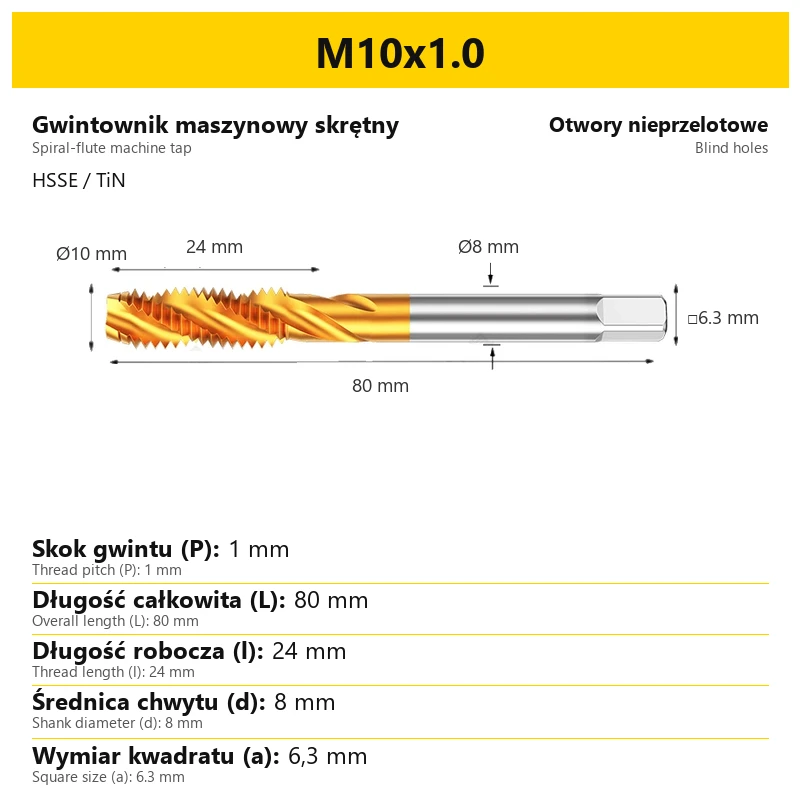
| M10x1.0 | 1 | 80 | 24 | Ø8 | 6.3 |
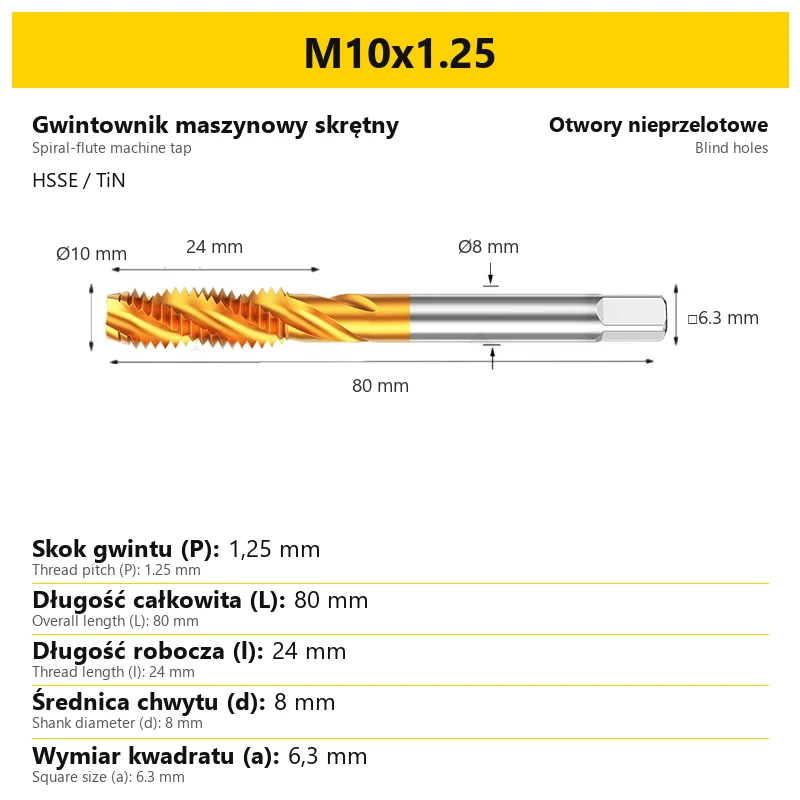
| M10x1.25 | 1.25 | 80 | 24 | Ø8 | 6.3 |
| M10x1.5 | 1.5 | 80 | 24 | Ø8 | 6.3 |
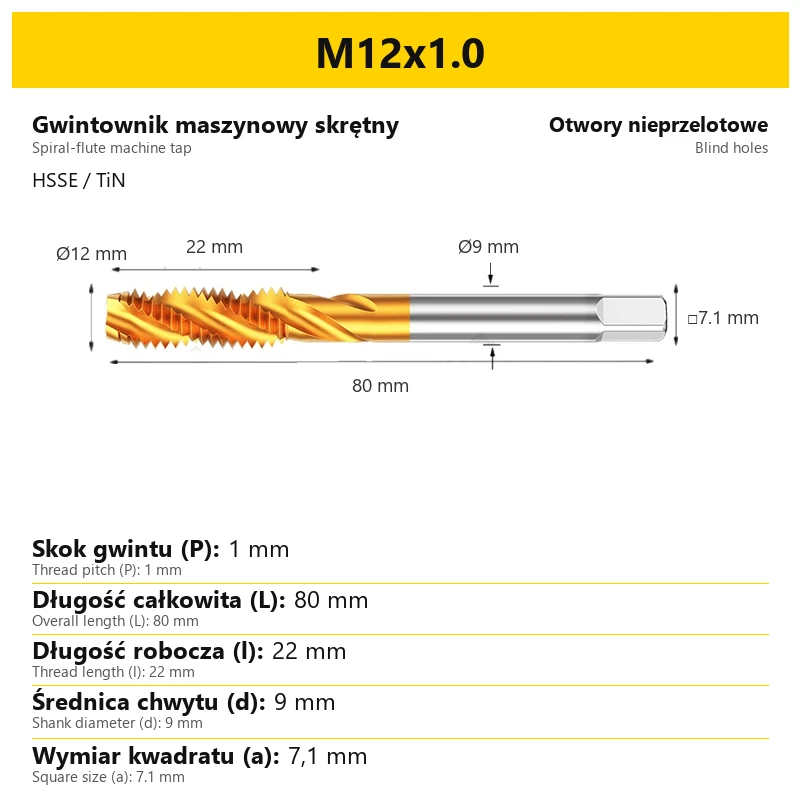
| M12x1.0 | 1 | 80 | 22 | Ø9 | 7.1 |
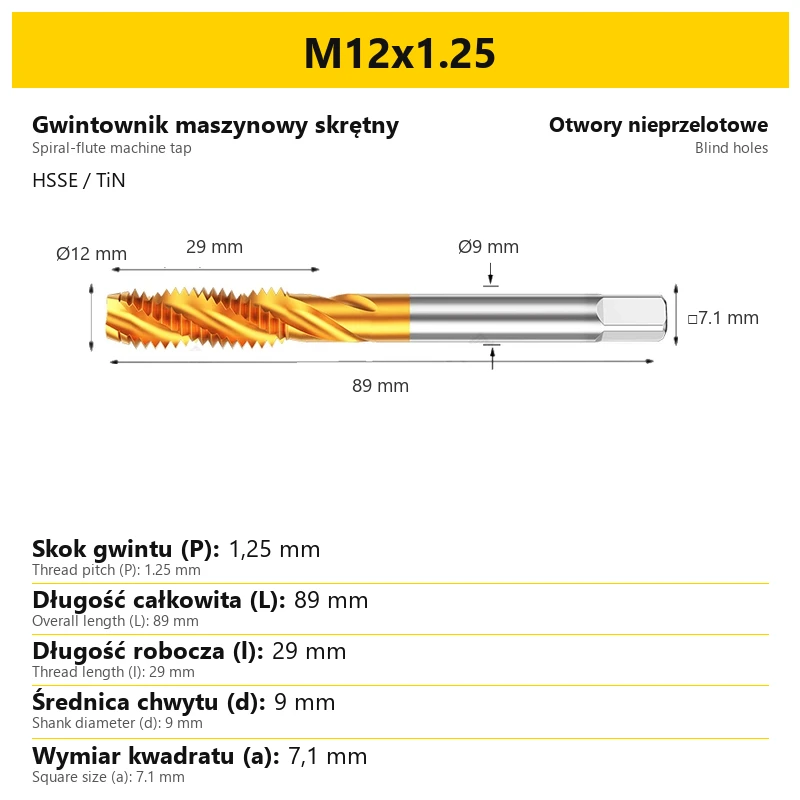
| M12x1.25 | 1.25 | 89 | 29 | Ø9 | 7.1 |
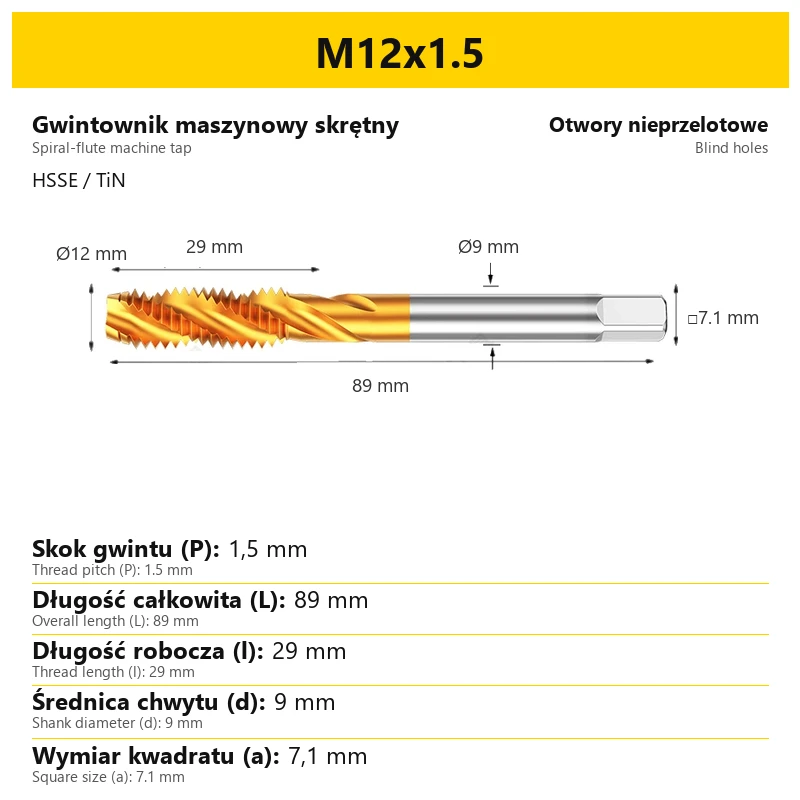
| M12x1.5 | 1.5 | 89 | 29 | Ø9 | 7.1 |
| M12x1.75 | 1.75 | 89 | 29 | Ø9 | 7.1 |
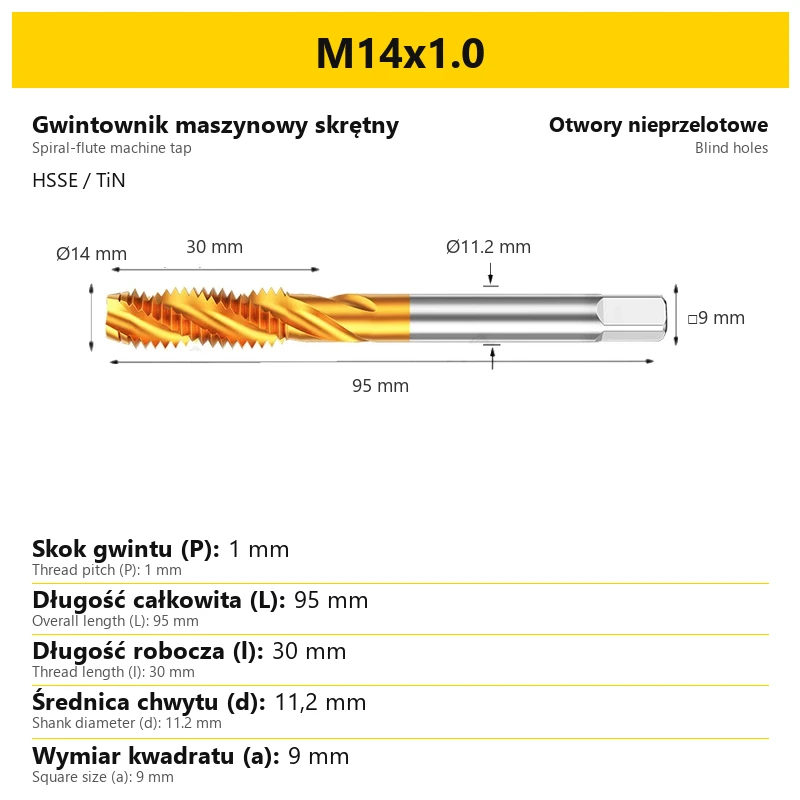
| M14x1.0 | 1 | 95 | 30 | Ø11.2 | 9 |
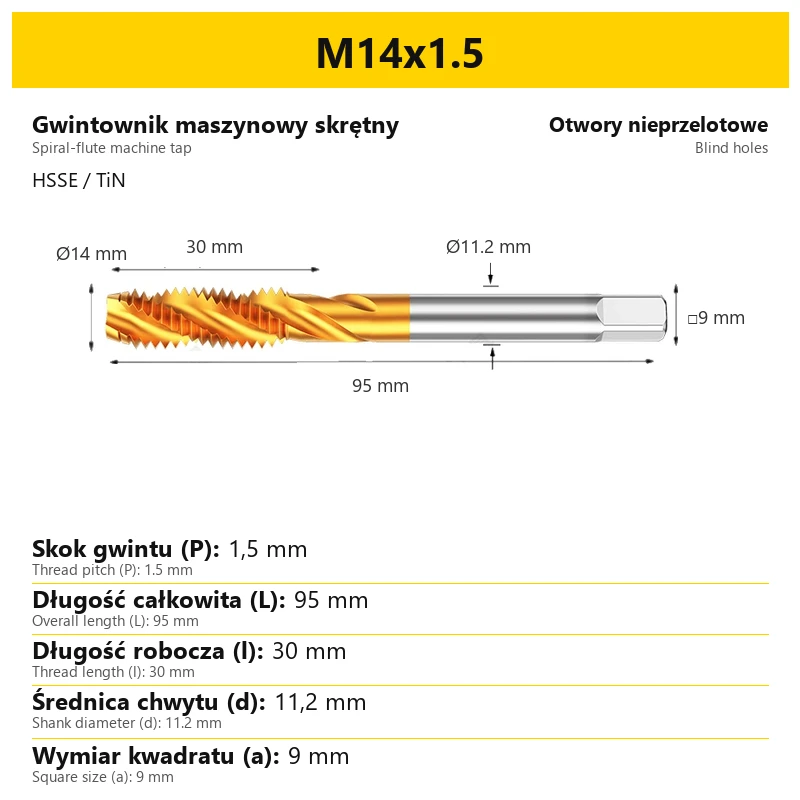
| M14x1.5 | 1.5 | 95 | 30 | Ø11.2 | 9 |
| M14x2 | 2 | 95 | 30 | Ø11.2 | 9 |
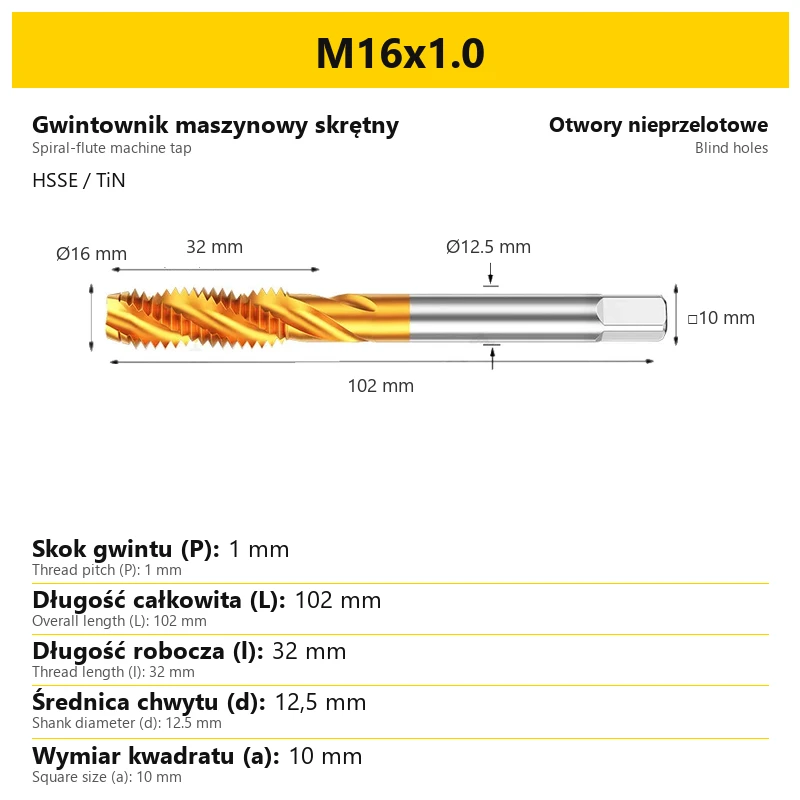
| M16x1.0 | 1 | 102 | 32 | Ø12.5 | 10 |
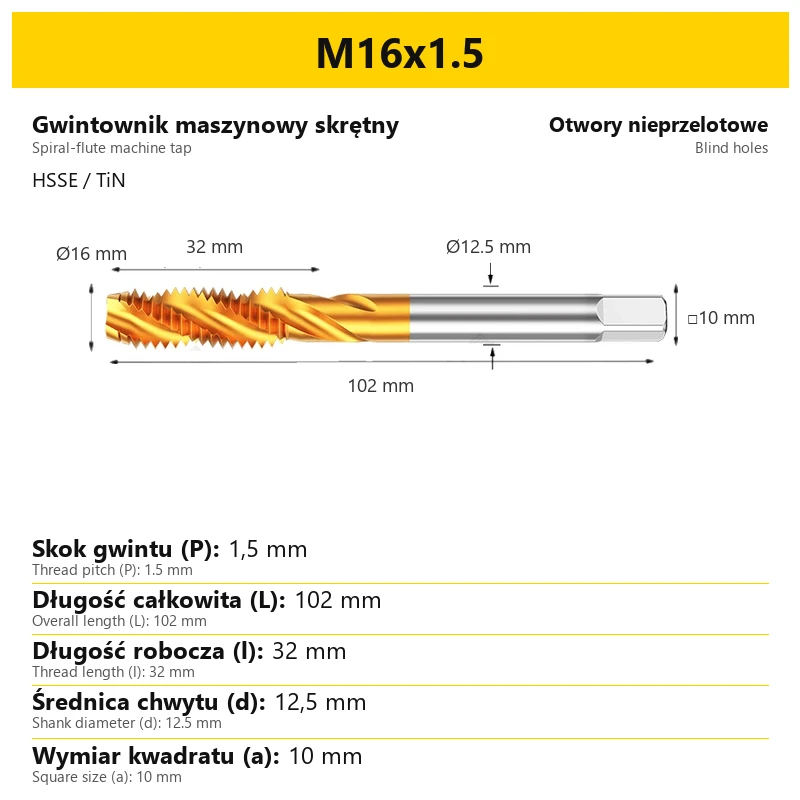
| M16x1.5 | 1.5 | 102 | 32 | Ø12.5 | 10 |
| M16x2 | 2 | 102 | 32 | Ø12.5 | 10 |
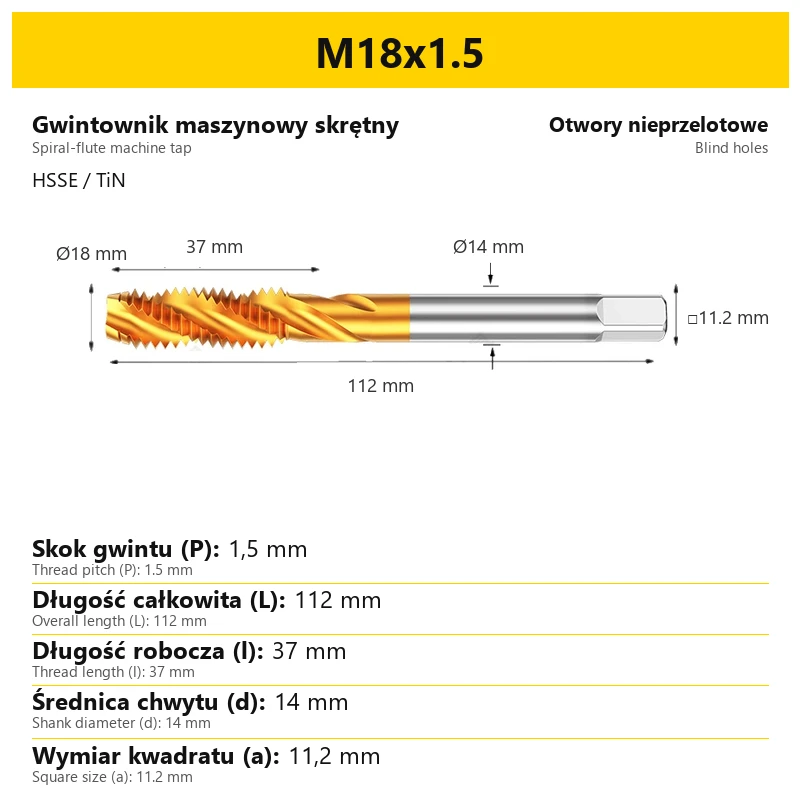
| M18x1.5 | 1.5 | 112 | 37 | Ø14 | 11.2 |
| M18x2.5 | 2.5 | 112 | 37 | Ø14 | 11.2 |
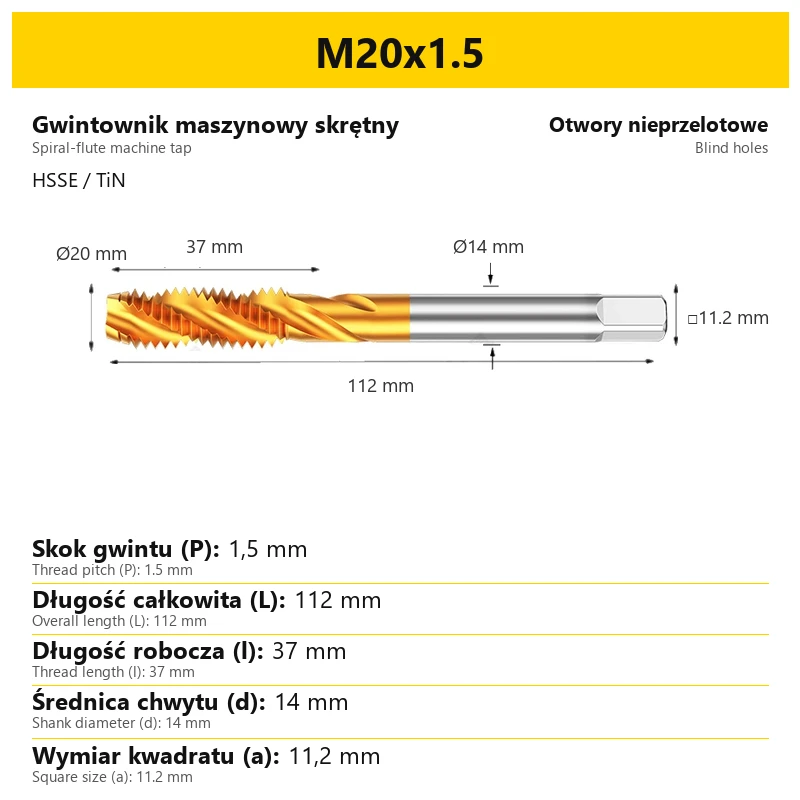
| M20x1.5 | 1.5 | 112 | 37 | Ø14 | 11.2 |
| M20x2.5 | 2.5 | 112 | 37 | Ø14 | 11.2 |
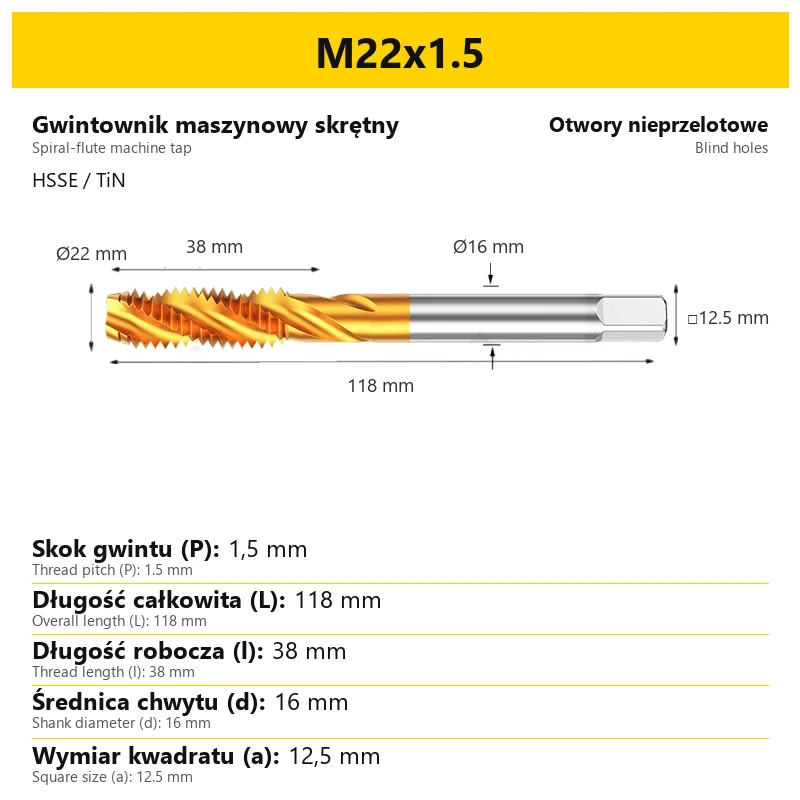
| M22x1.5 | 1.5 | 118 | 38 | Ø16 | 12.5 |
| M22x2.5 | 2.5 | 118 | 38 | Ø16 | 12.5 |
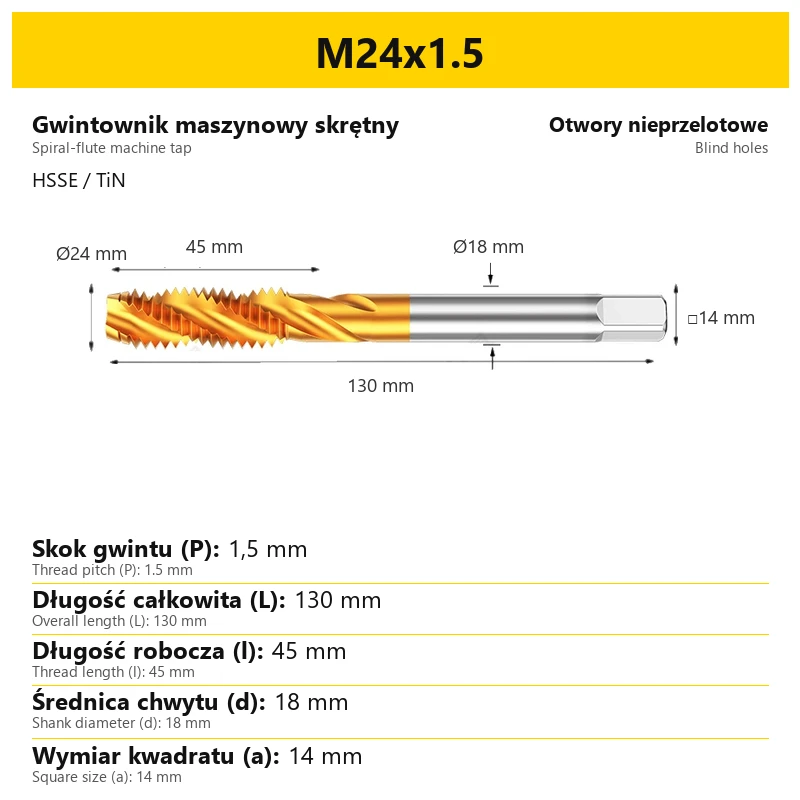
| M24x1.5 | 1.5 | 130 | 45 | Ø18 | 14 |
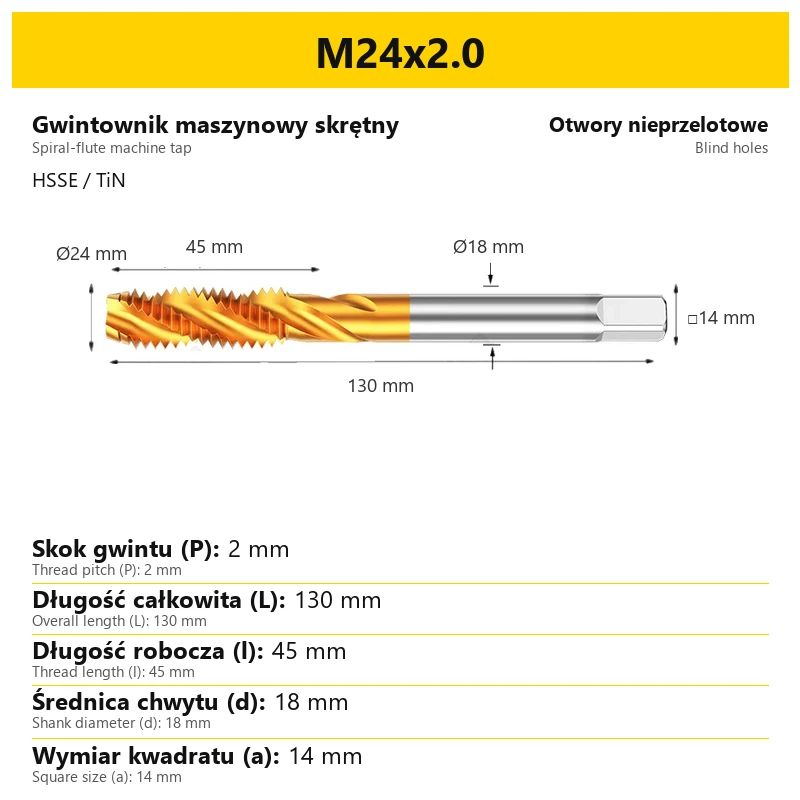
| M24x2.0 | 2 | 130 | 45 | Ø18 | 14 |
| M24x3.0 | 3 | 130 | 45 | Ø18 | 14 |
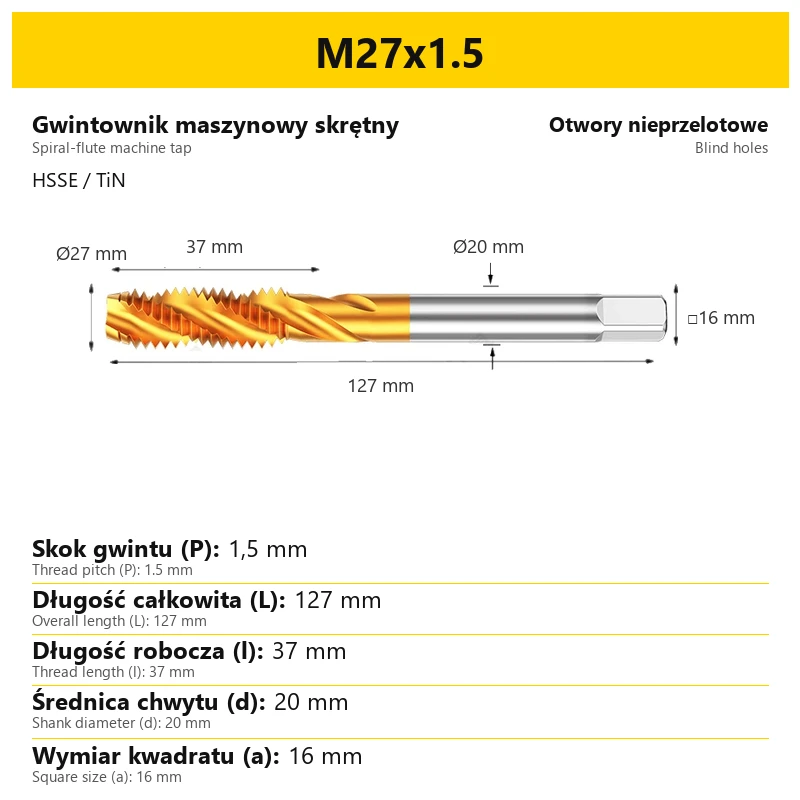
| M27x1.5 | 1.5 | 127 | 37 | Ø20 | 16 |
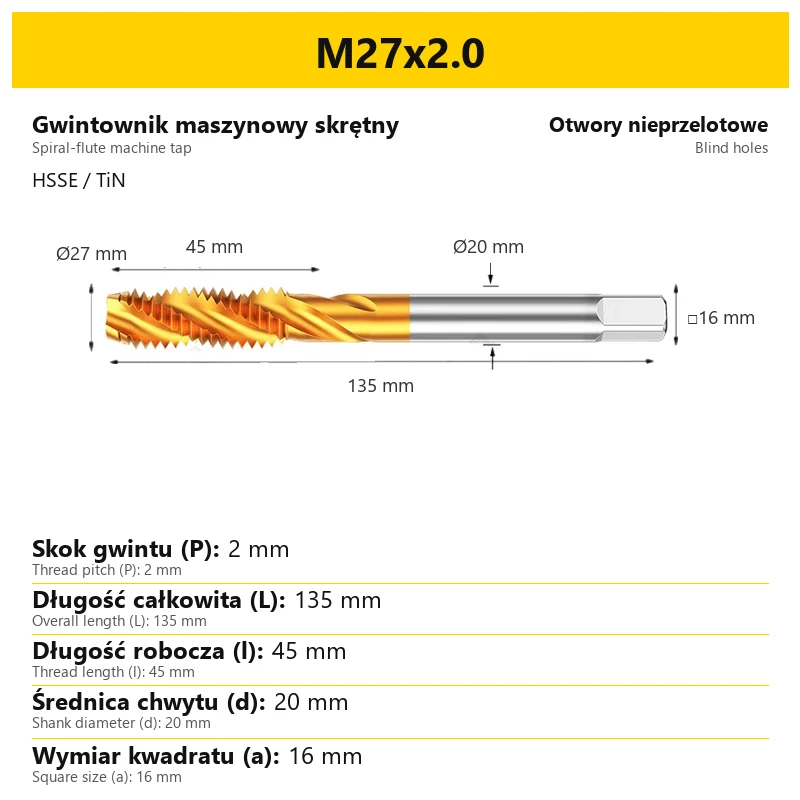
| M27x2.0 | 2 | 135 | 45 | Ø20 | 16 |
| M27x3.0 | 3 | 135 | 45 | Ø20 | 16 |
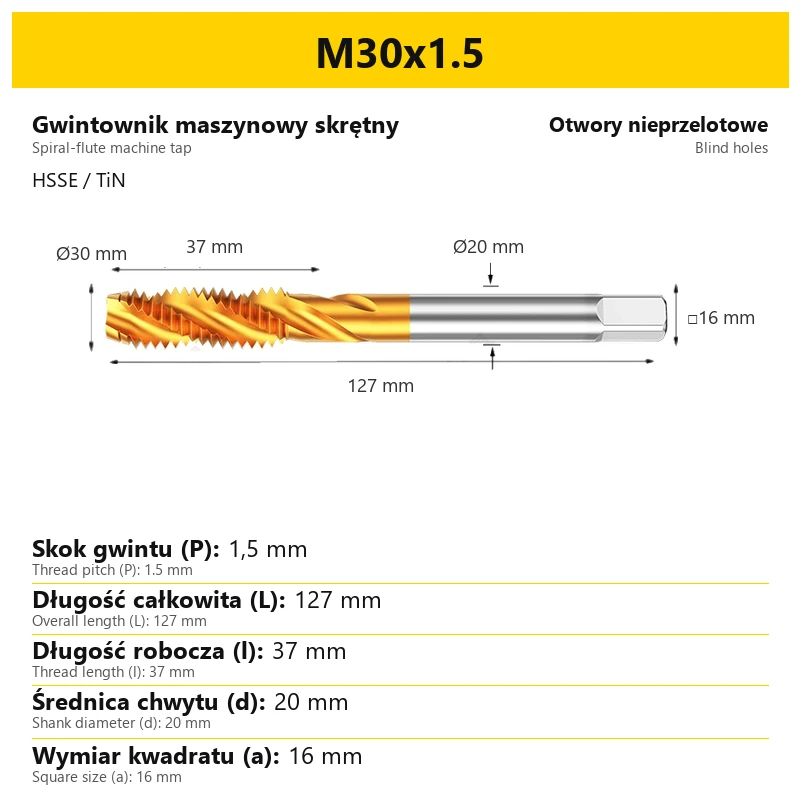
| M30x1.5 | 1.5 | 127 | 37 | Ø20 | 16 |
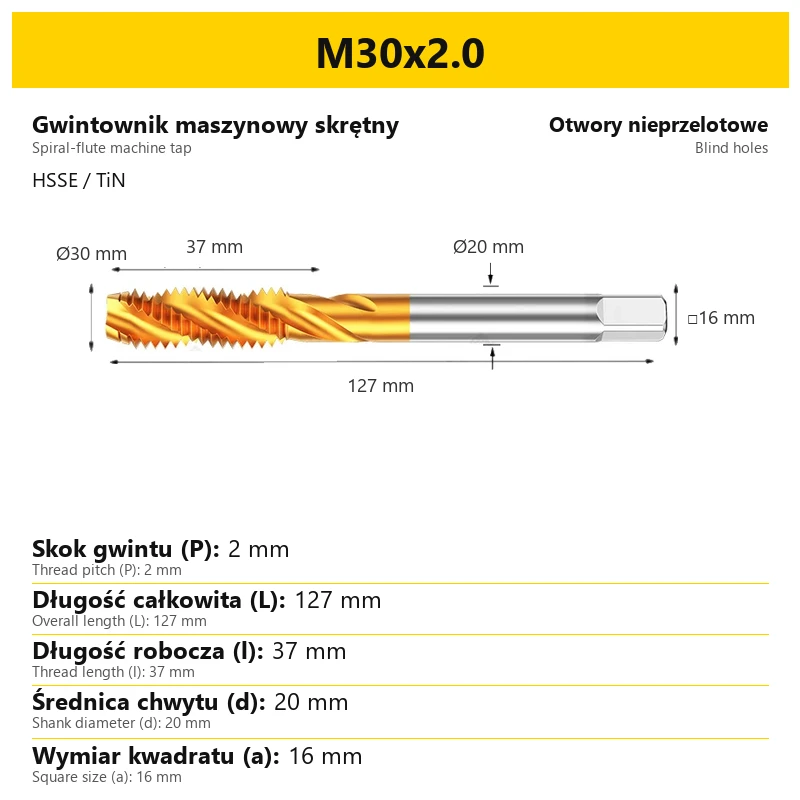
| M30x2.0 | 2 | 127 | 37 | Ø20 | 16 |
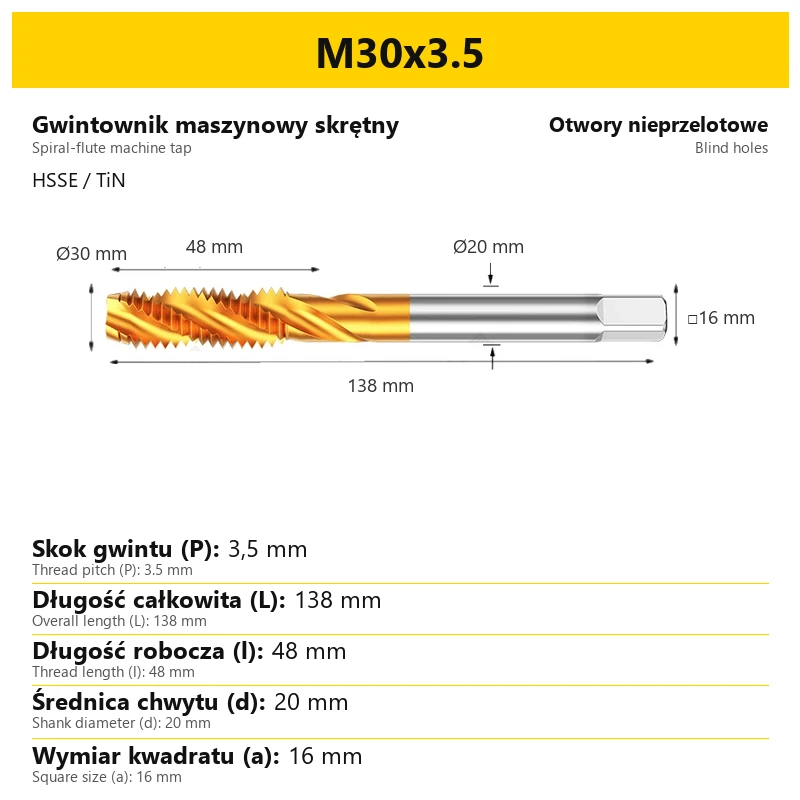
| M30x3.5 | 3.5 | 138 | 48 | Ø20 | 16 |
Selection and use
Select the tap for the hole type, workpiece material and required thread pitch. Check the shank diameter and square size against the holder. Use the correct tapping drill size, axial alignment and suitable lubrication. Leave clearance at the bottom of a blind hole for the tap lead.
Related products
-
253C-280A0Bestseller
 BT Tap Holders 5.00
Threading holder SK, BT, HSK63 | TER | ER/ERG Bushing Holder | Thread M2 - M36 | ERG sleeve holder set
-
07B7-296CF_2Bestseller
 Thread Mills 0.00
Thread Milling Cutter M0.8-M20 - Single Flute DLC
-
45A4-7408EBestseller
 JIS Taps 0.00
Straight Flute Machine Tap HSSE - TiN Coated M2-M30 ISO
-
BD5F-770CABestseller
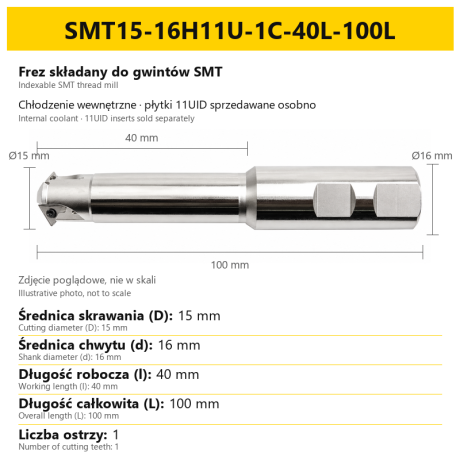
SMT threading head with cooling for UID inserts | Folding cutter


Bestsellers
-
Bestseller
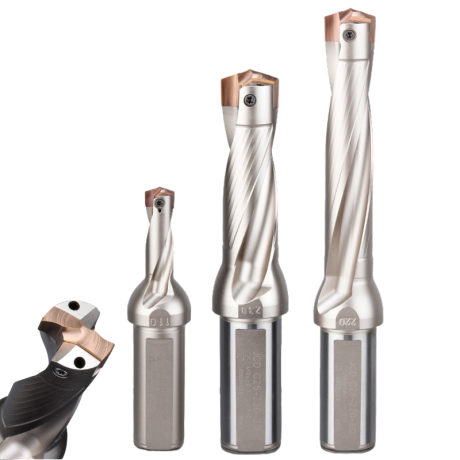
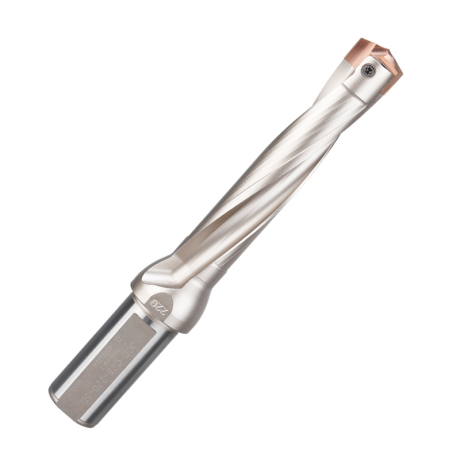
JCD modular drill with replaceable tip - internal cooling, for deep holes | GrotXD
JCD C20-100-3D Ø10~10.9 JCD C20-110-3D Ø11~11.9 JCD C20-120-3D Ø12~12.9 JCD C20-130-3D Ø13~13.9 JCD C20-140-3D Ø14~14.9 + 61 morePrice €69.86Price €56.79without VAT -
Bestseller
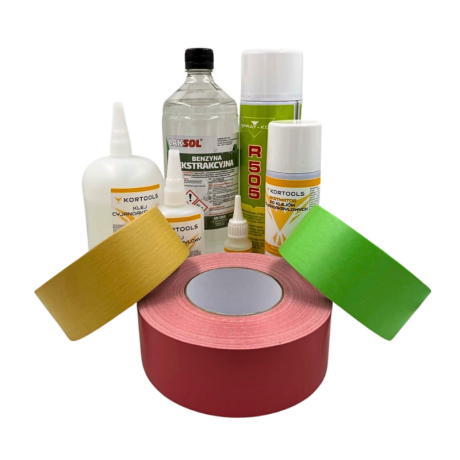
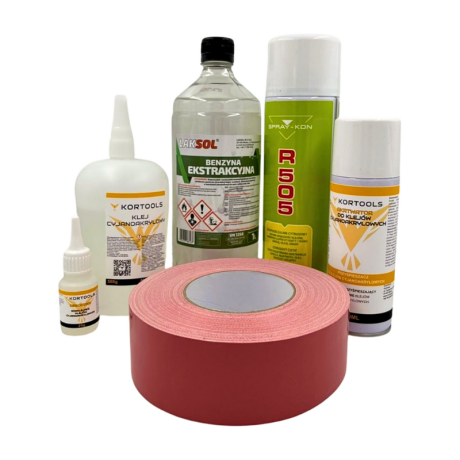
Kortools Adhesive + Tape CNC Workholding Kit
Yellow tape 5cm x 50m; adhesive 100g Yellow tape 5cm x 50m; adhesive 500g Yellow tape 10cm x 50m; adhesive 100g Yellow tape 10cm x 50m; adhesive 500g Green tape 5cm x 50m; adhesive 100g + 7 morePrice €44.66Price €36.31without VAT -
Price €17.18Price €13.97without VAT
-
Price €7.10Price €5.77without VAT
-
Price €7.56Price €6.14without VAT
-
Bestseller
 Other Accessories 0.00
CNC Chip Fan / Chip Blower
Complete CNC chip fan Kit: blades, springs, pins and screwsPrice €53.82Price €43.76without VAT -
Bestseller
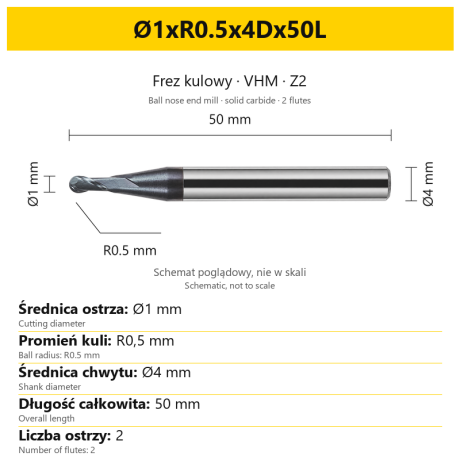 Ball Nose End Mills 0.00
2-Flute Carbide Ball Nose End Mill - HYPERCUT
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 26 morePrice €10.14Price €8.25without VAT -
Bestseller
 2-Flute End Mills 0.00
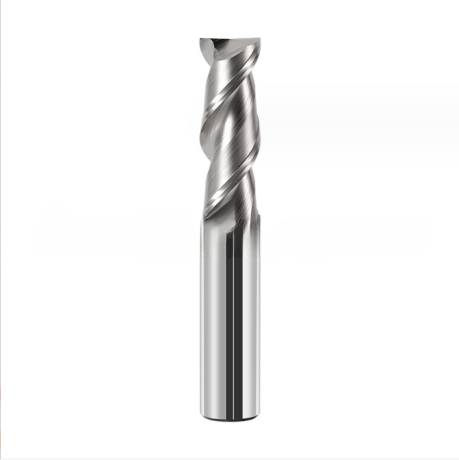
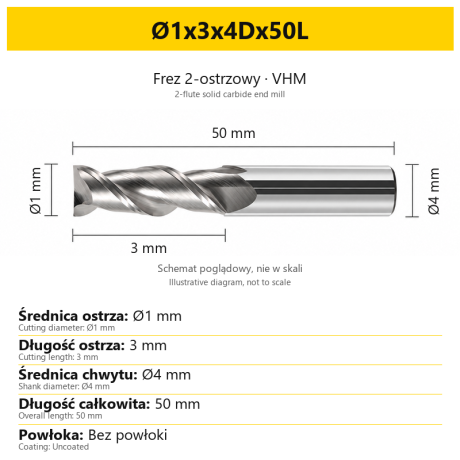
2-Flute Carbide End Mill for Aluminium
Ø1x3x4Dx50L Ø1.5x4x4Dx50L Ø2x6x4Dx50L Ø2.5x7.5x4Dx50L Ø3x9x3Dx50L + 31 morePrice €5.35Price €4.35without VAT -
Bestseller
 2-Flute End Mills 0.00
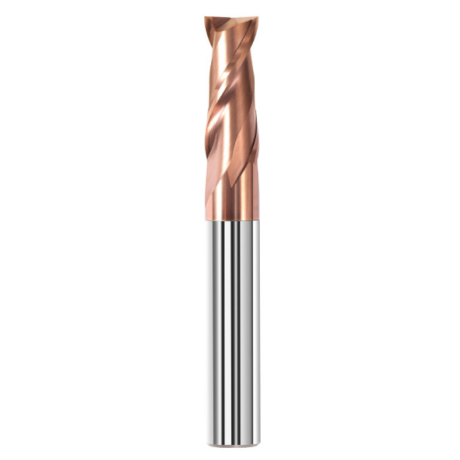
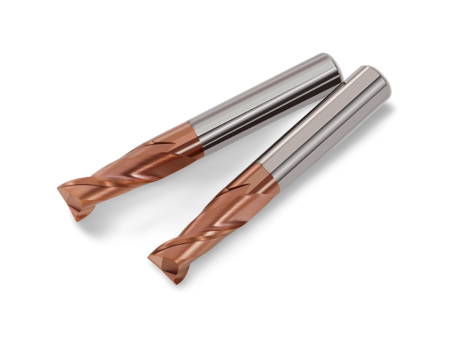
2-Flute Carbide End Mill for Steel 55 HRC - TiSiN - Solid Carbide
Ø6x24x6Dx75L Ø8x25x8Dx75L Ø4x20x4Dx100L Ø5x30x5Dx100L Ø6x30x6Dx100L + 31 morePrice €4.40Price €3.58without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute DLC Coated Carbide Ball Nose End Mill| DuraEdge Alu
Ø1.0xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2.0xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3.0xR1.5x3Dx50L + 34 morePrice €7.89Price €6.41without VAT -
Bestseller
 2-Flute End Mills 0.00
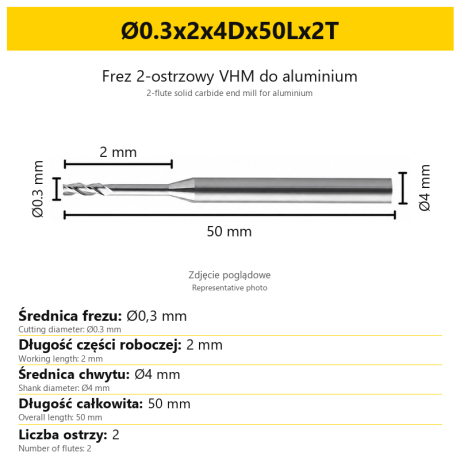
2-Flute End Mill for Aluminium | VHM | Miniature Ø0.3 - Ø0.9
Ø0.3x2x4Dx50Lx2T Ø0.3x3x4Dx50Lx2T Ø0.3x4x4Dx50Lx2T Ø0.4x2x4Dx50Lx2T Ø0.4x3x4Dx50Lx2T + 28 morePrice €7.99Price €6.50without VAT -
Bestseller
 Ball Nose End Mills 0.00
2-Flute TiSiN Coated Carbide Ball Nose End Mill
Ø1xR0.5x4Dx50L Ø1.5xR0.75x4Dx50L Ø2xR1x4Dx50L Ø2.5xR1.25x4Dx50L Ø3xR1.5x3Dx50L + 38 morePrice €7.28Price €5.92without VAT -
Bestseller
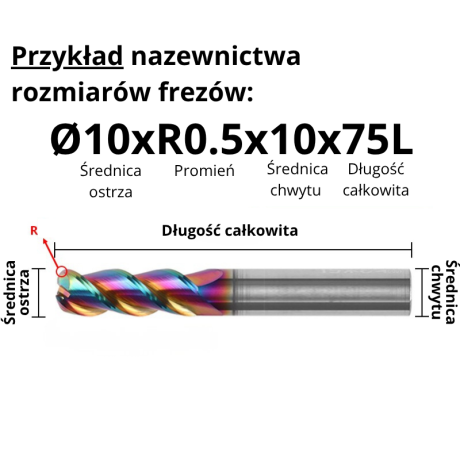
3-Flute Carbide Corner Radius End Mill for Aluminium| AL DLC
Ø1xR0.1x4Dx50L Ø1xR0.2x4Dx50L Ø1xR0.3x4Dx50L Ø1.5xR0.1x4Dx50L Ø1.5xR0.2x4Dx50L + 137 morePrice €4.96Price €4.04without VAT -
Bestseller
 3-Flute End Mills 0.00
3-Flute Carbide End Mill VHM Z-3 for Aluminium| TriMill AL
Ø1x3xD4x50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x9x3Dx50L + 41 morePrice €5.10Price €4.15without VAT -
Bestseller

 Countersinks 0.00
3-Flute Countersink Fi4.5-fi60, 90° - HSS-CO - 5% Kobaltu | Straight Shank
Ø4.5 x 4 x 90° x 40L Ø5 x 5 x 90° x 45L Ø6.3 x 5 x 90° x 45L Ø8.3 x 6 x 90° x 50L Ø10.4 x 6 x 90° x 50L + 12 morePrice €4.81Price €3.91without VAT -
Bestseller

 3-Flute End Mills 0.00
3-Flute DLC Coated Carbide End Mill | TriMill DLC AL
Ø1x3x4Dx50L Ø1.5x5x4Dx50L Ø2x6x4Dx50L Ø2.5x8x4Dx50L Ø3x8x3Dx50L + 38 morePrice €5.07Price €4.12without VAT


